
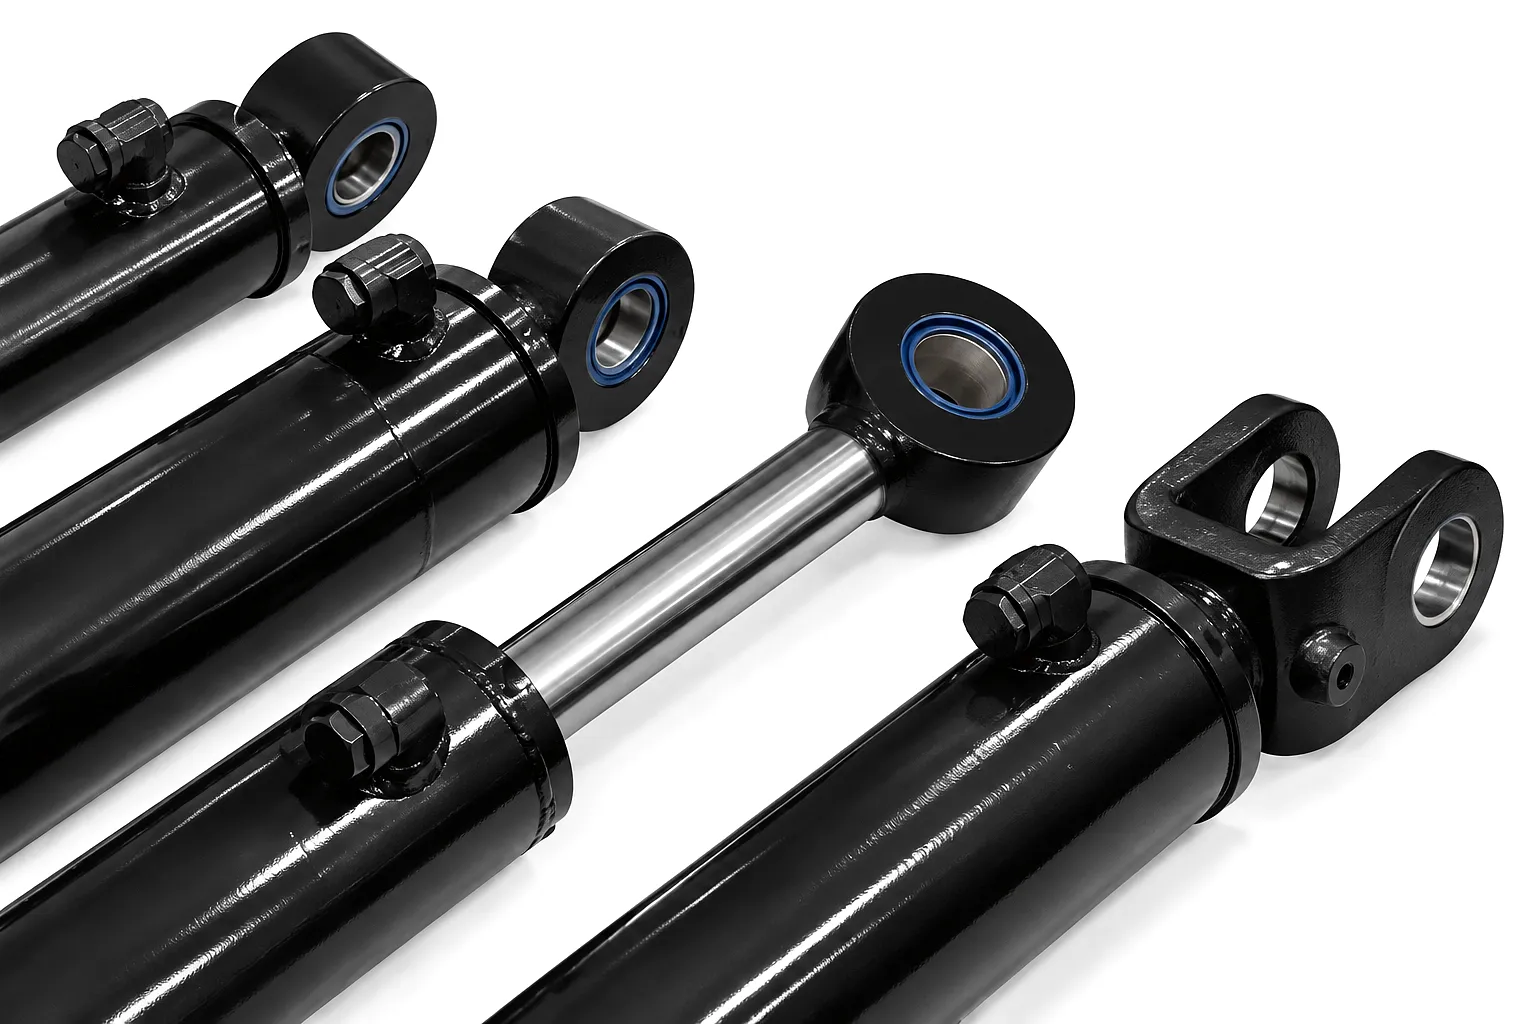
 Every time an excavator lifts its arm, curls a bucket through compacted clay, or reaches over a trench wall on a Birmingham ring-road project, the work is done by a deceptively compact component: the boom cylinder. These hydraulic actuators translate pressurised fluid into pure linear force, and in doing so they shoulder the entire mechanical burden of excavation. Despite being largely hidden inside steel-plated boom structures, boom cylinders are arguably the most load-critical parts of any earthmoving machine. When they perform well, site productivity flows without interruption; when they fail — through seal degradation, bore scoring, or chrome peel — downtime costs escalate rapidly, and in the UK’s competitive civil infrastructure market, idle plant can drain contract margins in hours.
This guide covers everything a plant engineer, fleet manager, or procurement specialist needs to understand about excavator boom cylinders — from the physics of double-acting cylinder design and the metallurgy of cylinder bores, through to performance specifications, replacement decision criteria, and sourcing considerations for UK-based operations. Whether you manage a fleet of 5-tonne mini-excavators working in Glasgow’s urban redevelopment zones, or 45-tonne demolition machines operating across Sheffield’s steel-works clearance sites, the principles remain consistent: quality engineering, correct specification, and timely replacement determine operational success.
How the Boom Cylinder Actually Works
The Double-Acting Principle
An excavator boom cylinder operates on the double-acting hydraulic principle, which means pressurised fluid is applied alternately to both the cap end and the rod end of the cylinder barrel. When the operator pushes the joystick forward to raise the boom, the machine’s hydraulic pump — typically delivering fluid at pressures between 280 and 380 bar — directs oil into the cap-end port. This pressure acts across the full internal bore area of the piston, generating the enormous thrust needed to lift tonnes of steel, soil, and aggregate. To lower the boom in a controlled manner, oil is redirected to the rod-end port, and return fluid from the cap end passes back through proportional control valves to the tank. The ability to generate power in both directions is what separates a double-acting cylinder from a single-acting ram and makes it indispensable for precise excavation work where gravity-assisted return is neither safe nor sufficient. This bidirectional hydraulic control is the engineering foundation upon which modern excavator performance is built, and it is why boom cylinders must be manufactured to tolerances that prevent internal bypassing even at peak system pressures.
Force, Stroke, and Geometry
The pushing force generated at the cap end is calculated as pressure multiplied by the full bore cross-sectional area (F = P × A), while the pulling force at the rod end is slightly lower because the rod itself occupies a portion of the piston’s annular area. This difference is a fundamental geometric characteristic of all asymmetric hydraulic cylinders, and engineers account for it when sizing boom lift versus curl circuits. Stroke length — the total travel from fully retracted to fully extended — directly determines how high the boom can rise and how far the machine can reach. On a typical 20-tonne hydraulic excavator common on infrastructure projects around Birmingham and the M6 corridor, boom cylinder strokes range from 1,100 mm to 1,500 mm. Getting stroke specifications exactly right during replacement is non-negotiable: a cylinder that is 20 mm too short will leave unused boom range, while one that is marginally too long risks damaging the boom structure at full extension, since the hydraulic system’s travel-stop function may not compensate accurately for the dimensional mismatch.
It is also worth understanding the role of the cylinder’s mounting geometry in determining the effective mechanical advantage at different boom angles. As the boom rises from horizontal to maximum elevation, the angle between the cylinder’s line of action and the boom arm changes continuously. At shallow boom angles — typical during digging cycles — the cylinder operates close to its ideal leverage position, delivering high breakout force. As the boom approaches vertical, the leverage angle becomes less favourable, and the hydraulic system must work harder to maintain the same tip force. This is why experienced plant operators develop an instinctive feel for managing boom angle relative to payload weight, a skill that also reduces thermal load on the hydraulic circuit and extends seal life in the boom cylinders themselves.
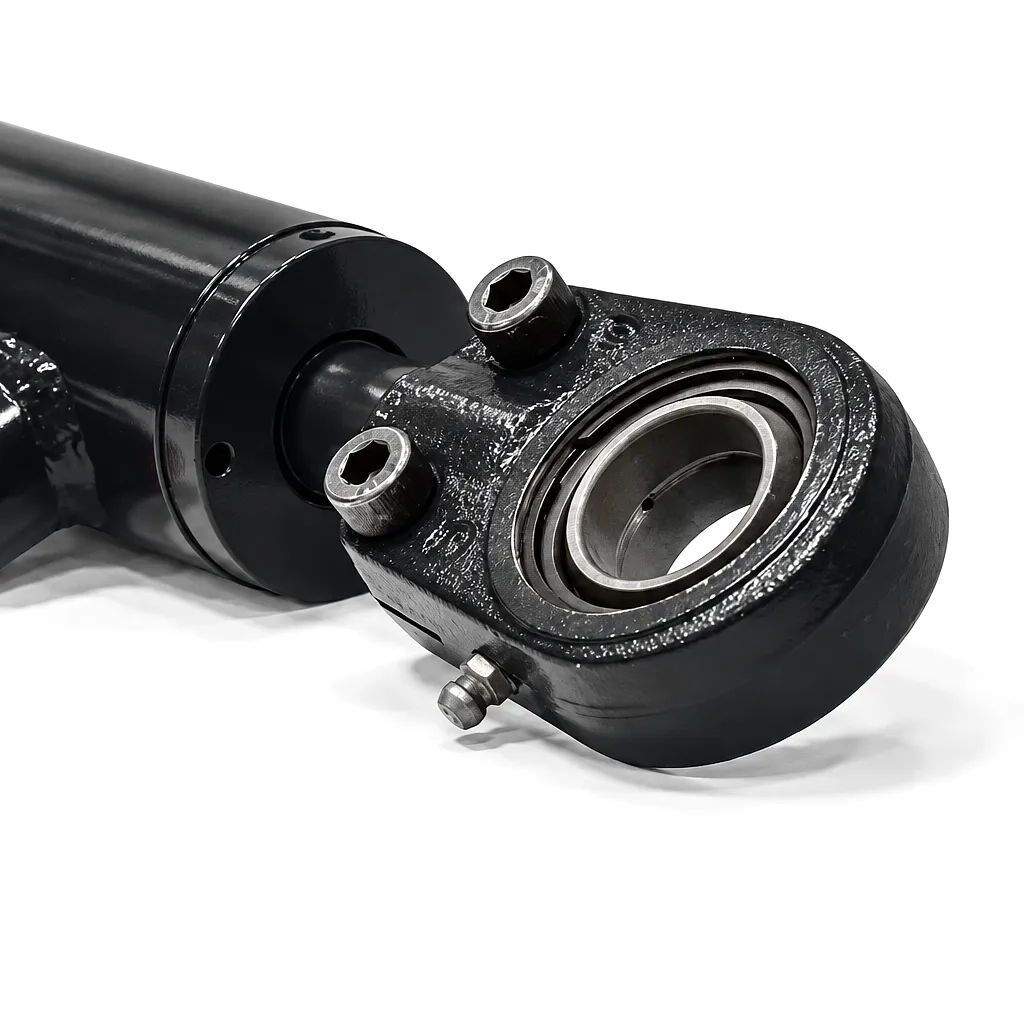
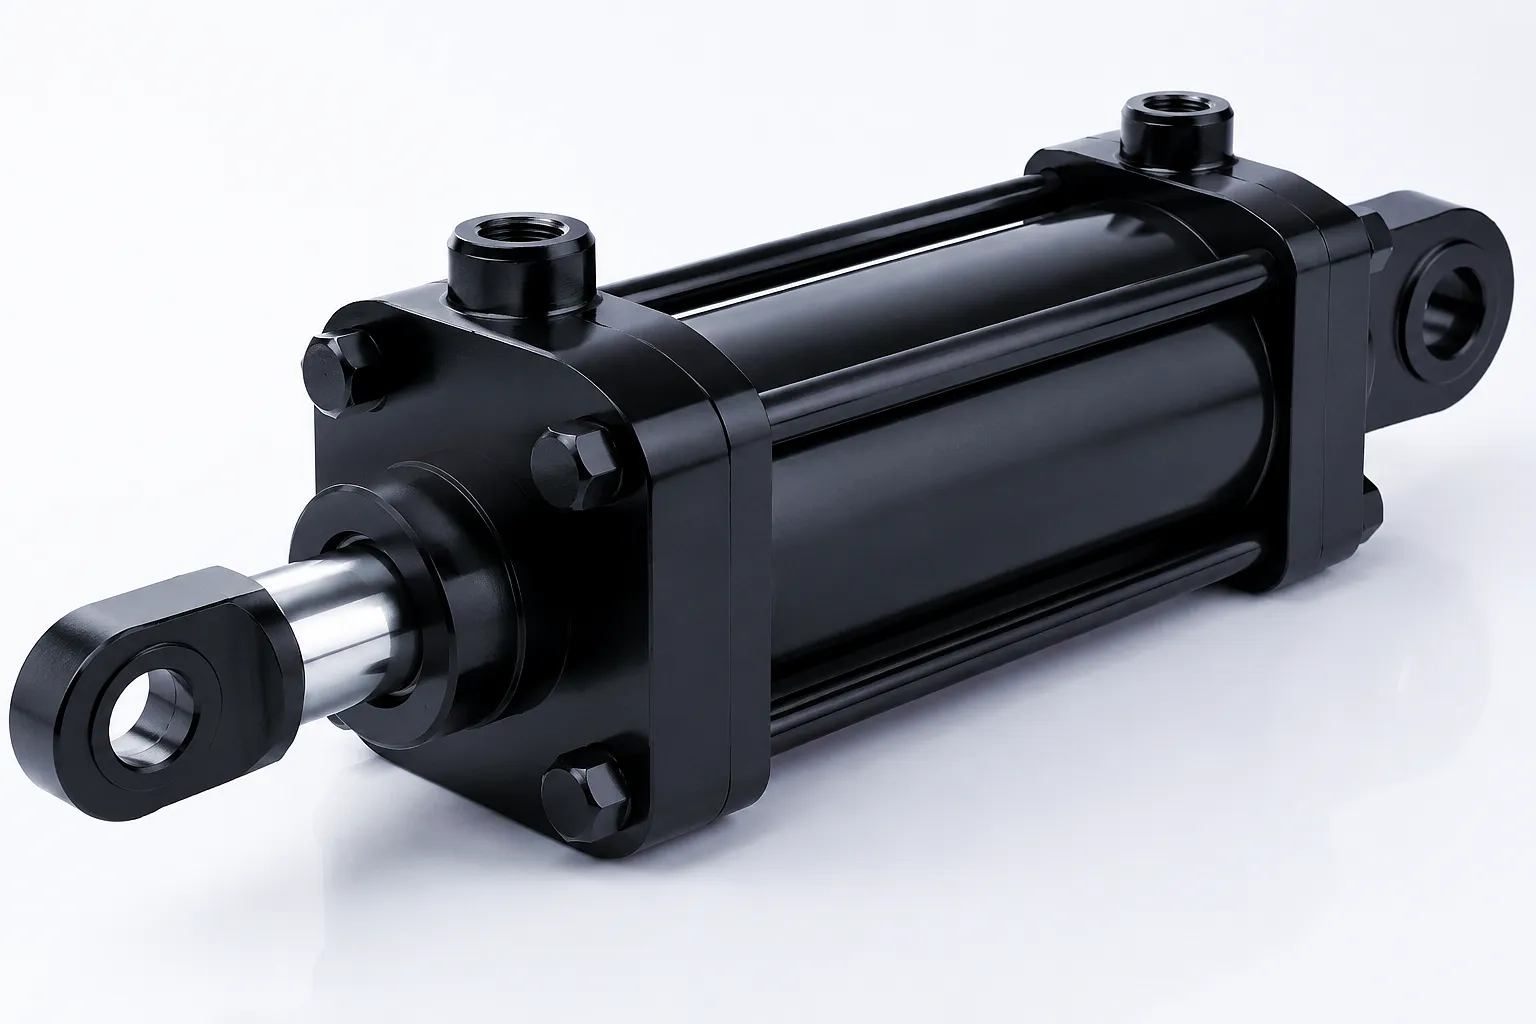
Ever Power precision-engineered boom cylinders — built for high-duty excavation cycles
Core Materials in Boom Cylinder Manufacture
The materials selected for each component of a boom cylinder determine its fatigue life, corrosion resistance, and dimensional stability under cyclic pressure loading. There is no single “best” material — the correct choice depends on bore diameter, operating pressure, ambient environment, and replacement cycle philosophy. Below is a breakdown of the key materials used in high-duty excavator boom cylinders, along with the engineering rationale behind each selection.
Κύλινδρος βαρελιού
Cold-drawn seamless steel tube, typically EN 10305-1 specification with carbon content optimised for honing. The bore is precision-honed to Ra 0.2–0.4 µm surface finish to ensure reliable seal contact without abrasive wear. Wall thickness is engineered to maintain a safety factor of at least 4:1 against burst pressure, typically exceeding 350 bar operating rating.
Ράβδος εμβόλου
CK45 or 42CrMo4 induction-hardened steel with hard chrome plating applied to 20–30 µm thickness, subsequently ground and polished to Rz 4 µm or better. The chrome layer resists corrosion from UK site conditions — frequent rain, clay contamination, and salt-laden winter air — while providing the hardness (HV 850+) needed to resist seal-induced scoring during millions of operational cycles.
Piston & Seals
Pistons are machined from ductile cast iron or low-alloy steel, carrying a composite seal stack that includes PTFE guide rings, polyurethane dynamic seals, and a back-up NBR O-ring. The seal compound is selected based on fluid type and temperature range — typically -20°C to +100°C for UK ambient operations. High-performance variants use Viton seals for extended thermal range or contaminated fluid tolerance.
Gland / End Caps
Machined from EN24T or equivalent high-tensile steel, the front gland retains the rod seal assembly and is typically secured via a fine-thread engagement or retaining ring. Correct gland torque during assembly — usually specified between 300 and 500 Nm depending on cylinder bore — is critical to preventing gland backing out under vibration, a failure mode observed on plant operating on rough demolition terrain such as brownfield sites in the Midlands.
Boom Cylinder Technical Performance Parameters
The table below covers the typical technical parameters for Ever Power boom cylinders across the most common excavator weight classes deployed on UK construction, demolition, and quarrying sites. Custom specifications are available on request — contact our engineering team to discuss dimensional matching, pressure ratings, or special material requirements.
| Παράμετρος | Mini (1–6t) | Mid (8–20t) | Large (22–45t) | Heavy-Duty (50t+) |
|---|---|---|---|---|
| Bore Diameter | 60–80 mm | 100–140 mm | 150–200 mm | 210–280 mm |
| Διάμετρος ράβδου | 40–55 mm | 65–95 mm | 100–140 mm | 150–200 mm |
| Μήκος πινελιάς | 450–750 mm | 900–1,300 mm | 1,200–1,700 mm | 1,500–2,200 mm |
| Operating Pressure (max) | 280 bar | 320 bar | 350 bar | 380 bar |
| Test Pressure (1.5× working) | 420 bar | 480 bar | 525 bar | 570 bar |
| Rod Surface Hardness | HV 850+ | HV 850+ | HV 850+ | HV 900+ |
| Chrome Layer Thickness | 20–25 µm | 25–30 µm | 25–35 µm | 30–40 µm |
| Seal Material (standard) | PU / PTFE / NBR | PU / PTFE / NBR | PU / PTFE / Viton | Viton / PTFE / NBR |
| Θερμοκρασία λειτουργίας | -20°C to +80°C | -20°C to +90°C | -30°C to +100°C | -30°C to +110°C |
| Υλικό βαρελιού | ST52-3 seamless | ST52-3 seamless | EN 10305-1 seamless | EN 10305-1 / 42CrMo4 |
| Typical Push Force (cap end) | 79–140 kN | 251–616 kN | 883–1,100 kN | 1,200–2,300 kN |
Why Ever Power Boom Cylinders Deliver a Competitive Advantage
Not all hydraulic cylinders perform equally. These are the engineering advantages that separate precision-manufactured boom cylinders from low-cost commodity units — and why UK plant operators return to Ever Power for their replacement requirements.
Zero-Leakage Seal Engineering
Our seal stacks combine polyurethane dynamic seals with PTFE anti-extrusion rings in a carefully sequenced arrangement that achieves leak-free operation across the full pressure range. This eliminates the hydraulic fluid contamination of surrounding soil — particularly important on UK groundworks projects where environmental permit conditions strictly prohibit hydrocarbon release into waterways.
Hard Chrome Rod Technology
The piston rod surface undergoes induction hardening to a base hardness of 50–55 HRC before chrome plating, producing a layered defence against both mechanical scoring and electrochemical corrosion. Testing to ISO 10763 salt spray standards confirms 500+ hours of coating integrity — an important performance threshold for excavators working year-round on UK coastal infrastructure contracts where sea-spray salinity accelerates corrosion on exposed chrome surfaces.
Precision Honing to Ra 0.2 µm
Cylinder bore honing is performed on CNC honing machines with in-process gauging, achieving bore diameter tolerances of H7 and surface roughness within Ra 0.2–0.4 µm. This level of precision is essential for long seal life: an overly rough bore surface acts like fine sandpaper on polyurethane seals, dramatically shortening their functional life. Our bore quality guarantees that seal replacement intervals exceed those of equivalent competitor cylinders by a measurable margin in controlled test conditions.
Fatigue-Rated Weld Joints
All structural weld joints on end caps and clevis mounts are rated to withstand 2 million load cycles at 90% of maximum working pressure without crack initiation, following EN 13480 fatigue classification. This specification directly addresses the failure mode most commonly seen on aggressively used plant: circumferential cracking at the barrel-to-cap weld junction, triggered by high-frequency vibration during rock-breaking or demolition attachment operations — both extremely common across Northern England’s active demolition sector.
Cross-Brand OEM Compatibility
Ever Power boom cylinders are engineered as direct-fit replacements for the most widely operated excavator brands on UK sites, including Caterpillar, Komatsu, Hitachi, JCB, Volvo, and Doosan. Each replacement unit is dimensionally verified against OEM drawings, with pin-to-pin eye distances, bore and rod diameters, and port thread specifications confirmed before despatch. This eliminates the adaptation work — and the associated risk — that comes with poorly matched aftermarket cylinders sourced without proper dimensional checks.
Rapid UK Despatch
With a dedicated logistics partnership serving UK mainland addresses, standard stock boom cylinders are despatched within 3–5 working days of order confirmation. Express pallet delivery via our UK freight partner can place replacement units on site in Birmingham, Manchester, or Leeds within 24 hours of collection from our warehouse facility. For project-critical machine downtime, our sales team can advise on available stock by phone or email to minimise plant idle time and protect programme dates.
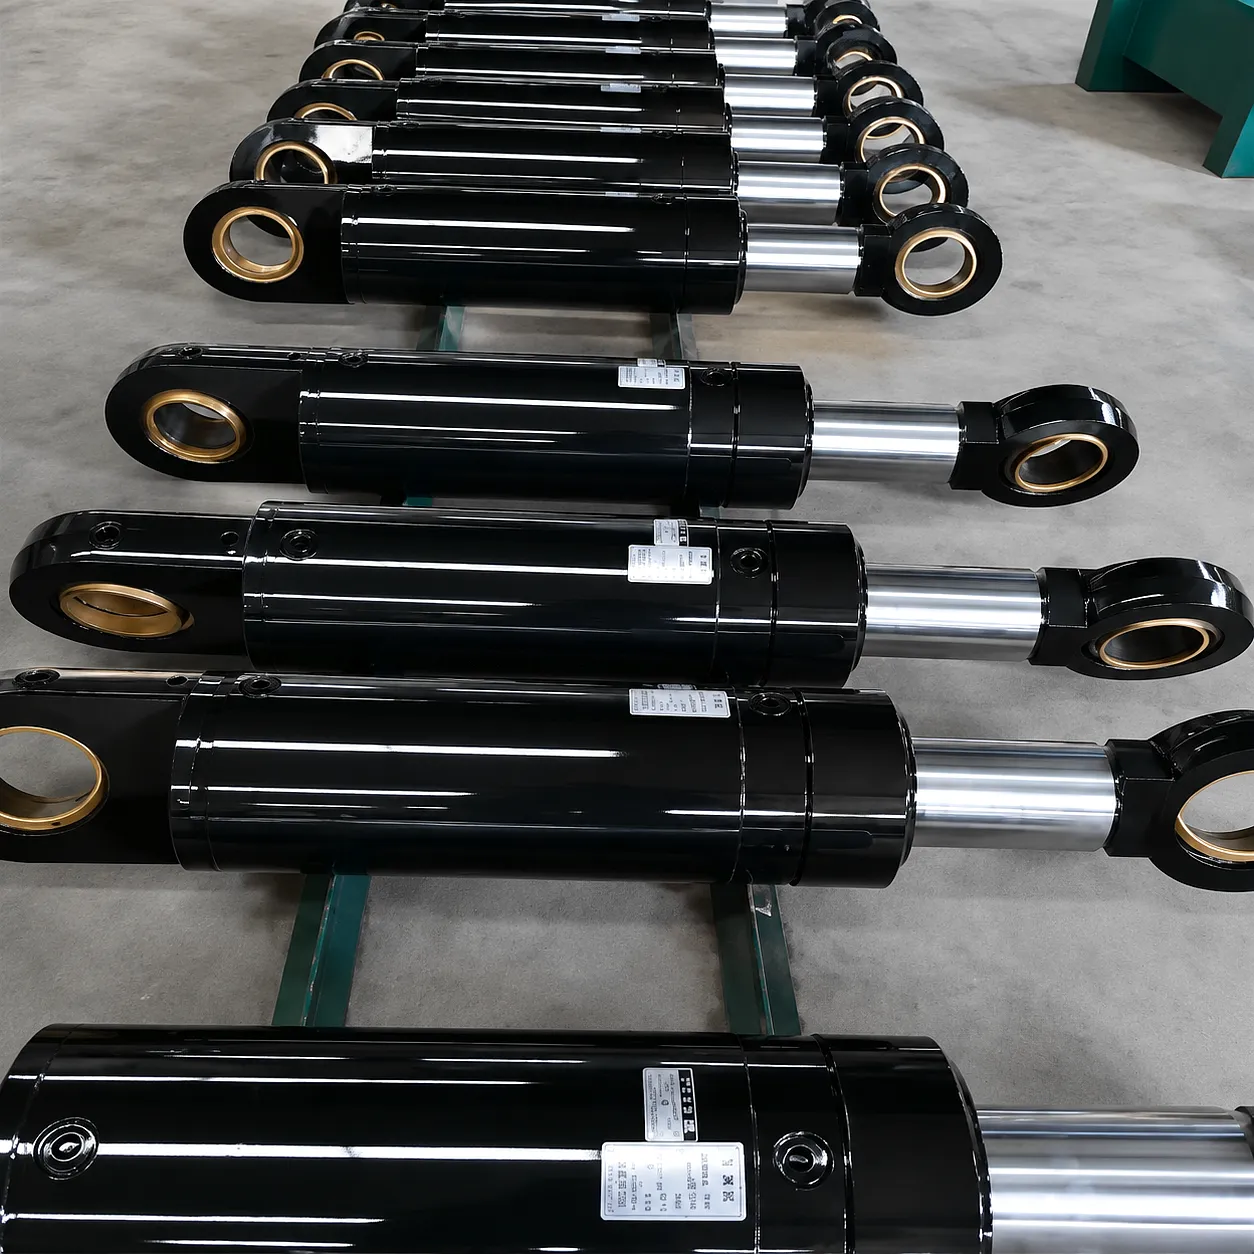
Industrial Application Scenarios for Excavator Boom Cylinders
Replacement Decision Guide: When to Replace vs. Rebuild
Deciding whether to reseal an existing boom cylinder or replace it outright is one of the most common cost decisions facing UK plant managers. The answer depends on the condition of the barrel bore and the piston rod surface. If these are undamaged, a professional reseal at a qualified hydraulic workshop can restore full function at 30–50% of replacement cost. If bore scoring, chrome peel, or taper is found on inspection, full replacement is almost always the more economical path — because a new seal set installed into a damaged bore will fail again within weeks.
Signs That a Reseal Is Sufficient
- Slow external weeping around the gland with no oil pooling on the ground
- Rod surface is visually clean, free from scoring, pitting, or chrome delamination
- Cylinder extends and retracts smoothly with no hesitation or barrel-side drift
- Machine has fewer than 2,000 hours since last seal service
- No visible deformation at the clevis eyes or barrel weld seams
Signs That Full Replacement Is Needed
- Active oil leakage onto ground, triggering environmental compliance concern
- Visible chrome peel, axial scoring marks, or corrosion pitting on the rod
- Cylinder drifts under load when the circuit is held static (internal bypass)
- Barrel shows circumferential cracking near end cap welds
- Replacement cost of bore re-sleeve plus reseal approaches or exceeds new cylinder price
- Machine is high-output fleet plant where downtime risk outweighs repair cost savings
Inspection Checklist Before Ordering
- Record the machine model, serial number, and year
- Measure pin-to-pin extended and retracted lengths
- Record bore diameter and rod diameter (visible on gland face or OEM data)
- Note port thread type and connection orientation (SAE or BSP)
- Ελέγξτε τη διάμετρο της οπής του στελέχους διχάλας και τις προδιαγραφές υλικού πείρου
- Σημειώστε τυχόν μη τυποποιημένη γεωμετρία τοποθέτησης σε σχέση με το σχέδιο OEM
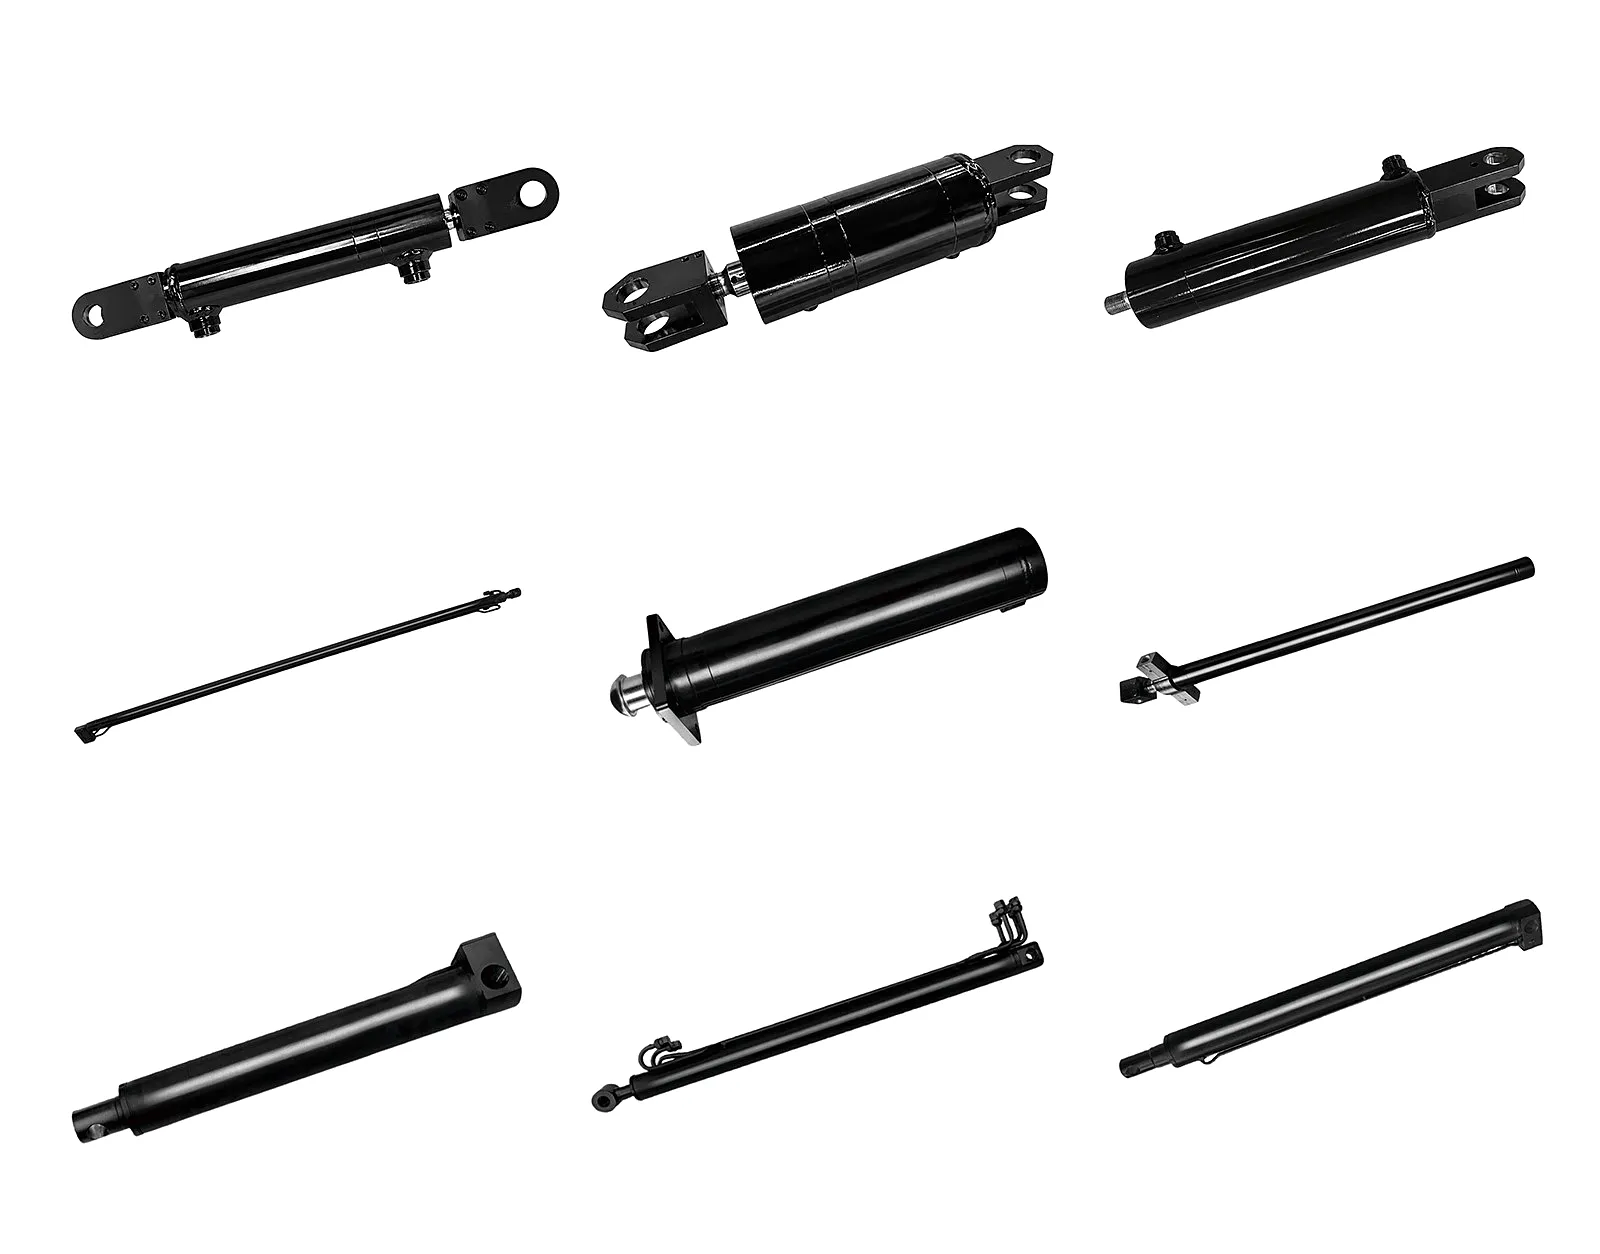
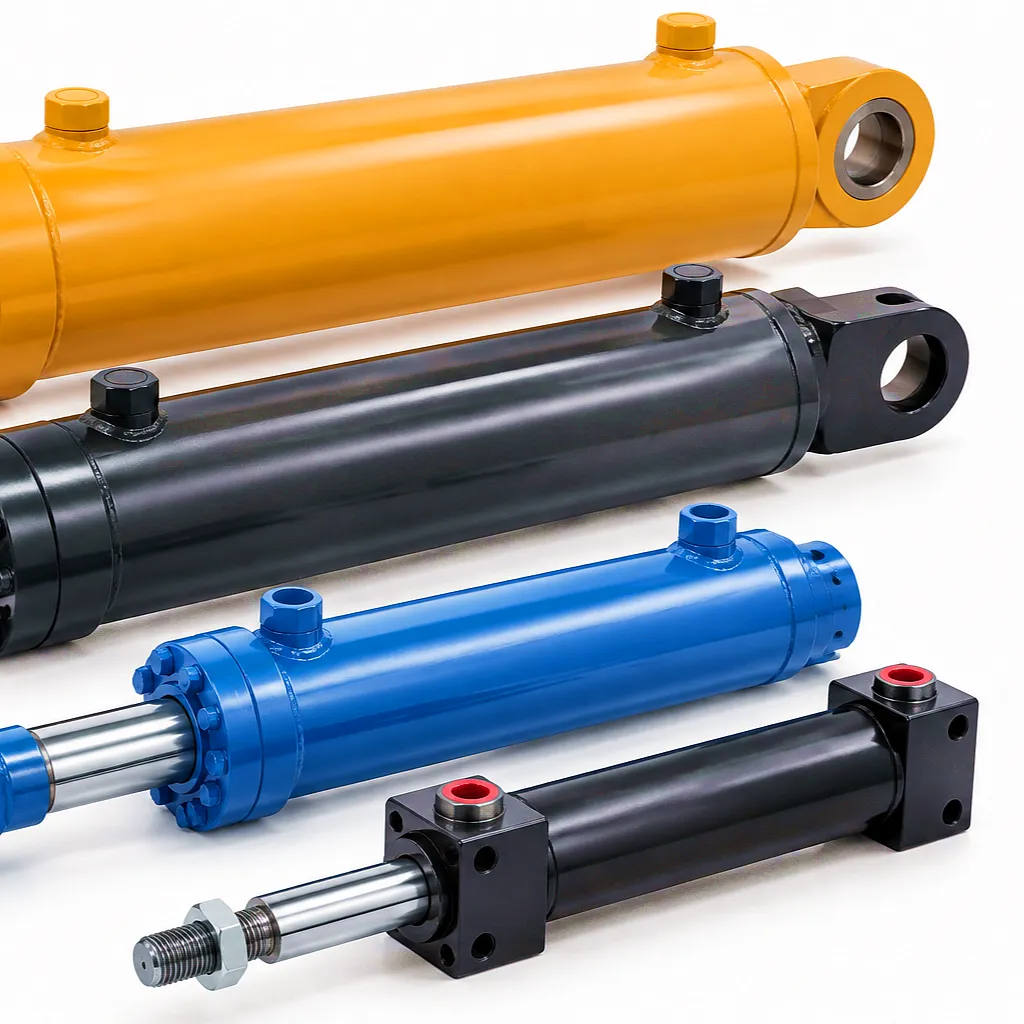
Πλήρης γκάμα προϊόντων Ever Power — κύλινδροι μπούμας για εκσκαφείς από 1 τόνο έως 100 τόνους+ λειτουργικό βάρος
Πάντα Ισχυρή Παραγωγή: Ακρίβεια, Προσαρμογή και Ισχύς Εφοδιαστικής Αλυσίδας
Η Ever Power λειτουργεί μια κάθετα ολοκληρωμένη μονάδα παραγωγής υδραυλικών κυλίνδρων, εξοπλισμένη με κέντρα τόρνευσης CNC, γραμμές ακριβείας λείανσης, ρομποτικά κελιά συγκόλλησης και μια πιστοποιημένη κατά ISO μονάδα δοκιμών πίεσης, ικανή να δοκιμάζει κυλίνδρους έως και 600 bar. Αυτή η υποδομή παραγωγής, σε συνδυασμό με μια αλυσίδα εφοδιασμού που βασίζεται σε σχέσεις με προμηθευτές χάλυβα με πιστοποίηση EN και υλικών στεγανοποίησης, επιτρέπει στην Ever Power να προσφέρει ένα επίπεδο δυνατότητας προσαρμογής που λίγοι προμηθευτές υδραυλικών κυλίνδρων που εξυπηρετούν την αγορά του Ηνωμένου Βασιλείου μπορούν πραγματικά να ανταγωνιστούν σε ανταγωνιστικούς χρόνους παράδοσης.
Προσαρμογή οπής
Μη τυποποιημένα μεγέθη οπών από 30 mm έως 450 mm, κατεργασμένα με ανοχή H7 ως στάνταρ προσφορά, με μη κυκλικά προφίλ οπών διαθέσιμα για εξειδικευμένες εφαρμογές κατόπιν αιτήματος.
Επιλογές επιφάνειας ράβδου
Σκληρό χρώμιο (στάνταρ), κεραμικό χρώμιο, νικέλιο-χρωμίου για ναυτιλιακές εφαρμογές και θερμικός ψεκασμός καρβιδίου βολφραμίου HVOF για εξαιρετικά λειαντικά περιβάλλοντα — όλα διαθέσιμα με εργοστασιακά φινιρίσματα.
Γεωμετρία τοποθέτησης
Διαμορφώσεις τοποθέτησης με διχάλα, άξονα και φλάντζα, όλες σχεδιασμένες με βάση σχέδια που παρέχονται από τον πελάτη με αποδοχή εισόδου αρχείου DXF/STEP για ταχύτερους χρόνους παράδοσης από το σχεδιασμό έως την παραγωγή.
Τεκμηρίωση ποιοτικού ελέγχου
Πλήρης ιχνηλασιμότητα υλικού με πιστοποιητικά μύλου, αρχεία δοκιμών σκληρότητας, διαγράμματα δοκιμών πίεσης και αναφορές διαστάσεων CMM που αποστέλλονται με κάθε κύλινδρο ειδικά κατασκευασμένο ως τυπική τεκμηρίωση.
Ιστορία Επιτυχίας Πελάτη: Διαχειριστής Στόλου, Τομέας Λατομείων South Yorkshire
Αδρανή υλικά Rotherham — Πρόγραμμα αντικατάστασης στόλου κυλίνδρων μπούμας
 Η Rotherham Aggregates λειτουργεί έναν στόλο δώδεκα εκσκαφέων Komatsu PC300 σε τρία ενεργά μέτωπα λατομείου ασβεστόλιθου στο Νότιο Γιορκσάιρ. Μέχρι τα τέλη του 2024, η ομάδα συντήρησης είχε εντοπίσει ένα μοτίβο επιταχυνόμενων βλαβών στεγανοποίησης στους κυλίνδρους του βραχίονα των έξι παλαιότερων μηχανημάτων της — όλες οι μονάδες με πάνω από 4.500 ώρες λειτουργίας. Η επιθεώρηση αποκάλυψε ότι οι αρχικοί κύλινδροι, που προμηθεύτηκαν μέσω του αντιπροσώπου εξοπλισμού τους κατά την αγορά, είχαν μετρήσεις τραχύτητας επιφάνειας οπής που είχαν υποβαθμιστεί σε Ra 0,9–1,1 µm στα παλαιότερα μηχανήματα, πολύ εκτός του αποδεκτού εύρους για αξιόπιστη απόδοση στεγανοποίησης. Η εσωτερική παράκαμψη ήταν μετρήσιμη και στις έξι μονάδες, με αποτέλεσμα την απώλεια ισχύος συγκράτησης του βραχίονα που εκδηλώθηκε ως αργή ερπυσμός του βραχίονα υπό το μέγιστο ονομαστικό φορτίο — ένα ζήτημα ασφάλειας σύμφωνα με τους κανονισμούς PSSR 2000 που ισχύουν για το εργοστάσιο του Ηνωμένου Βασιλείου.
Ο διαχειριστής στόλου επικοινώνησε με την Ever Power μέσω του διανομέα βιομηχανικού εξοπλισμού στο Ρόδερχαμ του Ηνωμένου Βασιλείου και παρείχε τους σειριακούς αριθμούς του μηχανήματος και τις μετρημένες διαστάσεις των κυλίνδρων. Η ομάδα μηχανικών εφαρμογών της Ever Power επιβεβαίωσε τις προδιαγραφές διασταύρωσης εντός 48 ωρών και μια παρτίδα έξι ανταλλακτικών κυλίνδρων βραχίονα — όλοι κατασκευασμένοι σύμφωνα με την προδιαγραφή διαστάσεων PC300 με ράβδους χρωμίου 30 µm και στοίβες στεγανοποίησης Viton για βελτιωμένη αντοχή στην τριβή σε περιβάλλον σκόνης ασβεστόλιθου — απεστάλησαν μέσω παλετοφόρου στο λατομείο εντός δέκα εργάσιμων ημερών από την επιβεβαίωση της παραγγελίας.
Δώδεκα μήνες μετά την εγκατάσταση, η Rotherham Aggregates ανέφερε μηδενικές βλάβες στεγανοποίησης και στους έξι αντικατεστημένους κυλίνδρους, παρά τις συνθήκες λειτουργίας που περιελάμβαναν εκτεταμένες βάρδιες κατά τη διάρκεια της καλοκαιρινής αιχμής των αδρανών και χειμερινές λειτουργίες σε θερμοκρασίες υπό του μηδενός. Ο διευθυντής συντήρησης σημείωσε ότι οι μετρούμενοι χρόνοι κύκλου - μια προσέγγιση για την υδραυλική απόδοση - είχαν επιστρέψει εντός 2% των ονομαστικών τιμών του κατασκευαστή, αντιπροσωπεύοντας μια πλήρη ανάκαμψη από την υποβάθμιση της απόδοσης που είχε γίνει αποδεκτή ως φυσιολογική κατά τα προηγούμενα δύο χρόνια λειτουργίας. Το πρόγραμμα αντικατάστασης στόλου απέφερε ένα υπολογισμένο κέρδος παραγωγικότητας που αντιστάθμισε το κόστος προμήθειας εντός του πρώτου τριμήνου παραγωγής.
Τι λένε οι διαχειριστές μονάδων στο Ηνωμένο Βασίλειο για την Ever Power
«Η ποιότητα του χρωμίου στις ανταλλακτικές ράβδους είναι αισθητά καλύτερη από αυτή που έβγαιναν από τα μηχανήματά μας Komatsu. Μετά από δεκαοκτώ μήνες στις επιφάνειες των λατομείων μας, δεν υπήρξε ούτε μία αστοχία στη στεγανοποίηση των υαλοκαθαριστήρων. Αυτό είναι ένα αποτέλεσμα που δεν είχαμε ποτέ με τον προηγούμενο προμηθευτή.»
— Διευθυντής Εργοστασίου, Rotherham Aggregates, Νότιο Γιορκσάιρ
«Χρειαζόμασταν μη τυποποιημένα μήκη διαδρομής που να ταιριάζουν με το ειδικά κατασκευασμένο πλαίσιο κατεδάφισης. Η ομάδα μηχανικών της Ever Power ολοκλήρωσε ένα επιβεβαιωμένο σχέδιο διαστάσεων εντός δύο ημερών και έφερε τους κυλίνδρους στο χώρο του στο Σέφιλντ εντός τριών εβδομάδων. Η εφαρμογή ήταν ακριβής — δεν απαιτήθηκαν τροποποιήσεις κατά την εγκατάσταση.»
— Μηχανικός Στόλου, Εργολάβος Κατεδαφίσεων Δομικών Έργων, Σέφιλντ
«Η τιμολόγηση ήταν ανταγωνιστική σε σχέση με τρεις άλλες προσφορές που λάβαμε και το πακέτο τεκμηρίωσης — πιστοποιητικά εργοστασίου, αρχεία δοκιμών πίεσης, έκθεση διαστάσεων — ήταν ακριβώς αυτό που χρειαζόταν ο διαχειριστής συμβάσεων μας για να ικανοποιήσει τον έλεγχο του πελάτη από τρίτους. Θα χρησιμοποιούμε την Ever Power για όλες τις αντικαταστάσεις του στόλου μας για εργασίες εδάφους στο μέλλον.»
— Διευθυντής Προμηθειών, Εργολάβος Πολιτικών Υποδομών, Μπέρμιγχαμ
Συχνές ερωτήσεις
Απαντήσεις φιλικές προς τη φωνητική αναζήτηση για χειριστές εργοστασίων και ομάδες προμηθειών στο Ηνωμένο Βασίλειο
Είστε έτοιμοι να μειώσετε τον χρόνο διακοπής λειτουργίας και να βελτιώσετε την απόδοση του στόλου σας;
Επικοινωνήστε με την ομάδα μηχανικών εφαρμογών της Ever Power. Αποστέλλουμε ποιοτικούς κυλίνδρους μπούμας σε όλες τις εγκαταστάσεις του Ηνωμένου Βασιλείου.
Ever Power Hydraulics — Κύλινδροι μπούμας ακριβείας για αγορές βαρέος εξοπλισμού στο Ηνωμένο Βασίλειο και παγκοσμίως | επεξεργασία από gzl
 Greek
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French