
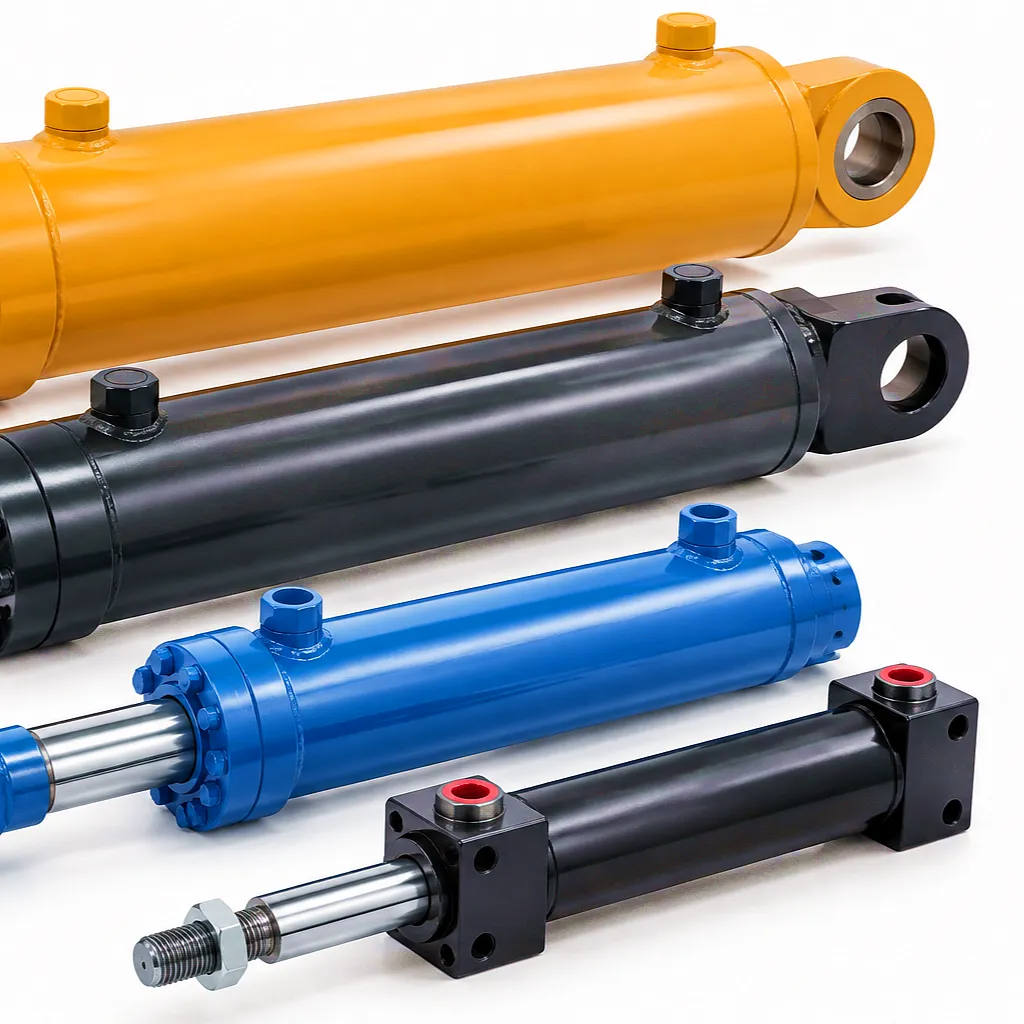
 Walk into any equipment bay in Sheffield, Birmingham, or along the East Midlands’ agricultural belt, and you’ll find boom cylinders doing some of the most mechanically demanding work in the building. They extend excavator arms, tilt loader buckets, operate telescoping aerial platforms, and drive the lift mechanisms of agricultural machinery that feeds the country. Yet despite their ubiquity, the fundamental choice between a single-acting and a double-acting boom cylinder is one that equipment buyers and design engineers frequently underestimate — sometimes with costly consequences for machine cycle times, energy efficiency, and long-term maintenance budgets.
📩 Get a Quote — Contact Our Engineering Team
Response within 24 hours • UK-friendly shipping • Custom specifications welcome
How Each Boom Cylinder Type Actually Works
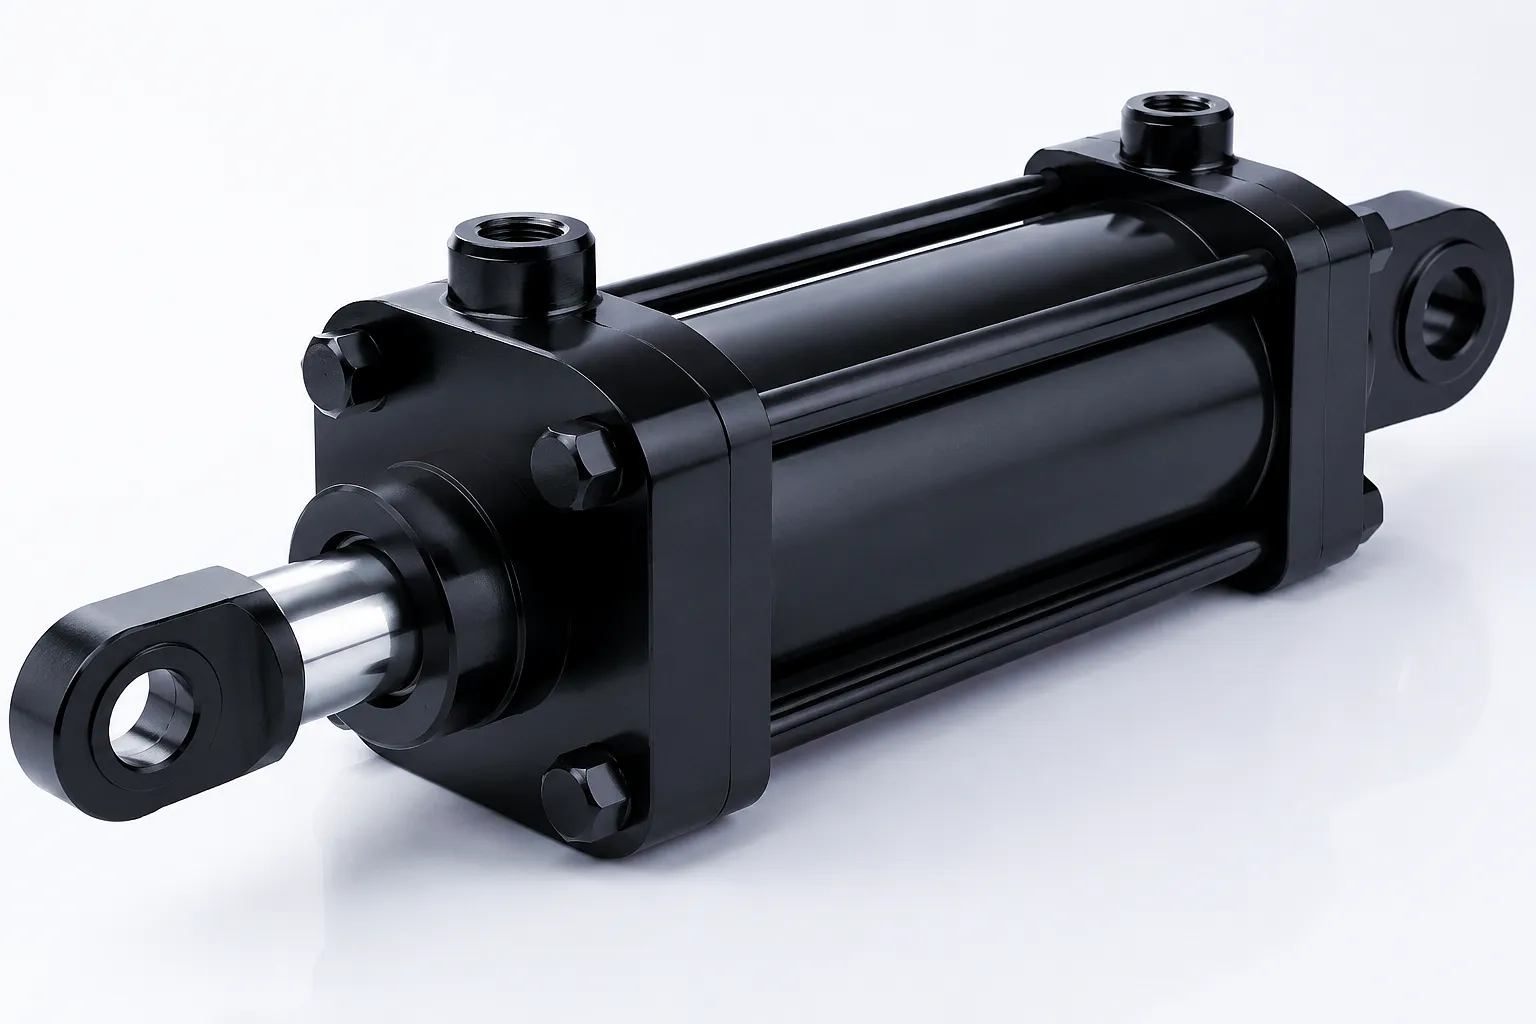
A single-acting boom cylinder has only one hydraulic port. Pressurised fluid enters through that single inlet and pushes against the face of the piston, driving the rod outward in the extension stroke. Return movement — retraction — is achieved through an external mechanical force, which in most boom applications is gravity acting on the weight of the arm or attachment, sometimes assisted by a return spring housed within the cylinder barrel.
The internal layout is elegantly simple: a sealed cylinder barrel, a single-ended piston rod, one set of seals at the rod end, and a single hydraulic connection. Because there is no oil pressure acting on the rod side of the piston, the circuit plumbing is minimal, and the hydraulic control valve only needs to manage one pressure circuit. This simplicity translates directly into lower manufacturing cost, easier maintenance, and a reduced number of potential leak points — all meaningful advantages in environments like UK construction sites where downtime is commercially punishing.
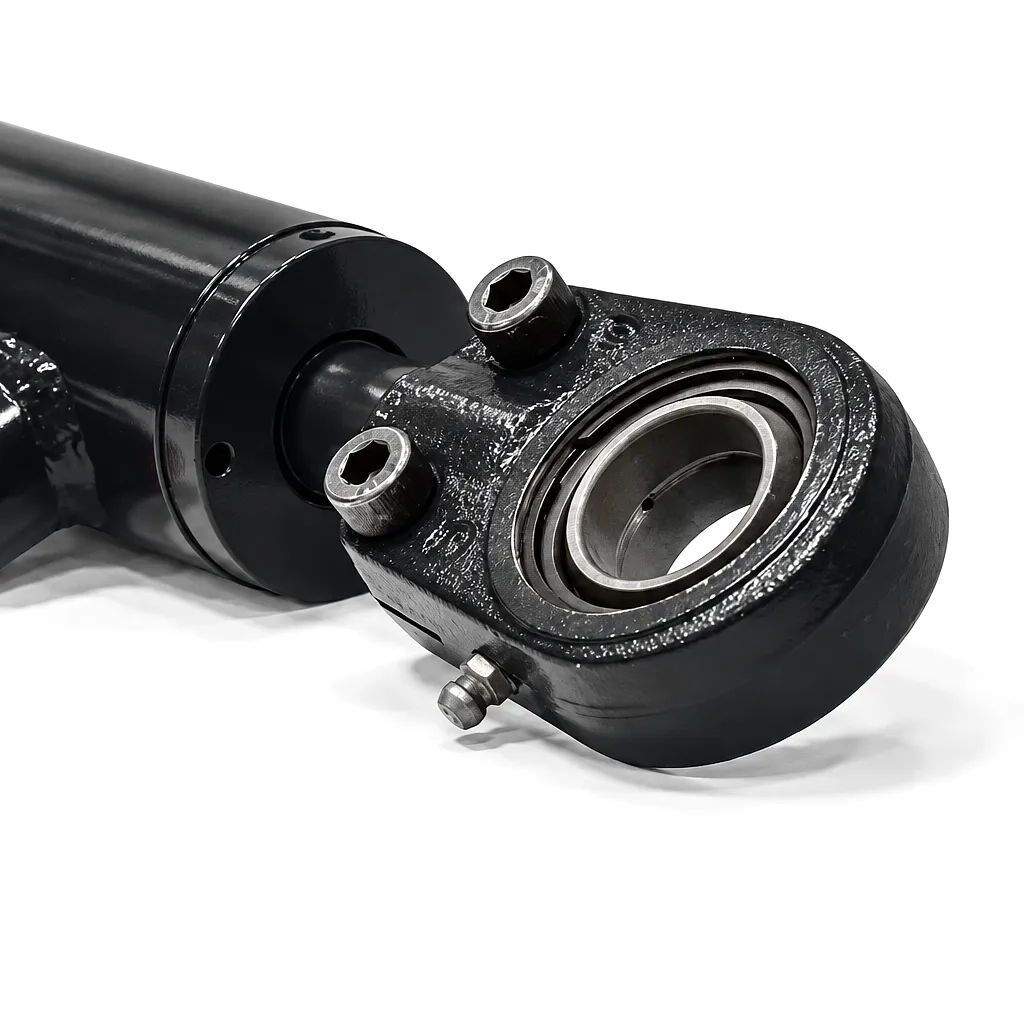
A double-acting boom cylinder operates on an entirely different principle. It has two hydraulic ports — one at the cap end and one at the rod end — and hydraulic pressure can be directed to either side of the piston through a 4/3-way directional control valve. Directing oil to the cap-end port extends the rod; directing oil to the rod-end port drives the piston back against the cap end, positively retracting the cylinder with full hydraulic force.
This bidirectional hydraulic force is what defines the double-acting cylinder’s capabilities. The retraction stroke carries the same type of controllable, metered force as the extension stroke, meaning the operator has precise command over speed, force, and position in both directions of travel. For boom applications where loads must be actively lowered, pressed, or pushed back against external resistance — rather than simply allowed to descend under gravity — this bidirectional authority is not a luxury but a functional requirement. Double-acting cylinders are inherently suited to applications that demand controlled deceleration, fine positioning, and heavy-duty cyclic work.
Core Materials: What Boom Cylinders Are Built From
The material selection for a boom cylinder is not incidental — it is what separates a component rated for 10,000 operating hours from one that fails at 3,000. Ever Power engineers specify materials based on bore size, working pressure, duty cycle severity, and the environmental conditions the cylinder will face in service.
The barrel is machined from cold-drawn seamless precision steel tube (typically EN 10305-1 grade E355 in the UK market), honed internally to a surface roughness of Ra 0.2–0.4 µm. This finish is critical: it minimises seal friction, extends piston seal life, and ensures a consistent oil film across the full stroke length. Honing also eliminates microporosity at the bore surface, which would otherwise provide initiation points for stress-corrosion cracking under cyclic pressure loading.
Piston rods are manufactured from high-tensile steel bar (CK45 or 42CrMo4 grade), ground and polished to h6 tolerance, then electroplated with hard chrome to a minimum depth of 25 µm. The chrome layer delivers surface hardness in excess of 850 HV, protecting against corrosion, abrasion from contaminated seals, and the mechanical scoring that results from particulate ingress on UK construction sites. For severe environmental duties, Ever Power offers nickel-composite or HVOF-sprayed ceramic chrome alternatives with enhanced corrosion resistance exceeding 1,000 hours in neutral salt spray testing.
Seal selection depends on operating temperature range, fluid type, and working pressure. Standard configurations use polyurethane (PU) piston seals for their excellent abrasion resistance and memory under dynamic loading, combined with NBR rod wiper seals that strip particulate contamination before it can reach the dynamic sealing zone. For applications involving fire-resistant hydraulic fluids (a requirement in certain UK mining and steel plant environments), Ever Power specifies PTFE-based or FKM sealing packages validated to BS EN ISO 6195 standards.
End caps and cylinder heads are precision-machined from EN-GJS-400 ductile iron or closed-die steel forgings, depending on pressure rating. Thread forms are machined to DIN 13 tolerances. Port threads comply with BSPP (parallel pipe thread) standards as standard for the UK market, with BSP taper, metric, or SAE options available. Forged construction eliminates the porosity risks inherent in cast components and gives consistent mechanical properties throughout the section thickness — critical for cylinders operating at pressures above 250 bar.
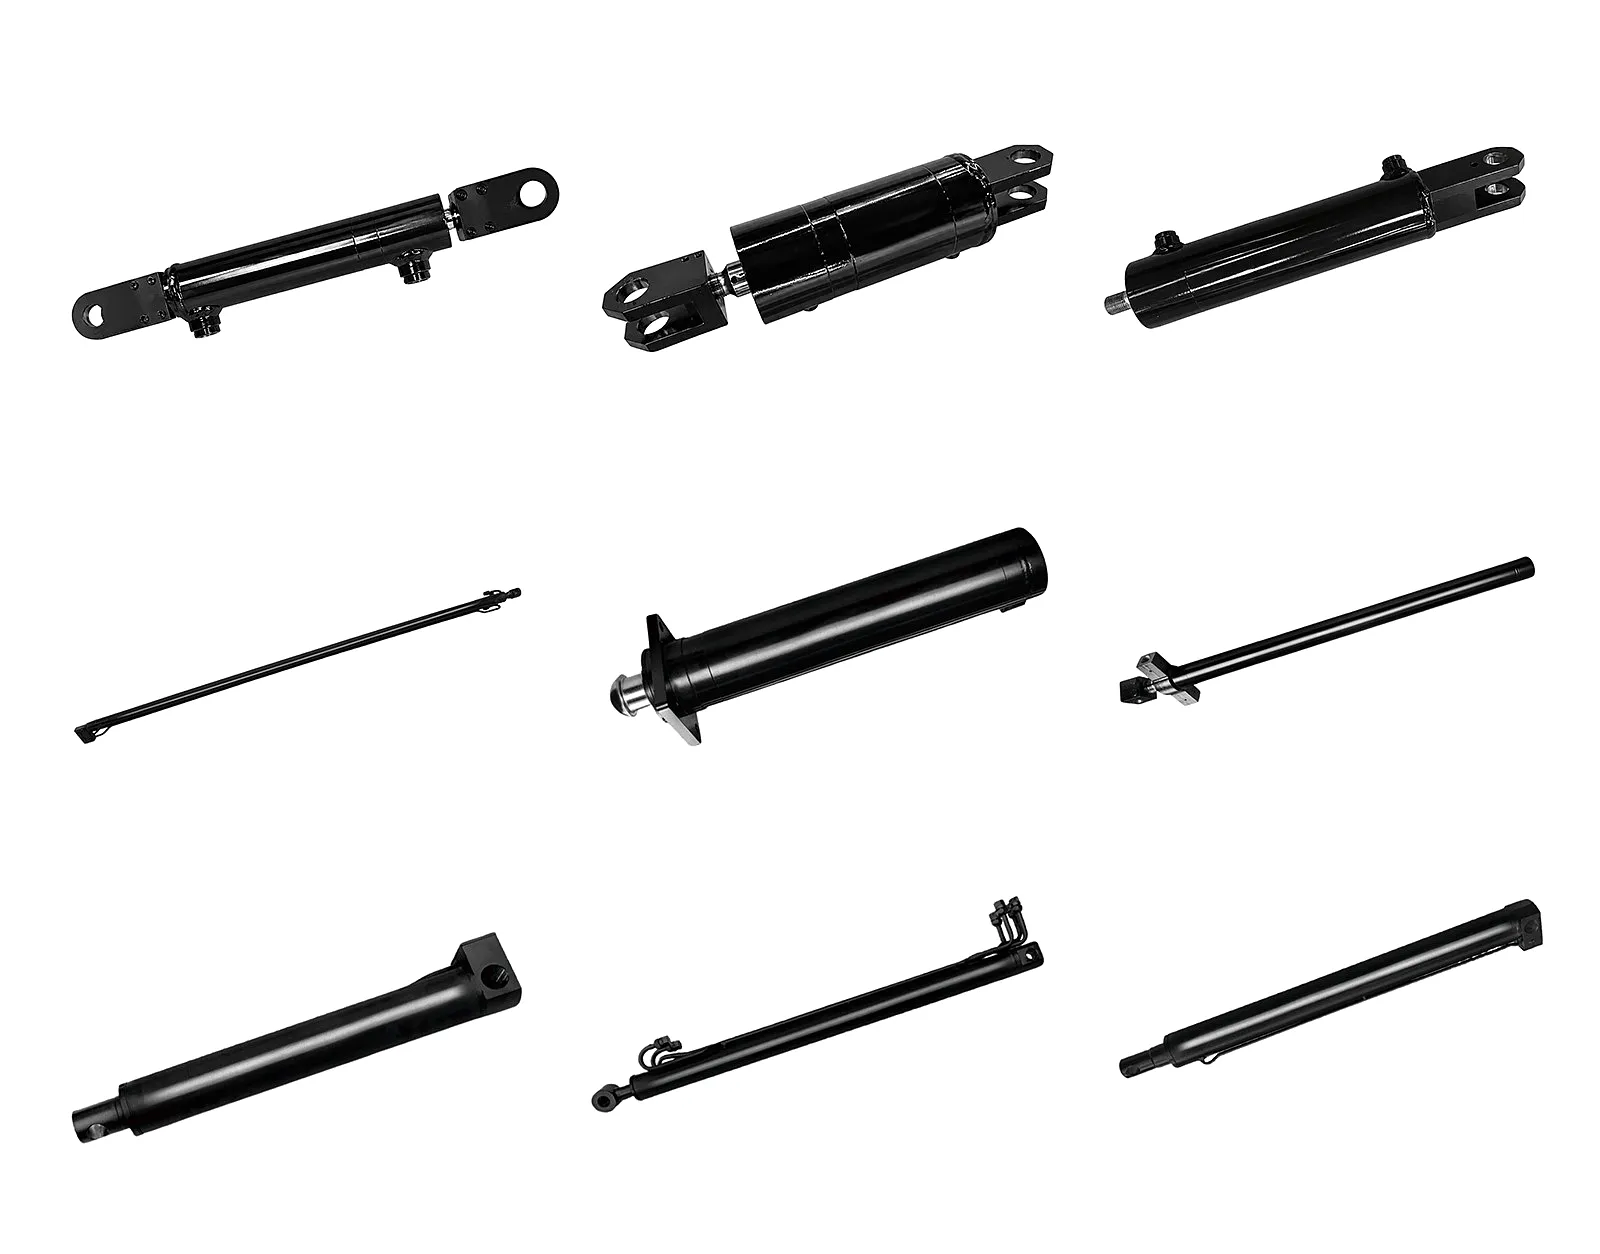
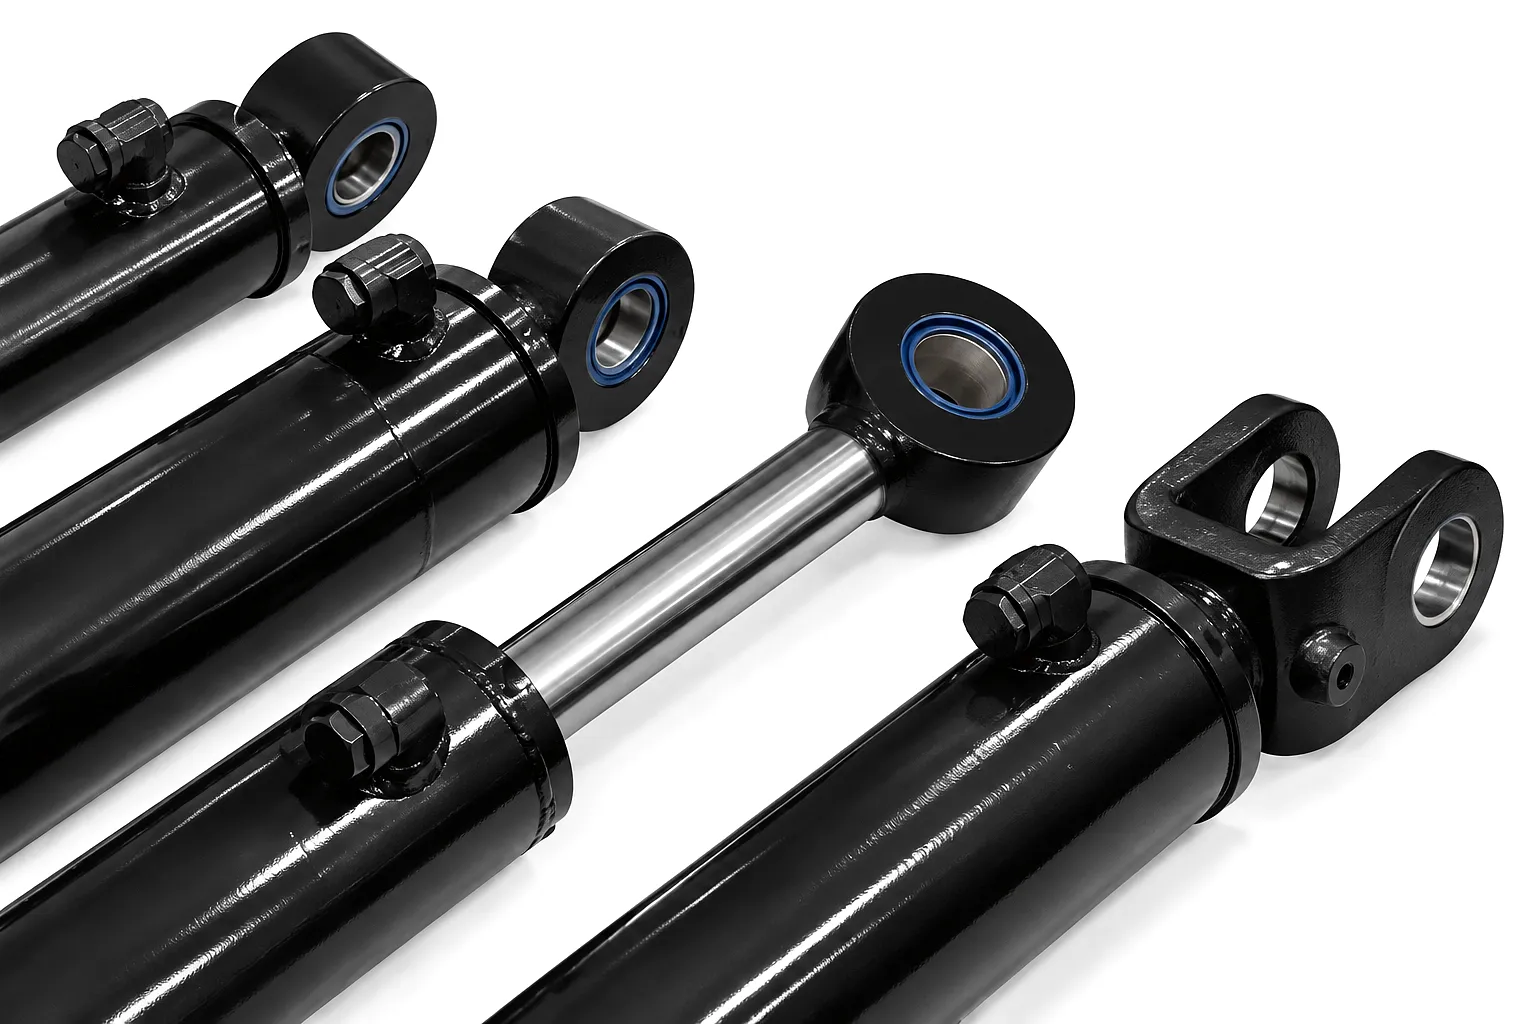
Ever Power Boom Cylinder Product Range — Single-Acting & Double-Acting Configurations
Technical Performance Parameters
The table below consolidates the critical performance parameters across both boom cylinder types as supplied by Ever Power. These figures represent standard production specifications; custom pressure ratings, stroke lengths, and bore diameters outside these ranges are available on request and represent a core part of Ever Power’s engineering offer to OEM customers across the UK and internationally.
Technical Advantages: Where Each Type Wins
One hydraulic line and a simpler directional valve reduce the likelihood of plumbing errors during commissioning and simplify troubleshooting when faults develop on site.
Fewer machined features, one less port, and a simplified gland assembly reduce both manufacturing cost and the bill of materials for the associated hydraulic circuit.
Where the load mass is large relative to the cylinder mass, gravity-driven retraction can be faster than hydraulically driven retraction, improving cycle times in certain tipper body and compactor applications.
With only the cap-end side requiring pressurised oil, reservoir capacity requirements and pump displacement needs are reduced, supporting smaller and more efficient hydraulic power units.
The defining advantage. Hydraulic force is available in both extension and retraction, enabling controlled pushing and pulling against any external load without relying on gravity or spring assistance.
Metered oil flow on the retraction side allows precise intermediate positioning, essential for excavator arm control, crane jib positioning, and CNC press beam applications where sub-millimetre repeatability matters.
Because retraction force comes from hydraulic pressure rather than gravity, double-acting cylinders perform identically whether mounted vertically, horizontally, or inverted — a prerequisite for horizontal drilling rigs, marine applications, and side-tilt mechanisms.
End-of-stroke cushioning can be built into both ends of a double-acting cylinder, decelerating the piston hydraulically before it contacts the end cap and eliminating the shock loading that degrades cylinder and machine structure longevity.
Ever Power’s custom hydraulic power units are engineered to match the flow and pressure demands of both single-acting and double-acting boom cylinder systems — from compact mobile packs to industrial fixed-installation units.
Σενάρια Βιομηχανικών Εφαρμογών σε όλο το Ηνωμένο Βασίλειο
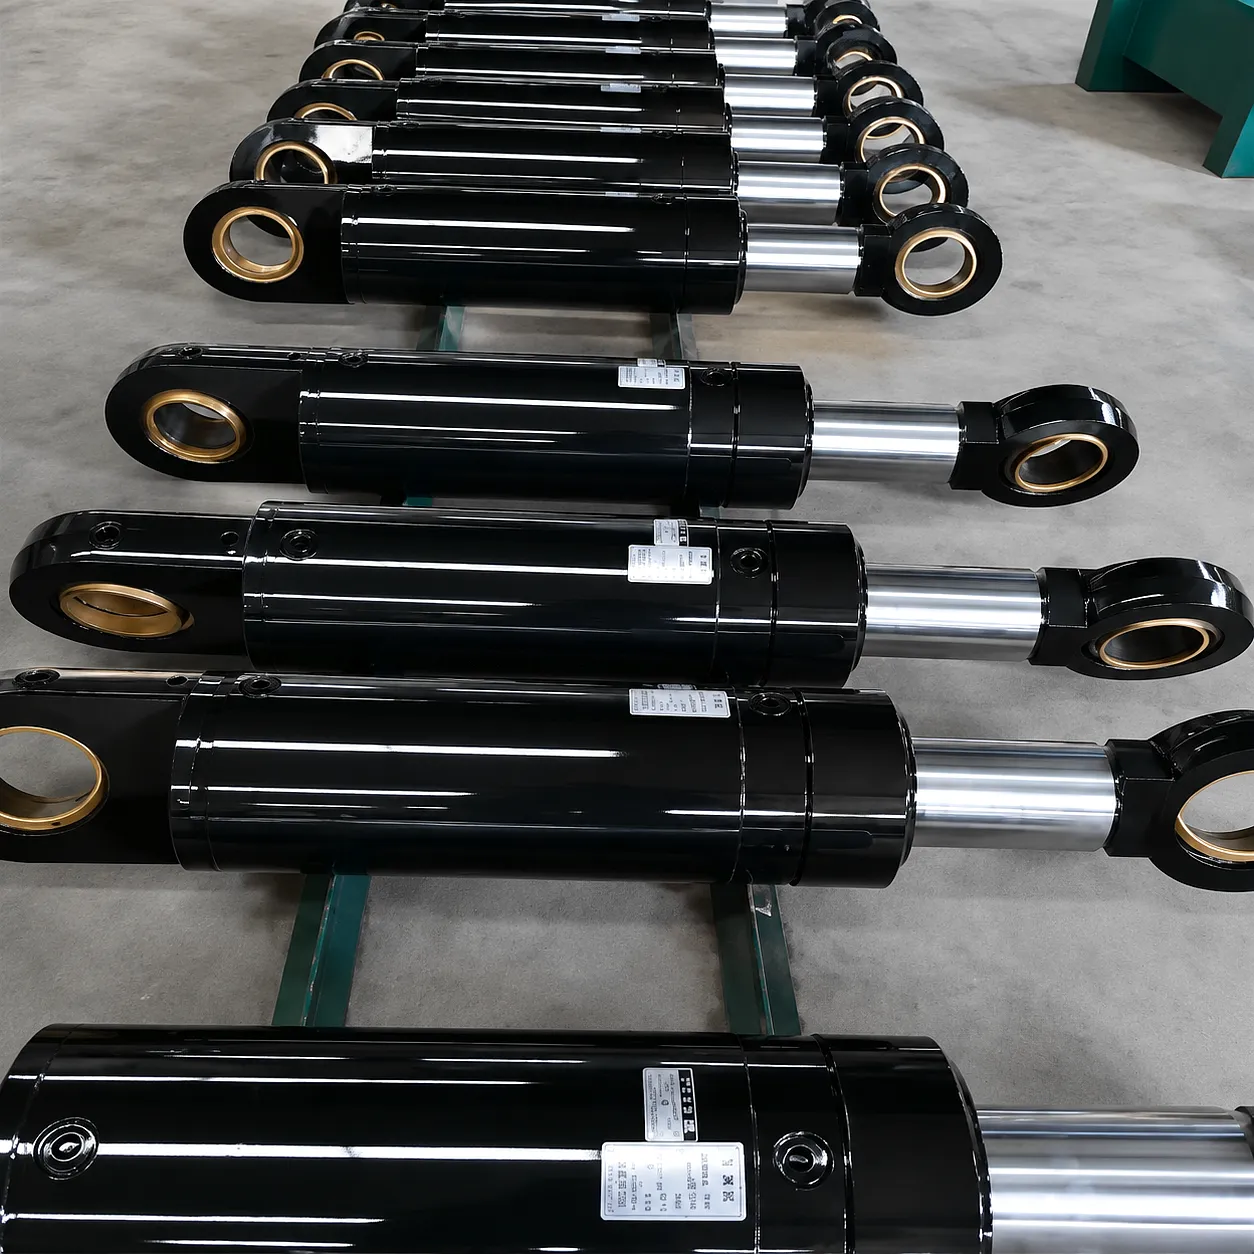
The boom, stick, and bucket cylinders on an excavator are almost exclusively double-acting. This is not a historical convention but an engineering necessity: excavator buckets must apply crowd force into hard ground on the curl stroke, and the boom must be actively raised against full bucket weight with no gravity assistance whatsoever. In the infrastructure projects expanding Birmingham’s metro network and the civil construction activity along the HS2 corridor through the Midlands, excavators are expected to maintain tight cycle times across 12-hour shifts in variable ground conditions. Every degree of lost positioning control or unpredictable retraction speed translates to operator fatigue and safety risk. Double-acting boom cylinders with adjustable hydraulic cushioning are specified as standard because they alone can meet the precision and durability demands of these high-utilisation applications.
Front-end loader booms on agricultural telehandlers represent one of the most nuanced cylinder selection scenarios. The lift stroke — raising a loaded pallet or bale against gravity — demands high force from a cylinder operating under full system pressure. The retraction stroke, however, is frequently assisted by the weight of the bucket and its contents, which means that in many agricultural loader designs a single-acting cylinder is entirely adequate for the lift mechanism, reserving the hydraulic pump capacity for other functions. Yorkshire and East Anglian contractors operating high-throughput grain or bale-handling equipment often prefer this configuration because it reduces hydraulic heat generation during prolonged use, extends pump service life, and simplifies the control valve arrangement on machines where operator intuition matters as much as engineering refinement. Double-acting boom cylinders remain the choice for tipping functions, crowd mechanisms, and anywhere the operator needs active lowering control — particularly when working on slopes common in the Yorkshire Dales or the rolling terrain of the North York Moors.
Sheffield’s remaining steel manufacturing facilities and precision forging plants present some of the most demanding hydraulic cylinder operating environments in the UK. Boom cylinders on furnace-charging machines, ingot-handling cranes, and press-feed systems must operate at temperatures well above ambient, resist hydraulic fluid degradation from thermal cycling, and maintain precise positioning repeatability cycle after cycle. In these environments, double-acting boom cylinders built with high-temperature FKM seals, bore-honed stainless steel tubes, and chrome-plated rods with enhanced corrosion resistance are the only configurations that deliver the service life that plant operators require. The Sheffield steel sector places a particular premium on cylinders with traceable material certification and documented test reports, requirements that Ever Power satisfies through full material traceability documentation from bar stock to finished cylinder, with hydrostatic pressure test certificates issued for every unit before despatch.
The UK’s access equipment rental sector — dominated by large fleet operators supplying construction, events, and facilities management markets nationwide — has specific requirements that differ markedly from static plant applications. Boom cylinders on self-propelled elevated work platforms (EWPs) must operate in both vertical and horizontal orientations, tolerate frequent rapid cycling, maintain positive load-holding capability through counterbalance valve integration, and do so across seasonal temperature extremes from Scottish winter conditions to warm southern summer days. Both single-acting cylinders (used in certain jib-extension mechanisms where spring retraction saves circuit complexity) and double-acting boom cylinders (used in main boom lift and articulation functions) find application in this sector. What EWP operators consistently require is minimal variation in retraction speed between cycles — a characteristic that well-specified double-acting cylinders with matched flow control valves deliver far more reliably than single-acting spring-return designs under variable temperature conditions.
Forestry cranes and forwarder boom arms working in the Highlands and conifer plantations of northern Scotland present a distinct selection challenge. The working environment is extreme — sub-zero temperatures for months at a time, persistent moisture ingress, abrasive wood debris, and terrain-induced machine rocking that places dynamic side loads on boom pivot points. Cylinders in this service need cold-temperature sealing performance (rated to -30°C with appropriate Arctic-grade hydraulic fluid), enhanced rod wiper seals to exclude bark and grit, and sufficiently robust gland housings to resist the impact loads that occur when booms snatch at logs. Double-acting boom cylinders in this sector are typically specified with non-adjustable, fixed-geometry hydraulic cushioning to prevent operator override on end-of-stroke impact — a simple feature that measurably extends cylinder life in forestry applications where operators prioritise speed of work over gentleness of operation.
For applications requiring rotational motion rather than linear stroke — vehicle steering systems, crane slewing mechanisms, and industrial turntable drives — Ever Power’s hydraulic rotary actuator steering cylinders complement boom cylinder installations in complex multi-axis hydraulic systems.
Ever Power: Manufacturing & Custom Engineering Capability
Ever Power operates a vertically integrated manufacturing facility equipped with CNC deep-hole boring and honing machines capable of processing tubes from 25 mm to 400 mm bore diameter. Our in-house hard chrome plating line handles rod diameters from 16 mm to 280 mm, with chrome layer thickness controlled to ±2 µm through continuous bath chemistry monitoring. This level of manufacturing control is not common among hydraulic cylinder suppliers — it is what allows Ever Power to offer performance guarantees that are backed by process data rather than catalogue claims.
Ever Power maintains bonded stock of the most common seal kits, rod diameters, and barrel sizes specifically to support UK customers requiring short lead times. Our logistics partnerships with established freight forwarders provide DDP delivery options to all major UK ports and inland locations, with documentation prepared to post-Brexit customs clearance requirements as standard.
Our technical team provides bore size calculations, rod buckling analysis to Euler beam column criteria, and mounting load analysis at no additional charge during the quotation process. We work from customer drawings, application descriptions, or performance specifications — whichever level of detail your project has reached when you first make contact.
Get a Quote from Ever Power Engineering
Email: [email protected] • Drawings welcome • Custom specifications supported
Customer Success: Sheffield Steel Handling Facility
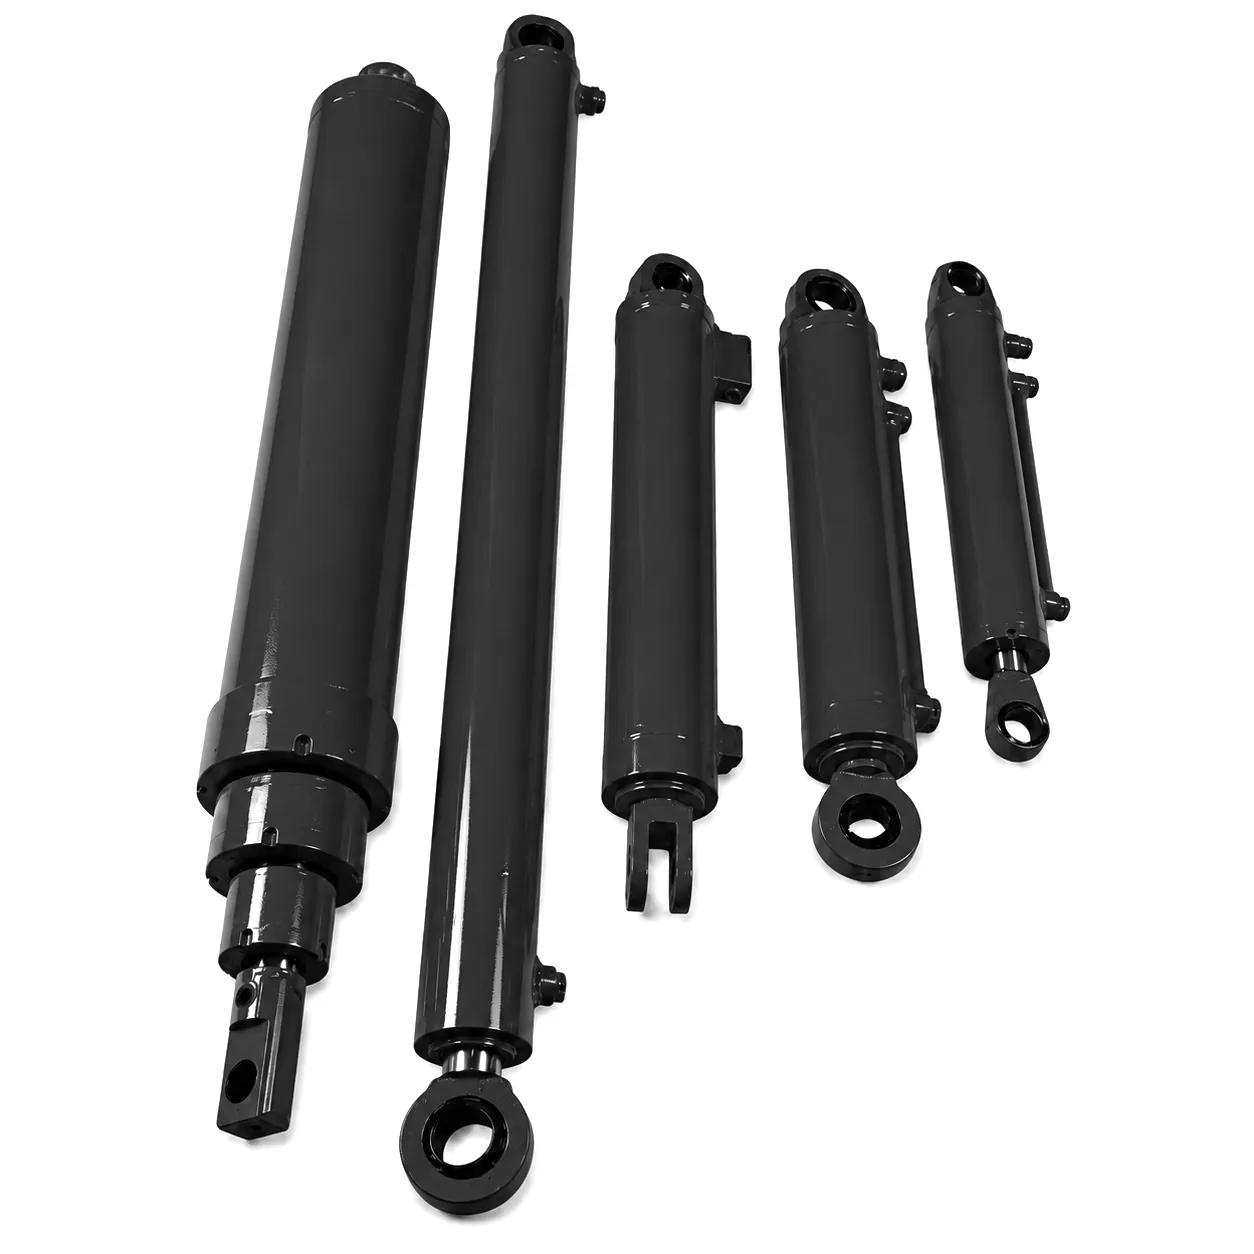 A precision steel processor operating two induction furnace bays in Sheffield’s Lower Don Valley contacted Ever Power following repeated boom cylinder failures on their furnace-charging cranes. The original cylinders — single-acting, spring-return units from a European supplier — had been specified on the assumption that the crane boom’s mass would provide adequate gravity return force. In practice, the operating environment created conditions that the original specification had not accounted for: furnace-bay ambient temperatures regularly reached 55–65°C, degrading the spring elasticity that the single-acting cylinders depended on for retraction, and causing the hydraulic seals to harden and crack within 18 months of installation.
“The FKM seal specification Ever Power proposed was spot on for our furnace environment. We’ve run 18 months without touching them — that’s double the service life we were getting from the previous supplier. The test certificates and material traceability documentation were exactly what our quality department needed.”
“We had an unusual mounting envelope and a non-standard stroke requirement. Ever Power turned around a detailed technical proposal within 48 hours, including an Euler column check on the rod diameter. First sample passed our incoming inspection without any snags. Very professional team.”
“We run a large fleet of access platforms across the UK and are under constant pressure to keep maintenance costs down. Ever Power’s double-acting cylinders with hydraulic cushioning have significantly reduced end-of-stroke impact damage at the boom pivot points. The DDP delivery arrangement suits our centralised stock management perfectly.”
From bore honing to chrome plating to final hydrostatic test, each Ever Power boom cylinder passes through documented inspection stages with records retained for full product lifecycle traceability.
Συχνές ερωτήσεις
Common questions from UK plant engineers, OEM designers, and procurement teams.
For excavators and any boom application where active retraction force is needed — pushing back against soil, rubble, or structural resistance — a double-acting boom cylinder is the only correct choice. Single-acting units are suitable only where gravity alone provides adequate retraction under all working conditions, which is rarely the case for excavator boom arms. If you’re uncertain about your specific application, Ever Power’s engineering team will review your cycle requirements at no charge during the quoting process.
A double-acting boom cylinder typically costs 25–40% more than a comparable single-acting unit, reflecting the additional machined port, the more complex gland assembly, and the higher-grade directional control valve required in the hydraulic circuit. For custom dimensions, Ever Power provides itemised quotations based on your specific bore, stroke, pressure rating, and mounting requirements. Contact [email protected] with your dimensional drawing or specification sheet to receive a detailed price within 24–48 hours.
Material traceability certification — covering mill test reports for steel bar and tube stock, hard chrome plating bath records, and hydrostatic test certificates — is standard on all Ever Power boom cylinders, not an optional extra. For UK customers in sectors with formal quality management requirements (steel processing, offshore, defence supply chains), Ever Power can supply documentation packages that include EN 10204 3.1 material certificates and individual pressure test records for each cylinder serial number.
Lead times for custom double-acting boom cylinders depend on bore size and any special material or surface treatment requirements. Standard configurations with bore diameters up to 200 mm typically ship within 20–30 working days from drawing approval. Larger bore or high-pressure units may require 35–45 working days. Ever Power offers DDP delivery to UK addresses as standard — all customs clearance, import documentation, and import duty are handled at the origin, so UK customers receive a single invoice price with no unexpected port charges on arrival.
In most cases, converting from a single-acting to a double-acting boom cylinder requires more than simply changing the cylinder — it also requires replacing the directional control valve (from a 4/2 to a 4/3 centre-block valve), adding a return line from the rod-end port back to the reservoir, and recalculating the pump flow requirements to account for differential area effects on the retraction stroke. Ever Power can provide full system-level guidance as part of our engineering support service. For UK agricultural OEMs considering a design upgrade, we strongly recommend a circuit review before specifying the replacement cylinder to avoid downstream commissioning issues.
Seal kits for Ever Power double-acting boom cylinders are priced according to bore size and seal material specification. Standard PU/NBR kits for common bore sizes between 60 mm and 160 mm are maintained in stock and can be despatched to UK addresses within 3–5 working days. For fleet operators managing large numbers of identical machines — a common scenario for telehandler rental companies based in the Midlands, the North West, or the Home Counties — Ever Power can supply branded seal kits in bulk quantities with pre-sorted, individually labelled packs to simplify your workshop inventory management.
Ever Power supplies both single-acting and double-acting boom cylinders across the full range of bore sizes, stroke lengths, and pressure ratings required for OEM applications. Our engineering team works directly with design engineers during concept and prototype stages, providing bore sizing recommendations, rod diameter calculations, and application-specific seal material guidance before final drawings are issued. UK OEM customers benefit from our established DDP logistics arrangement, consistent on-time delivery performance, and the availability of English-language technical documentation — all of which simplify the supplier qualification process. Contact us at [email protected] to discuss your project requirements.
Send your drawing, application description, or performance specification to Ever Power’s engineering team. We respond within 24 hours with a technical assessment and competitive quotation.
📩 Get a Quote — [email protected]
επεξεργασία από gzl
 Greek
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French