
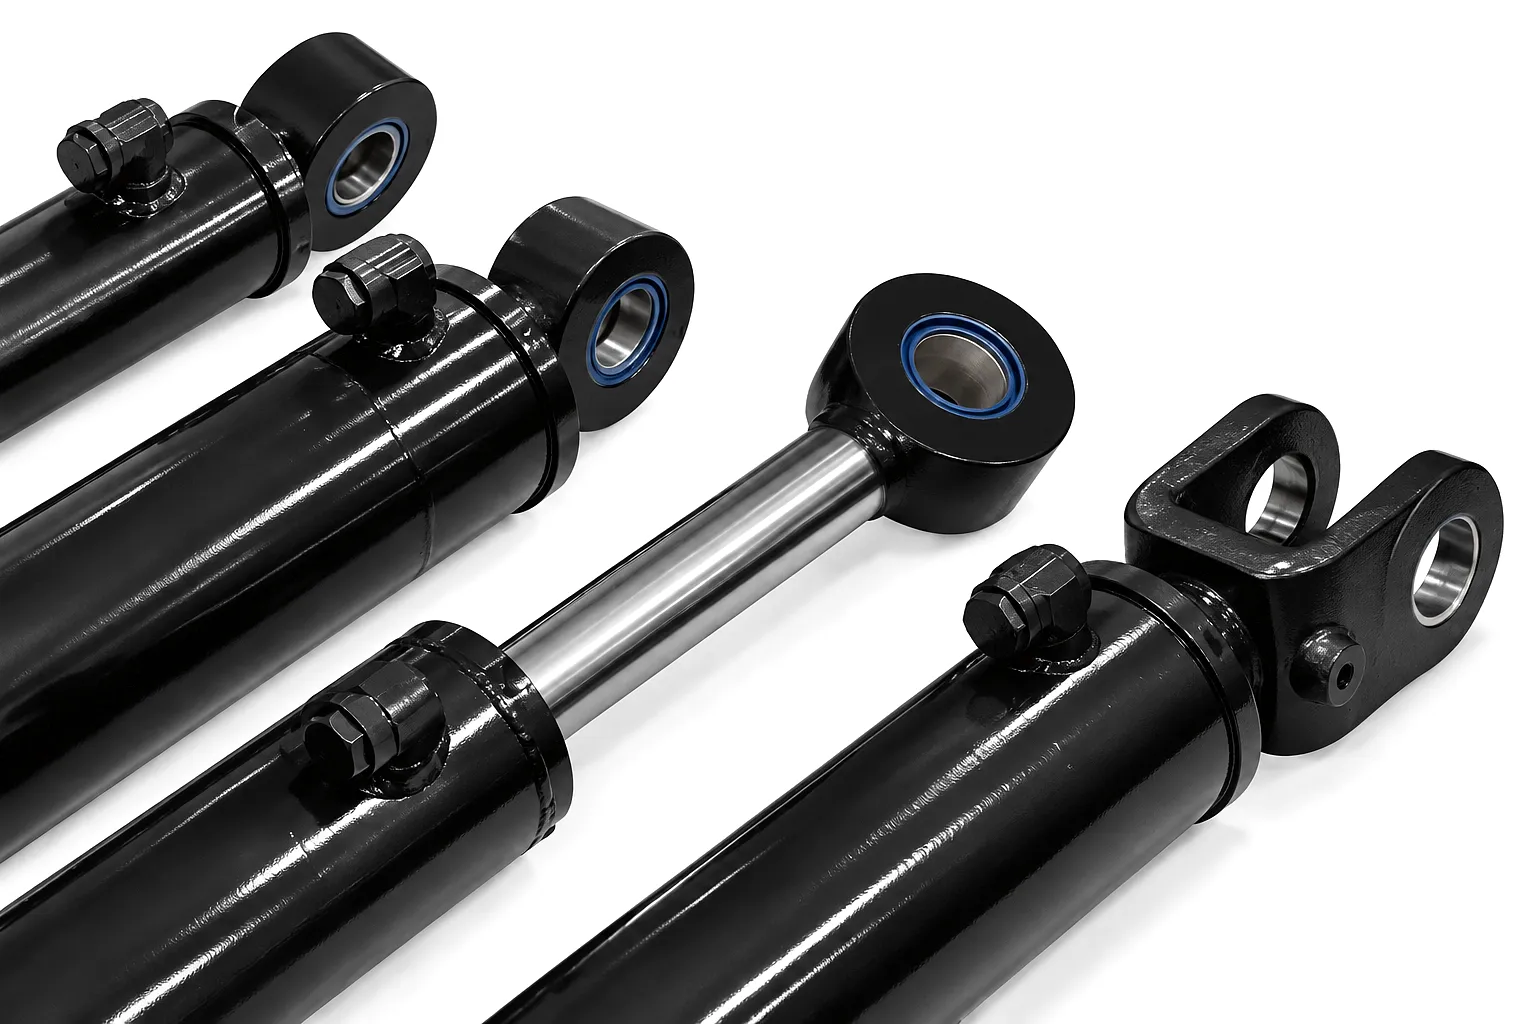
 Air entrainment in hydraulic cylinders is one of the most common — and most underappreciated — causes of poor system performance across British manufacturing sites. From fabrication workshops in Sheffield to agricultural machinery depots in East Anglia, maintenance engineers regularly encounter symptoms that point directly to trapped air: spongy or unresponsive cylinder movement, erratic positioning under load, unusual squealing during operation, and premature seal degradation caused by micro-cavitation events. What makes this problem particularly damaging is that many operators mistake the symptoms for mechanical wear or hydraulic pump failure, leading to costly — and entirely unnecessary — component replacements when the true fix is a straightforward bleeding procedure.
Why Air Enters Hydraulic Cylinders
Before you can bleed a hydraulic cylinder correctly, it pays to understand exactly how air gets into the system in the first place. There is rarely a single cause — it is usually a confluence of maintenance gaps, installation errors, and operating conditions that together allow air to infiltrate what should be a sealed, pressurised fluid circuit. Recognising these entry points helps not only with immediate remediation but with implementing long-term preventive measures that reduce bleed frequency and extend component life.
Pipe connections, port adapters, and hose end fittings that are not torqued to specification allow air to be drawn into the suction side of the circuit under low-pressure conditions. This is especially common after maintenance work where fittings are re-assembled without a torque wrench — a surprisingly frequent occurrence on busy UK plant hire sites.
Piston seals, rod seals, and end cap seals that have deteriorated through age, chemical incompatibility, or thermal cycling can allow air ingestion. In double-acting hydraulic cylinders, a compromised piston seal can permit air to migrate between chambers during retraction strokes, building up over successive cycles until performance becomes noticeably degraded.
When the hydraulic tank runs low — either through fluid leakage or evaporation in high-temperature environments — the pump inlet can draw air along with oil. This is a root cause that is simple to prevent through routine sight-glass checks, yet it accounts for a significant proportion of aeration-related call-outs at UK construction sites, particularly during extended summer operating periods.
New hydraulic cylinders arrive without oil inside — both the cylinder bore and connecting pipework are full of air. If the system is pressurised without first cycling the cylinder slowly through its full stroke at low pressure to allow displacement, large volumes of trapped air remain in the circuit from day one. This is one of the most common commissioning errors seen when installing replacement cylinders on agricultural machinery and industrial presses across the Midlands and North of England.
When return lines discharge above the oil level in the reservoir — rather than below it — turbulence creates foam and whips air into the oil. This aerated oil is then recirculated by the pump before the reservoir has time to allow the bubbles to rise and dissipate. Correct return line positioning is a design detail that is frequently overlooked on site-fabricated hydraulic systems.
Recognising the Symptoms: What Trapped Air Looks and Feels Like
Identifying the specific signature of aeration — rather than attributing it to other hydraulic faults — is a skill that experienced engineers develop over time. The symptoms of air in a hydraulic cylinder system tend to be distinctive once you know what to look for, and they differ meaningfully from the patterns caused by pump wear, valve malfunction, or fluid contamination. Catching these signs early can prevent the cascade of secondary damage that prolonged aeration causes.
The most immediately noticeable sign is that the cylinder feels soft or cushioned when extending or retracting under load — it may not reach its commanded position with the expected force, or may drift back slightly after the control input is released. This compressibility is the direct physical consequence of air bubbles being compressed rather than the oil transmitting force.
Hydraulic cavitation and aeration both generate noise. Air pockets that get rapidly compressed within the cylinder bore produce sharp reports or knocking sounds. In severe cases, micro-cavitation events at seal surfaces produce a high-pitched squealing. These sounds often appear and disappear as the cylinder moves through its stroke, making them easy to distinguish from mechanical bearing noise which tends to be more consistent.
When checking the reservoir, aerated fluid appears lighter, cloudy, or frothy compared to healthy oil which should be clear amber. Milky oil can also indicate water contamination, so distinguishing between the two is important — aerated oil tends to clear relatively quickly when the system is idle, while water-contaminated oil retains its milky appearance.
Compressed air generates significant heat — much more than compressed oil. Systems suffering from persistent aeration often run hotter than they should, accelerating oil degradation, seal softening, and metal fatigue simultaneously. Temperature sensors triggering protection shutdowns on hydraulic presses or injection moulding machinery in Birmingham-area facilities have sometimes been traced back to air entrapment rather than cooler malfunction.
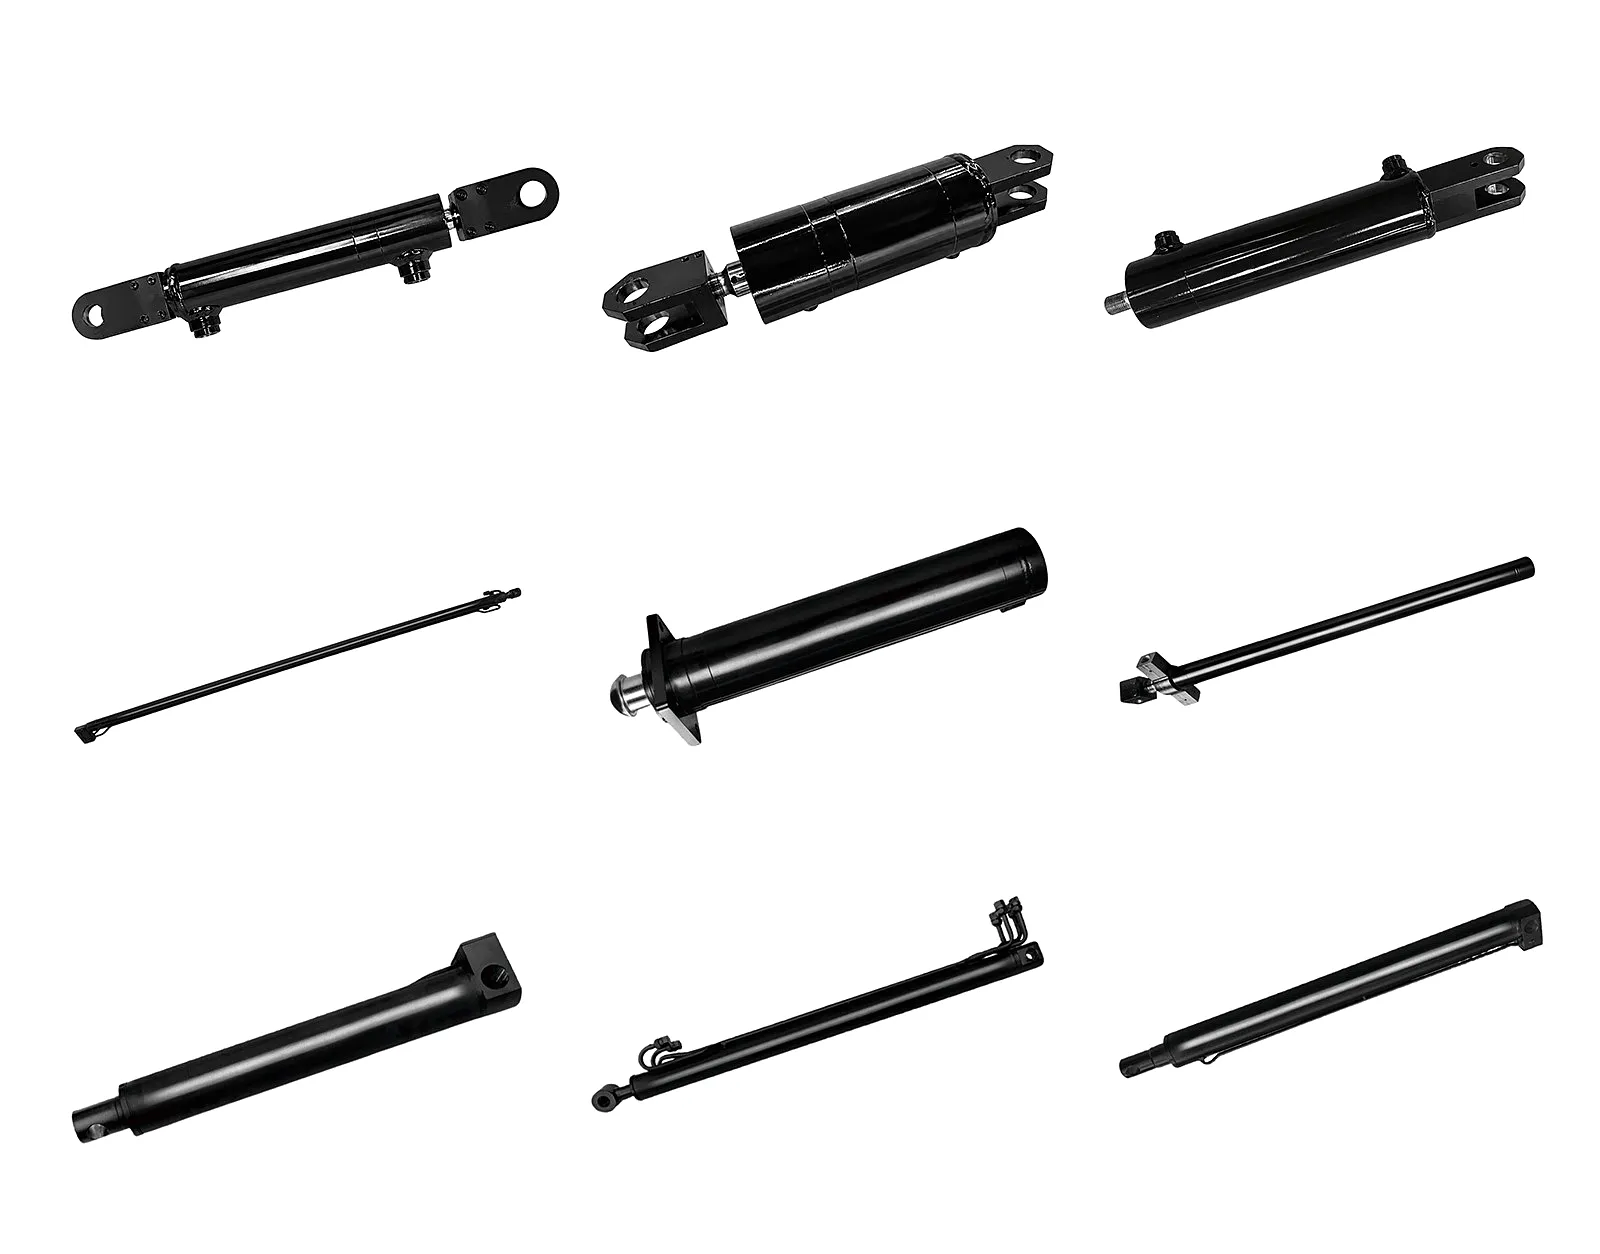
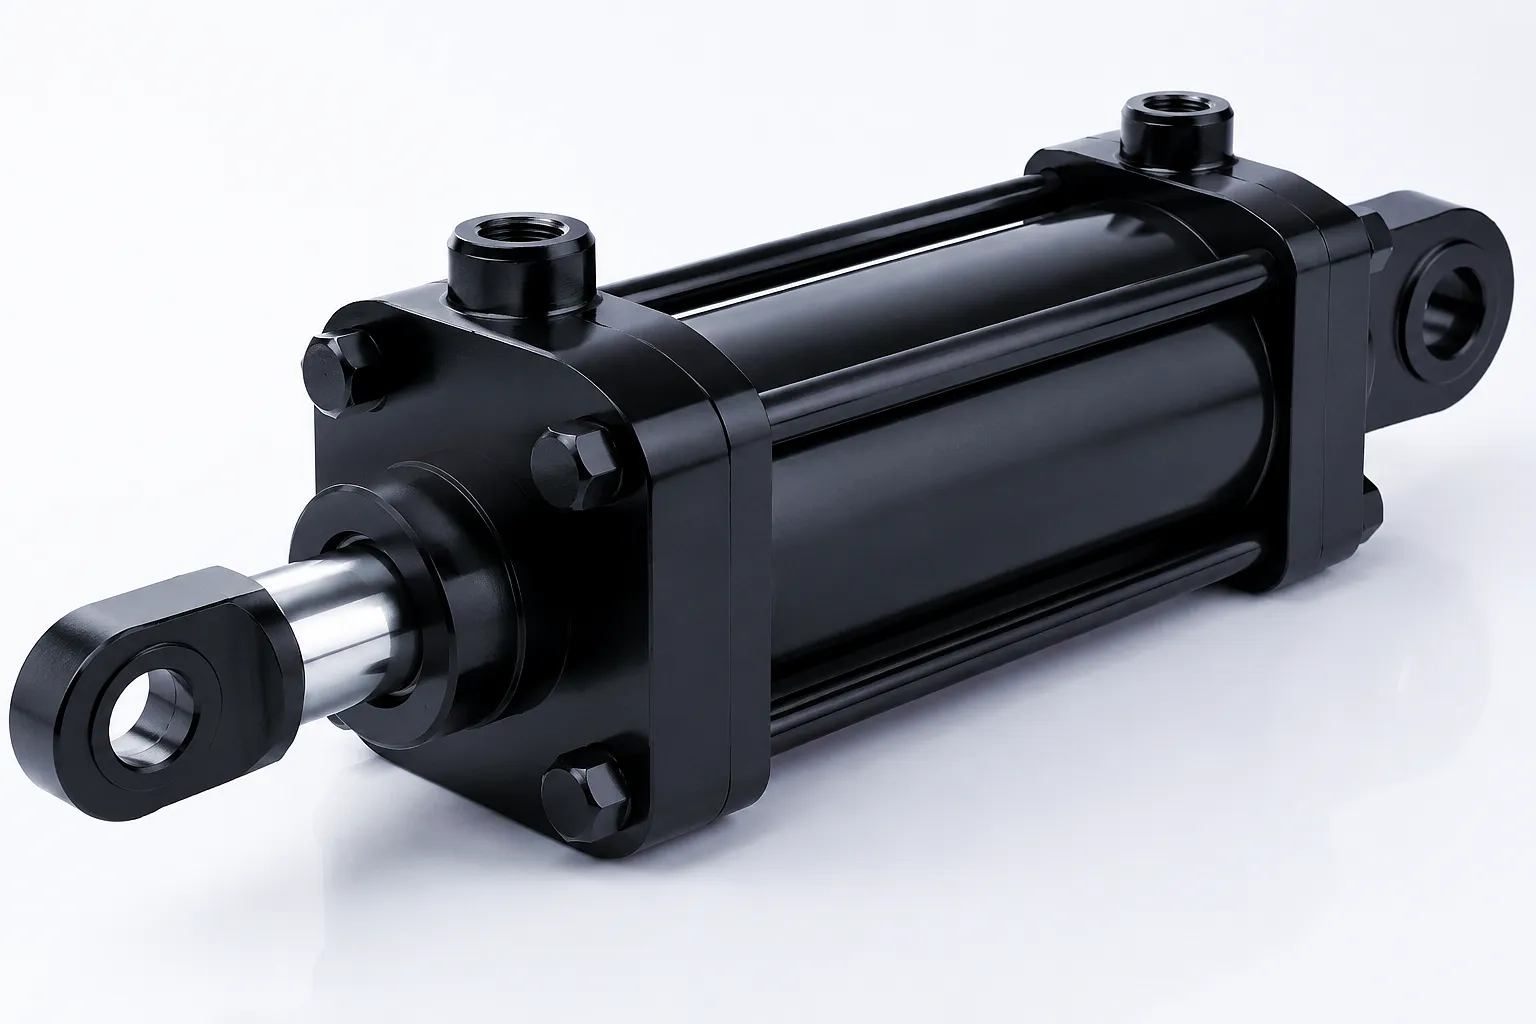
Ever Power hydraulic cylinder product range — custom engineered for UK and global B2B clients
The Correct Procedure for Bleeding Air from a Hydraulic Cylinder
Bleeding a hydraulic cylinder is not a single-step task — it is a methodical process that requires patience, proper preparation, and an understanding of the circuit configuration you are working with. Attempting to rush this procedure, or skipping safety checks, can result in incomplete purging that leaves residual air pockets, or in oil spillage that creates a workplace hazard. The following sequence applies to the majority of single-acting and double-acting hydraulic cylinder installations. Always consult the cylinder manufacturer’s documentation for any model-specific requirements before beginning.
Shut down the hydraulic power unit and allow system pressure to drop to zero. Never attempt to work on or near a pressurised hydraulic circuit — residual pressure in accumulators or locked cylinders can cause catastrophic fluid injection injuries. After shutting the pump, cycle any directional control valves to release trapped pressure, then verify with a calibrated pressure gauge. Follow your site’s lockout/tagout procedure and comply with UK Provision and Use of Work Equipment Regulations (PUWER) requirements before proceeding. Ensure you have a clean drip tray positioned under any connections that will be loosened, and have absorbent material ready for oil spills.
Verify that the reservoir is filled to the correct level — typically between the minimum and maximum marks on the sight glass. If the level is low, top up with the correct grade and specification of hydraulic oil as specified by the original equipment manufacturer. Using the wrong fluid viscosity — a common mistake when a UK depot is out of the specified grade and substitutes an alternative — can itself cause foaming and aeration. If the existing fluid appears milky, dark, or contaminated, a complete fluid change and system flush should precede the bleed procedure.
Many modern industrial hydraulic cylinders, particularly those designed for mobile plant machinery and agricultural equipment, are equipped with dedicated bleed screws or Schrader-type valves positioned at the highest point of each chamber. If your cylinder has these, locate them on both the cap-end and rod-end ports. If no dedicated bleed screw is fitted — which is common on older working cylinders found on legacy plant in Scotland and Northern England — you will bleed through the port connections themselves by briefly slackening the fitting while the cylinder is at a high point in the circuit orientation.
With the bleed point slightly open — just enough to allow air and a small amount of oil to escape — restart the hydraulic pump and extend and retract the cylinder very slowly through its full stroke. For double-acting cylinders, begin with the cap-end (full extension) stroke first, then retract. The slow cycling action moves air pockets along the fluid path toward the bleed point. You will observe a mixture of oil and air — sometimes appearing as frothy or bubbling fluid — escaping at the bleed point. Allow this to continue until only a steady, clear stream of oil flows with no bubbling. Tighten the bleed fitting as soon as continuous oil flow is confirmed.
For double-acting hydraulic cylinders — the most common configuration found on excavators, tipper vehicles, and industrial hydraulic presses — both chambers must be independently bled. After addressing the cap-end chamber, move to the rod-end port. Retract the cylinder fully and open the rod-end bleed point while slowly extending and retracting the piston several times. Again, watch for bubble-free oil flow before tightening. On cylinders with significant bore diameter or long stroke lengths, you may need to repeat each chamber cycle two or three times before all trapped air is purged completely.
Each time oil escapes during bleeding, the reservoir level drops. After completing the bleed sequence, shut down the system, allow it to rest for two to three minutes so any residual micro-bubbles can rise and dissipate, then recheck the reservoir level and top up as required. After refilling, cycle the cylinder again under normal operating load and observe response: movement should be smooth and direct with no sponginess or hesitation. Confirm that all bleed fittings and port connections are properly torqued. Record the procedure in the equipment maintenance log as required by UK workplace safety documentation standards.
Working with combine harvester or agricultural machinery? Our range of purpose-built cylinders for field equipment is engineered for UK farming conditions: Hydraulic Cylinders for Combine Harvester Machine — designed for reliable operation through demanding UK harvest seasons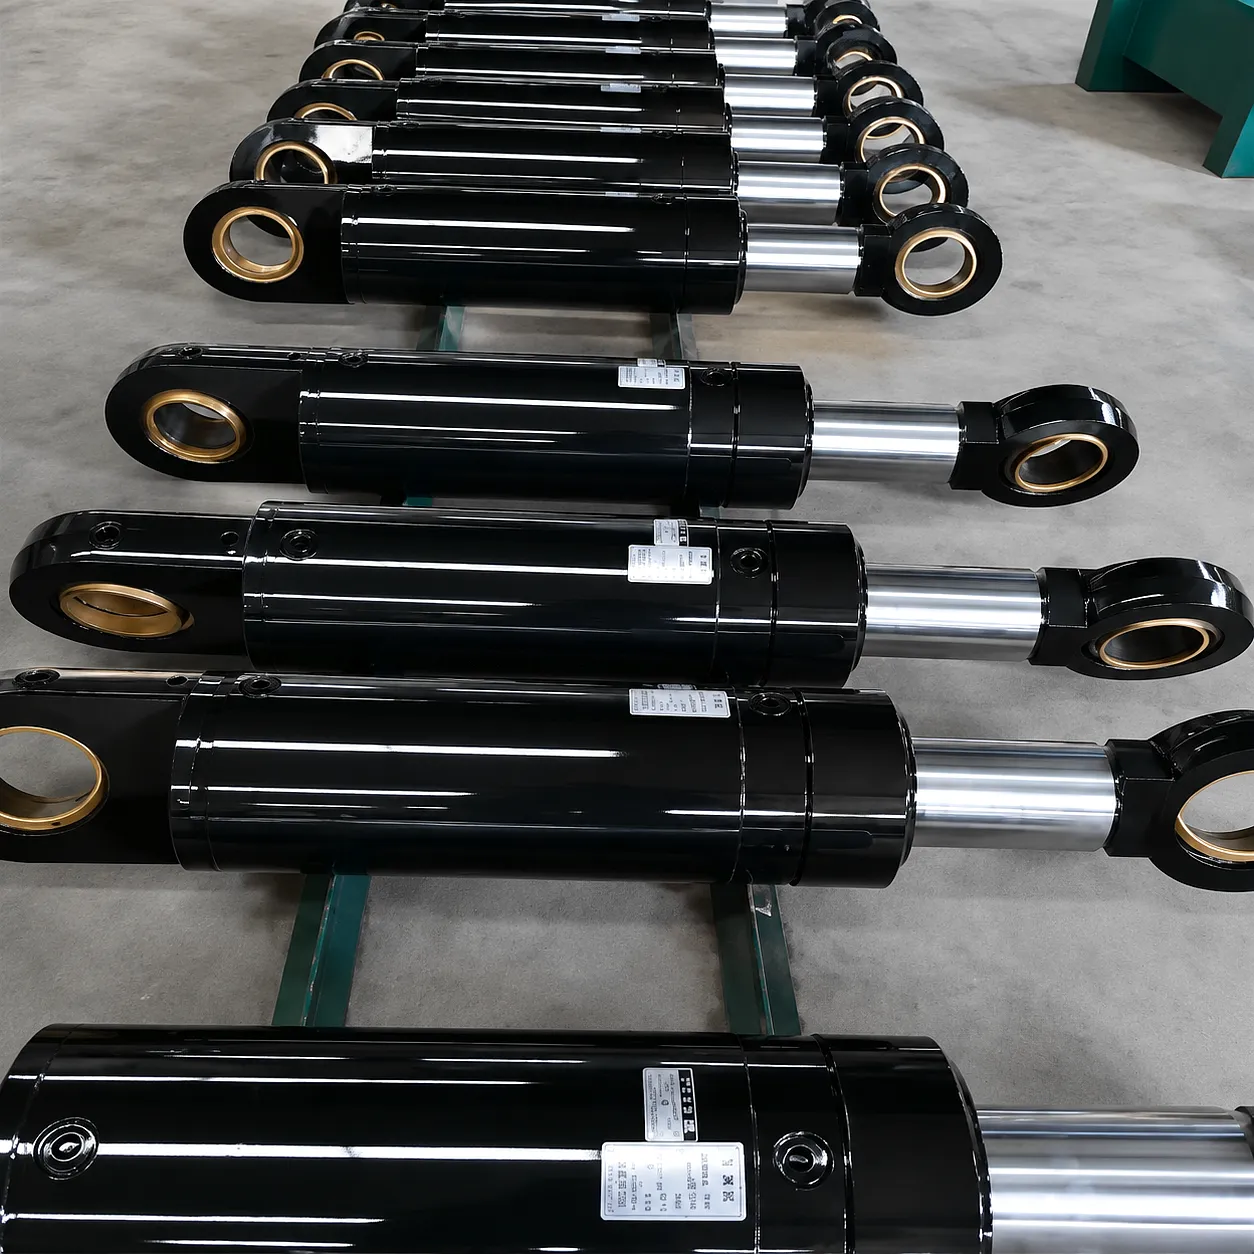
Technical Performance Parameters: Ever Power Hydraulic Cylinders
The table below provides reference performance data for standard Ever Power hydraulic cylinder configurations. All values are for guidance and can be modified to meet specific application requirements through our engineering consultation and custom manufacturing service. Values marked with an asterisk (*) indicate parameters that are particularly relevant to air-bleed and commissioning procedures.
Application Scenarios: Where Proper Bleeding Makes the Critical Difference
The consequences of inadequate air bleeding vary significantly depending on the application. In some industries, trapped air is merely an inconvenience; in others, it is a safety-critical failure mode. The following scenarios represent the industrial contexts where Ever Power hydraulic cylinders are most frequently deployed across the UK, and where correct bleeding procedures have the greatest operational impact.
Excavator boom cylinders, dozer blade rams, and tipper body cylinders operate under high dynamic loads with frequent direction reversals. Air-contaminated circuits on construction plant cause drift under load — a phenomenon where a raised bucket or tipper body slowly descends when the control is in neutral — which poses a direct risk to ground workers operating underneath. Correct bleeding and regular inspection schedules are mandatory on UK construction sites under the Construction (Design and Management) Regulations 2015.
Combine harvester header height cylinders, bale accumulator rams, and cultivator folding mechanisms are all vulnerable to aeration, particularly at the start of the harvesting season when equipment returns from winter storage. Oil that has been sitting for months can absorb dissolved air, which then releases when the system is first pressurised. Dedicated seasonal commissioning procedures — including cylinder bleeding — are increasingly required by UK agricultural contractors’ liability insurers.
Hydraulic presses for sheet metal forming, forging, and composite lay-up rely on precise, repeatable cylinder force and position. Air entrainment in a press circuit creates what machinists call “ghost tonnage” — the press indicator shows the set force, but the actual forming pressure delivered to the tooling is lower due to compressible air absorbing force. This produces inconsistent part dimensions, increased scrap rates, and potential tooling damage. Sheffield’s steel forming industry and Birmingham’s precision engineering sector both have strong reasons to prioritise hydraulic cylinder integrity.
Marine hydraulic systems — controlling anchor winches, hatch covers, crane luffing, and stabiliser fins — operate in environments where both low temperatures and high vibration levels accelerate air ingestion. Aberdeen’s North Sea support vessel fleet and Portsmouth’s naval facilities both operate hydraulic cylinder systems that require exacting commissioning and bleed procedures. In subsea applications, the hydrostatic head also creates pressure differentials that can mask early aeration symptoms, making proactive scheduled bleeding particularly important.
Scissor lifts, dock levellers, and mezzanine lifting tables are subject to UK Lifting Operations and Lifting Equipment Regulations (LOLER), which mandate regular thorough examination of all lifting mechanisms including hydraulic cylinders. Air in a lifting platform cylinder does not merely cause slow operation — it can result in uncontrolled descent under load if a sufficient volume of compressible gas allows the piston to travel back under gravity. Post-inspection bleed procedures are an essential part of LOLER compliance for UK warehouse operators.
For lifting platform applications requiring certified hydraulic cylinders with built-in bleed provisions, explore our purpose-designed range: Custom Double Acting Telescopic Hydraulic Cylinders for Lifting Platform — engineered to meet UK LOLER standards and available with optional bleed valves as standard.
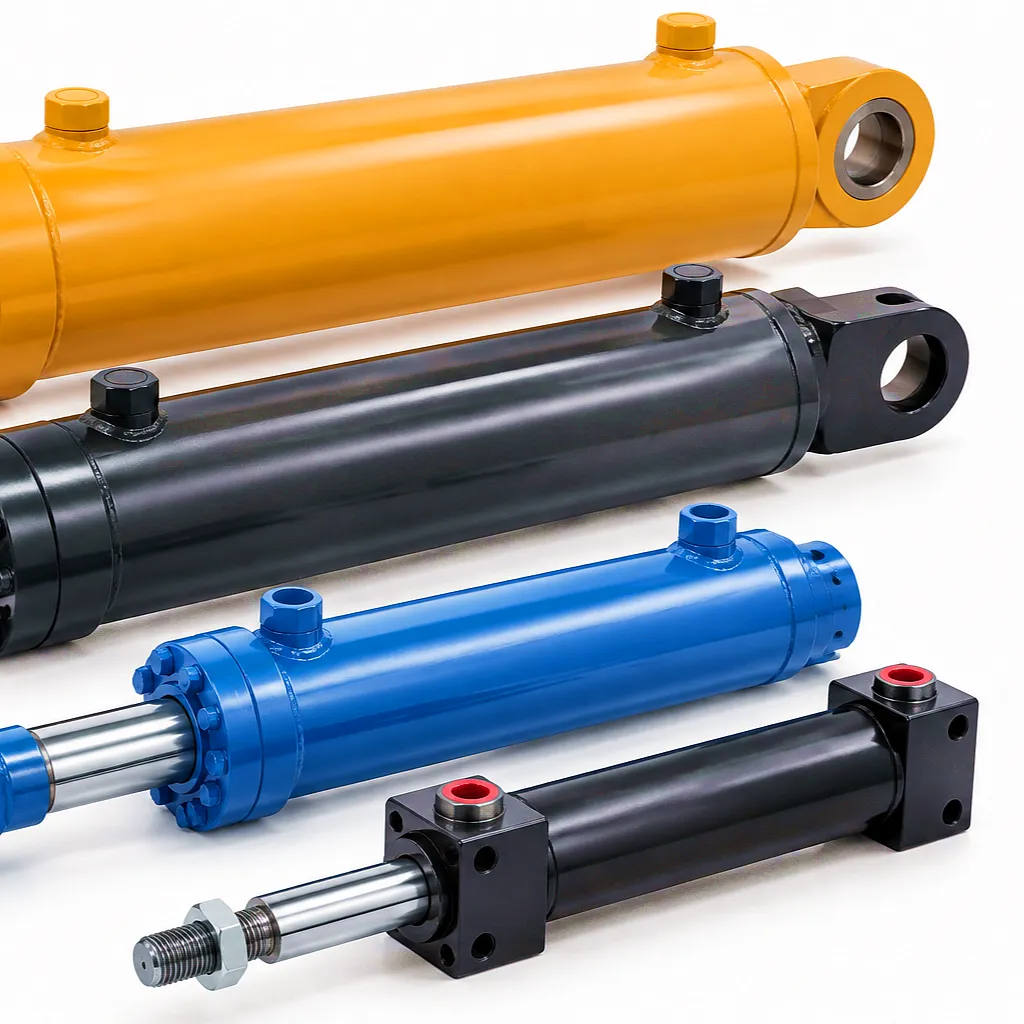
Succès client : Résolution d'un problème d'aération persistant dans une forge de Sheffield
⚙️ Forgeage lourd / Transformation de l'acier
Une entreprise de forgeage à chaud de taille moyenne, située à Sheffield et exploitant deux lignes de presses hydrauliques de 800 tonnes, a constaté une dégradation progressive de ses performances sur trois trimestres de production consécutifs. Les vérins des presses produisaient une force de formage irrégulière ; l’équipe de contrôle qualité a enregistré des variations dimensionnelles sur les pièces forgées dépassant les tolérances spécifiées par le client du secteur automobile. Les premières investigations ont mis en évidence une usure des pompes hydrauliques, ce qui a conduit à deux remplacements coûteux de ces pompes, sans toutefois résoudre le problème.
Après avoir fait appel à l'équipe d'assistance technique d'Ever Power, un audit systématique du circuit a révélé une aération persistante dans les vérins principaux de la presse. Cette aération était due à une combinaison de facteurs : des conduites de retour mal positionnées, dont le débit dépassait la surface de l'huile, et un jeu de joints de piston présentant un léger défaut de contournement, permettant une migration d'air entre les chambres. La conception d'origine des vérins ne prévoyait pas de soupapes de purge, obligeant l'opérateur à desserrer partiellement les raccords d'orifice à chaque purge – une procédure fastidieuse et salissante, souvent négligée en période de forte production.
Ever Power a fourni des vérins de remplacement équipés de purgeurs intégrés aux orifices côté piston et côté tige, positionnés stratégiquement. Le circuit de retour a été modifié pour un rejet souterrain. Après l'installation et un cycle de purge initial complet, réalisé conformément à la documentation fournie, les lignes de presse ont retrouvé leurs performances optimales en deux équipes de production. Les contrôles de maintenance trimestriels suivants, effectués rapidement et proprement grâce aux nouvelles purgeurs, ont permis de maintenir des performances constantes, sans aucune réapparition du problème d'aération. L'usine de Sheffield utilise désormais systématiquement les vérins Ever Power avec purgeurs intégrés pour le remplacement de toutes ses presses hydrauliques.
Ce que disent nos clients britanniques
« Au cours des 18 derniers mois, nous avons remplacé cinq vérins de presse par des unités Ever Power. Les purgeurs intégrés ont transformé notre procédure de maintenance : ce qui prenait auparavant trois heures et deux techniciens ne prend plus que 20 minutes et peut être effectué par un seul mécanicien entre deux équipes. Fini les déversements d’huile et les incertitudes quant à la purge. »
« Nous avons opté pour les vérins Ever Power pour le système de réglage de la hauteur de notre nouvelle moissonneuse-batteuse suite à des problèmes d'aération persistants avec les unités de notre précédent fournisseur. La différence en termes de facilité de mise en service a été remarquable : les vérins se sont purgés complètement en deux ou trois cycles lents et ont fonctionné parfaitement pendant deux saisons de récolte complètes. La documentation fournie couvrait exactement la procédure dont notre équipe avait besoin. »
« L’assistance technique fournie par Ever Power avant l’achat était vraiment impressionnante. Ils ont examiné le schéma du circuit de notre plateforme élévatrice et ont identifié un problème de positionnement de la ligne de retour qui aurait entraîné des problèmes d’aération persistants. Une fois ce problème corrigé et leurs vérins installés, notre équipe d’inspection LOLER a validé le système sans aucune intervention supplémentaire. Un tel niveau d’expertise technique avant-vente est rare de la part d’un fournisseur à ce niveau de prix. »
Les ingénieurs d'Ever Power sont prêts à discuter de votre application, à examiner vos spécifications et à vous fournir un devis compétitif, incluant une documentation complète et une assistance à la mise en service.
 French
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 Greek