
Torque Specs and Fastener Best PracticesWhen Installing Hydraulic Cylinders
A precision-focused field guide for engineers, maintenance teams, and procurement specialists across the UK’s manufacturing and heavy industry sectors — covering torque values, thread standards, sealing, and installation protocol from the ground up.
ISO 6020 / BS Standards
B2B Industrial Supply
When a hydraulic cylinder fails in the field, the root cause is rarely the cylinder itself — more often, it traces back to how it was installed. Improper torque values on mounting bolts, mismatched thread standards, or under-specified fasteners create the conditions for hydraulic fluid leaks, structural misalignment, seal damage, and ultimately catastrophic failure under load. Across the UK’s heavy engineering regions — from the precision machining clusters of Birmingham to the steel fabrication yards of Sheffield — engineers consistently report that tightening fasteners to manufacturer-specified torque is the single most preventable cause of premature hydraulic cylinder failure. This guide covers the full installation sequence: understanding torque tables, selecting the right fastener grade and coating, applying thread sealing correctly, and verifying your work with proper calibration procedures that satisfy both site safety requirements and supply chain audit standards.
Why Torque Specifications Are Non-Negotiable in Hydraulic Cylinder Installation
Every fastener in a hydraulic cylinder mounting assembly serves a specific mechanical role — clamping force, shear resistance, or a combination of both. Torque is the rotational force applied to a fastener during tightening, and its primary purpose is to generate a predictable clamping load between the joined components. This clamping load is what holds the cylinder in alignment, prevents the end cap from separating under pressure spikes, and maintains the compression on face seals at the port connections. When UK plant engineers in sectors like automotive body pressing in Coventry or underground mining equipment maintenance in County Durham work with hydraulic systems, they often encounter both metric ISO threads and, in older equipment, British Standard Whitworth (BSW) or British Standard Fine (BSF) threads. Knowing which standard applies — and using the correct torque table for each — is not an optional detail but a safety-critical requirement. Misidentifying thread standards is one of the leading causes of cross-threading during installation, which ruins fastener holes and invalidates the cylinder warranty in most supply agreements.
Torque = Force × Moment Arm. The relationship between applied torque and the resulting bolt tension is governed by a clamp-load equation: T = K × D × F, where T is the applied torque (Nm), D is the nominal bolt diameter (m), F is the desired clamping force (N), and K is the nut factor — a dimensionless constant that accounts for thread geometry, surface finish, lubrication, and coating. For unlubricated zinc-plated steel fasteners (common in agricultural and construction hydraulics), K typically runs between 0.18 and 0.22. For cadmium-plated or waxed fasteners used in defence and aerospace hydraulic sub-assemblies, K drops to 0.12–0.15. Never apply a torque specification from one fastener condition to a fastener of a different surface treatment without recalculating — the resulting clamping force can be off by 30% or more.
A phenomenon called elastic interaction means that tightening one bolt in a multi-bolt pattern will partially relax its neighbours. This is particularly significant on hydraulic cylinder end cap flanges with four, six, or eight bolt patterns. If you tighten all bolts to final torque in a single pass starting at position one and working clockwise, the last bolts you torque will partially unload the earlier ones. Standard best practice calls for tightening in a star or cross pattern across at least three passes: 30% of final torque on the first pass, 70% on the second, then a full final torque pass, followed by a verification pass in the same sequence. This multi-pass star pattern approach is mandated in ISO 4413, the UK-applicable standard for hydraulic fluid power safety requirements, and should be documented in every installation record as part of CE marking compliance.
Hydraulic Cylinder Fastener Torque Specification Reference Table
The following table consolidates recommended torque values for common metric fastener grades used across hydraulic cylinder mounting, port fitting, and end cap applications. Values assume dry (unlubricated) threads unless otherwise stated. Always cross-reference with your cylinder manufacturer’s datasheet — the values below are general engineering references, not a substitute for OEM documentation.
| Bolt Size (Metric) | Grade 8.8 Dry (Nm) | Grade 10.9 Dry (Nm) | Grade 12.9 Dry (Nm) | With Molykote (Nm) | Typical Application |
|---|---|---|---|---|---|
| M8 | 24 | 34 | 40 | 18 | Sensor boss, bleed port |
| M10 | 48 | 68 | 80 | 36 | Trunnion bracket, side lug |
| M12 | 84 | 118 | 140 | 63 | End cap flange (small bore) |
| M16 | 200 | 285 | 335 | 150 | End cap flange (medium bore) |
| M20 | 390 | 555 | 650 | 290 | Heavy-duty clevis pin bolt |
| M24 | 680 | 960 | 1130 | 510 | Boom cylinder root pin (excavator) |
| M30 | 1350 | 1900 | 2230 | 1010 | Hydraulic press platens, heavy lift |
| 3/8″ BSP Port | 27–34 | — | — | — | BSP hydraulic port fitting |
| 1/2″ BSP Port | 54–68 | — | — | — | BSP hydraulic port fitting |
* BSP port torque values assume use of PTFE tape or hydraulic sealant. Verify against ISO 228-1 for thread class tolerances. Nm = Newton-metres.
Fastener Grade Selection: Matching the Bolt to the Load
Selecting the correct fastener grade for a hydraulic cylinder mounting is not simply a question of strength — it also involves ductility, fatigue resistance, hydrogen embrittlement susceptibility, and corrosion protection in the operating environment. A grade 8.8 bolt has a minimum tensile strength of 800 MPa and a yield-to-ultimate ratio of 0.8, giving it enough ductility to absorb vibrational loads without sudden fracture. This makes grade 8.8 the standard choice for general-purpose hydraulic cylinder mounting on agricultural machinery across Yorkshire, forestry equipment in the Scottish Highlands, and most construction plant applications. Grade 10.9 fasteners (1000 MPa minimum tensile, 0.9 yield ratio) are used where space is restricted and a smaller diameter bolt must carry a higher clamping load — common in compact excavators and loader cylinders. Grade 12.9 is reserved for specialist applications such as hydraulic press cylinder tie-rods and high-cycle industrial presses, where the combination of high clamping force and tight dimensional tolerance justifies the additional cost. One important warning for UK engineers working in marine or offshore environments along the North Sea coast: high-strength fasteners (grade 10.9 and above) are susceptible to hydrogen embrittlement, particularly after electroplating with zinc or cadmium. Always specify a hydrogen embrittlement relief bake (190°C for 4 hours minimum per ASTM F1941) when using plated high-strength fasteners in critical hydraulic cylinder applications.
Yield: 640 MPa
General construction, agriculture
Best ductility
The workhorse of hydraulic cylinder fastening. Zinc-plated or hot-dip galvanised for corrosion resistance. Adequate for the vast majority of medium-duty hydraulic cylinder installations.
12.9: 1200 MPa
Presses, offshore, defence
H2 embrittlement risk
For space-critical or high-cycle applications. Specify hydrogen embrittlement bake after any electroplating. Check compatibility with your thread locker — some grades attack high-alloy steel.
Thread Sealing and Port Fitting Installation: BSP, BSPT, and Metric Hydraulic Ports
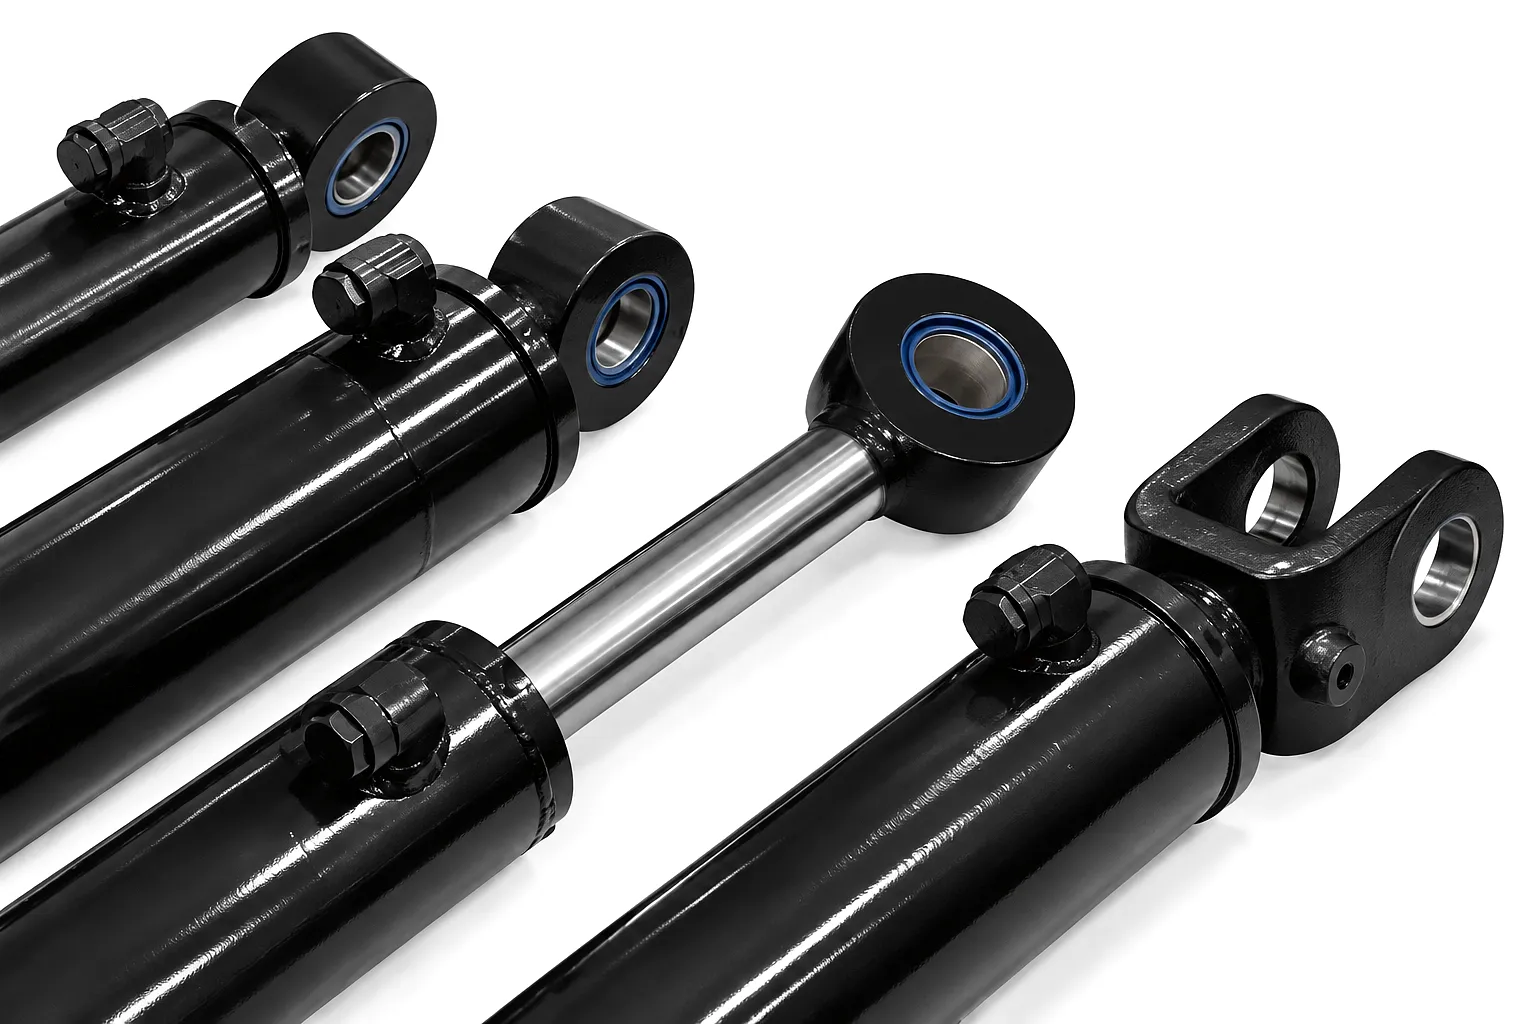 Port fitting torque is a separate discipline from structural fastener torque, but it is equally critical to the long-term integrity of any hydraulic cylinder installation. The UK uses British Standard Pipe (BSP) threads extensively — both the parallel BSPP form (ISO 228-1), which seals on a bonded seal or O-ring face, and the tapered BSPT form (ISO 7-1), which provides a degree of mechanical interference sealing in the thread itself. A common and costly mistake in UK workshops and machine shops throughout Birmingham, Wolverhampton, and Leeds is applying PTFE tape to a BSPP parallel port fitting that should be using an O-ring face seal or bonded seal washer. PTFE tape applied to a parallel thread creates the illusion of a seal but will extrude under pressure cycling, leading to slow hydraulic cylinder leaks that are notoriously difficult to locate because the fluid travels along the thread before escaping at the external hex. For BSPT tapered ports: wrap PTFE tape clockwise (viewed from the thread end), starting from the second thread, in two to three overlapping passes. For BSPP parallel ports: never use PTFE tape — install a bonded seal (Dowty washer) beneath the fitting hex, and torque to the value specified in the table above. Over-torquing BSPP fittings is also damaging: it can crack the cast iron or aluminium port boss, especially in lightweight hydraulic cylinders designed for material handling equipment across the UK’s warehousing and logistics sector.
| BSPP (parallel) | Bonded seal / O-ring face |
| BSPT (tapered) | PTFE tape + thread sealant |
| Metric (ISO 6149) | O-ring on port face |
| SAE straight (UNF) | O-ring on boss face |
| Mineral oil (HM/HLP) | PTFE tape or Loctite 542 |
| HF-E (water-glycol) | Loctite 565 or face seal |
| Phosphate ester | Face seal O-ring only |
| Biodegradable ester | Check compatibility — face seal preferred |
Step-by-Step Hydraulic Cylinder Installation Protocol for UK Industrial Applications
Whether you are installing a tie-rod cylinder on a material handling platform in a Leeds distribution centre or a welded heavy-duty cylinder on a steel press in a Sheffield fabrication shop, the installation sequence below should be treated as a minimum baseline procedure, supplemented by the cylinder manufacturer’s specific documentation and your site’s PSSR (Pressure Systems Safety Regulations 2000) competency requirements.
Before any fastener is inserted, inspect all threaded holes in the mounting structure for damage, contamination, or corrosion products. Run a thread tap or thread chaser through any hole that shows resistance, and blow clean with dry compressed air. Remove all hydraulic port plugs from the cylinder only at the point of connection — ports left open during installation risk contamination with swarf, moisture, or Loctite curing products that will cause seal and valve damage at commissioning. Inspect the cylinder rod for straightness using a dial indicator if the cylinder has been stored or transported horizontally; a bent rod will cause uneven seal loading from the first stroke.
Hydraulic cylinders must be aligned to their load path before a single fastener is torqued to final value. Misalignment introduces side loading on the cylinder rod, which accelerates rod seal wear, scores the chrome rod surface, and causes premature bearing failure in the rod eye or trunnion. Use a straight edge, laser alignment tool, or precision spirit level depending on the installation class. For cylinders handling eccentric loads — common in boom and arm applications on plant in the UK’s civil engineering sector — pillow block bearings or self-aligning rod eyes are specified at the design stage, but alignment verification at installation is still required. Hand-tighten all mounting bolts uniformly before torquing any to a higher value.
Using a calibrated torque wrench (calibration traceable to UKAS standards, calibrated within the previous 12 months), apply torque in three progressive passes in a star or cross pattern. Pass one: 30% of final torque. Pass two: 70% of final torque. Pass three: 100% of final torque. For flanged joints with six or more bolts, a fourth verification pass at full torque — working clockwise this time — catches any elastic interaction relaxation in the joint. Mark each bolt head with a witness line using torque-marking paint or a paint pen after the final pass; this is mandatory on sites operating under ISO 9001 quality management and is good practice on all installations. The witness line allows visual confirmation that no bolt has rotated loose between installation and the first scheduled inspection.
Connect hydraulic hoses or hard lines starting with the cylinder port that is on the non-pressure side during initial pressurisation — this prevents an uncontrolled rod extension during the first test cycle. Torque port fittings to the values shown in the table and confirm thread type before applying sealant. Bleed air from the circuit by operating the cylinder through several slow, low-pressure strokes with the system return line slightly loose to allow air to purge, then retighten. Pressurise to 1.0 times the cylinder working pressure and hold for two minutes, then to 1.25 times working pressure for a further two minutes. Inspect all connections for weeping or propagating wetness using a dry white rag — never use your hands near high-pressure connections, as hydraulic fluid injection injuries are a medical emergency. The UK Health and Safety Executive (HSE) lists hydraulic injection injuries under RIDDOR-reportable incidents where surgical intervention is required.
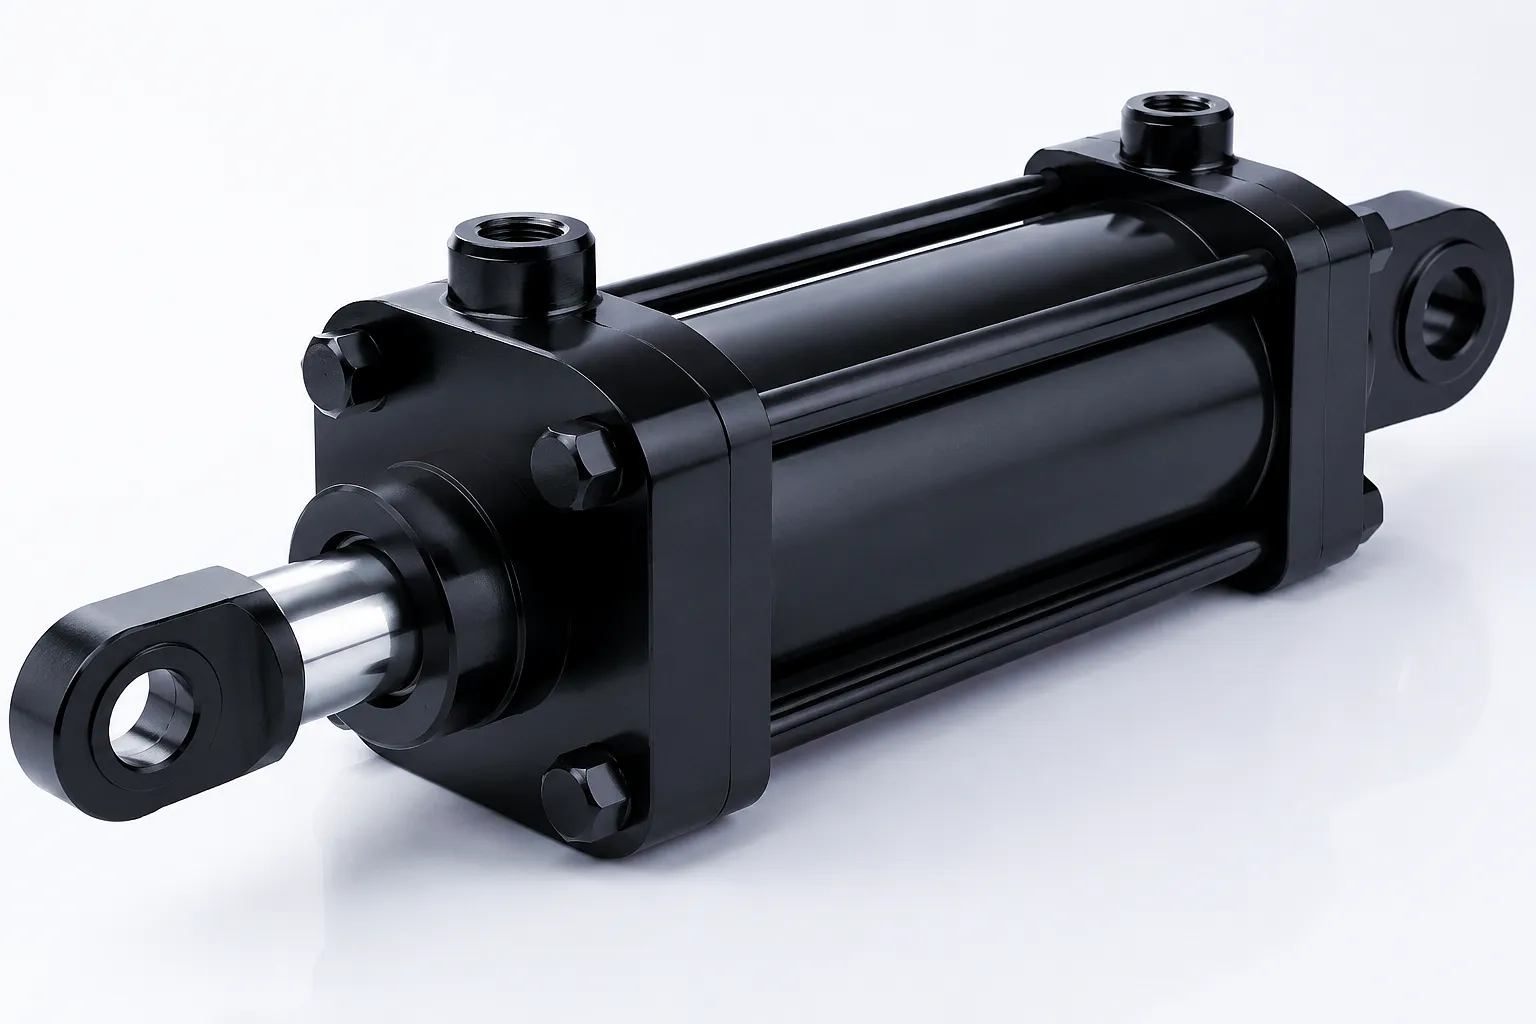
Application Scenarios: Where Correct Torque Practice Is Most Critical
Combine harvesters, round balers, and front loader arms subject hydraulic cylinders to severe vibration, mud contamination, and thermal cycling between cold mornings and operating temperature. The frequent disassembly of cylinders for winter storage means fastener condition is checked and torque verified more often than in static industrial installations. Torque settings for agricultural hydraulic cylinders are typically at the lower end of the grade 8.8 range, and thread locking compounds are avoided on pivot pin retainers that need field-replacement capability. Hydraulic cylinders for combine harvesters require specific attention to clevis pin torque and split pin replacement every season.
Telescopic and double-acting cylinders on lifting platforms face the most demanding combination of loads: variable eccentricity as the platform tilts, sudden dynamic loading when operators drive vehicles onto the deck, and frequent short-stroke cycling that prevents the rod seal from distributing wear evenly. LOLER (Lifting Operations and Lifting Equipment Regulations 1998) requires that lifting equipment is examined by a competent person and that examination reports specify whether fasteners meet the torque specification defined in the device’s technical file. Installers working to LOLER compliance should always use a calibrated torque wrench, retain calibration certificates, and record torque values in the equipment file. Custom telescopic cylinders for lifting platforms are a core offering from Ever Power, engineered to meet LOLER-relevant engineering standards.
Sheffield’s steel press and forging operations use hydraulic cylinders generating forces of 500 to 5000 tonnes. At these force levels, even small fastener torque variances produce measurable frame distortion that affects part dimensional consistency. The tie-rod tensioning on large hydraulic presses is a precision engineering task: rod nuts are typically torqued using hydraulic bolt tensioners rather than torque wrenches, achieving consistent clamping loads of ±2% across all rods simultaneously. The record of each tensioning operation — including hydraulic tool pressure, rod stretch measurement, and final turn angle — forms part of the press acceptance record and must be retained for the life of the machine. Mismanaged tie-rod torque on a Sheffield press has historically caused off-centre ram loading, which cracks the press frame at the tie-rod bore — a repair that costs weeks of downtime and is entirely preventable.
HS2, major road expansion programmes, and port infrastructure projects across Bristol, Liverpool, and the Humber Estuary all use large excavators with hydraulic boom and arm cylinders that see continuous operating cycles often exceeding 20 hours per day. On these machines, pin retention fastener torque is checked at every 1000-hour service interval, and cylinder mounting bracket bolt torque at every 500-hour interval. The high-vibration environment created by rock breaking and demolition attachment work is particularly aggressive toward fastener retention. Loctite medium-strength threadlocker (typically 243 or equivalent) is standard on pin retainer bolts in these applications; high-strength threadlocker should be avoided on bolts that maintenance technicians may need to remove in the field without a heat source.
Ever Power — Precision Hydraulic Cylinder Manufacturing & Global Supply
Custom-engineered hydraulic cylinders, built to your torque, pressure, and dimensional specification — with full traceability documentation for UK compliance requirements.
Ever Power manufactures hydraulic cylinders to bore diameters from 25 mm to 650 mm, with rod diameters from 12 mm to 400 mm. Mounting styles — clevis, flange, foot, trunnion, and custom fabricated — are produced to drawing with thread forms specified per customer standard: ISO metric, BSP, BSPT, UNF, or customer-specific profiles. All fastener hole positions and thread depths are CMM-verified against the accepted drawing before dispatch. This precision eliminates the field adjustment problem that delays commissioning on custom hydraulic cylinder installations at UK engineering sites.
Cylinder barrels are manufactured from precision-honed seamless hydraulic tubing to EN 10305-4, supplied with a hardness certificate confirming Ra 0.4 or better bore finish. Rods are ground and hard chrome plated to 15–25 microns, with chrome deposit hardness specified at 850–1000 HV. For UK coastal and offshore applications, Ever Power offers nickel-chrome composite plating and stainless steel rod options in 316L grade — eliminating the corrosion mechanism that most frequently causes hydraulic cylinder rod seal failure in marine environments along the UK coastline.
Every hydraulic cylinder dispatched from Ever Power undergoes hydrostatic pressure testing at 1.5 times the rated working pressure, with a minimum five-minute hold. Test certificates are issued with each unit and include the serial number, test pressure, test date, and inspector signature. For UK orders subject to PSSR compliance, Ever Power can supply a pressure equipment technical file on request, supporting the customer’s written scheme of examination. Logistics to UK ports — Felixstowe, Southampton, and Tilbury — are handled on DDP Incoterms with full insurance and customs clearance documentation, minimising the administrative burden on UK procurement teams.
Contact Ever Power — Get a Custom Quote
Email: [email protected] | Technical drawings welcome
Customer Success Story: Sheffield Precision Forgings Ltd.
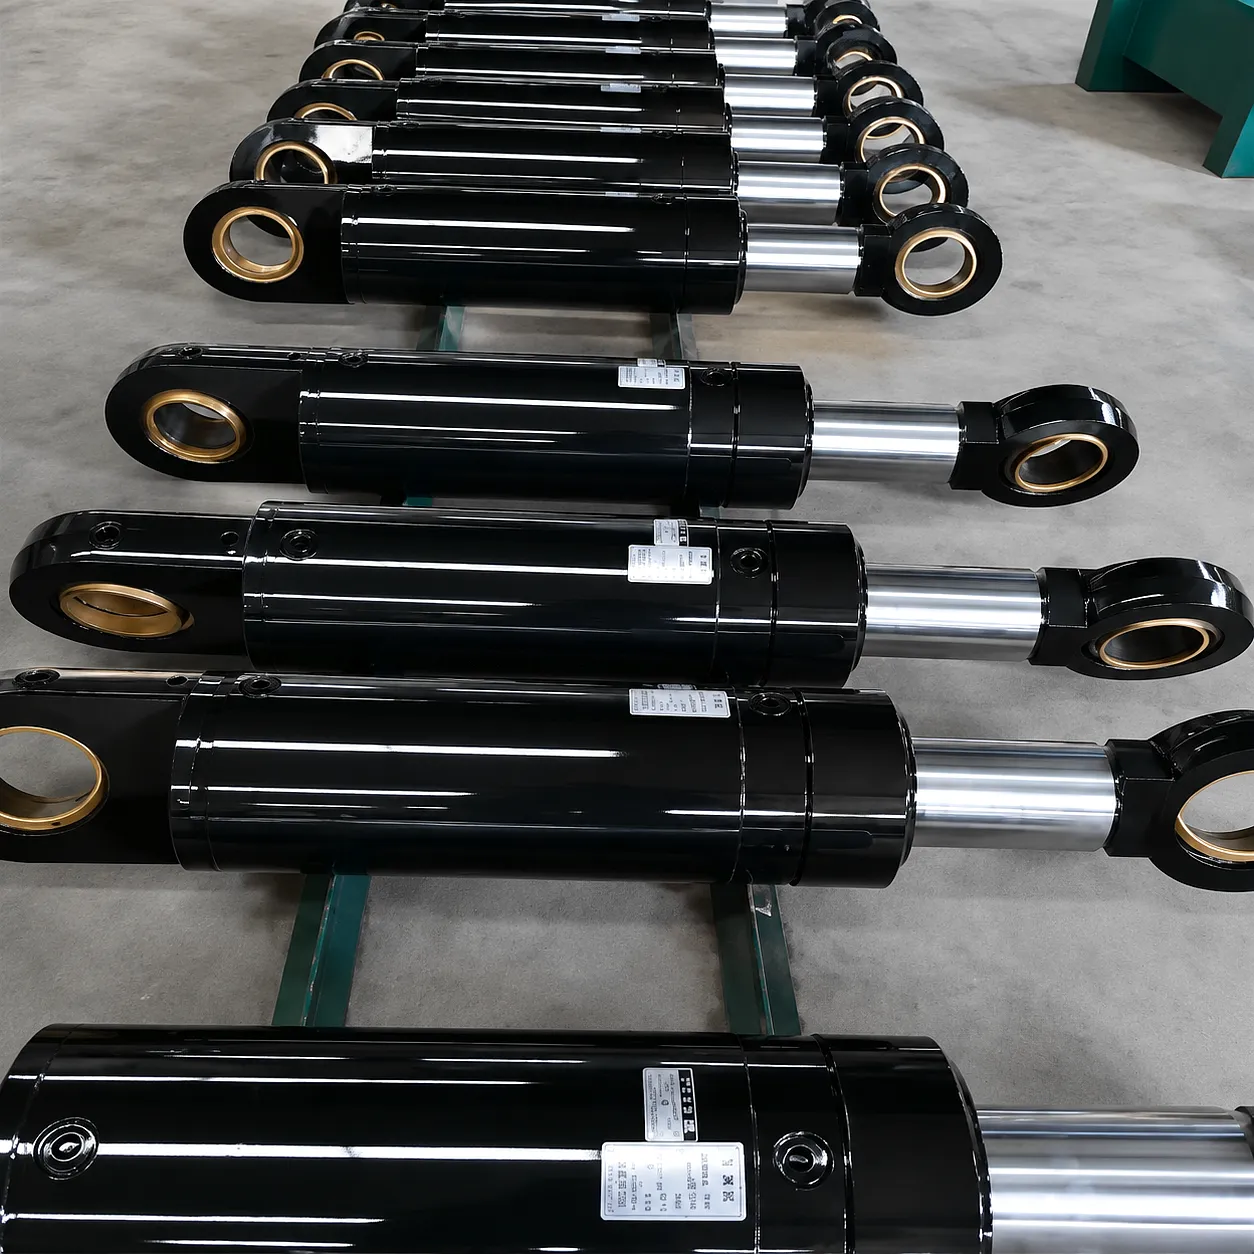 Sheffield Precision Forgings Ltd., a third-generation steel forging business operating a 1,200-tonne hydraulic press for automotive die components, contacted Ever Power after experiencing repeated hydraulic cylinder end cap separation on their primary forging press cylinder. The failure mode was consistent: after approximately 8,000 to 10,000 press cycles, the six-bolt end cap flange on a 320 mm bore welded cylinder would develop a hydraulic fluid weep at the face seal, rapidly progressing to full weep and forced shutdown. Their internal maintenance team had replaced the face seal O-ring four times in three years without resolving the root cause. Downtime cost per incident averaged £14,000 in lost production and emergency labour.
Ever Power’s technical team conducted a remote engineering review of the cylinder drawings and installation records provided by Sheffield Precision Forgings. The diagnosis was clear: the end cap bolts were M20 Grade 8.8, but the torque specification in the installation manual called for 350 Nm — a value consistent with Grade 8.8 dry. The maintenance records showed that the replacement bolts sourced locally were zinc-chrome plated and the torque wrench used was the maintenance team’s general-purpose model, last calibrated two years earlier. Applying a 350 Nm dry torque value to a plated bolt generates a clamping load approximately 25% lower than specified, due to the reduced nut factor of the plated surface. Over thousands of press cycles, this under-clamped end cap joint was flexing, gradually extruding the O-ring from its groove, and allowing hydraulic pressure to track along the bolt to the exterior.
Ever Power supplied three replacement cylinders with the same 320 mm bore, specified with Grade 10.9 end cap bolts to provide a higher torque-to-clamping-load ratio using a more forgiving plated torque coefficient, and included a revised installation procedure specifying 485 Nm for the plated Grade 10.9 M20 fasteners with a UKAS-calibrated torque wrench. The cylinders have now completed over 60,000 press cycles with zero end cap incidents. Ever Power’s logistics team arranged delivery to Sheffield on a 5-day lead time from drawing confirmation, with DDP delivery directly to the press shop floor.
What Our Customers Say
“The technical consultation Ever Power provided was more thorough than anything we had received from domestic cylinder suppliers. They identified the torque and plating mismatch within two days of receiving our drawings, and the replacement cylinders have been running without a single incident for over a year. The calibrated torque installation guide they supplied is now standard procedure on our press shop.”
“We operate a fleet of agricultural lifting trailers across Yorkshire and needed cylinders with specific clevis dimensions and BSP port configurations. Ever Power delivered exact-specification cylinders with the technical file documentation our LOLER examiner requires. The 5-day delivery to our workshop in Harrogate was excellent — no extended lead times, no port delays.”
“The customisation capability at Ever Power is genuinely impressive. We needed a 200 mm bore cylinder with a non-standard 6-bolt flange pattern to fit a Birmingham automotive press retrofit project. Their engineers turned around the drawing approval in 48 hours and delivered four cylinders to our Solihull facility within ten days. The CMM verification certificates came with the shipment, which is exactly what our customer’s QA team needed.”
 Indonesian
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Malay
 French
 Greek