
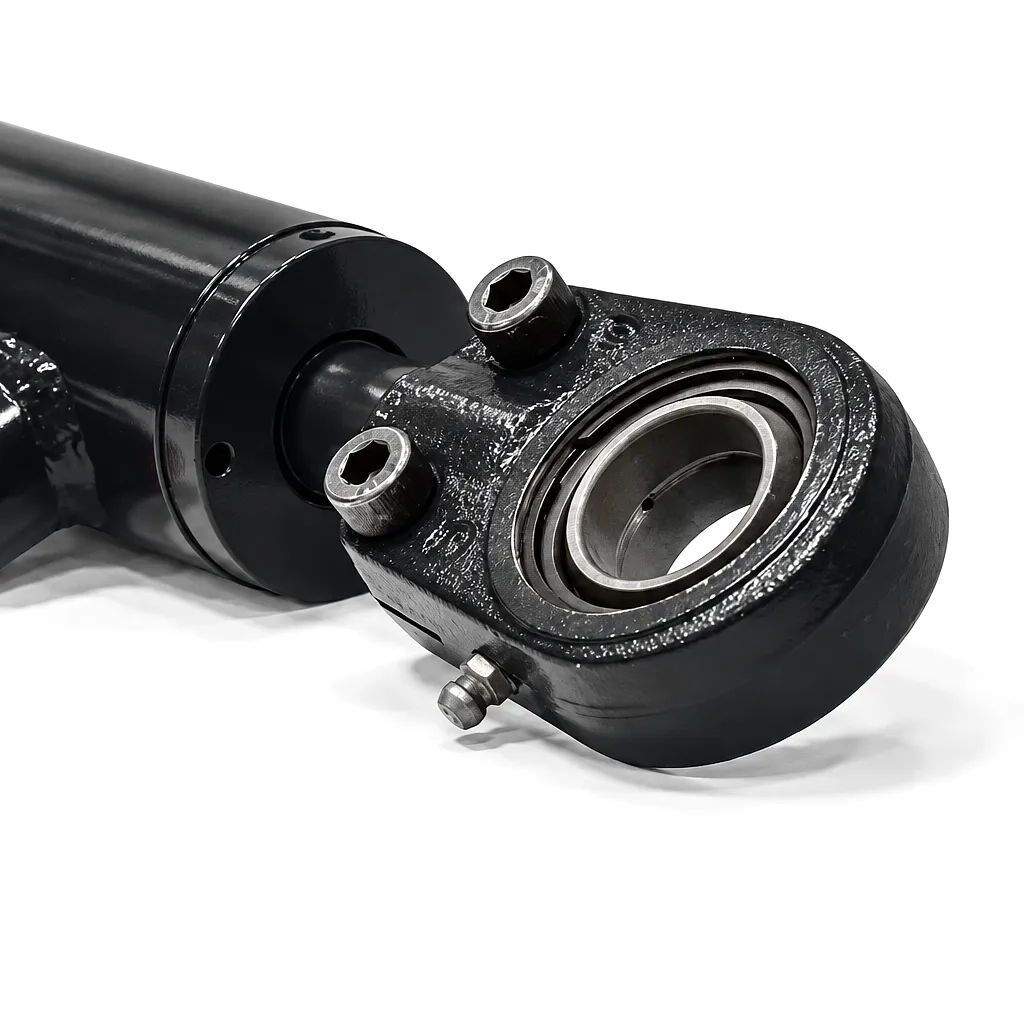
 In hydraulic cylinder engineering, one detail quietly determines whether a system runs cleanly for a decade or bleeds fluid within months — the chrome layer on the piston rod. Hard chrome plating is not cosmetic. It is a precision tribological interface: the surface that interacts with seals thousands of times per cycle, bearing the full burden of pressure containment, environmental exposure, and mechanical abrasion. Get the chrome thickness wrong, and no matter how well-engineered the rest of the cylinder is, seal degradation follows. The geometry of the plated surface, measured in microns, dictates friction coefficients, fluid film retention, and the precise rate at which polyurethane or PTFE seal lips wear down under load.
The Electrochemical Mechanism Behind Hard Chrome Plating on Hydraulic Rods
Hard chrome plating on hydraulic piston rods is deposited via electroplating from a hexavalent or trivalent chromium electrolyte bath. A current passes through the solution, causing chromium ions to migrate and deposit atom by atom onto the steel substrate. The deposit is crystalline, extremely hard — typically 850–1,100 HV on the Vickers scale — and exhibits a characteristic network of micro-cracks at the surface. These micro-cracks, when properly controlled, act as microscopic oil reservoirs that maintain a continuous lubricating film between the rod surface and the seal lips during reciprocating motion.
The deposit builds up over the entire rod surface at a relatively uniform rate, though corners and edges tend to attract heavier deposition. This is why reputable manufacturers like Ever Power apply post-plating grinding and superfinishing processes to bring the plated rod back to its precise dimensional specification — typically Ra 0.1 to 0.4 µm surface roughness — ensuring a seal contact surface that is smooth enough to prevent abrasion yet textured enough to retain the oil film essential for low-friction sliding.
Chrome Thickness Standards and Why the Numbers Matter More Than You Think
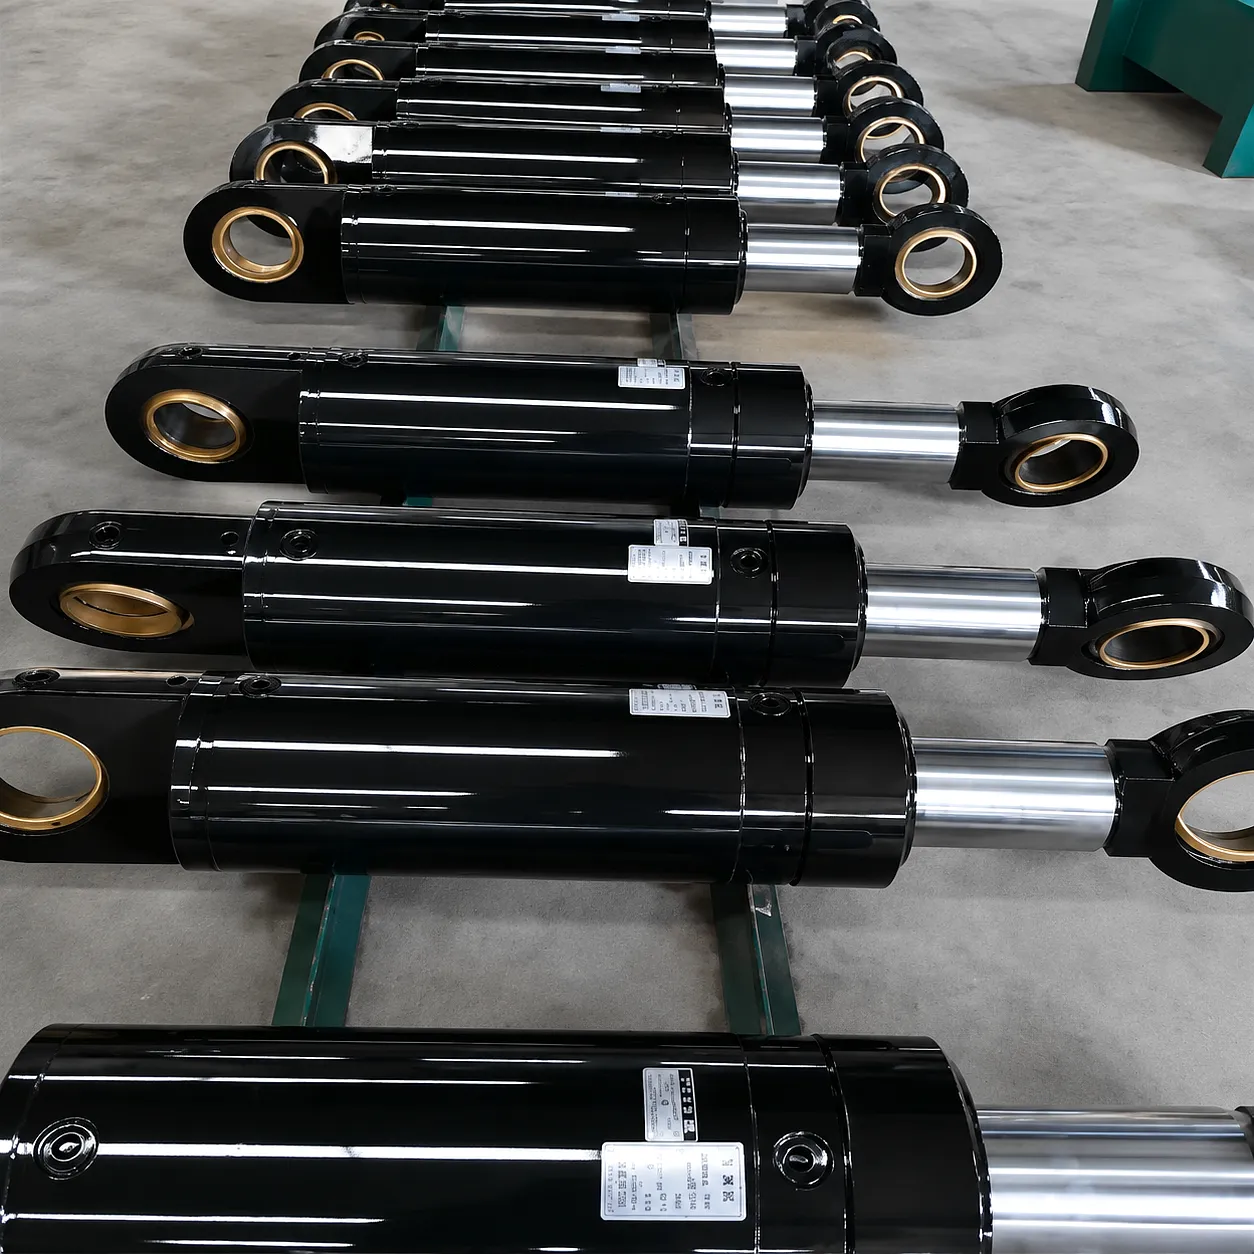
The hydraulics industry has converged on chrome plating thickness ranges that reflect decades of empirical evidence from field failures and laboratory tribology research. For standard industrial hydraulic cylinders operating at pressures up to 250 bar, a chrome layer of 15 to 25 µm (micrometres) after grinding provides the optimal balance between wear resistance, substrate adhesion, and corrosion protection. At this thickness, the plated layer is deep enough to accommodate the micro-crack network without propagating cracks through to the steel base metal — a critical failure mode that initiates pitting corrosion and accelerates rod-to-seal abrasive wear dramatically.
Heavy-duty applications — including the kinds of telescopic cylinders used in refuse vehicles operating out of Birmingham depots, or the long-stroke boom cylinders on aerial work platforms deployed on UK construction sites — require thicker deposits, typically 30 to 50 µm, to withstand the cumulative abrasion of contaminated environments and extended service intervals. For offshore or marine applications, where salt spray and moisture impose additional corrosion loading, specifications may call for 50 to 75 µm deposits with additional sealing via post-plating treatments.
What is less well understood in the field is that going too thick creates its own problems. Deposits exceeding 75 µm begin to exhibit greater internal tensile stress and a higher density of through-crack networks. When these cracks are wide and interconnected, the lubricating oil film retention advantage inverts — the cracks become pathways for corrosive media to reach the steel substrate, and the rough crack edges impose higher abrasive loads on seal lips than a properly finished thin deposit would. This is why specification-led procurement from experienced manufacturers like Ever Power, rather than simply demanding “more chrome,” produces better long-term outcomes for UK plant operators.
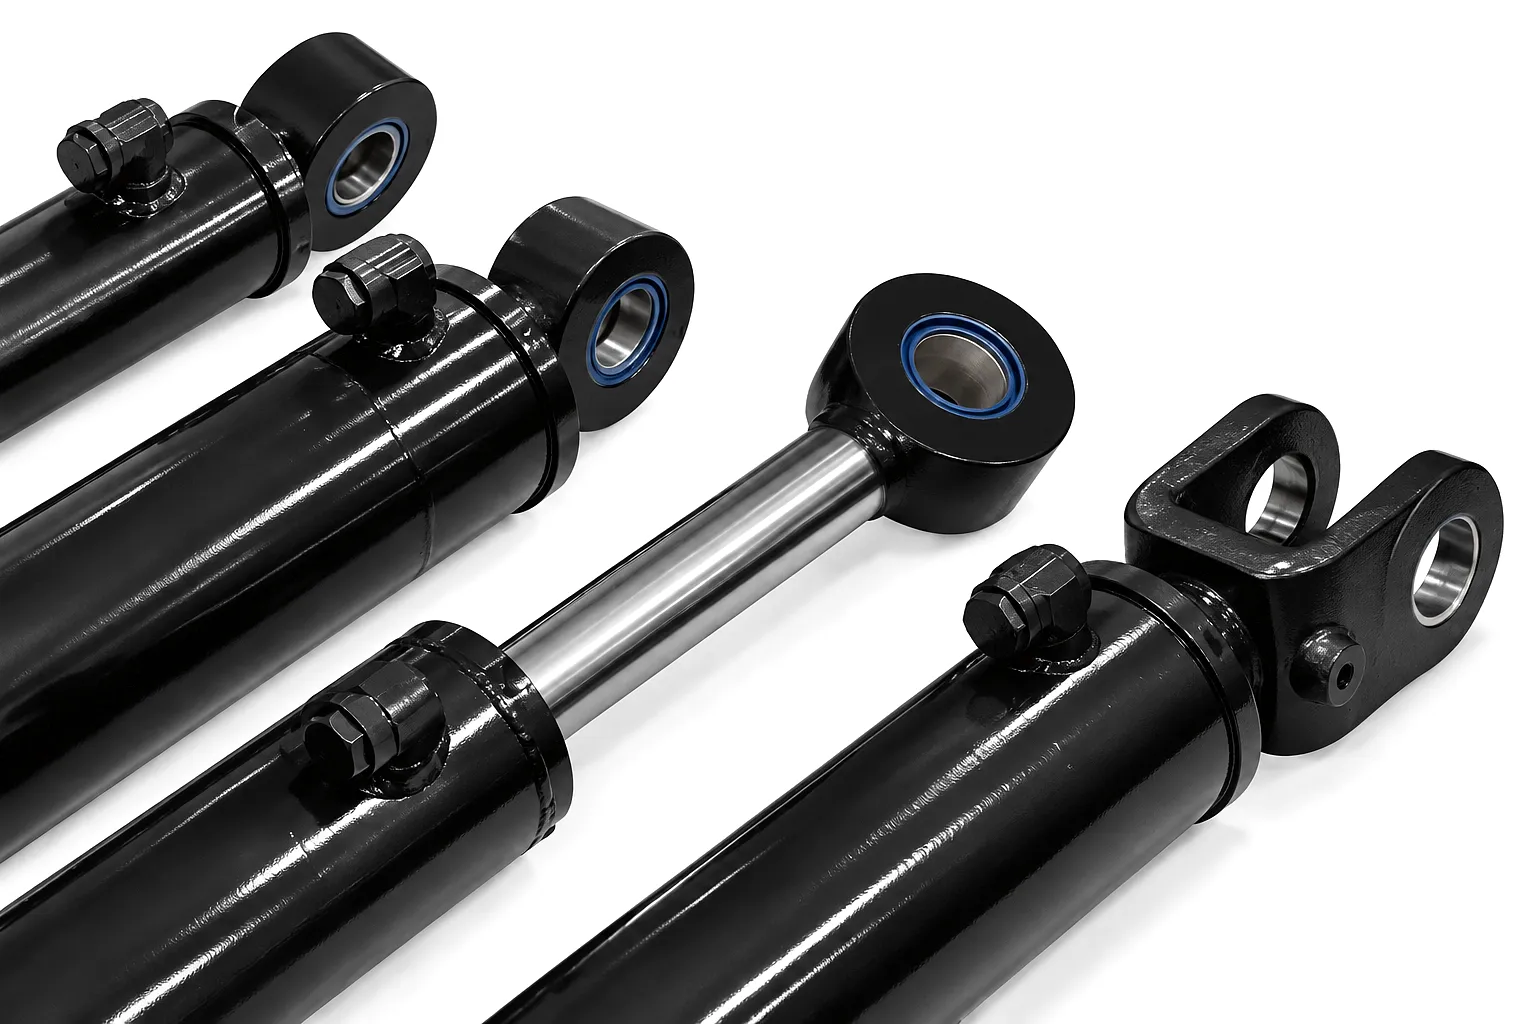
Chrome Plating Thickness Standards — Technical Performance Parameters
| Application Category | Chrome Thickness (µm) | Operating Pressure | Surface Roughness Ra | Expected Seal Life | Notes |
|---|---|---|---|---|---|
| Light Industrial / Mobile | 15 – 25 µm | Up to 160 bar | 0.2 – 0.4 µm | 3,000 – 6,000 hr | Standard PTFE or PU seals |
| Heavy Industrial | 25 – 40 µm | 160 – 250 bar | 0.1 – 0.3 µm | 6,000 – 12,000 hr | Steel/mining sector use |
| Aerial Work Platform / Construction | 30 – 50 µm | Up to 280 bar | 0.1 – 0.25 µm | 8,000 – 15,000 hr | Outdoor UK weather exposure |
| Marine / Offshore | 50 – 75 µm | Up to 350 bar | 0.1 – 0.2 µm | 10,000 – 20,000 hr | Plus nickel undercoat recommended |
| High-Cycle Precision Systems | 20 – 35 µm | 100 – 200 bar | 0.05 – 0.15 µm | 10,000 – 25,000 hr | Superfinished, ultra-low friction |
How Hard Chrome Surface Quality Directly Controls Seal Degradation Rates
The relationship between chrome plating quality and hydraulic seal wear is not linear — it is a multi-variable interaction that encompasses surface roughness, micro-crack geometry, lubricant film retention, and the compliance characteristics of the seal material itself. When a hydraulic rod reciprocates, each stroke pushes the rod surface past the seal lips under a defined contact pressure determined by the system pressure and the seal’s elastic return force. At the contact interface, three things happen simultaneously: the oil film is continuously replenished from the micro-crack reservoirs in the chrome, the seal lip elastomer deforms slightly to conform to surface irregularities, and any abrasive particles trapped in the interface cause progressive micro-cutting of the seal material.
A chrome surface with a Ra of 0.2 µm retains enough oil to maintain a hydrodynamic film across the majority of the seal contact zone during normal operating speeds above roughly 0.05 m/s. Below this speed — during slow-speed positioning typical of aerial platform fine-adjustment operations — the film degrades and boundary lubrication conditions prevail, placing far greater demands on the hardness and surface geometry of the chrome. This is precisely why fine-pitch bore-honed cylinders used in precision aerial platforms specify tighter Ra tolerances than standard construction cylinders. The chrome specification is not the same document for every application — it should be engineered to the duty cycle.
Rod seals in outdoor UK hydraulic systems are exposed to combined moisture, particulate ingress, and temperature cycling between -15°C and +40°C. Chrome porosity above 5% under these conditions permits corrosive moisture to permeate to the base metal, creating rust tubercles that are abrasive enough to destroy seal lips within hundreds rather than thousands of operating hours.
Seal Material Compatibility with Hard Chrome Plating: Polyurethane, PTFE, and NBR
Polyurethane rod seals offer the highest abrasion resistance of common hydraulic seal materials, tolerating chrome surface roughness up to Ra 0.4 µm without significant wear acceleration. Their mechanical elasticity allows them to self-adjust against minor chrome surface irregularities, but they are sensitive to temperature cycling above 80°C, which can cause the seal lip to lose conformance if the chrome’s surface film is disrupted. PU seals perform exceptionally on boom cylinder rods operating across UK construction sites — applications where daily cycles between ambient temperature and hydraulic oil heat stress the seal material repeatedly throughout a service life spanning several years.
PTFE-based seals, often with bronze or glass fibre reinforcement, demand the most exacting chrome surface finishes — Ra below 0.15 µm — but reward that precision with extraordinarily low friction coefficients and extremely long service lives. PTFE does not elastically conform to surface roughness the way PU does; instead, it develops a thin PTFE transfer film on the chrome surface during the initial run-in period. If the chrome is too rough, this transfer film is continuously disrupted and the seal wears rapidly. When chrome plating and finishing are executed correctly, PTFE seals on precision hydraulic rods in Sheffield’s advanced manufacturing facilities have demonstrated service lives exceeding 20,000 operating hours.
Nitrile rubber seals remain cost-effective for many standard hydraulic applications, but they are the most sensitive to chrome surface quality. NBR’s relatively low hardness — typically Shore A 70–90 — means that any asperities on the chrome surface above Ra 0.5 µm impose measurable abrasive wear on each stroke. For UK-sourced hydraulic systems where NBR is specified for cost reasons, a chrome specification towards the finer end of the Ra 0.2–0.4 µm range becomes critical. Attempting to extend seal service life through more frequent oil changes while neglecting chrome condition is a documented false economy frequently encountered in older plant across the Midlands industrial corridor.
Hard chrome rod to 30–50 µm specification, superfinished to Ra 0.2 µm for maximum seal compatibility in outdoor UK AWP applications.
Precision-plated rod with Ra 0.15 µm finish and chrome thickness matched to the duty cycle of UK urban access platform operations.
Industrial Application Scenarios: Where Chrome Thickness Specification Is Mission-Critical
The correct chrome thickness is not a single number applied across all hydraulics — it is a context-dependent engineering decision that varies by industry, duty cycle, environment, and the specific seals in the system. The following scenarios, all drawn from active UK industrial contexts, illustrate why matching chrome specification to application prevents premature seal failure and unplanned downtime.
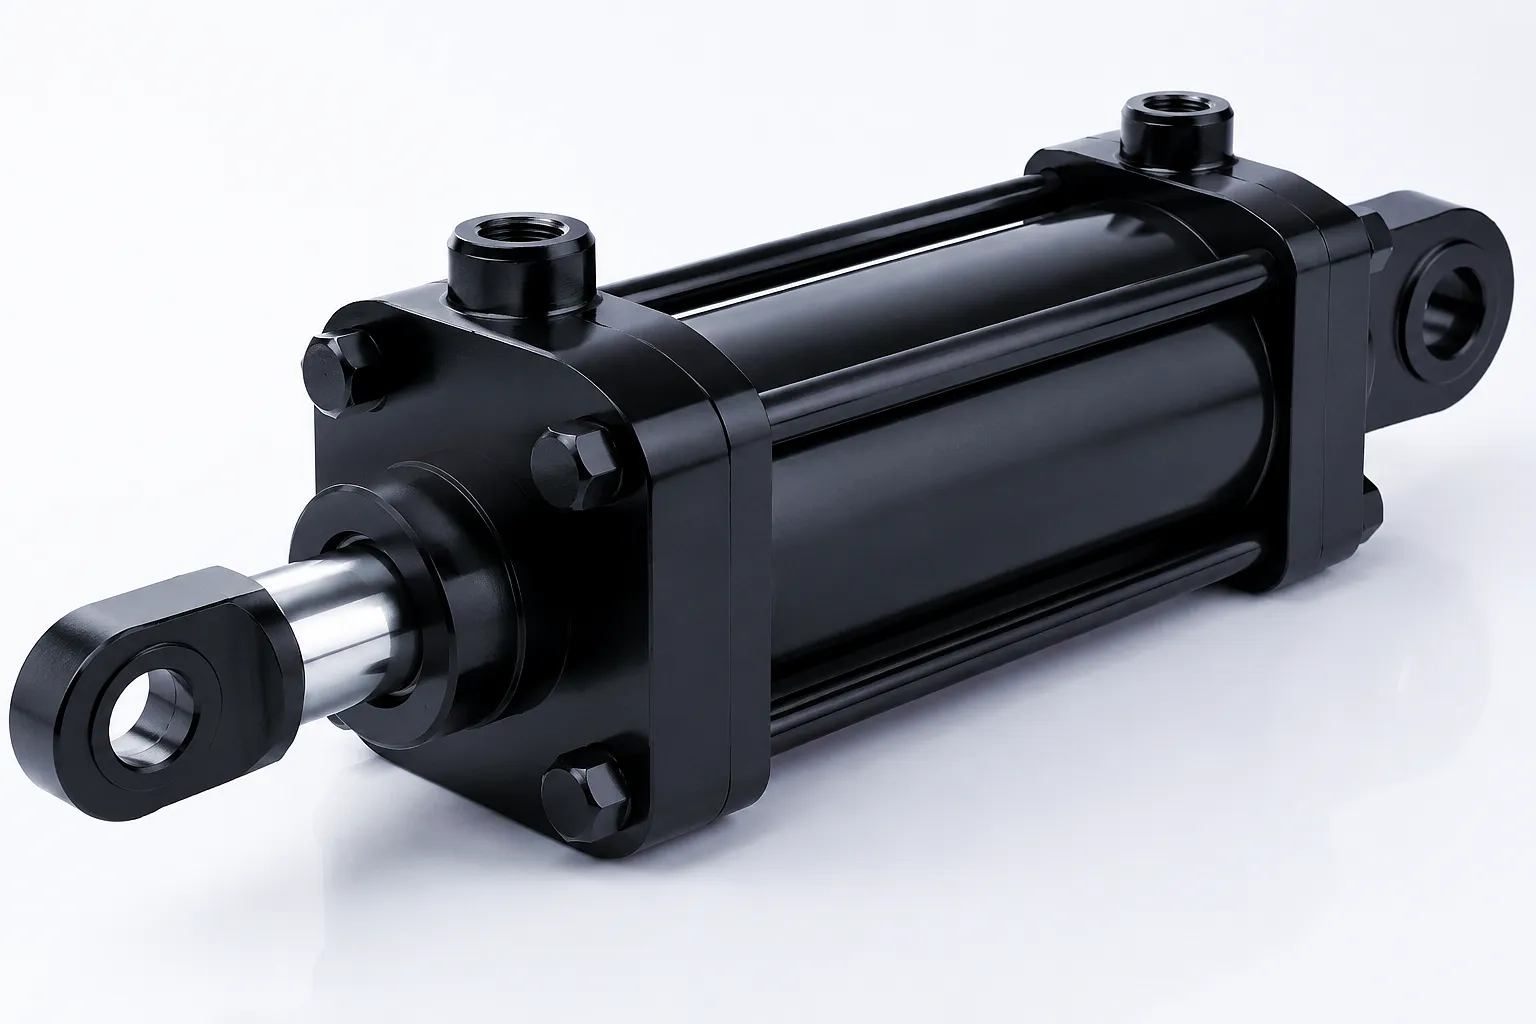
Core Technical Advantages of Properly Specified Hard Chrome Plated Hydraulic Rods
Hard chrome’s micro-crack network retains hydraulic oil under pressure, maintaining a continuous lubricating film that reduces friction coefficients at the seal interface by up to 40% compared to unplated or zinc-coated alternatives, directly extending seal service life and reducing operating temperature.
At 850–1,100 HV, hard chrome resists surface damage from hydraulic particle contamination ISO 4406 Class 16 and below without scoring — scores that would act as seal-destroying abrasives on softer rod materials. This hardness also prevents fretting fatigue at the seal-rod interface under high-cycle conditions.
A properly deposited and sealed chrome layer provides 240+ hours of salt spray resistance per ISO 9227 at 25 µm thickness, rising to 500+ hours at 50 µm with nickel undercoat — a performance level that protects rod integrity through the wet British climate and prevents the rust tubercle formation that is the primary cause of accelerated seal wear in outdoor hydraulic equipment.
Chrome plating adds to the rod diameter in a highly controllable and predictable manner, and post-plating grinding restores the rod to its exact specified diameter with tolerances of ±0.01 mm achievable at production scale. This precision ensures that seal lip contact pressure remains within design parameters throughout the rod’s service life, preventing the over-compression or under-engagement that causes either premature wear or hydraulic leakage.
Hard chrome retains its mechanical properties up to approximately 400°C, well beyond the service temperature of any hydraulic seal material in current use. This thermal stability means that in furnace-adjacent or foundry applications — environments such as Birmingham’s automotive die casting plants — the chrome does not soften or micro-plastically deform under the combined loading of pressure and heat that would affect alternative surface treatment methods.
Unlike many hard coating technologies, electroplated chrome can be stripped and re-deposited on worn rods multiple times without compromising the base metal geometry, provided the substrate is free from corrosion pitting. This gives гидравликалық цилиндр users a cost-effective maintenance route: rather than purchasing a replacement rod assembly, a worn rod can be re-plated and ground to original specification — an approach widely used by hydraulic service centres across the UK’s engineering heartlands.
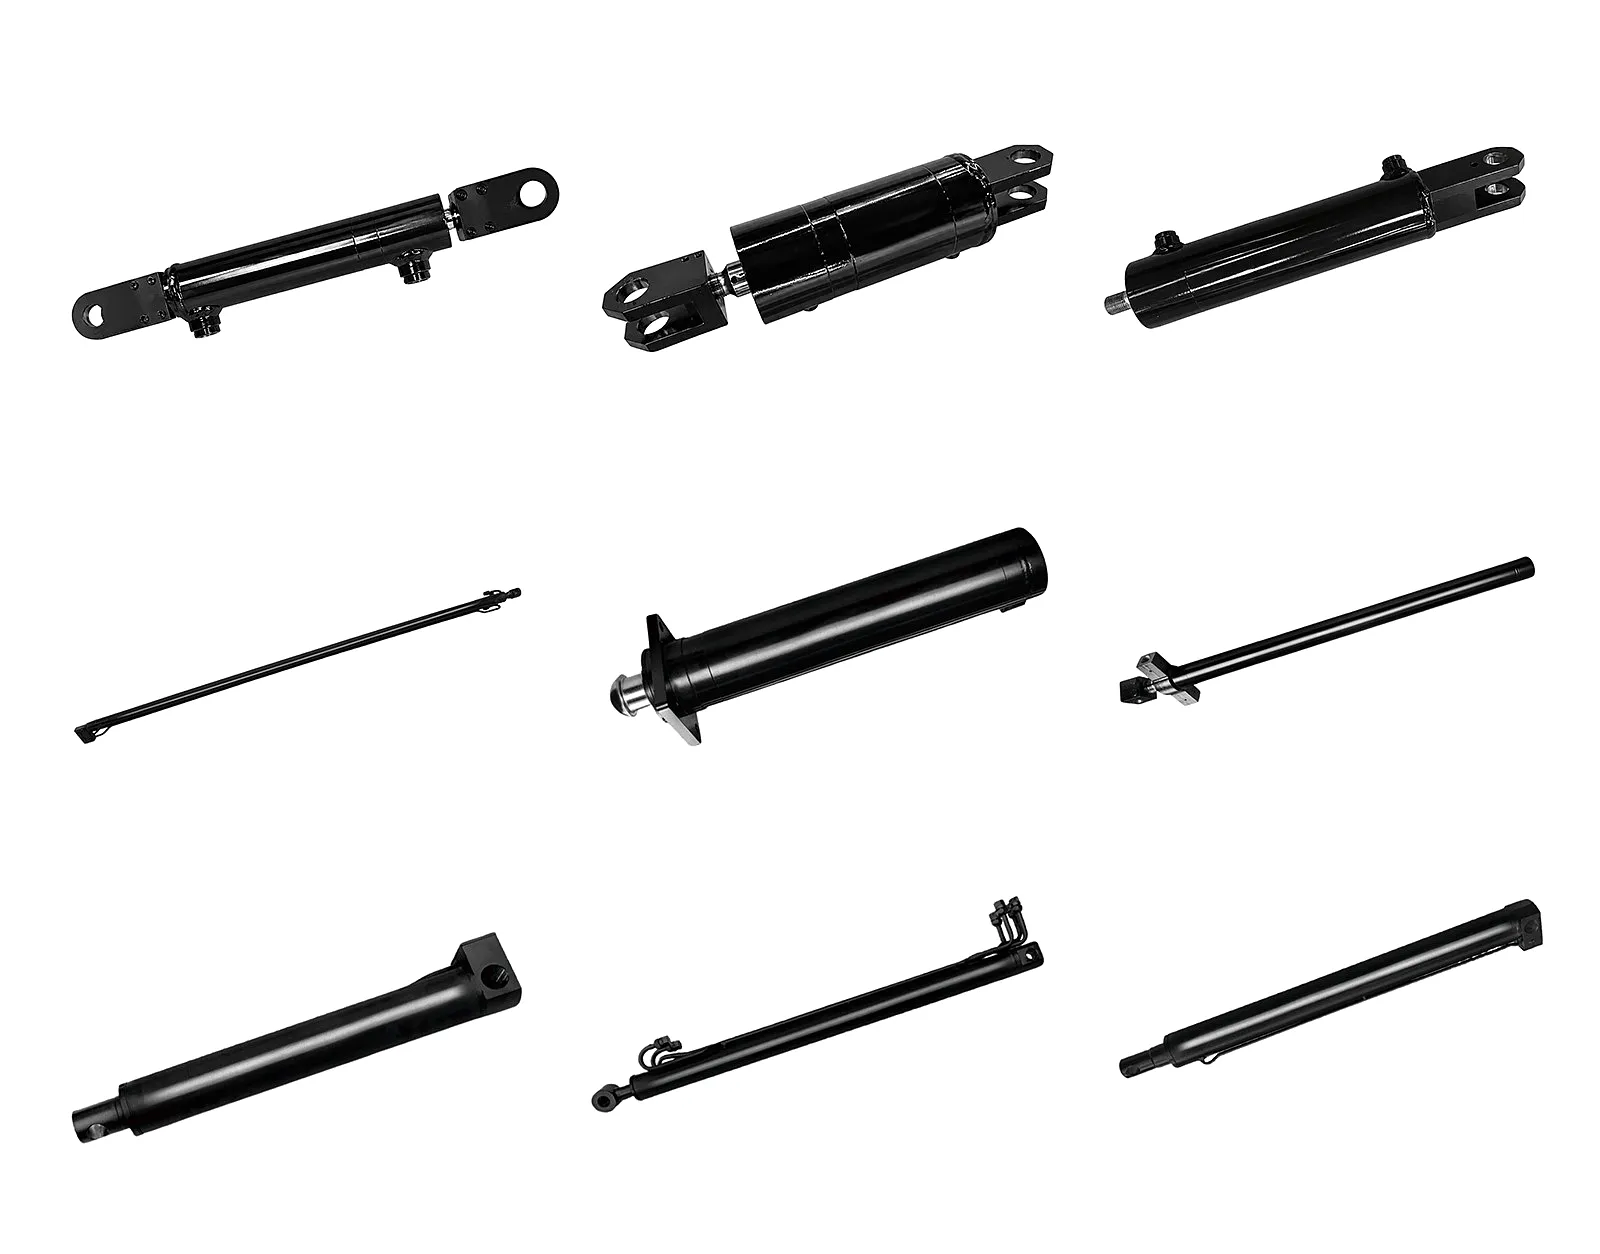
Ever Power: Precision Chrome Plating, Custom Hydraulic Cylinder Manufacturing, and UK Export Supply Chain
Ever Power operates dedicated hydraulic cylinder manufacturing facilities equipped with automated electroplating lines that maintain bath chemistry, current density, and temperature within tight tolerances across each production run. The chrome plating process at Ever Power is not a batch-production afterthought — it is a central engineering discipline with dedicated quality engineers, bath analysis conducted every four hours, and SPC (Statistical Process Control) charting of plating thickness on every rod lot. Post-plating, every rod passes through CNC cylindrical grinding and superfinishing stages that consistently deliver Ra 0.05 to 0.2 µm surface finish, verified against ISO 4287 with profilometer measurement.
Customisation capability is a genuine differentiator at Ever Power. UK customers across the aerial platform, offshore, and specialist manufacturing sectors regularly require chrome specifications that deviate from catalogue standards — whether that means a 65 µm marine-grade deposit with intermediate nickel on a 100 mm diameter rod, a specialist low-friction superfinished surface for a PTFE-sealed precision positioning cylinder, or a rod diameter tolerance of ±0.008 mm for a replacement part where the original manufacturer’s specification must be matched exactly. Ever Power’s engineering team works directly with UK customers’ technical buyers to develop a plating specification datasheet for each custom order, covering deposit thickness band, Ra target, porosity test method, and inspection protocol.
The supply chain from Ever Power to UK customers is supported by sea freight consolidation with typical lead times of 28–35 days ex-works for standard orders, with express air freight options available for maintenance-critical replacement cylinders. All shipments include a full material certificate, plating inspection report, and dimensional check certificate — documentation that satisfies the traceability requirements of UK OEMs and industrial operators under BSI and BSEN standards.
20 – 360 мм
6000 мм дейін
10 – 100 мкм
0,05 мкм
400 бар (арнайы тапсырыс бойынша)
ISO 9001, CE
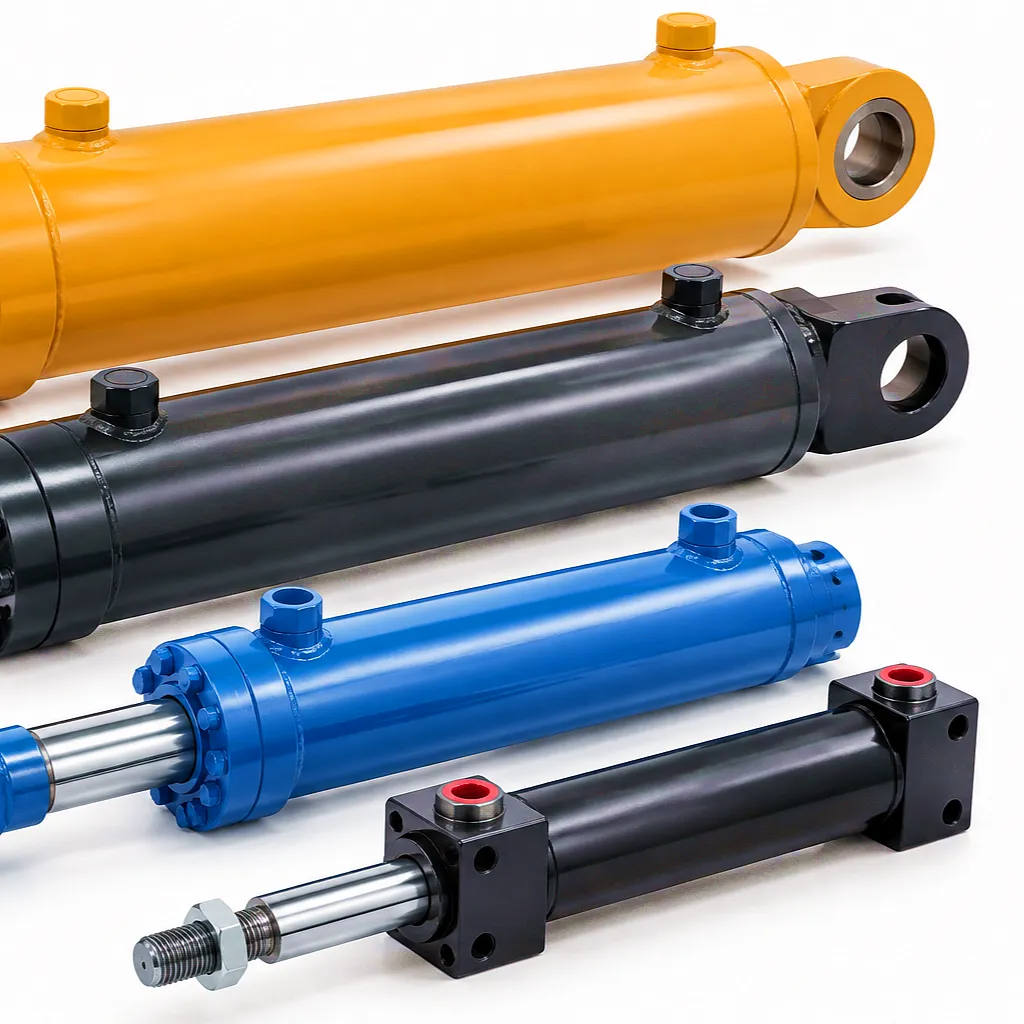
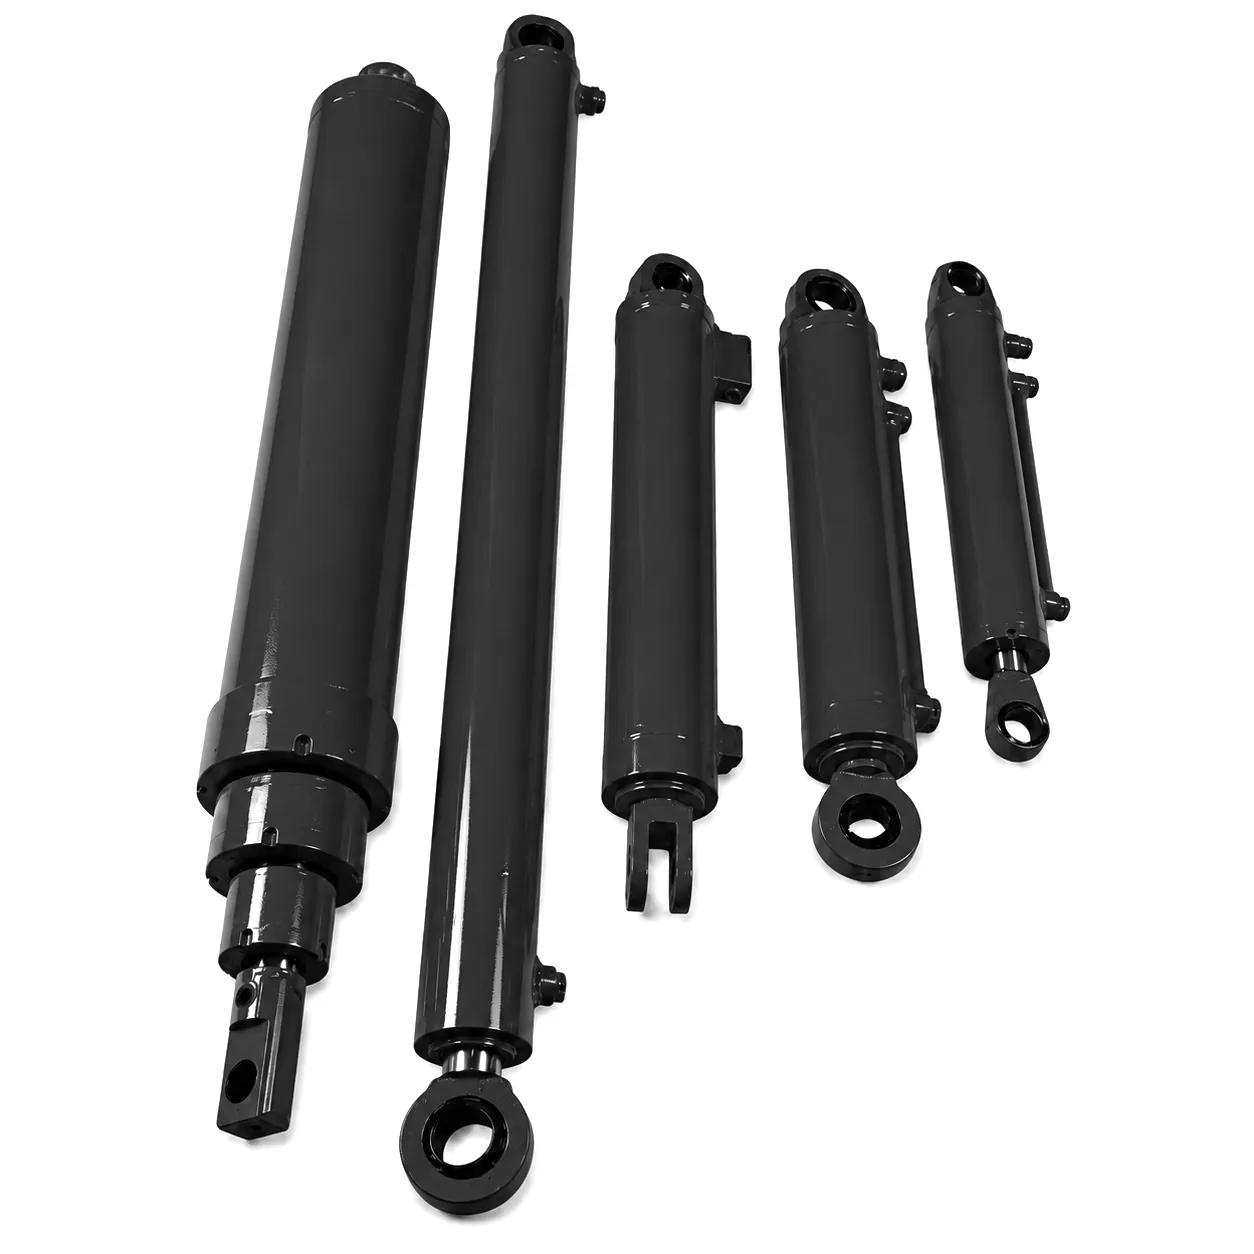
Ұлыбританиялық инженерлер мен сатып алу мамандары Ever Power Chrome шыбық цилиндрлері туралы не айтады
«Біз Felixstowe-дегі контейнерлерді өңдеу жабдықтарымызда үш маусым бойы 35 мкм хром сипаттамасы бар Ever Power цилиндрлерін бірде-бір шыбық тығыздағышын ауыстырмай пайдаландық. Беткі өңдеу сапасы алдыңғы жеткізушімізден алған сапасымыздан айтарлықтай жақсы — біздің техникалық қызмет көрсету тобымыз шыбықтарды алған кезде тексерген кезде айырмашылықты бірден байқады. Жағалаудағы порт ортасы үшін никель астарлы жабын опциясы міндетті емес — бұл өте маңызды, және Ever Power командасы бұл туралы білім алудың қажеті жоқ екенін түсінді».
«Біздің PTFE тығыздалған дәл цилиндрлеріміз үшін сұраған арнайы Ra 0,12 мкм суперфиниш дәл спецификацияға сәйкес жеткізілді, әрбір шыбық үшін профилометр өлшеу сертификаттары қосылды. Біздің ISO сапа жүйеміз осындай құжаттама деңгейін талап етеді және бұл баға санатында шынымен сирек кездеседі. Хром қалыңдығы 1800 мм шыбық ұзындығы бойынша біркелкі болды - біз тексердік. Ever Power компаниясының бәсекеге қабілетті бағамен техникалық тұрғыдан талап етілетін спецификацияны қолдай алу қабілеті - біз қазір барлық дәлдік гидравликасын сатып алуды оларға тапсырдық».
«Біз әуедегі жұмыс платформаларындағы штанга тығыздағыштарын әр он екі-он алты ай сайын ауыстырып отырдық және бұл жай ғана ашық ауада жұмыс істеуден қалыпты тозу деп ойладық. Ever Power техникалық тобы біздің бұрынғы цилиндр жеткізушіміз ешқашан көтермеген хром сипаттамалары туралы сұрақтар қойды. Біз бар штангаларды үлкейтіп қарап шыққан кезде, хромның қалыңдығы аз және өңделмегені анық болды. Ever Power ауыстыратын цилиндрлері қазір Лондондағы паркімізде 22 ай бойы бірде-бір тығыздағыш мәселесіз жұмыс істеп келеді. Хром сапасы айтарлықтай ерекшеленеді - ашық, қатты және біздің шеберхана тобымыз орнату алдында көзбен тексере алатын тұрақты өңделеді».
 Kazakh
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French
 Greek