
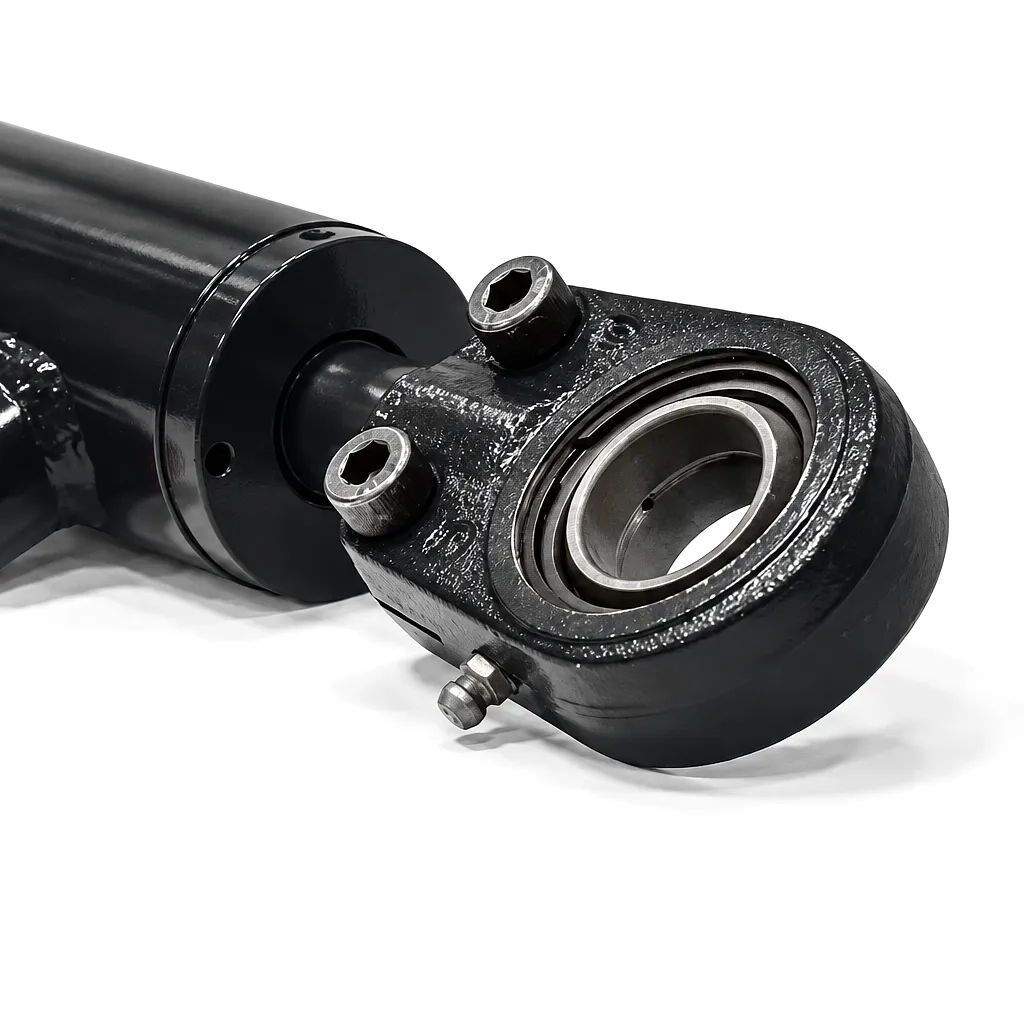
 Hydraulic cylinders are the silent workhorses of heavy industry. Whether they are lifting a steel plate in a Sheffield fabrication shop, controlling the boom arm of a crane on a Birmingham construction site, or powering the press in a Coventry automotive plant, these components are expected to perform reliably under relentless pressure. Yet one question comes up time and again on the plant floor: how long should a hydraulic cylinder actually last? The answer is rarely a simple number. Service life is shaped by a web of interacting variables — design quality, operating conditions, maintenance culture, fluid cleanliness, and the precision with which the cylinder was manufactured in the first place. Understanding those variables is the first step toward getting the most out of every unit you install.
How Hydraulic Cylinders Work — And Why It Matters for Longevity
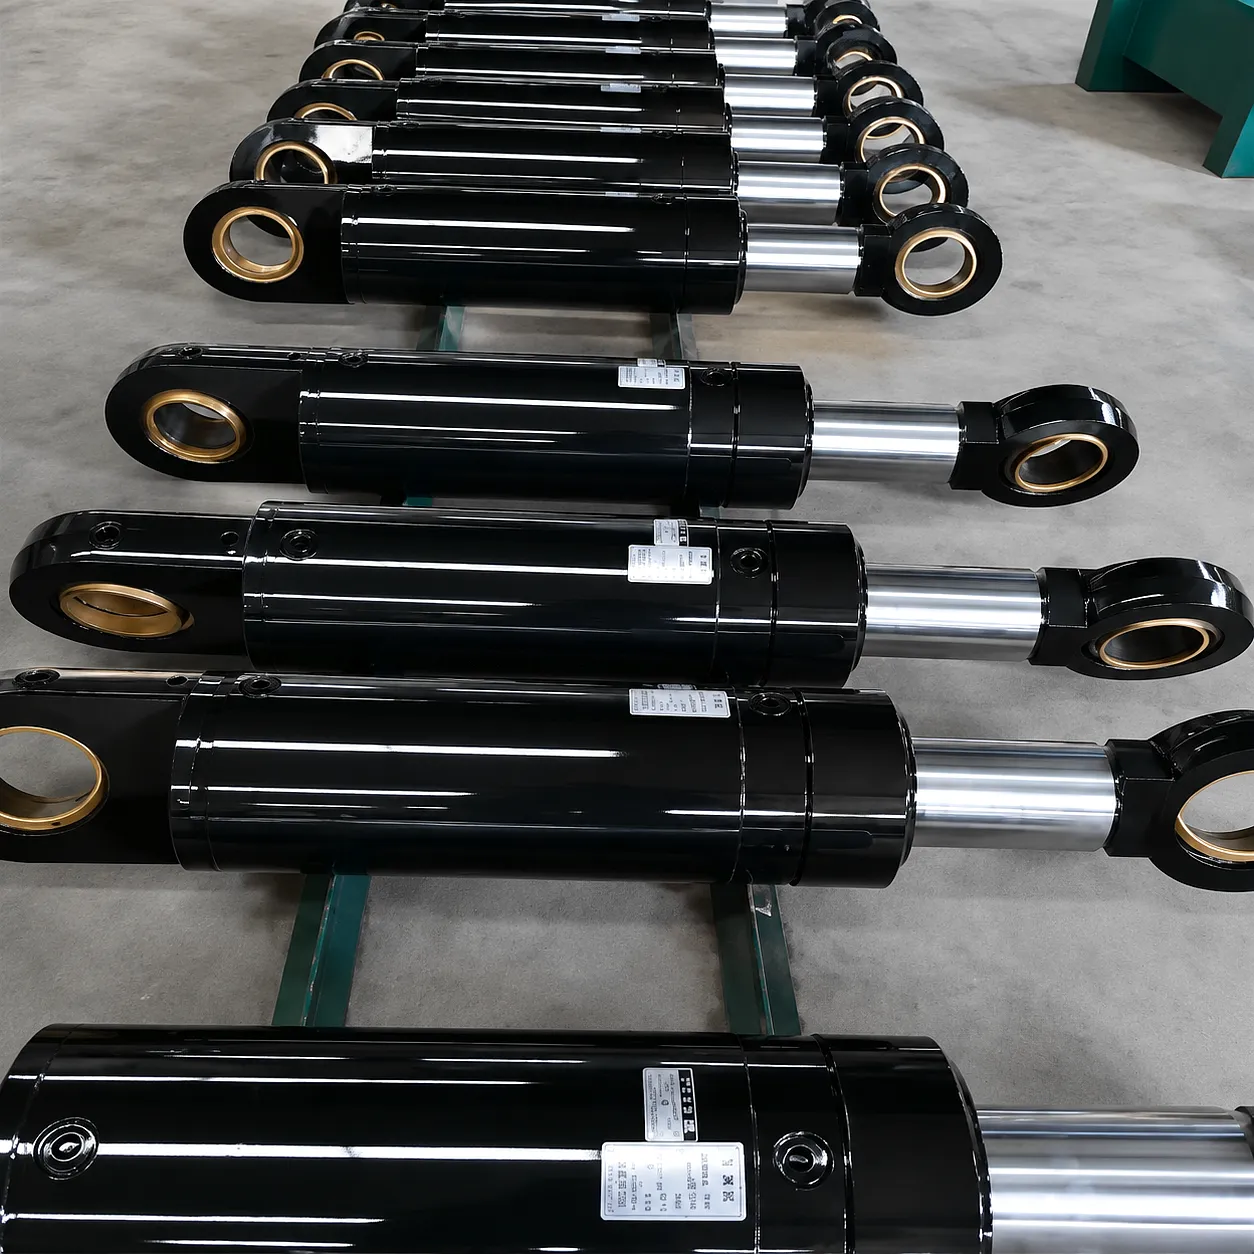 A hydraulic cylinder converts pressurised fluid energy into controlled linear mechanical force. Hydraulic oil — delivered by a pump at pressures typically ranging from 200 bar to 350 bar in industrial settings — enters the cylinder barrel through a port, acting against the face of a piston. The pressure differential across the piston produces a force measured by the formula F = P × A, where P is operating pressure in pascals and A is the piston cross-sectional area in square metres. The rod then extends or retracts, transmitting that force to the load attached at the clevis or flange mounting point.
What makes this relevant to service life is the nature of the internal environment. Every single stroke cycles the dynamic seals, generates heat through fluid shear, and subjects the barrel bore to micro-abrasive contact from the piston rings. If the fluid carries particulate contamination above ISO cleanliness class 16/14/11, abrasive wear on these surfaces accelerates dramatically. If the operating temperature routinely exceeds 80°C, seal elastomers degrade at an accelerated rate. The working principle itself contains the seeds of wear — and understanding exactly where those seeds germinate gives engineers the knowledge to slow the process considerably.
Six Factors That Directly Determine How Long a Hydraulic Cylinder Lasts
Fluid Cleanliness
Contaminated hydraulic fluid is the single most destructive force in any hydraulic circuit. Particles as small as 10 to 15 microns — invisible to the naked eye — act as grinding media between the piston rod and seal lip, scoring the chrome surface and accelerating leakage. Industry data consistently shows that over 70% of hydraulic component failures can be traced to fluid contamination. Maintaining oil cleanliness at ISO 4406 class 15/13/10 or better can extend cylinder seal life by a factor of three or more compared to unfiltered systems. For UK operations running multi-shift patterns, sampling the hydraulic oil every 500 operating hours and using offline filtration loops is a practical baseline that pays back many times over in avoided downtime costs.
Operating Temperature
Hydraulic seals are designed to perform within a defined temperature band. Standard nitrile (NBR) seals work reliably from -30°C to +100°C, but performance degrades noticeably above 80°C. Polyurethane seals, commonly used in high-cycle industrial presses, begin to harden and crack when repeatedly exposed to temperatures above 90°C. In foundry applications around Stoke-on-Trent and Birmingham, where cylinders operate near heat-intensive processes, specifying Viton (FKM) seals rated to 200°C is a straightforward upgrade that dramatically extends mean time between seal replacements. Equally important is monitoring system oil temperature: every 10°C rise above 60°C halves the oxidation life of mineral hydraulic oil, compounding the wear problem through fluid degradation and varnish formation inside the barrel.
Load and Pressure Cycling
A cylinder’s rated working pressure is not the ceiling at which damage begins — it is the point at which fatigue accumulates measurably. Every pressure spike above the design threshold contributes to fatigue crack initiation in the barrel wall, end cap welds, and piston rod threads. In applications with rapid reversals — such as a hydraulic press cycling 30 times per minute — the cumulative stress cycles can exceed 100 million over a five-year production run. Pressure spikes caused by load shock (common in demolition equipment operating across the Midlands and North West England) should always be managed with inline pressure relief valves set at no more than 110% of system working pressure. Correct specification of cylinder bore diameter and stroke length to match the actual load requirement — rather than over-pressuring an undersized unit — is the most cost-effective engineering decision a plant manager can make at the procurement stage.
Rod Surface Finish and Coating
The piston rod is the most exposed moving component in a hydraulic cylinder. Hard chrome plating — typically applied at 20 to 25 microns depth to achieve a surface hardness of 800–1000 HV — has been the standard finish for decades. However, in corrosive marine environments such as those found along the UK coastline from Hull to Portsmouth, or in chemical processing facilities in Teesside, standard chrome can show pitting within 18 months. Nickel-chrome composite coatings, or increasingly popular ceramic spray coatings applied by HVOF (High Velocity Oxy-Fuel) thermal spray, extend the corrosion-resistant service life of the rod by a factor of two to three compared to standard chrome, while also improving seal compatibility due to their smoother surface finish at Ra 0.1 to 0.2 microns.
Mounting Alignment
Side loading is one of the most underappreciated causes of premature hydraulic cylinder failure. When the line of force transmitted through the piston rod is not coaxial with the cylinder bore — even by as little as 1 to 2 degrees — the radial load on the rod seal, front bearing bush, and barrel bore increases exponentially with stroke length. In a 1500 mm stroke cylinder, a 2-degree misalignment at the pin mounting creates a side force at mid-stroke that can exceed 15% of the axial load, effectively reducing the design service life of the front gland seals by half. Proper installation using aligned mounting brackets, spherical rod eye bearings where angular movement is unavoidable, and torque-checked fasteners according to the manufacturer’s service schedule is a straightforward intervention that production engineers in the Sheffield fabrication sector have found consistently extends maintenance intervals beyond original design targets.
Maintenance Discipline
No hydraulic cylinder — regardless of manufacturing quality — will achieve its designed service life without a structured maintenance regime. The most impactful routine tasks are also the simplest: checking the rod wiper seal for ingress of grit and water, monitoring for weeping around the gland nut that signals early seal wear, inspecting the rod surface for scoring or corrosion spots, and verifying that the breather on the hydraulic reservoir is clean and serviceable. UK manufacturing sites operating under Health and Safety Executive (HSE) guidance are increasingly adopting condition-based monitoring approaches using ultrasonic leak detectors and thermal imaging cameras to identify deteriorating cylinders before they reach catastrophic failure. This proactive culture, now well established in automotive Tier 1 suppliers across the Midlands, is perhaps the single most powerful lever available to maintenance managers seeking to extend hydraulic cylinder service life without capital investment.
Core Materials That Determine Structural Life
The material selection for each component of a hydraulic cylinder is a direct expression of how the engineer has balanced strength, machinability, corrosion resistance, and cost against the intended service environment. There is no universally optimal material set — the correct specification depends entirely on the application.
Cylinder barrels are most commonly produced from E355 (formerly ST52-3) seamless cold-drawn steel tube, which offers a yield strength of 355 MPa and good honing characteristics for achieving the Ra 0.3 to 0.6 micron bore finish required for optimal piston ring and seal performance. For applications demanding higher burst pressure — such as deep-sea ROV actuators or high-tonnage press cylinders — chrome-moly alloy steel (42CrMo4) is preferred, offering yield strengths above 900 MPa in the heat-treated condition.
Piston rods are typically manufactured from case-hardened and ground carbon steel or 42CrMo4 alloy steel, hard chrome plated, then precision ground to h8 or f7 tolerance for correct seal fit. In aggressive environments, duplex stainless steel (1.4462) rods offer substantially better corrosion resistance without the risk of hydrogen embrittlement associated with high-strength plated steel. Offshore and marine applications along the UK’s North Sea coastline increasingly specify Inconel or titanium sleeve inserts at high-wear locations.
Seals form the functional heart of the cylinder. The correct seal compound — NBR for general-purpose oil service, HNBR for elevated temperature and ozone resistance, Viton (FKM) for extreme heat or phosphate ester fluids, and PTFE composites for low-friction, high-speed applications — should be selected based on the fluid chemistry, temperature range, and duty cycle rather than cost alone. A seal upgrade that costs £40 per rebuild can save thousands in unplanned production stoppages at a manufacturing facility running continuous shifts.
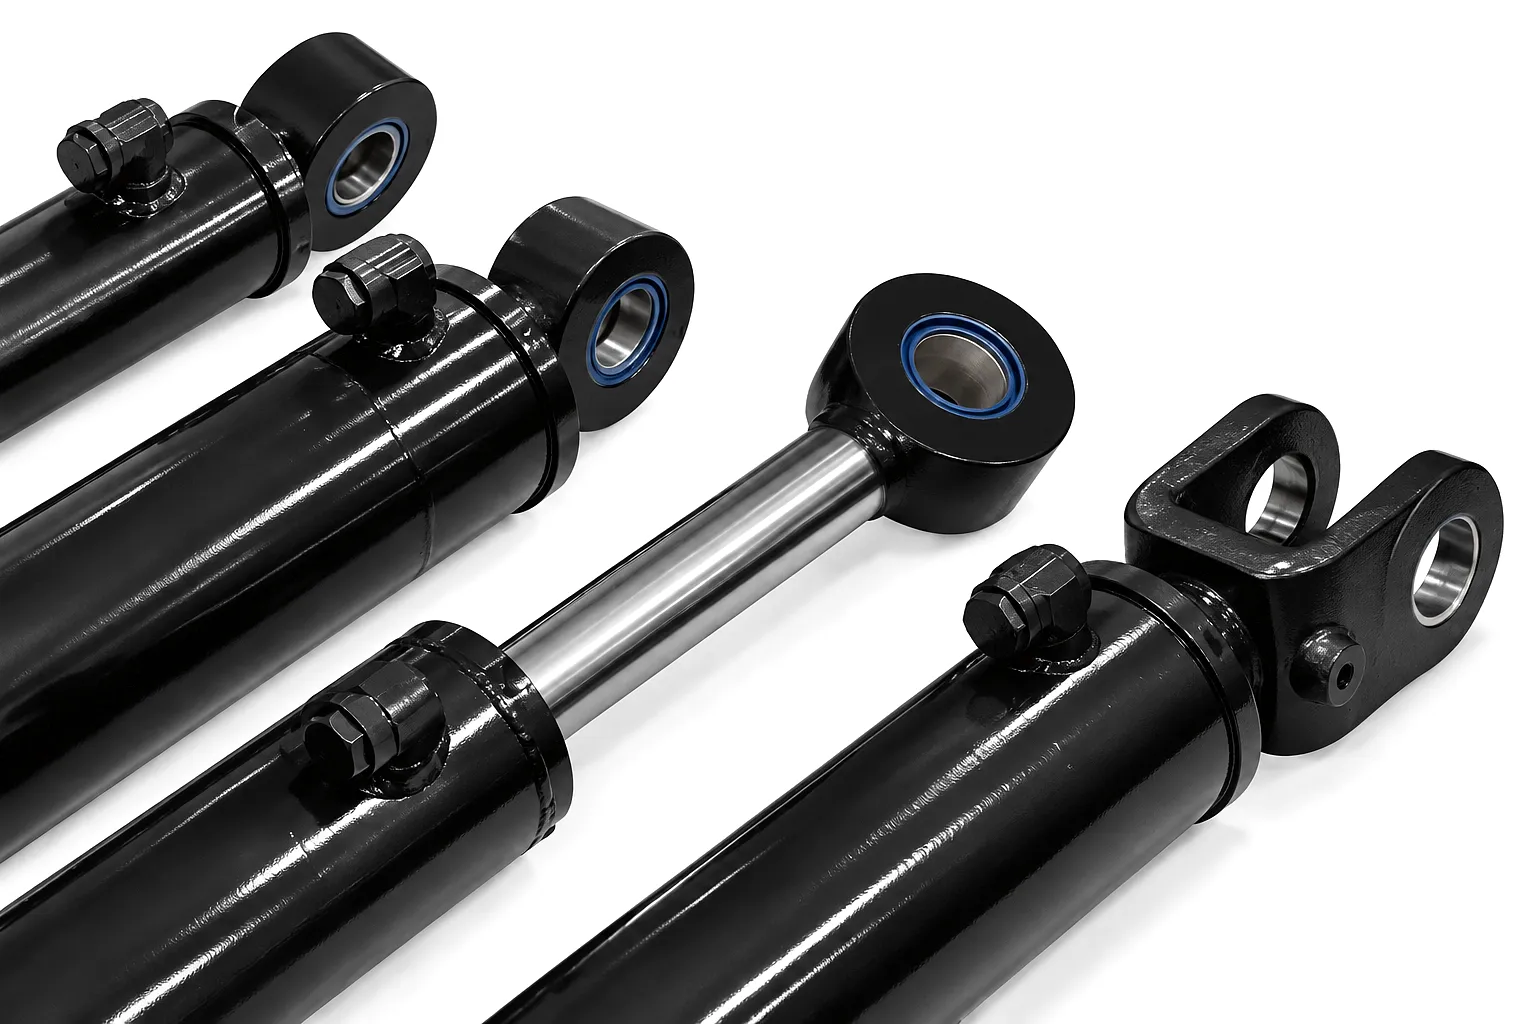
Material Quick Reference
Barrel
E355 / 42CrMo4 seamless tube
Rod
Hard chrome on 42CrMo4 / Duplex SS
Seals
NBR / HNBR / FKM / PTFE composite
End Caps
Ductile iron / EN8 / Stainless 316
Technical Performance Parameters — Industrial Hydraulic Cylinders
The table below represents typical performance parameters for industrial-grade welded and tie-rod hydraulic cylinders produced by Ever Power. Custom specifications are available across all parameters to meet specific UK project requirements.
| Parameter | Standard Range | High-Performance Option | Notes |
|---|---|---|---|
| Bore Diameter | 40 – 500 mm | Up to 1,000 mm (custom) | Honed to Ra 0.3–0.6 µm |
| Rod Diameter | 25 – 320 mm | Up to 600 mm (custom) | Hard chrome / duplex SS options |
| Tekanan Kerja | Up to 250 bar | Up to 500 bar | Test pressure 1.5x working |
| Panjang Strok | 50 – 6,000 mm | Up to 12,000 mm (telescopic) | Intermediate supports for long stroke |
| Operating Temperature | -20°C to +80°C | -50°C to +200°C (FKM seals) | Seal compound determines range |
| Rod Surface Hardness | 800 – 1,000 HV (hard chrome) | 1,200+ HV (HVOF ceramic) | For abrasive or marine service |
| Cushion Type | Fixed or adjustable needle | Dual adjustable with bypass check | Reduces end-of-stroke shock loading |
| Mounting Options | Clevis, foot, flange, trunnion | Full custom mounting geometry | To ISO 6020/6022 standards |
| Design Service Life | 10,000 – 20,000 hours | 30,000+ hours (premium build) | Subject to maintenance regime |
Engineering Advantages That Extend Cylinder Service Life
✓
Precision Bore Honing
A correctly honed barrel bore achieves the crosshatch pattern required for oil film retention and controlled piston ring seating. This reduces piston-to-barrel micro-abrasion during the critical break-in period — typically the first 100 to 200 operating hours — and sets the baseline for all subsequent seal wear rates throughout the cylinder’s operational life.
✓
Integrated Cushioning at End of Stroke
Hydraulic shock at end of stroke is a primary driver of structural fatigue in cylinder end caps, piston assemblies, and attachment pins. Adjustable deceleration cushions — built directly into the head and cap — progressively restrict oil flow as the piston approaches the end of travel, decelerating the load smoothly and reducing peak impact forces by up to 80% compared to uncushioned designs running at equivalent speeds.
✓
Contamination-Exclusion Wiper Design
The rod wiper seal is the frontline defence against external contamination entering the hydraulic circuit through the gland. Heavy-duty scraper wipers with embedded polyurethane lips and optional integral metal scrapers can be specified for environments where concrete dust, swarf, coal particulate, or airborne grit is present — exactly the conditions found in quarrying operations across the Pennines, tunnelling projects around London, and aggregate processing sites in South Wales.
✓
Full Hydrostatic Pressure Testing
Every hydraulic cylinder dispatched from the Ever Power manufacturing facility undergoes hydrostatic pressure testing at 1.5 times the rated working pressure before despatch. This protocol, compliant with ISO 10100 and BS EN 4413 guidance for UK installations, confirms barrel integrity, end cap weld quality, and initial seal performance under load — eliminating the risk of early-life structural failure and giving plant engineers and procurement managers in the UK a verified baseline for their maintenance scheduling from day one of operation.
Industrial Application Scenarios Across UK Heavy Industry
Steel Processing — Sheffield & Rotherham
Steel rolling mill hydraulic cylinders operate in one of the most demanding environments imaginable — high temperature, scale contamination, vibration, and very high cycle rates. Cylinders controlling roll gap adjustment on hot strip mills in the Sheffield and Rotherham steel corridor must maintain positioning accuracy to within 0.1 mm under loads exceeding 500 tonnes. High-pressure, short-stroke servo cylinders with integrated linear position transducers and dual cushions are the standard specification for these applications. Mean time between overhauls in well-maintained steel mill applications typically runs to 8,000 to 12,000 hours.
Automotive Manufacturing — Midlands Corridor
Body pressing and stamping lines in automotive plants across the Midlands — from Solihull to Coventry — rely on large-bore, high-speed hydraulic cylinders to deliver the closing force required for deep-drawn body panels. In these applications, cycle rates can reach 20 to 30 strokes per minute, generating cumulative seal cycles that make seal quality the limiting factor in overall cylinder life. Specified correctly with polyurethane piston seals, phenolic resin guide rings, and filtered hydraulic circuits, these cylinders routinely achieve 15,000 to 20,000 hours between major rebuilds.
Marine & Offshore — Aberdeen, Hull & Portsmouth
Offshore support vessels, dock gate controls, and ship lifting equipment along the UK coastline — from the oil service ports of Aberdeen to the commercial docks at Hull and the naval facilities at Portsmouth — expose hydraulic cylinders to seawater spray, salt-laden air, and cyclic bending loads from vessel motion. These environments demand duplex stainless steel rods, full stainless or hot-dip galvanised external hardware, and Viton seals as a minimum specification. Properly specified marine-grade hydraulic cylinders from Ever Power have achieved 12,000+ hours of service on North Sea offshore support vessels operating 24 hours per day, 365 days a year.
Construction Equipment — Nationwide UK Infrastructure
Excavators, mobile cranes, telescopic handlers, and concrete pump booms deployed on UK infrastructure projects — from HS2 civil works to urban regeneration schemes in Manchester and Leeds — subject their hydraulic cylinders to the full spectrum of demanding conditions: soil abrasion on the rod, shock loads from ground engagement, wide temperature swings between seasons, and the contamination risks associated with working in earthen environments. Boom cylinders and arm cylinders on these machines are a critical wear item. Correct specification of bore size, stroke, and sealing system against the machine’s hydraulic circuit parameters determines whether a cylinder lasts one season or five.
Product Range
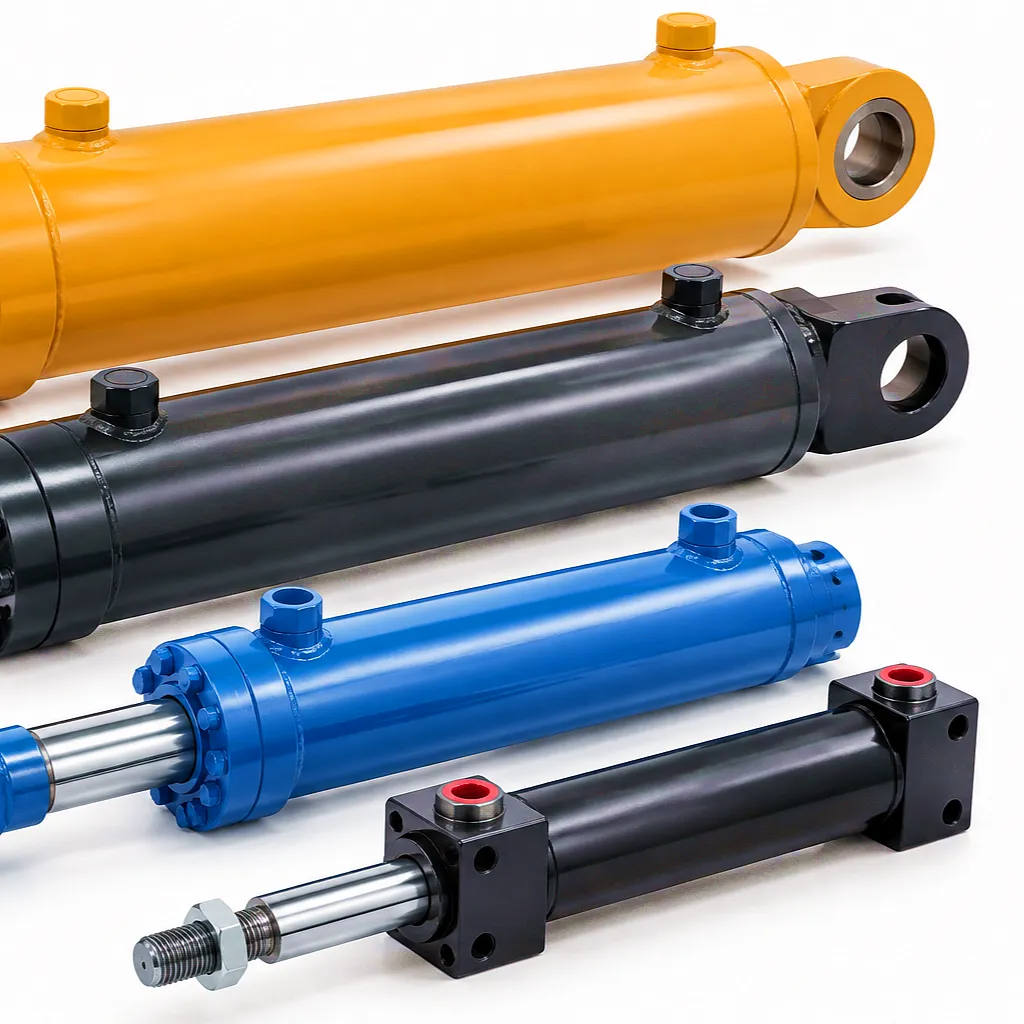
Ever Power Hydraulic Cylinder Collection
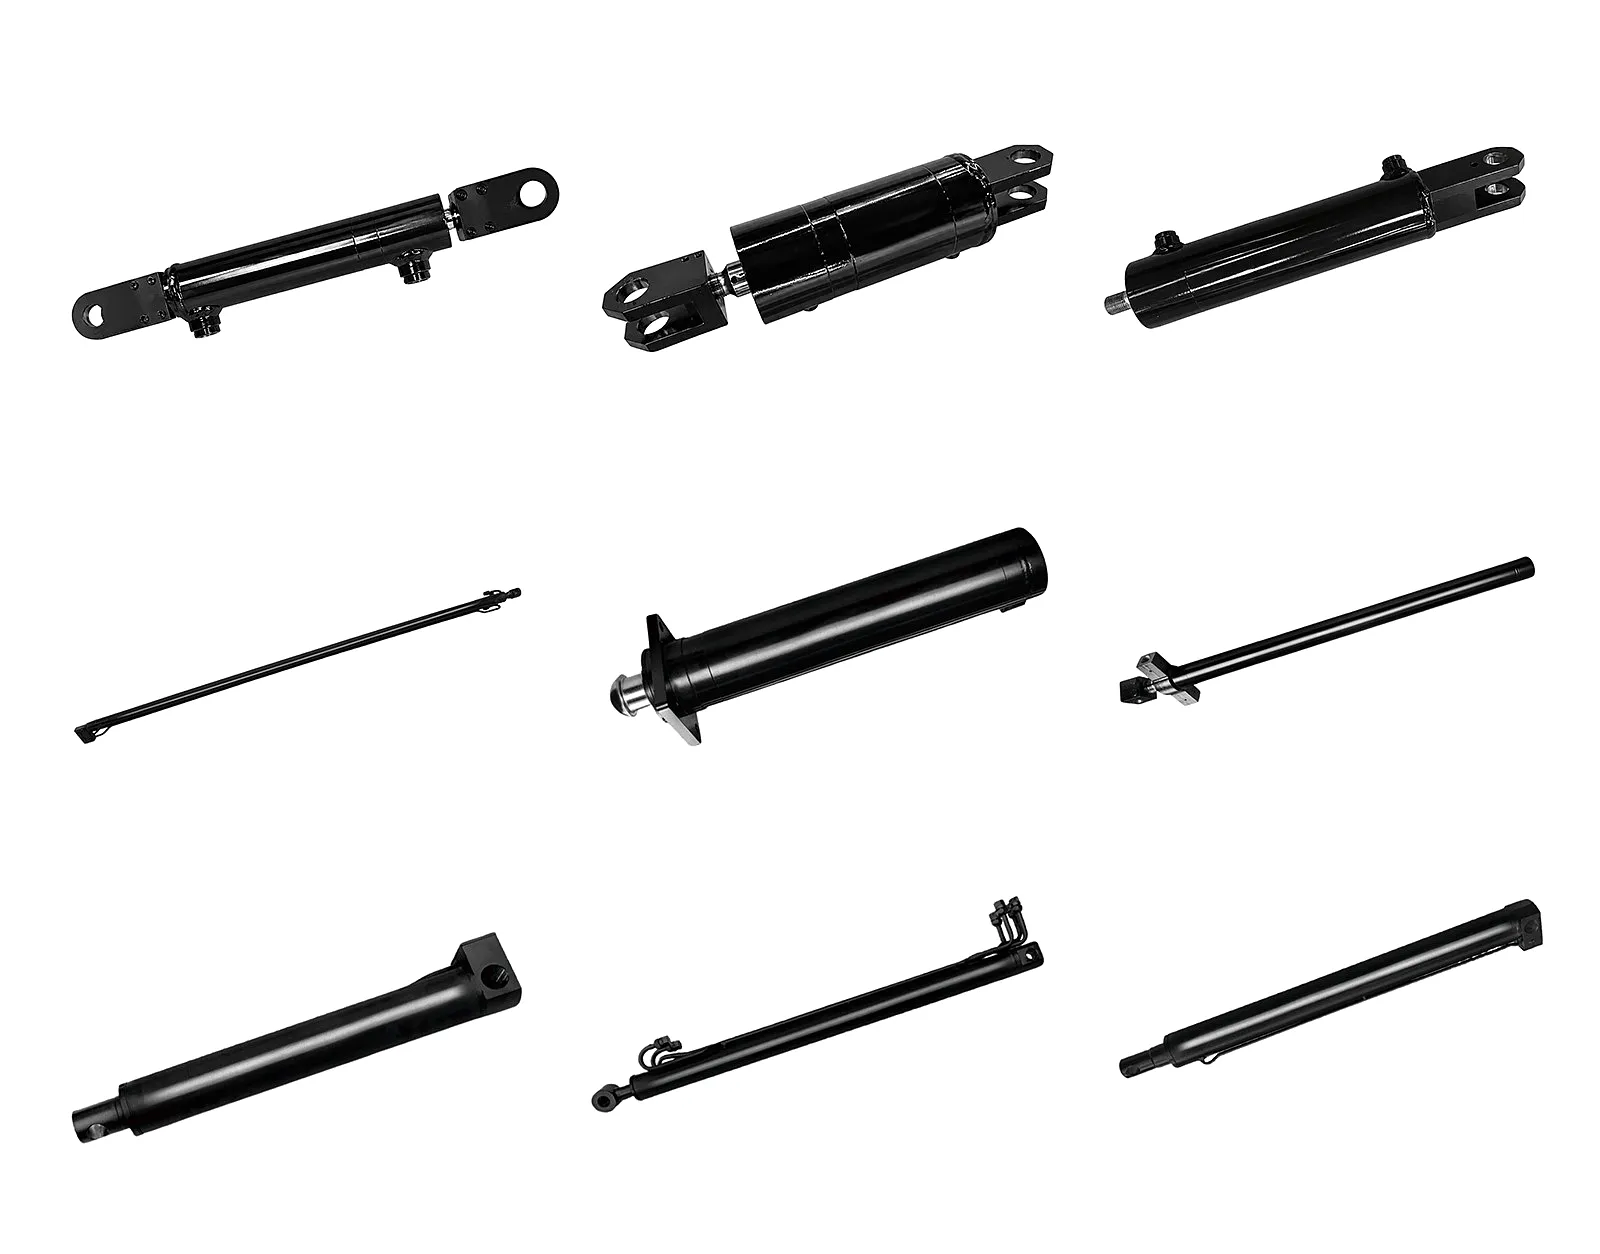
From compact tie-rod cylinders to large-bore custom welded units — engineered to BS EN and ISO standards for UK industrial service.
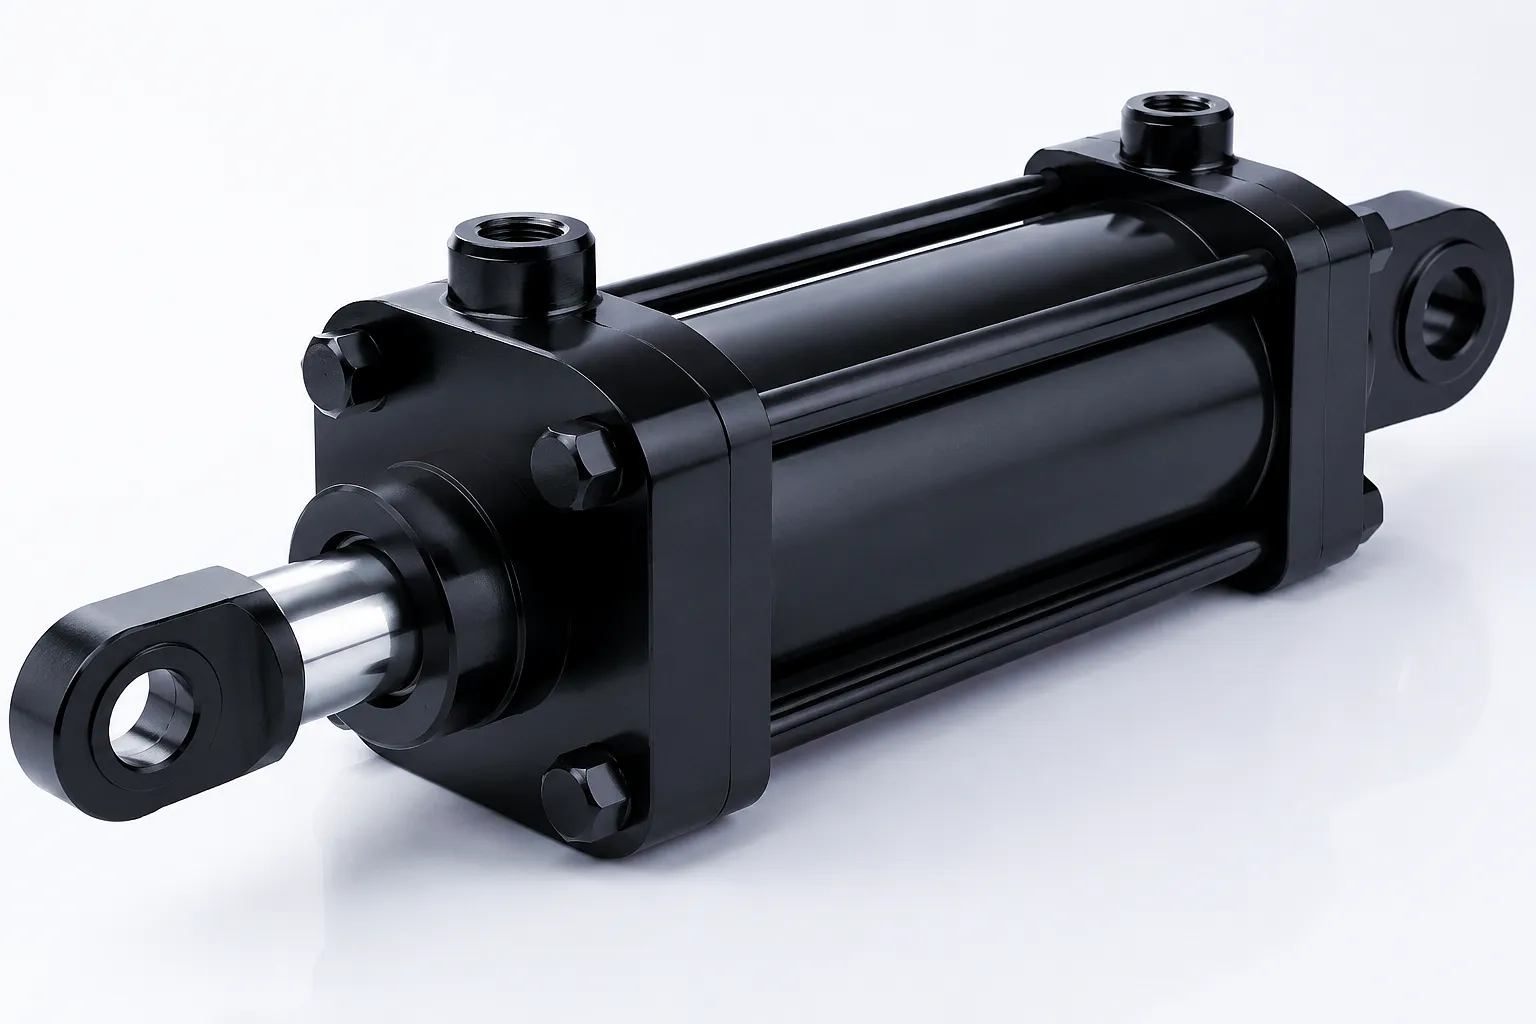
Customer Success Story
Sheffield Steel Fabricator Extends Cylinder Life from 3 Years to 7 Years
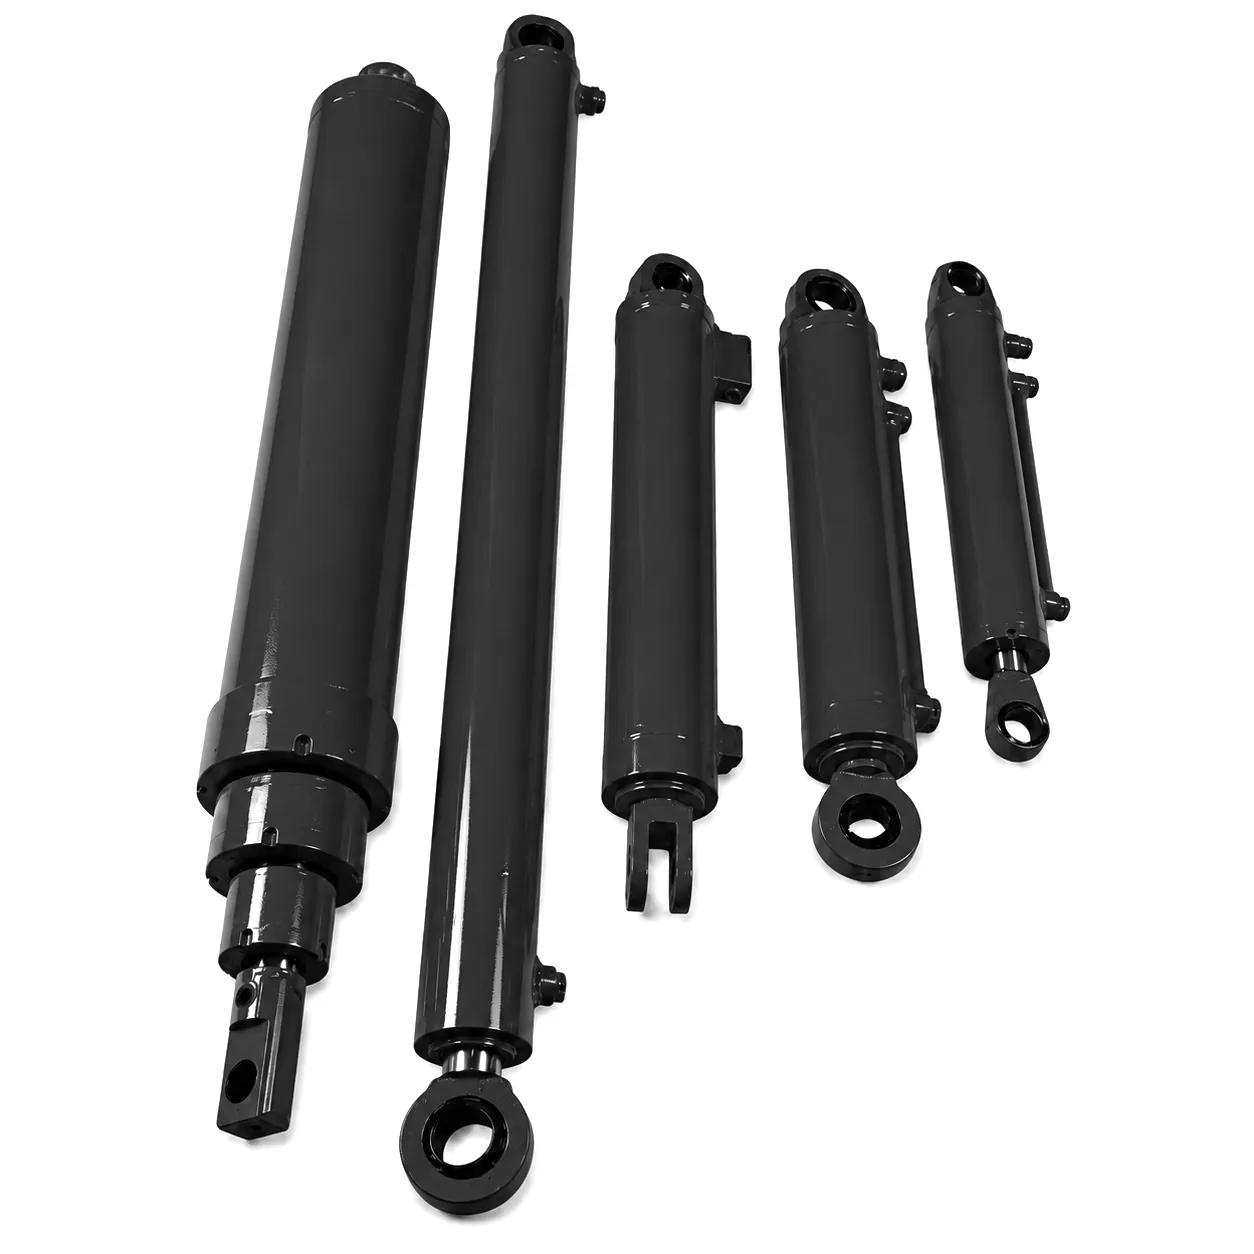 HM Steel Fabrications Ltd, a structural steel contractor based in Sheffield’s Lower Don Valley, operates a fleet of plate bending rollers, press brakes, and hydraulic shears on a two-shift production cycle — some 16 operating hours per day, five to six days per week. Their legacy silinder hidraulik were reaching end of useful life after approximately 14,000 operating hours — roughly three years at their run rate — with recurring seal failures being the dominant maintenance issue. The root causes identified during a joint technical audit with Ever Power’s applications engineering team were three-fold: excessive fluid operating temperature (measured at 88°C during peak production periods), standard NBR seals operating beyond their thermal design range, and a hydraulic return line filter with a 25-micron rating that was admitting contamination particles large enough to score the rod surface.
Ever Power supplied a batch of replacement hydraulic cylinders specified with HNBR dynamic seals rated to 120°C, hard chrome rods ground to Ra 0.15 microns for improved seal compatibility, and stainless steel wiper assemblies with integral metal scrapers. Simultaneously, the team recommended upgrading the return line filter to an absolute 10-micron element and fitting an oil cooler to bring the operating temperature below 70°C. The combined intervention — new cylinders plus system upgrades — was implemented during a planned maintenance shutdown in February 2024.
By mid-2026, the new Ever Power cylinders had accumulated over 17,000 operating hours without a single seal replacement. The maintenance team projects they will comfortably reach 30,000 hours — the equivalent of seven years at their production intensity — representing a saving of approximately £28,000 in replacement parts and labour costs compared to the previous three-year replacement cycle. Plant Director Mike Harrison noted that the project had delivered a return on investment within the first 14 months of operation.
What UK Customers Say About Ever Power Hydraulic Cylinders
“We’ve been running Ever Power cylinders on our press brake lines for over two years now and the improvement in seal life compared to our previous supplier is genuinely remarkable. The HNBR seal upgrade they recommended has made a night-and-day difference. We’ve gone from budgeting for seal kits every eight months to not needing them at all within our current planning horizon.”
— James Thornton, Maintenance Manager, HM Steel Fabrications Ltd, Sheffield
“When we needed replacement cylinders for a tunnelling project in Birmingham with a six-week delivery window, most suppliers couldn’t come close to that timeline. Ever Power had the custom units with non-standard port positions and duplex stainless rods on-site in five weeks, complete with the 3.1 material certificates our project specification demanded. Impressive logistics from a supplier working to this level of technical specification.”
— Sarah Bhattacharya, Procurement Director, Nexciv Civil Engineering Ltd, Birmingham
“We operate offshore support vessels out of Aberdeen and the salt environment destroys standard cylinders in under two years. Ever Power’s duplex stainless rod specification with Viton seals has been running on our deck crane cylinders for 26 months with zero corrosion issues. The technical data sheet they supplied with each unit is genuinely detailed — exactly what you need when you’re working to DNV survey requirements. These are a proper step up from what we were buying before.”
— Calum Fraser, Fleet Technical Superintendent, Caledonian Offshore Services, Aberdeen
Voice-Search Ready FAQ
Soalan Lazim — Jangka Hayat Perkhidmatan & Perolehan Silinder Hidraulik di UK
Berapa lama silinder hidraulik biasanya tahan dalam persekitaran pembuatan berat UK dengan operasi dua syif berterusan?
Dalam persekitaran pembuatan dua syif yang diselenggara dengan baik — kira-kira 16 jam operasi sehari — silinder hidraulik perindustrian yang ditentukan dengan betul daripada pengeluar berkualiti seperti Ever Power sepatutnya memberikan antara 10,000 dan 20,000 jam perkhidmatan sebelum pembinaan semula yang besar. Pada dua syif sehari, lima hari seminggu, itu bermakna kira-kira 4 hingga 8 tahun hayat pengeluaran. Pembolehubah kritikal ialah kebersihan bendalir, suhu operasi dan sama ada silinder telah disaizkan dengan betul untuk beban sebenar pada mulanya.
Apakah yang menyebabkan pengedap silinder hidraulik gagal lebih awal pada peralatan pemprosesan keluli di Sheffield dan Rotherham?
Tiga punca utama kegagalan pengedap awal dalam sektor pemprosesan keluli Sheffield dan Rotherham ialah suhu minyak yang tinggi (melebihi 80°C), pencemaran zarah daripada kerak dan serpihan yang masuk melalui pengelap rod, dan penggunaan pengedap NBR dalam aplikasi yang sebenarnya memerlukan sebatian HNBR atau Viton. Menangani ketiga-tiganya melalui gabungan pemilihan pengedap yang betul, spesifikasi pengelap yang betul, dan penaiktarafan penyejukan dan penapisan minyak khusus biasanya memanjangkan hayat pengedap sebanyak dua hingga tiga kali ganda.
Di manakah saya boleh mendapatkan harga atau sebut harga untuk silinder hidraulik tersuai yang dibekalkan kepada projek UK dengan pensijilan bahan mengikut BS EN 10204 3.1?
Ever Power membekalkan silinder hidraulik tersuai dengan pensijilan kebolehkesanan bahan penuh mengikut BS EN 10204 3.1 dan 3.2 untuk projek UK yang memerlukan bukti dokumentari pematuhan bahan. Untuk mendapatkan sebut harga, emelkan spesifikasi teknikal — lubang, lejang, tekanan kerja, susunan pemasangan dan persekitaran pengedap — terus kepada [email protected]Jurutera aplikasi kami akan menyemak spesifikasi dan memberikan sebut harga rasmi, biasanya dalam tempoh 48 jam untuk konfigurasi standard dan 5 hari bekerja untuk unit yang sangat disesuaikan.
Bahan rod silinder hidraulik yang manakah berfungsi paling baik dalam persekitaran marin dan luar pesisir di sepanjang pantai UK berhampiran Aberdeen dan Hull?
Keluli tahan karat dupleks (gred 1.4462 atau setaraf) ialah bahan rod yang disyorkan untuk aplikasi marin dan luar pesisir di perairan UK, termasuk operasi yang berpangkalan di Aberdeen, Hull dan Portsmouth. Keluli tahan karat dupleks menawarkan rintangan kakisan kira-kira lima kali ganda lebih baik daripada krom keras standard pada keluli karbon sambil mengekalkan kekerasan permukaan yang mencukupi (biasanya 380 hingga 420 HV) untuk keserasian pengedap yang memuaskan apabila disiapkan pada tahap tanah Ra 0.2 mikron. Untuk zon percikan yang paling teruk atau aplikasi tenggelam sepenuhnya, sisipan lengan super-dupleks atau Inconel di zon larian pengedap memberikan perubahan langkah selanjutnya dalam hayat perkhidmatan.
Berapakah kos untuk menggantikan pengedap silinder hidraulik pada brek tekan di kilang automotif Birmingham atau Coventry, dan adakah ia berbaloi untuk dibina semula daripada membeli unit baharu?
Pembinaan semula pengedap penuh pada silinder brek tekan berlubang sederhana di kilang automotif Midlands biasanya berharga antara £180 dan £800 untuk alat ganti, bergantung pada saiz lubang, sebatian pengedap dan sama ada rod memerlukan kemasan semula. Buruh menambah lagi £150 hingga £400 bergantung pada kadar akses dan tapak. Jika lubang laras dan permukaan rod berada dalam keadaan baik, pembinaan semula pengedap hampir selalu lebih menjimatkan kos daripada membeli silinder gantian. Walau bagaimanapun, jika rod berlubang, lubang berjeruji, atau kimpalan penutup hujung menunjukkan keretakan, silinder baharu daripada Ever Power — dibekalkan dengan harga yang kompetitif dan penghantaran 4 hingga 8 minggu — adalah pelaburan jangka panjang yang lebih dipercayai. Hubungi [email protected] untuk penetapan harga unit gantian.
Bilakah pasukan penyelenggaraan loji UK perlu menggantikan silinder hidraulik dan bukannya terus membaikinya, dan apakah tanda-tanda amaran yang menunjukkan tamatnya hayat struktur yang berguna?
Petunjuk utama bahawa silinder hidraulik telah mencapai akhir hayatnya yang boleh dibaiki secara ekonomi termasuk: kesan penorehan atau lubang yang kelihatan pada permukaan rod omboh yang lebih dalam daripada 0.15 mm yang tidak boleh ditanggalkan dengan menggilap tanpa mengurangkan saiz rod di bawah toleransi pengedap; haus lubang laras melebihi 0.3 mm secara jejari, mengakibatkan kebocoran pengedap omboh yang tidak boleh dibetulkan dengan penggantian pengedap; keretakan atau keliangan pada kimpalan penutup hujung yang dikenal pasti melalui pemeriksaan penembusan ultrasonik atau pewarna; dan sejarah penyelenggaraan yang menunjukkan selang penggantian pengedap yang semakin pendek dengan setiap pembinaan semula berturut-turut — isyarat jelas bahawa punca utamanya adalah kemerosotan struktur dan bukannya peristiwa kegagalan pengedap tertentu. Apabila mana-mana keadaan ini wujud, menggantikan silinder adalah keputusan yang lebih selamat dan akhirnya lebih menjimatkan.
HIDRAULIK INDUSTRI EVER POWER
Kejuruteraan Ketepatan untuk Industri British
suntingan oleh gzl
 Malay
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 French
 Greek