
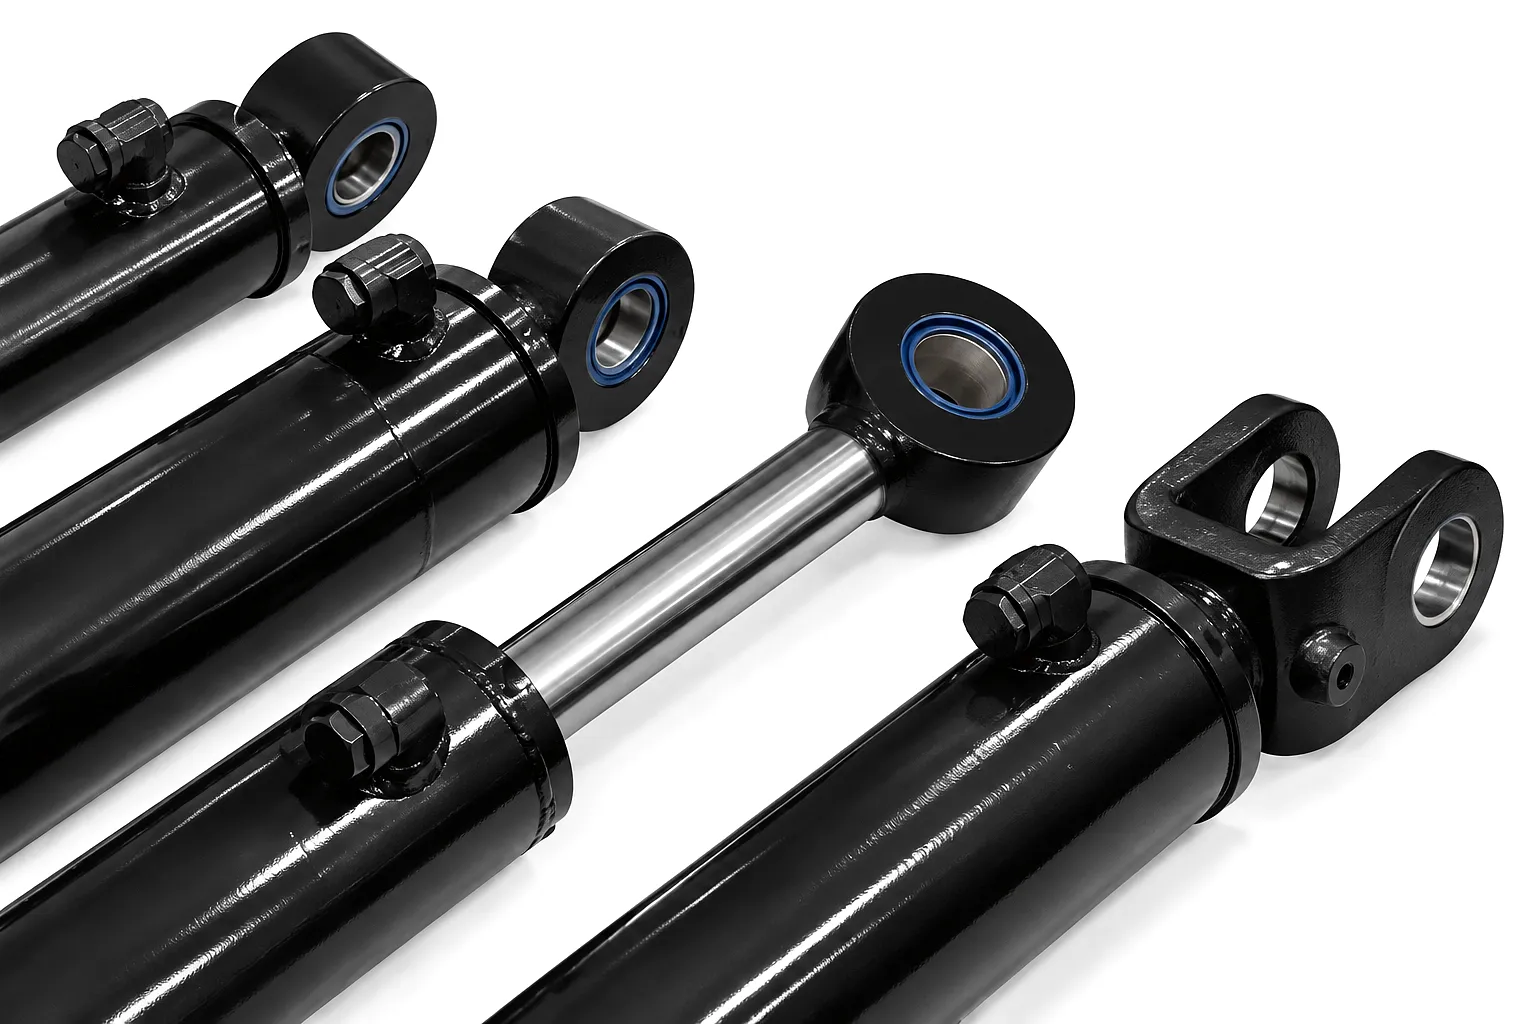
 A leaking boom cylinder is rarely a minor inconvenience. Whether it is a telescopic arm on a crane operating out of Sheffield’s steel fabrication yards, a bucket cylinder on an excavator working a Birmingham infrastructure project, or a luffing cylinder on a mobile elevated work platform in Glasgow, hydraulic seal failure translates directly into machine downtime, lost productivity, and — if ignored — catastrophic component damage. Understanding exactly when an in-house maintenance team can safely address seal replacement, and when the job demands a specialist rebuild, is one of the most commercially important decisions a plant manager can make. Get it wrong in either direction and the consequences are steep: unnecessary contractor costs on one hand, or voided warranties, component scrappage, and injury risk on the other.
How Boom Cylinder Seals Function and Why They Fail
A boom cylinder seal package typically comprises a rod seal, wiper seal, piston seal, buffer seal, and guide rings. Together they create a pressure-tight environment that keeps hydraulic oil where it belongs — driving the piston — while excluding contaminants from the rod cavity. In a double-acting cylinder, the piston seals manage pressurised oil on both sides of the piston, while the rod seal prevents external leakage along the cylinder rod. Each element is engineered to specific material grades and dimensional tolerances. In high-cycle crane boom cylinders operating around the ports of Felixstowe or the offshore supply yards at Aberdeen, seal integrity determines whether a lift cycle completes safely or produces an incident.
Seal degradation rarely happens overnight. The most common causes in UK working environments include rod surface scoring from contaminated hydraulic oil, UV and ozone exposure on outdoor plant, thermal cycling on machines operating between cold Scottish winters and heated workshop environments, incompatible seal materials exposed to incorrect hydraulic fluid grades, and side-loading on cylinders subjected to off-axis forces. Hydraulic fluid that contains water — a particular concern in coastal regions and agricultural applications across the English Fenlands — accelerates elastomer swelling and reduces seal lip hardness, dramatically shortening service life. Identifying the precise failure mode before ordering replacements is essential; fitting a new seal onto a scored rod, for example, simply repeats the problem within weeks.
Operators should watch for a visible oil film along the rod surface (external leakage), a gradual loss of holding force under static load, cylinder drift under gravity with no commanded movement, sluggish extension or retraction response, and contaminated return-line filter debris. On boom cylinders specifically — those driving the primary arm extension of cranes, aerial work platforms, and reach stackers — any combination of these symptoms should trigger an immediate inspection protocol. The UK’s Health and Safety Executive has published guidance linking hydraulic seal failure to incidents involving uncontrolled load movement, making early detection a compliance obligation as much as a maintenance preference.
The Decision Framework: DIY Repair vs Specialist Rebuild
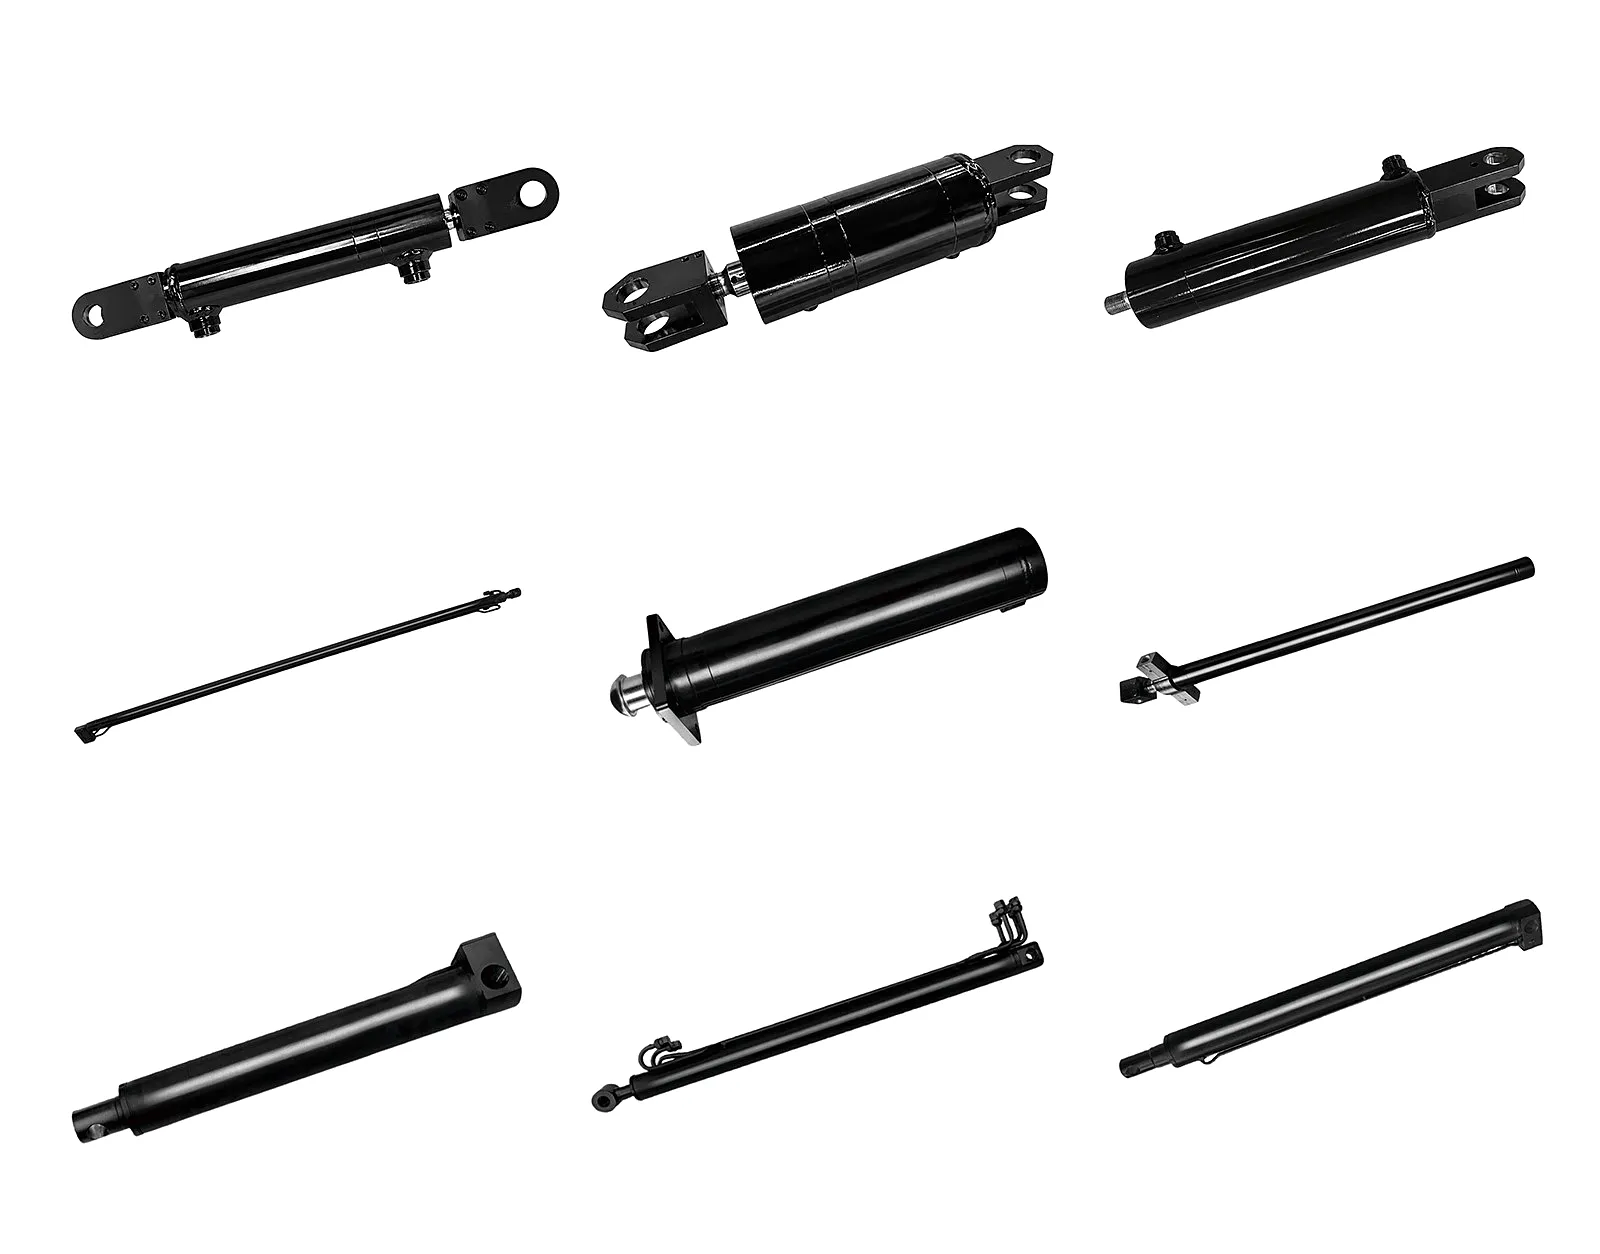
Deciding between in-house seal replacement and a specialist rebuild depends on a layered set of technical, operational, and regulatory factors. This framework walks through each one systematically so that UK maintenance managers can make a documented, defensible decision.
In-house seal replacement is genuinely viable when the following conditions are fully satisfied. The cylinder bore is undamaged — confirmed by visual inspection and, ideally, bore gauge measurement. The rod surface shows no scoring, pitting, or chrome delamination beyond superficial polish marks. The cylinder is a standard, single-stage design with no specialised internal geometry. The maintenance team holds documented training in hydraulic component dismantling, has access to a clean workshop environment (critical — contamination introduced during assembly is the leading cause of premature reseal failure), and possesses the manufacturer’s torque specifications for retaining nuts and gland threads.
Where these conditions apply, a straightforward external rod seal and wiper replacement — the most common single-point failure mode — can be completed safely with the correct OEM or premium aftermarket seal kit, a clean hydraulic press or pusher tool, and a calibrated torque wrench. Many UK plant hire companies operating fleets of mini-excavators and compact telehandlers manage this work entirely in-house, reducing their call-out costs significantly over a season.
Specialist intervention is non-negotiable in several scenarios. Any indication of rod scoring — even light surface marks — demands professional chroming or hard-chrome re-grinding before re-sealing; fitting seals over a damaged rod surface guarantees accelerated failure and potential oil injection injury risk. Telescopic boom cylinders used on all-terrain cranes and marine knuckle-boom applications involve multi-stage configurations with close-tolerance bearing lands that require precision measuring equipment and specialist assembly jigs far beyond standard workshop kit.
Cylinders operating at pressures above 350 bar — common in offshore crane applications from Aberdeen and Peterhead supply bases, and in heavy forging press equipment in Sheffield’s remaining steel works — carry inherently higher risk profiles that require hydraulic pressure testing to certified standards post-rebuild. Machines operating under LOLER (Lifting Operations and Lifting Equipment Regulations) or PSSR (Pressure Systems Safety Regulations) may require third-party inspection and certification of the repaired cylinder before the machine returns to service — work that only an accredited hydraulic specialist can support with the required documentation.
Several scenarios sit between clear DIY territory and mandatory specialist referral. A cylinder showing minor barrel wear but acceptable surface finish may be rebuildable in-house with an oversized piston seal, but this decision requires precise bore measurement with a calibrated internal micrometer. Cylinders with corroded or damaged gland threads often fall into this category — the repair is technically possible for a skilled engineer but carries disproportionate risk if thread engagement is insufficient after repair.
In these borderline situations, a partial inspection by a specialist — with full documentation — followed by in-house seal installation is often the most cost-effective path. UK hydraulic repair centres in the West Midlands and Yorkshire typically offer cylinder condition assessment as a standalone service, giving maintenance teams the data they need to make an informed decision without necessarily committing to a full contracted rebuild.
Seal Material Selection: The Core Decisions
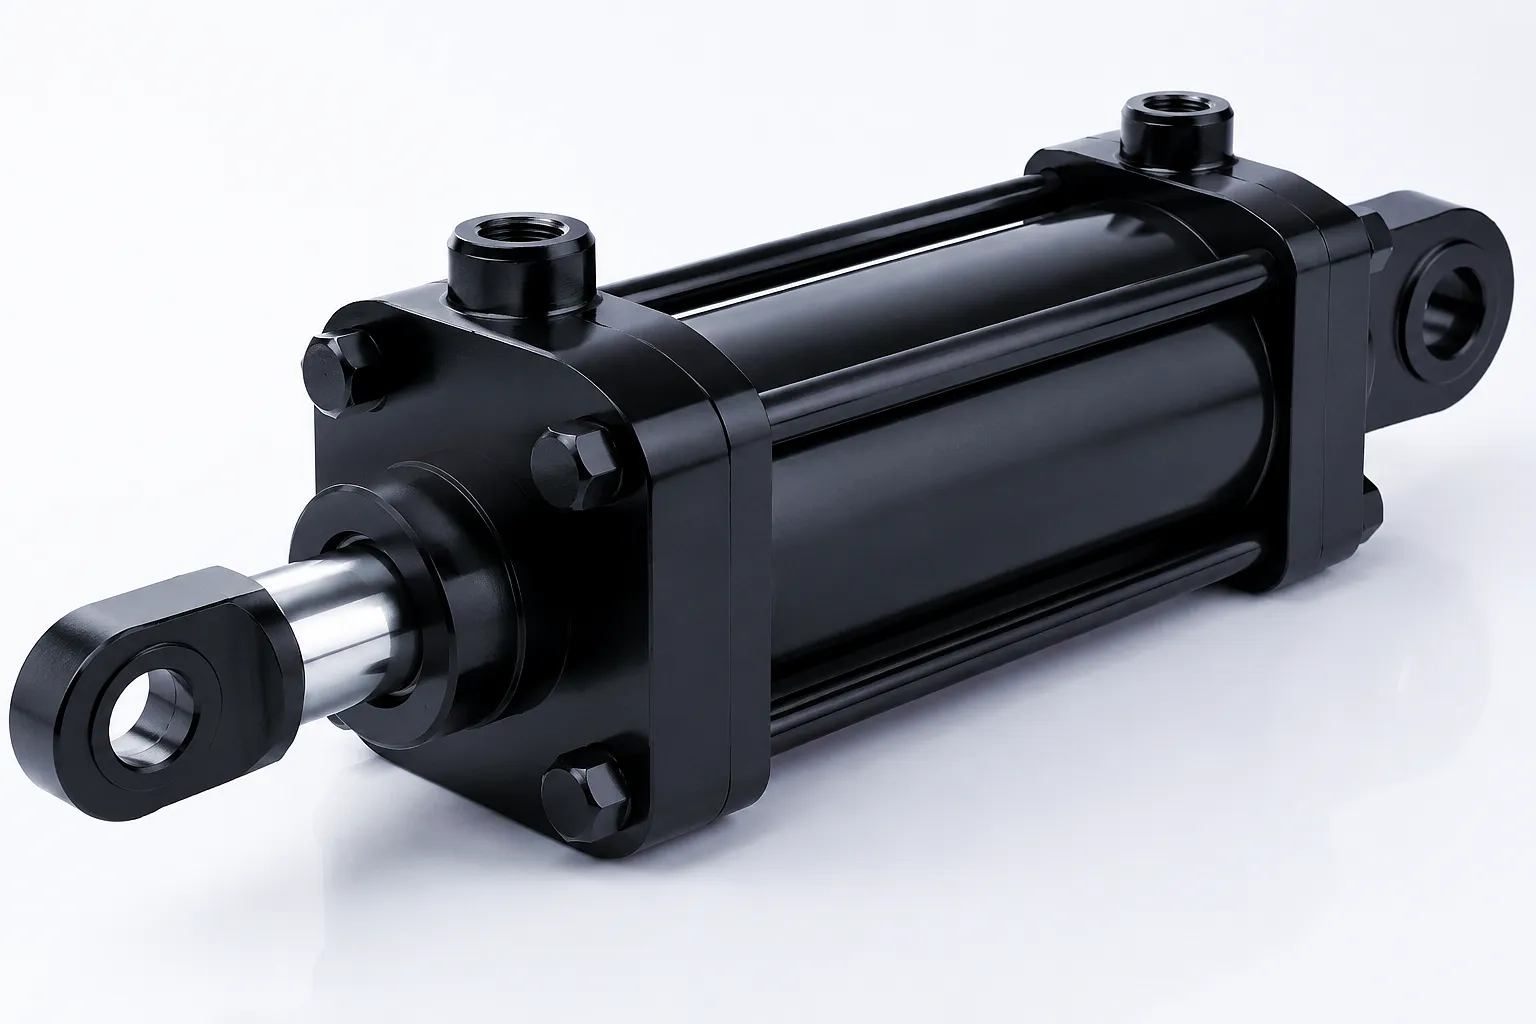
Choosing the wrong seal material is one of the most reliably expensive mistakes in hydraulic cylinder maintenance. The seal compound must be chemically compatible with the system’s hydraulic fluid, rated for the working temperature range, capable of withstanding the system’s maximum operating pressure, and physically suited to the surface finish of the cylinder rod and bore. For UK operators, the working environment adds further complexity: coastal plant equipment experiences salt-laden air that can attack certain elastomers over time, while agricultural boom cylinders in the UK’s farming heartlands — from the Lincolnshire Wolds to the Somerset Levels — are often contaminated with aggressive agrochemicals that degrade standard nitrile compounds rapidly.
Polyurethane seals dominate general-purpose hydraulic cylinder applications due to their excellent abrasion resistance and good pressure capacity, making them the standard choice for construction plant and materials handling equipment. However, polyurethane’s temperature ceiling — typically around 100°C continuous — makes it unsuitable for proximity to heat sources in foundry or steel mill environments. PTFE-based compound seals offer near-universal chemical resistance and extremely low friction, making them ideal for high-cycle servo-hydraulic systems and applications requiring minimum breakout force, such as precision positioning cylinders in automotive assembly plants in the English Midlands. For high-temperature applications — flame-cutting equipment, forge press cylinders, die-casting machine actuators — fluorocarbon (Viton) compounds offer the best thermal stability at the cost of a significantly higher unit price.
NBR (Nitrile) — general hydraulic oils, -30°C to +100°C
PU (Polyurethane) — high abrasion resistance, excellent for mobile plant
PTFE — low friction, chemical resistant, servo applications
FKM (Viton) — high temp, aggressive fluids, premium cost
EPDM — water-glycol fluids, fire-resistant HF fluids
Boom Cylinder Technical and Performance Specification Table
Industrial Application Scenarios: Where Boom Cylinder Seal Decisions Matter Most
Understanding the application environment is central to making the right seal replacement decision. Different industries in the UK impose very different demands on cylinder sealing systems, and the maintenance strategy must reflect those specific operational realities.
On HS2 construction sites across the Midlands corridor, and major bridge rehabilitation projects in Bristol and London, boom cylinders on excavators, demolition machines, and concrete pump trucks work at extreme duty cycles. High-cycle, high-load operation in abrasive environments makes polyurethane seals the dominant choice, but contamination control during reseal work is critical — construction sites are rarely clean environments, and even microscopic grit introduced during assembly will generate rod scoring within days. Specialist seal replacement with full fluid flush and filter change is strongly recommended for any cylinder operating in active construction zones. Explore our Frame Support Cylinder for construction-grade applications.
Agricultural boom cylinders — on telescopic handlers, tractor front loaders, and precision sprayer booms across Norfolk, Lincolnshire, and the Yorkshire Wolds — face a uniquely aggressive environment. Agrochemicals, fertiliser residue, and biological contamination attack standard nitrile seals aggressively. EPDM or FKM seals provide superior resistance and are worth the premium cost for machines operating through full spray seasons. UK farming’s seasonal downtime window — typically November through January — represents the ideal opportunity for planned seal replacement, allowing the work to be done in a heated workshop at low urgency rather than on a mud-soaked headland with a crop waiting. DIY replacement is appropriate for experienced agricultural engineers on standard loader cylinders, provided the bore and rod are confirmed undamaged.
Sheffield’s remaining special steel producers and Rotherham’s rolling mill operators place exceptional demands on hydraulic boom cylinders used in ladle cranes, billet manipulators, and rolling mill coiler arms. Thermal radiation, scale contamination, and radiant heat exposure demand FKM or PTFE seal compounds rated above 150°C continuous, combined with external heat shields on cylinder mounting brackets. In these environments, DIY seal replacement is generally inadvisable — the specialist knowledge of thermal barrier design, correct fluid viscosity for ambient operating temperatures, and post-rebuild pressure testing to 1.5x working pressure demands equipment and expertise that most in-house maintenance teams do not routinely maintain. An accredited hydraulic cylinder rebuild service with documented testing procedures is the right choice here, both technically and from a liability standpoint under UK HSE enforcement.
Port cranes at Tilbury, Grimsby, and Southampton’s container terminals operate knuckle-boom and luffing-boom hydraulic cylinders continuously under salt-mist conditions. External seal compound and wiper lip material must resist chloride-accelerated degradation, and rod chrome plating specification is typically more demanding than standard plant equipment — minimum 25 µm hard chrome depth is common in marine-grade specifications. For vessels and port equipment operating under Maritime and Coastguard Agency (MCA) or Lloyd’s Register oversight, seal replacement work may form part of a statutory maintenance record and should be documented to the required standard. Our Outrigger Rack Support Cylinder is engineered for precisely these marine-grade demands.
Executing a Safe In-House Boom Cylinder Seal Replacement
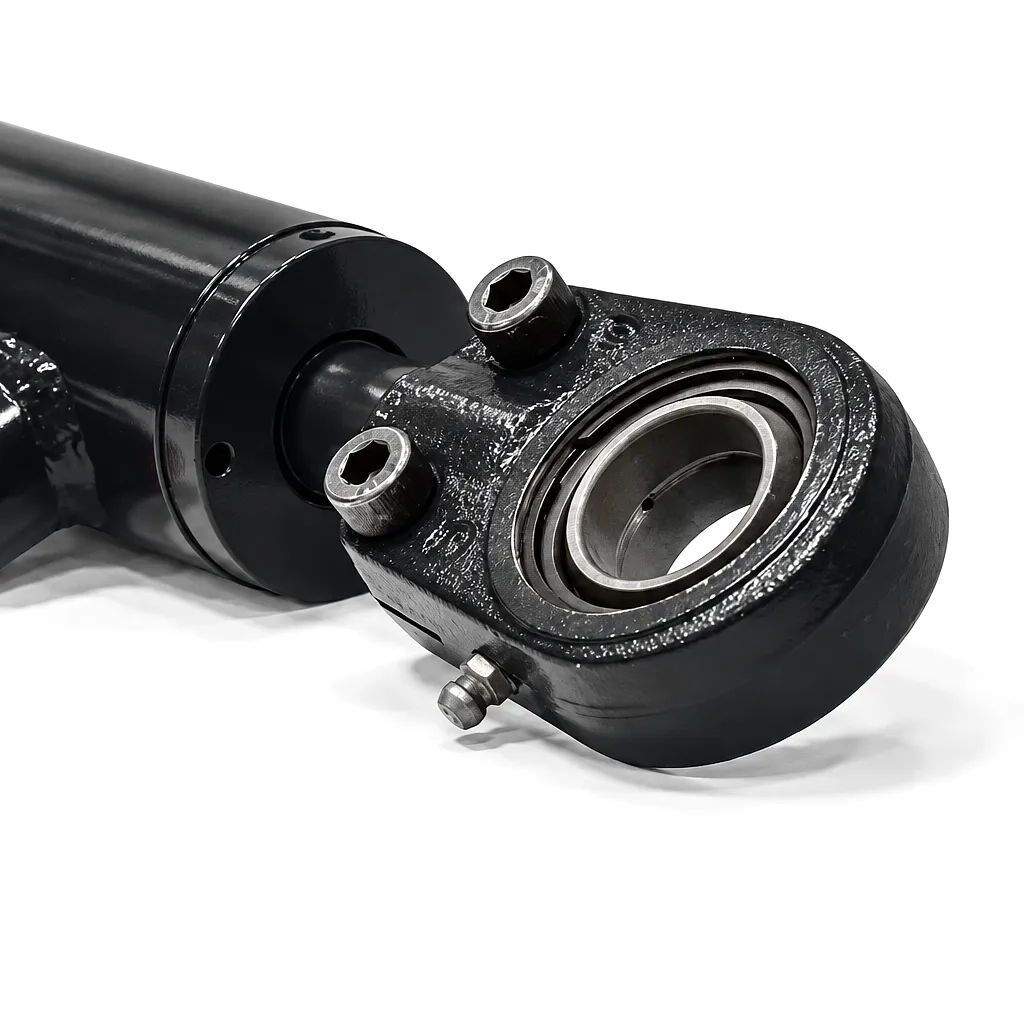
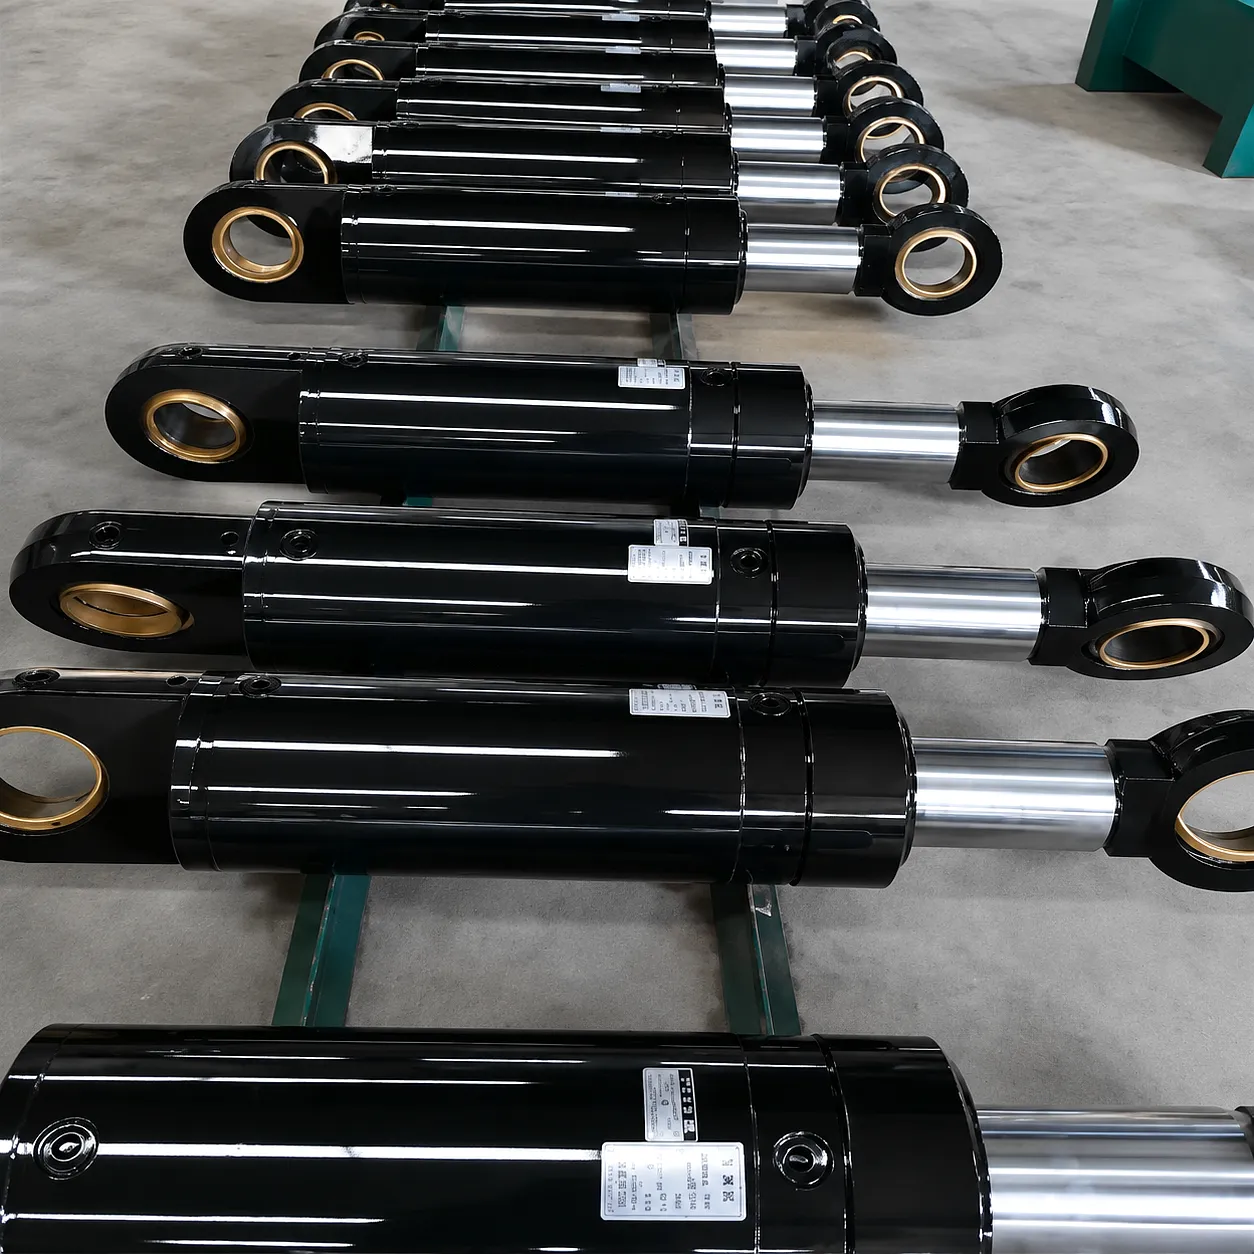
Where a DIY replacement has been determined appropriate after completing the decision framework above, the following procedure provides the technical foundation for a safe, successful outcome. This covers a standard welded double-acting boom cylinder — the most prevalent type found on construction excavators and agricultural telehandlers across the UK.
Before touching any hydraulic fitting, the system must be fully depressurised. This means shutting down the prime mover, cycling the control valve through all positions to release accumulator pressure, and confirming zero pressure on a gauge fitted to the service port. Lock-out/tag-out procedures must be applied, documented, and signed off per the Provision and Use of Work Equipment Regulations (PUWER). This step is absolute — stored hydraulic energy at typical working pressures is lethal if released suddenly. Any component under residual pressure must never be loosened until confirmed at zero bar.
Cap all hydraulic ports immediately on disconnection using clean, purpose-made port plugs — never rags or tape, which introduce contamination. Support the cylinder using appropriate lifting equipment rated for its mass (large boom cylinders can exceed 200 kg). Transport to a clean, well-lit, temperature-controlled workshop environment. The quality of the working environment during seal replacement is as critical as the quality of the seal components themselves — airborne dust landing on a freshly installed piston seal before the gland is torqued down is enough to cause premature failure.
Remove the gland nut or retaining ring using the manufacturer-specified tool — improvised methods risk thread damage that will escalate a straightforward seal job into a full gland replacement. Once the gland is removed, withdraw the rod assembly carefully, supporting it horizontally to prevent side-loading on the barrel bore edge. Inspect the rod surface under bright light for scoring, pitting, or corrosion. Measure bore diameter at three positions along the barrel with an internal micrometer. Any out-of-round measurement exceeding the manufacturer’s tolerance stops the DIY process immediately and triggers specialist referral.
Remove all existing seals using a non-metallic pick tool — metal tools will score seal grooves and generate metal particles that contaminate the rebuilt assembly. Clean all seal grooves thoroughly with lint-free cloth and compatible cleaning solvent, ensuring no residue remains. Inspect groove profiles for wear or damage. Measure groove dimensions against the new seal manufacturer’s specifications — groove wear beyond tolerance means a replacement piston or gland housing, not a seal-only repair. This meticulous preparation is what separates a durable rebuild from one that leaks within a season.
Lubricate all new seals with fresh system hydraulic fluid immediately before installation — never petroleum jelly or grease, which can degrade seal compounds. Install seals in the correct orientation (direction of pressure acts against the primary seal lip). Assemble the rod into the barrel slowly, using a lead-in chamfer or fitting sleeve to prevent lip damage at the bore entry edge. Torque the gland nut to the manufacturer’s specification — under-torquing causes gland movement under pressure; over-torquing distorts the seal housing. Fill the cylinder with clean, filtered fluid through the service port before reconnection. On first re-pressurisation, cycle the cylinder slowly through three full extension/retraction cycles at low pressure before returning to full working pressure.
Customer Success Story: Leeds-Based Materials Handling Equipment Manufacturer
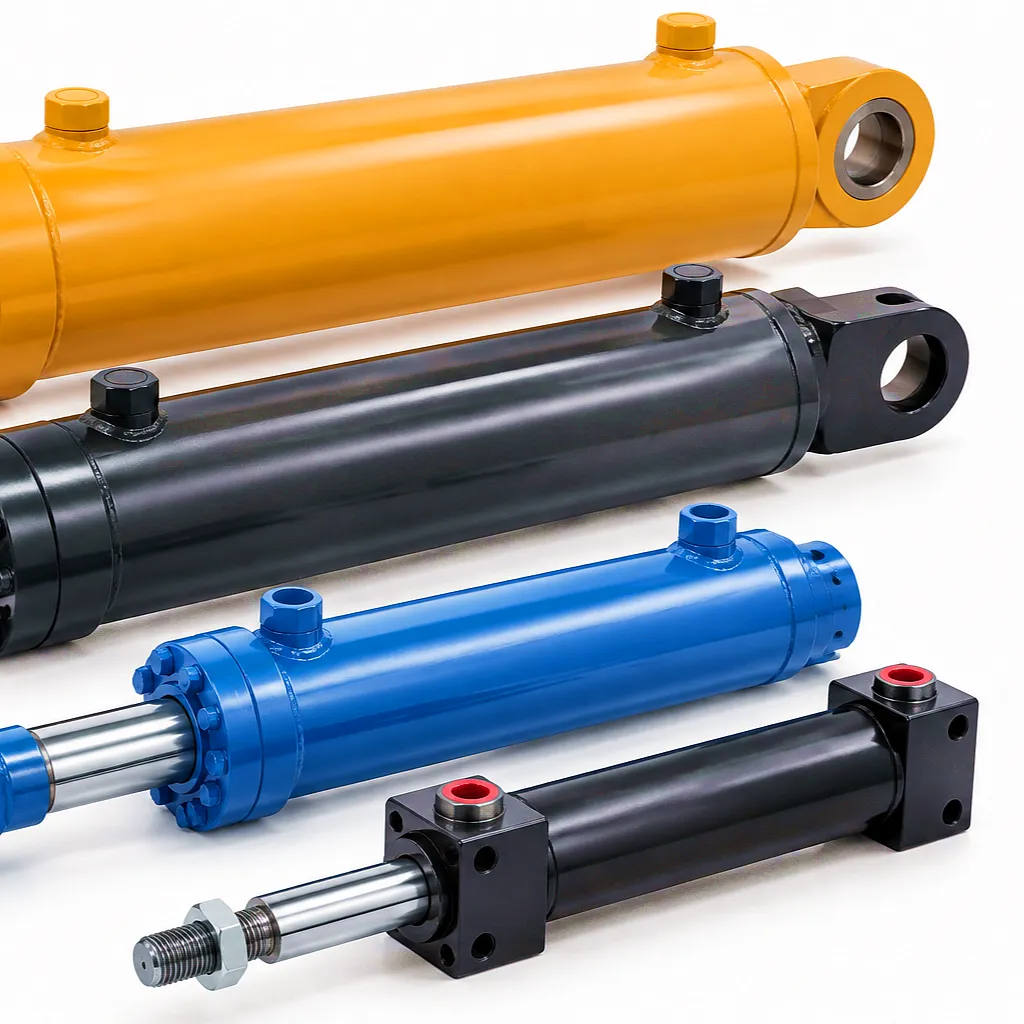 Pennine Industrial Handling Ltd, a West Yorkshire-based manufacturer of custom telescopic handlers for the UK logistics and port sectors, faced a recurring challenge: the boom cylinders fitted to their third-generation reach stacker design were requiring seal replacement every 14–18 months of operation — far below the 36-month target interval the product engineering team had designed for. Symptoms included gradual rod seal weeping commencing around 6,000 operating hours, progressing to visible oil pooling on the boom arm by 8,000 hours. The company’s in-house maintenance workshop had been performing seal replacements but found they were cycling through kits without improving service life.
Nachdem das technische Team von Ever Power mit einer Ursachenanalyse beauftragt wurde, wurden zwei verstärkende Faktoren identifiziert: Die ursprüngliche Dichtungsspezifikation verwendete eine Standard-Polyurethan-Stangendichtung in einer Anwendung, bei der die Geometrie des Auslegerarms eine kontinuierliche außermittige Belastung erzeugte – was zu lokalen Lippenspannungen führte, die unter den Validierungsbedingungen des Prüfstands nicht auftraten. Die Oberflächenrauheitsspezifikation der Stange von Ra 0,6 µm, die für Standardzylinder akzeptabel ist, erwies sich zudem als unzureichend für die Betriebsfrequenz einer Hafenmaschine im 16-Stunden-Schichtbetrieb. Ever Power empfahl ein Kombinationsdichtungspaket, bestehend aus einer PTFE-beschichteten Polyurethan-Primärstangendichtung mit einer präzisionsgeschliffenen Stangenoberfläche von Ra 0,3 µm und einem modifizierten Abstreifdichtungsprofil, um den Belastungen durch Ablagerungen im Hafenterminal standzuhalten.
Pennine rüstete die nächste Produktionscharge von 12 Maschinen, die an einem großen Containerterminal an der Humber-Mündung eingesetzt wurden, mit der überarbeiteten Zylinderspezifikation von Ever Power aus. Die anschließende Überwachung nach 12 Monaten zeigte, dass es bei der gesamten Flotte zu keinen Dichtungsausfällen gekommen war – die zuvor wiederkehrende Fehlerursache war somit vollständig beseitigt. Das Ingenieurteam von Pennine integrierte die Zylinderspezifikation von Ever Power daraufhin als Standard für alle neuen Reachstacker-Modelle. Das Unternehmen stellte außerdem auf ein geplantes jährliches Dichtungsinspektionsprotokoll um – anstatt auf den reaktiven Austausch zu setzen – und senkte so die gesamten Wartungskosten pro Maschine weiter.
„Nachdem wir 18 Monate lang immer wieder dieselben Dichtungsausfälle an unserer Reachstacker-Flotte bekämpft hatten, deckte Ever Powers Ursachenanalyse etwas auf, das unserem Team völlig entgangen war. Die modifizierte Dichtungsspezifikation hat das Problem vollständig beseitigt. Zwölf Maschinen, null Dichtungsausfälle in zwölf Monaten – genau diese Zuverlässigkeit benötigen unsere Hafenkunden. Der technische Support vor und nach der Lieferung war gleichermaßen beeindruckend.“
„Wir benötigten eine spezielle Bohrungs- und Hubkombination für den Austausch des Auslegers eines Forstkrans, mit FKM-Dichtungen für die Chemikalienbeständigkeit in unserer Holzbehandlungsanlage. Ever Power fertigte innerhalb von drei Wochen nach Zeichnungsfreigabe einen vollständig dokumentierten Sonderzylinder inklusive Prüfzertifikaten. Die Passform war auf Anhieb perfekt, und die PSSR-Dokumentation erfüllte die Anforderungen unseres Versicherungsprüfers ohne Nachbesserungsbedarf.“
„Unsere Abbruchabteilung setzt in Birmingham und im Black Country Hochleistungs-Pulverzerrer und Scherenaufsätze auf Liebherr- und Volvo-Trägerfahrzeugen ein. Die Auslegerzylinder dieser Maschinen sind enormen Seitenbelastungen ausgesetzt, und die Standard-Dichtungssätze hielten weniger als sechs Monate. Ever Power entwickelte eine Pufferdichtung und eine Führungsringkonfiguration speziell für asymmetrische Lastprofile. Wir haben nun seit 14 Monaten keinen Dichtungswechsel mehr durchführen müssen – ein Ergebnis, das unsere Ausfallkosten in diesem Geschäftsjahr messbar reduziert hat.“
Häufig gestellte Fragen
Dieser Artikel beantwortet die Fragen, die britische Anlagenbetreiber, Wartungsingenieure und Beschaffungsteams am häufigsten zum Thema Austausch und Lieferung von Auslegerzylinderdichtungen stellen.
bearbeitet von gzl
 German
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French
 Greek