
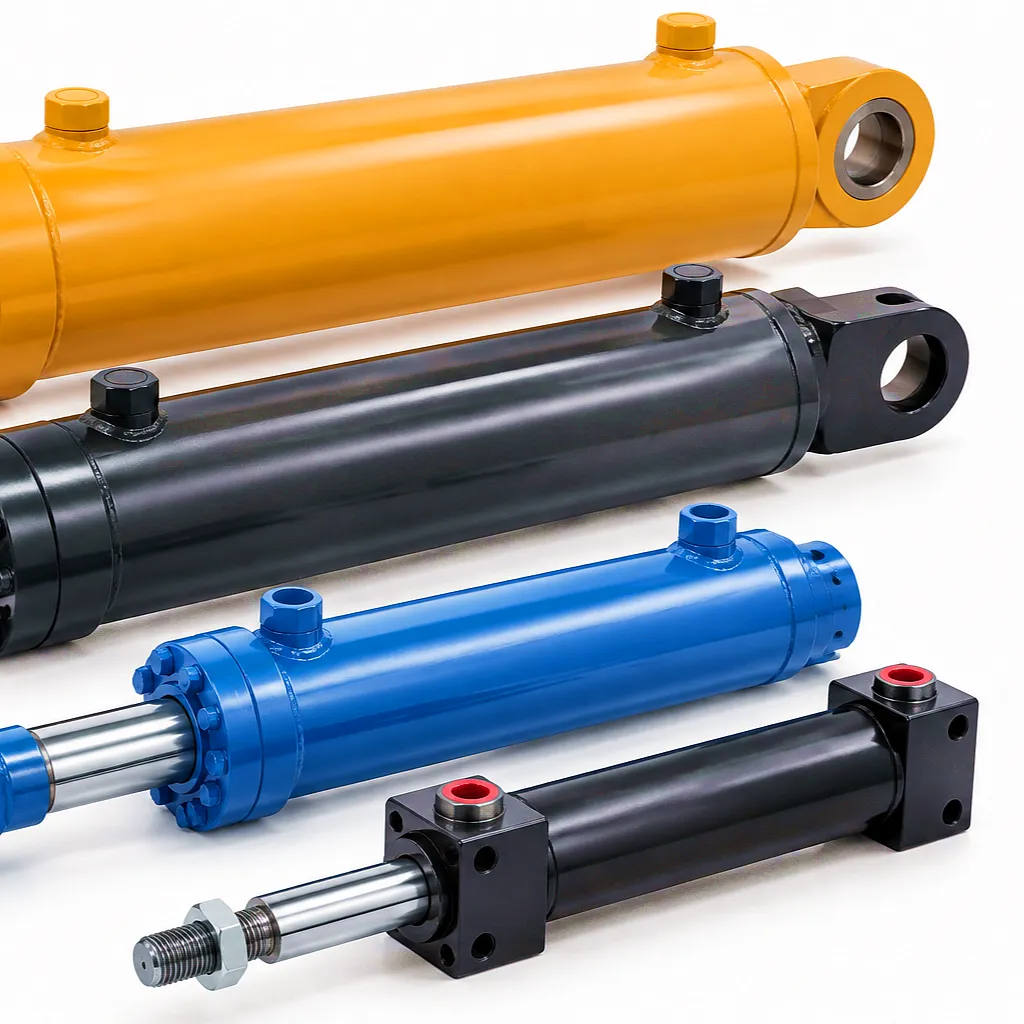
 Walk through any warehouse in Sheffield, Birmingham, or along the industrial corridors of the Midlands, and you will find hydraulic cylinders sitting in inventory for weeks, months, or sometimes years between project cycles. These components represent a significant capital commitment — precision-machined chrome rods, hardened steel barrels, and high-specification sealing systems that must perform flawlessly the moment they are called back into service. The challenge is straightforward but routinely underestimated: a hydraulic cylinder that looks intact on the outside can carry invisible corrosion damage that renders it unreliable or entirely inoperable once reinstalled.
Why Hydraulic Cylinders Corrode in Storage
UK warehouses and outdoor storage yards experience significant daily and seasonal temperature swings. When a hydraulic cylinder cools overnight, the air trapped inside the barrel contracts, drawing in ambient air through imperfect seals. As temperatures rise again, that moisture-laden air deposits condensation directly onto internal metal surfaces. This thermal pumping effect — cycling through hundreds of warm-cool-warm events over a single winter — generates far more internal moisture exposure than most engineers anticipate. Steel that would be stable for years in a controlled environment can show visible rust within a few months under these conditions.
Hydraulic fluid left inside a cylinder during storage is a double-edged asset. Fresh, well-maintained mineral oil provides a protective film on internal surfaces — but degraded fluid, or fluid that has absorbed water during service, becomes actively corrosive. Water-contaminated hydraulic oil forms acidic compounds that attack both steel and aluminium alloy components. Cylinders removed from plant equipment should always be drained, flushed with clean preservative oil, and refilled before storage. Leaving service fluid in place without testing its condition is one of the most common and most damaging storage errors made across UK industrial workshops.
The chrome-plated piston rod is the most visible and most vulnerable component during storage. Chrome plating provides excellent corrosion resistance under dynamic operating conditions — the rod is continuously lubricated by the wiper seal — but in static storage, any area of exposed rod that protrudes beyond the rod seal is at the mercy of ambient humidity and airborne contaminants. Near coastal or industrial areas of the UK, such as those around Bristol, Teesside, or the Humber estuary, salt-laden or chemically active air can initiate corrosion on unprotected chrome within days. Even micro-pitting invisible to the naked eye compromises the sealing surface for the working life of the cylinder.
Pre-Storage Preparation: The Correct Procedure
No storage method is effective without proper preparation before the cylinder goes on the shelf. The preparation sequence is not a checklist of optional extras — it is a systematic engineering process that determines the condition of the cylinder when it returns to service. Hydraulic cylinders that have been correctly prepared before long-term storage can remain in fully serviceable condition for 18 to 36 months without any intermediate intervention. Cylinders that go into storage in service condition — ports open, rod exposed, fluid unchecked — can show significant corrosion damage within 90 days, particularly in UK storage environments where ambient humidity regularly exceeds 70% RH from autumn through spring.
Remove all contamination from the external barrel, end caps, and rod using a non-corrosive degreasing agent. Pay particular attention to port threads and seal grooves. Any trapped mud, cutting fluid, or industrial residue left on the surface will hold moisture against the metal and accelerate localised corrosion during storage.
Drain all service hydraulic fluid and test it for water content before proceeding. If water content exceeds 500 ppm or the acid number is elevated, the fluid must be replaced. Flush the internal chamber with clean, fresh mineral oil (ISO VG 46 or 68 grade) until effluent runs clear. This removes acid degradation products and suspended particles that would otherwise remain in contact with internal surfaces throughout storage.
After flushing, fill the cylinder completely with a storage-grade preservative oil. Specialist hydraulic preservation fluids contain vapour-phase corrosion inhibitors (VCI additives) that protect surfaces not directly wetted by the oil film. Fill to 100% of internal volume to eliminate the air gap that would otherwise allow condensation. Ensure the cylinder is positioned horizontally and rotated 90 degrees every 4 to 6 months to redistribute the preservative coating across all internal surfaces.
Retract the piston rod to its fully retracted position before storage — this minimises the rod surface area exposed beyond the rod seal. Coat all exposed chrome rod surface with a thin layer of VCI-impregnated grease or a specialist wax-based rod preservation compound. Do not use petroleum jelly (Vaseline) as a long-term coating: it degrades, absorbs moisture, and can contaminate the hydraulic system when the cylinder returns to service.
Install solid plastic or metal port plugs in every hydraulic port — both pressure and return side. Plastic dust caps are inadequate for long-term storage: they permit air movement. Solid plugs maintain the internal pressure of the preservative fill and prevent atmospheric moisture from bypassing the plugs through thread gaps. Label each plug with the port size and thread specification so they can be correctly replaced with matching hydraulic fittings when the cylinder is returned to service.
Storage Environment Requirements
The storage environment is as important as the preparation of the cylinder itself. Even a perfectly prepared hydraulic cylinder will suffer degradation if placed in an unsuitable environment. Across Birmingham’s manufacturing belt, Sheffield’s steel fabrication yards, and the logistics hubs around Leeds and Manchester, storage conditions vary enormously — from temperature-controlled warehouse bays to open outdoor storage compounds where cylinders are left stacked on pallets exposed to the elements. Understanding what each environment does to a stored cylinder is essential for making the right storage decisions.
Ideal storage temperature for hydraulic cylinders is between +5°C and +25°C. Below 0°C, trapped water in seals or residual fluid can expand on freezing, damaging seal lips and cracking polyurethane components. Above 35°C sustained, elastomeric seals begin to harden and lose recovery — a process that is not reversed when temperatures normalise. UK climate is generally within range, but outdoor or uninsulated storage in January in northern England regularly breaches the lower threshold.
Relative humidity must be maintained below 60% RH for corrosion risk to remain low. Above 70% RH, condensation becomes active on metal surfaces whenever temperature fluctuates. Above 85% RH — a common condition in unventilated UK storage sheds during winter — even well-prepared cylinders with coated rod surfaces can develop surface corrosion within 60 days if any preparation step was incomplete. Installing dehumidifiers rated for the storage volume is strongly recommended for any facility storing more than 10 cylinders over a period exceeding 90 days.
Hydraulic cylinders must be stored horizontally on padded racking — never vertically with the rod facing down, which causes preservative oil to drain away from the rod seal area, and never standing upright on their end caps, which concentrates load stress on gland threads. Horizontal storage keeps the preservative fluid evenly distributed across internal surfaces. Padding the contact points with rubber or HDPE blocks prevents the barrel from developing flat spots, particularly on thinner-wall cylinders used in mobile plant applications.
Wrap each cylinder individually in VCI (Vapour Corrosion Inhibitor) poly film before placing it in storage. VCI film emits a chemical vapour that forms a monomolecular protective layer on metal surfaces within the enclosed space, providing ongoing corrosion protection even against moisture that penetrates the external packaging. Do not use standard polythene sheeting as a substitute — it traps moisture rather than controlling it, creating a warm, humid microenvironment that accelerates corrosion instead of preventing it.
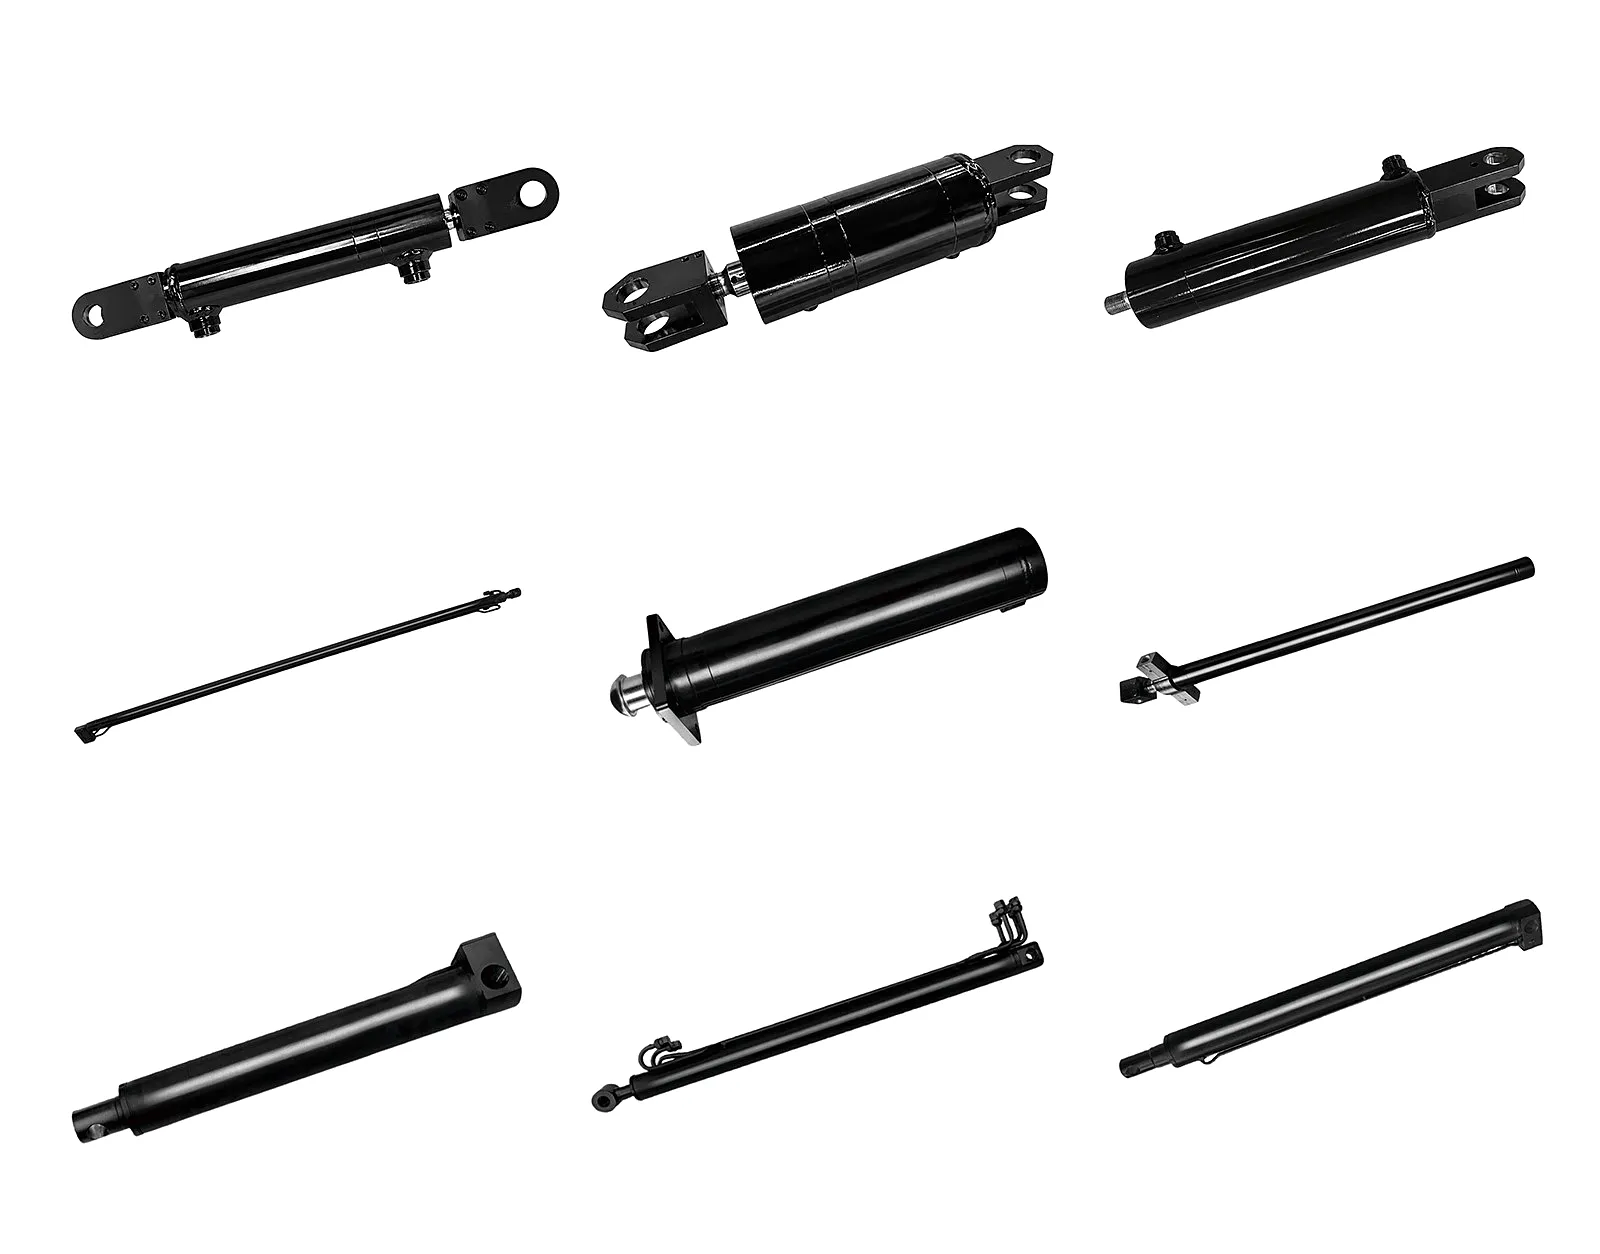
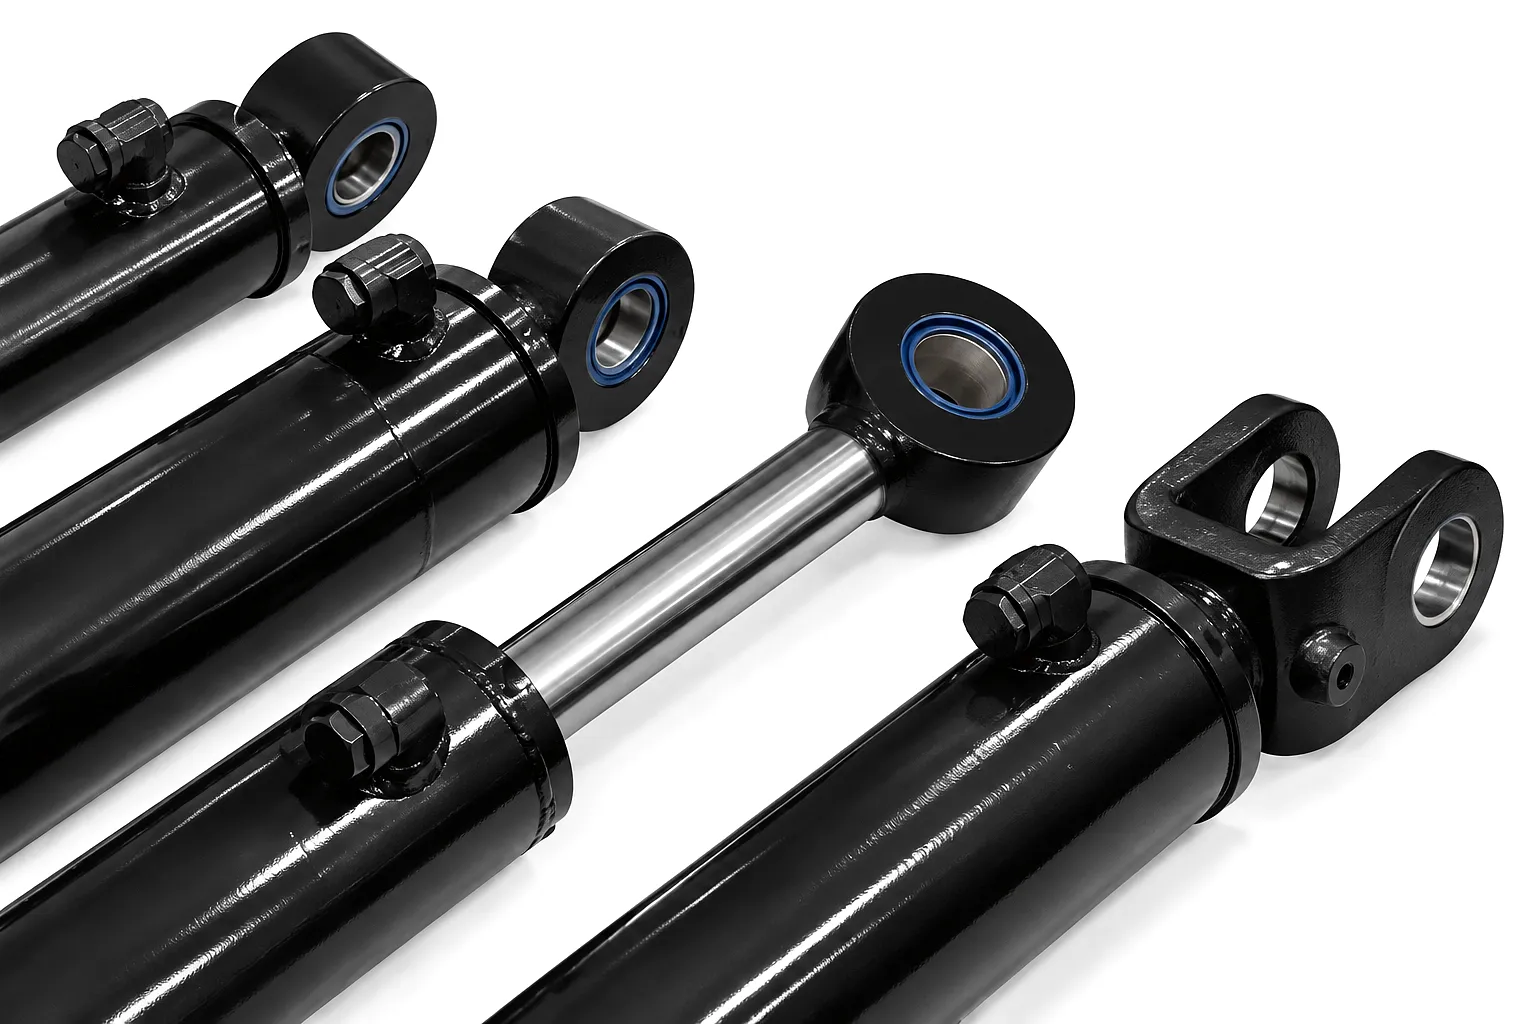
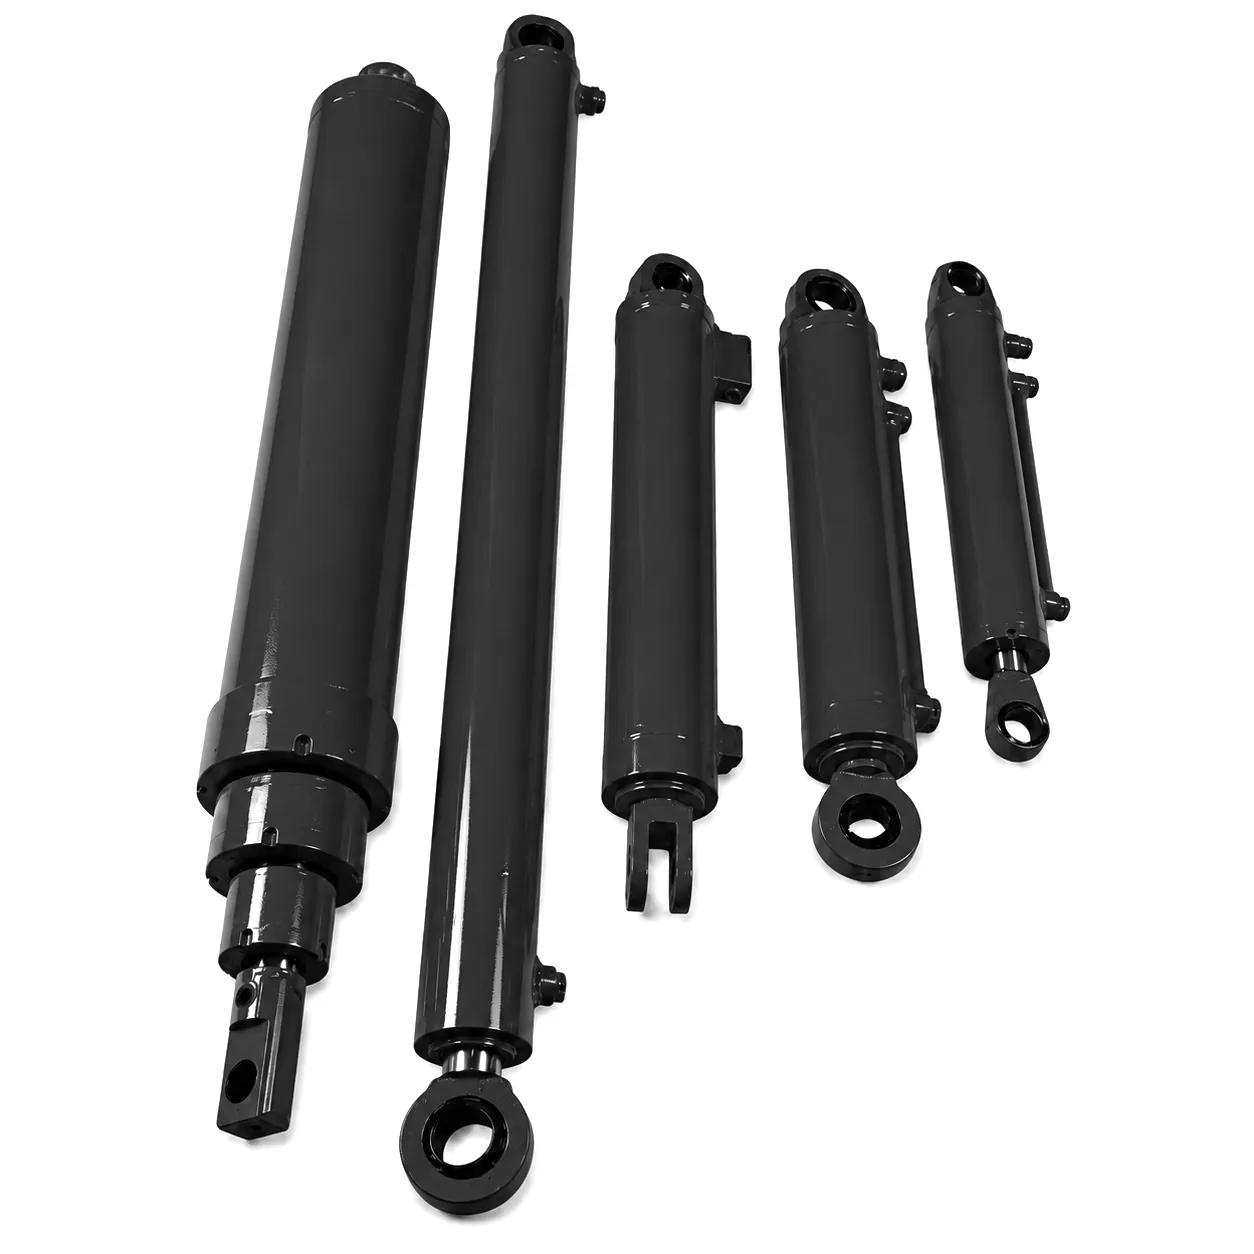
Ever Power hydraulic cylinder product range — engineered for demanding UK industrial applications
Hydraulic Cylinder Storage Parameters — Technical Reference Table
The table below consolidates the key storage parameters, material compatibility data, and performance thresholds for hydraulic cylinders in long-term UK storage conditions. These figures are based on engineering standards including BS EN ISO 4413 (Hydraulic Fluid Power — General Rules), internal testing from major cylinder manufacturers, and operational data from UK plant hire and heavy industry sectors. Use these values as minimum benchmarks for your own storage procedure documentation.
| Parameter | Short-Term (0–3 months) | Medium-Term (3–12 months) | Long-Term (12–36 months) |
|---|---|---|---|
| Storage Temperature | 0°C to +35°C | +5°C to +25°C | +10°C to +20°C (controlled) |
| Max Relative Humidity | ≤ 75% RH | ≤ 60% RH | ≤ 50% RH (dehumidified) |
| Internal Fluid | Service oil if tested clean | Preservation oil (VCI additive) | Dedicated hydraulic preservation fluid, full fill |
| Rod Coating | Light VCI grease layer | VCI wax compound, 0.2–0.5 mm film | Heavy wax preservation + VCI poly wrap |
| Port Plugs | Plastic dust caps acceptable | Solid steel or brass plugs | Solid plugs + PTFE thread tape seal |
| Inspection Interval | Visual check on receipt | Every 90 days | Every 60 days; fluid test every 6 months |
| Seal Material Limits | PU: to -10°C; NBR: to -20°C | PTFE/HNBR preferred | HNBR or FKM for best shelf stability |
| Chrome Rod Hardness | Maintained: 850–1000 HV | Maintained if correctly coated | Verify on recommission; min 800 HV |
| Cylinder Rotation | Not required | 90° rotation every 6 months | 90° rotation every 4 months |
| Packaging | Standard poly wrap | VCI poly film | VCI film + sealed VCI bag + moisture indicator |
Industrial Storage Scenarios: Where These Guidelines Apply
These hydraulic cylinder storage protocols are not theoretical — they apply directly to real-world industrial operations across the UK where cylinders routinely spend extended periods in inventory. The specific challenges and risk factors differ between industry sectors, and understanding those differences allows procurement and maintenance teams to tailor their storage procedures accordingly.
Recommissioning After Long-Term Storage
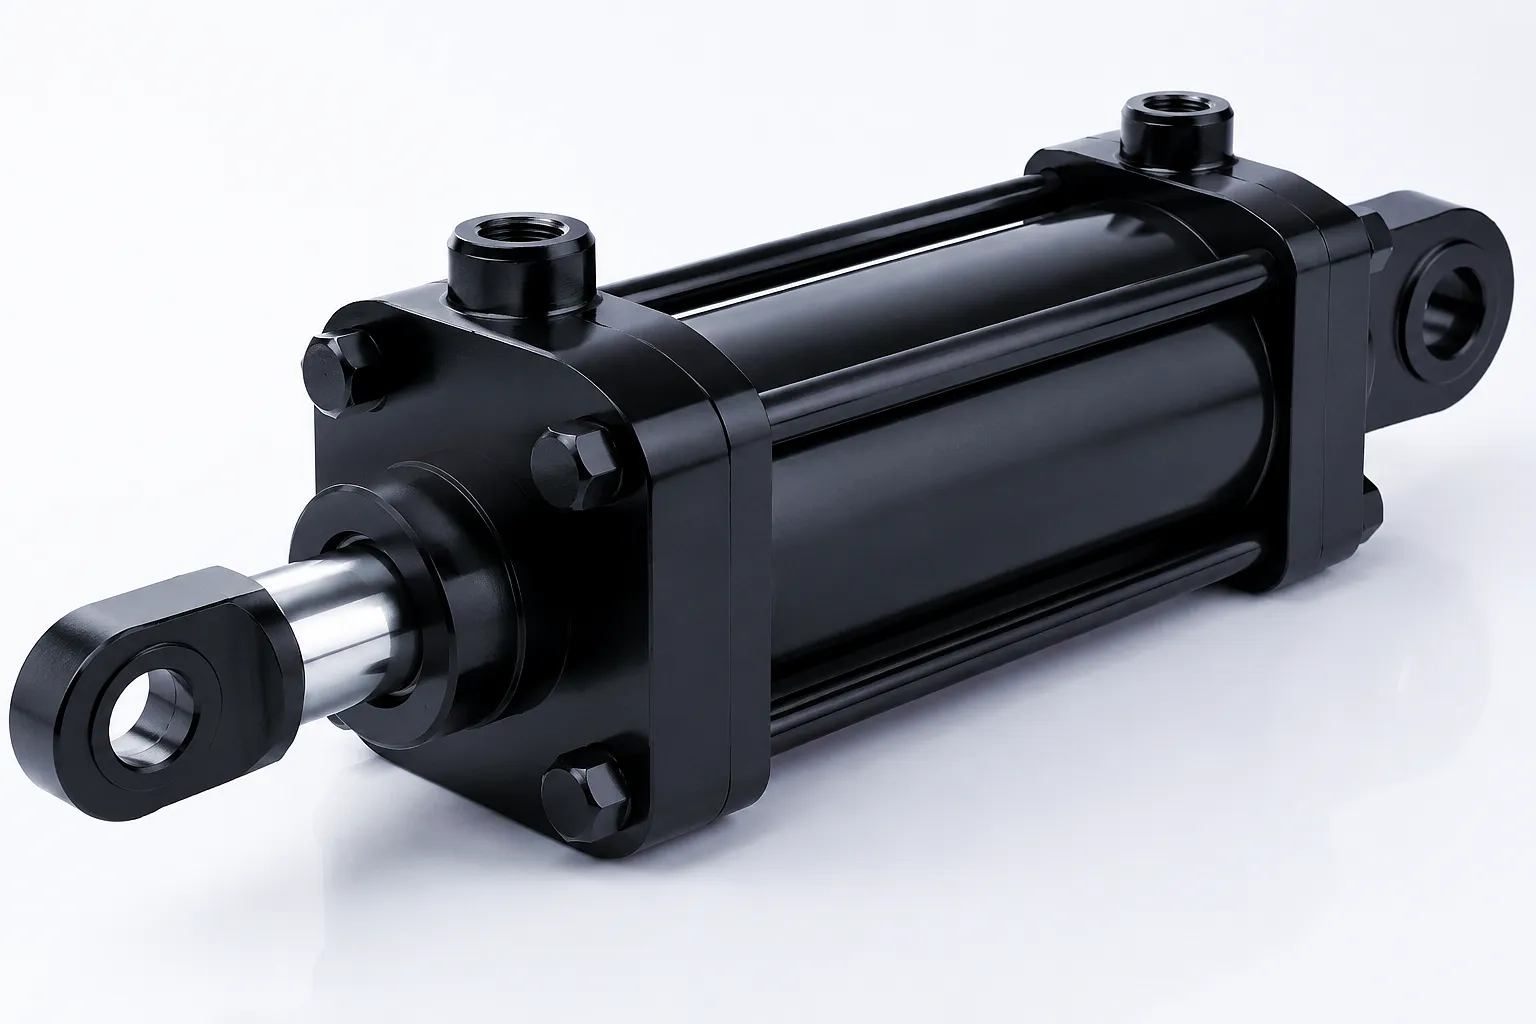
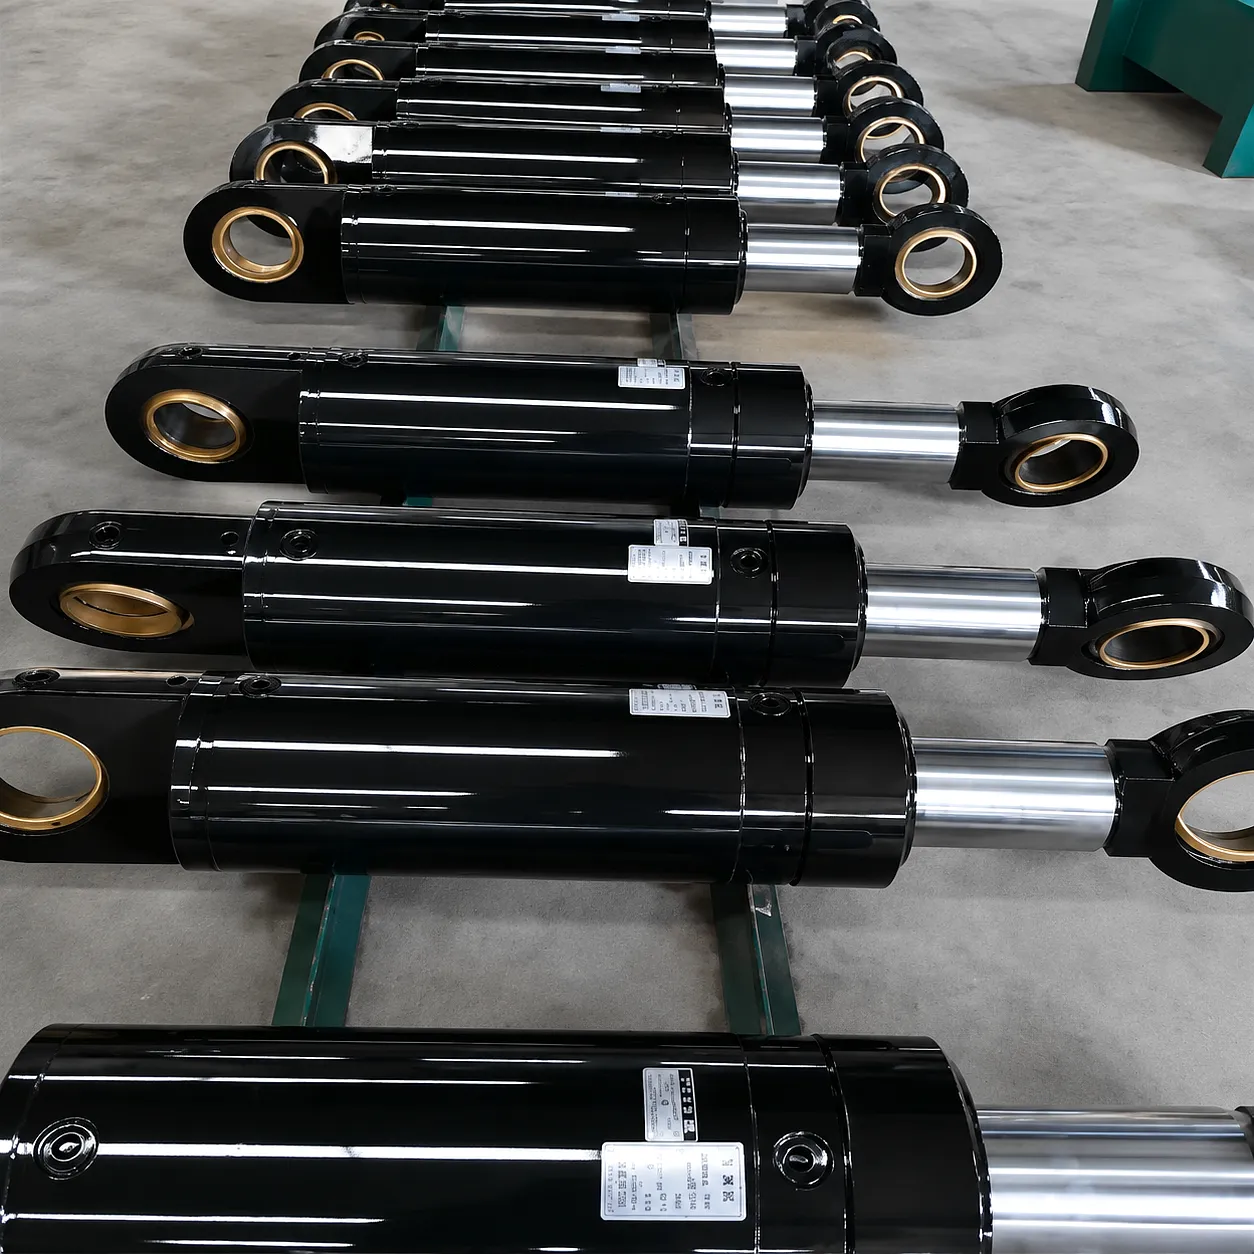
Recommissioning a hydraulic cylinder from long-term storage requires a structured inspection and preparation sequence before the cylinder is installed in the machine. The purpose of this sequence is to verify that the storage period has not compromised any component, and to prepare the cylinder for the transition from its preservation state to operational hydraulic service. Skipping this process and installing a stored cylinder directly is a false economy: an unverified cylinder that fails in service costs many times more in downtime and repair than the 30–60 minutes required for a thorough recommissioning inspection.
Check the entire external surface for corrosion, impact damage, and seal condition. Inspect the chrome rod surface under direct light for pitting, scoring, or corrosion spots. Any visible pitting larger than 0.2 mm diameter or deeper than 0.1 mm on the sealing zone of the rod is cause for rejection — the rod must be re-plated or the cylinder returned for refurbishment before installation.
Drain and collect all preservative fluid for disposal or analysis. If the preservation fluid has emulsified, shows visible discolouration, or tests positive for elevated water content, the internal surfaces should be flushed with clean mineral oil before service fluid is added. Do not discharge preservative hydraulic fluid to drain — dispose of it in accordance with EA (Environment Agency) waste oil regulations applicable in England.
Before full installation, conduct a bench pressure test at 1.5 times the rated working pressure, held for 5 minutes with no visible external leakage or pressure drop exceeding 2%. This test verifies that the rod and port seals have retained their elasticity and dimensional integrity through the storage period. Cylinders that fail the pressure test should be fully stripped for seal inspection — the seals may require replacement even if the storage conditions appeared correct.
After installation, perform 10–15 slow stroke cycles at 30–40% of maximum working pressure before bringing the cylinder to full operating load. This break-in procedure redistributes seal lubrication, expels any residual air from the circuit, and allows the seal lip to re-conform to the rod surface after the static set that inevitably occurs during extended storage. Monitor for creep, drift, or external leakage through the first 4 hours of loaded operation.
Customer Success Story: Sheffield Steel Fabrication
 Meridian Steel Structures, a Sheffield-based manufacturer of structural steel components for bridge and infrastructure projects, operates a series of large-tonnage hydraulic press lines. During the 14-month hiatus of a major bridge fabrication contract — caused by planning approval delays on a new motorway junction scheme in the North — two of their 250-tonne presses were taken offline. The hydraulic cylinders in these presses, with bore diameters of 180 mm and 220 mm and working pressures of 350 bar, were left in place without any formal storage preparation procedure.
“The replacement cylinders from Ever Power arrived pre-filled with preservation oil and correctly sealed — they arrived ready to store, which is something we have never seen from a supplier before. When we recommissioned them eight months later, every single one passed the pressure test first time.”
“The stainless rod specification on these cylinders has been exceptional for our environment. We store equipment near a coastal yard in Immingham and previous cylinders from other suppliers were showing rod pitting within six months. The Ever Power units have now been through two full storage cycles without a single corrosion issue.”
“We specified custom HNBR seals and a 316L rod on a batch of cylinders for buffer stock in our Birmingham facility. Ever Power’s technical team guided us through the seal grade selection for our specific fluid and temperature range, and the cylinders were delivered with a full factory storage certificate. Exactly what a serious industrial supplier should offer.”
Explore Our Storage-Ready Cylinder Range
Häufig gestellte Fragen
Contact Ever Power’s technical sales team for a custom quotation — bore, stroke, seal grade, preservation specification, and UK shipping included in every enquiry response.
Get a Quote — [email protected]
bearbeitet von gzl
 German
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French
 Greek