
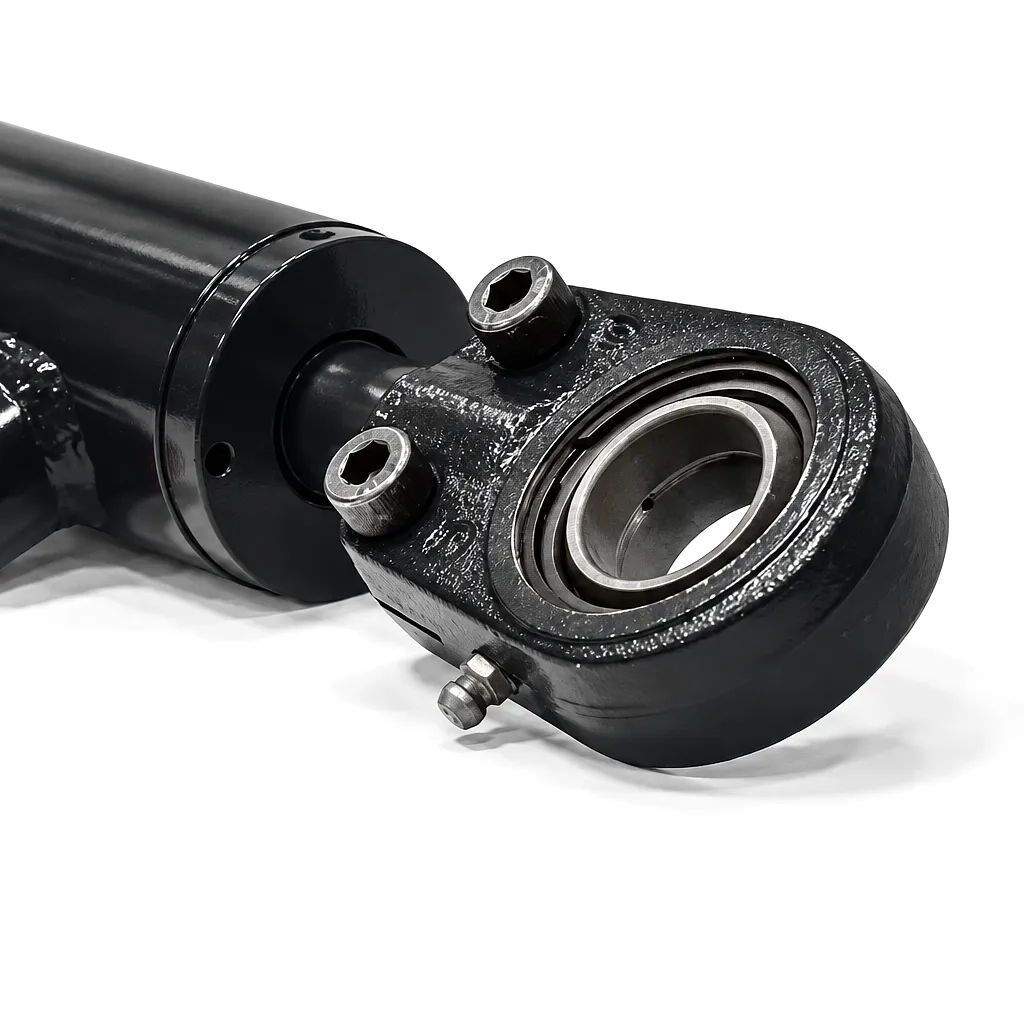
 When a hydraulic cylinder fails in service — whether in a Sheffield steel plant, a Birmingham construction equipment yard, or an offshore platform off Aberdeen — the root cause more often than not traces back to the bore surface. The inner tube wall is where the seal rides, where friction is generated, and where contamination particles either pass harmlessly or embed and score. Getting that surface right demands a deliberate choice between two proven machining processes: honing and skiving. Both produce a smooth, geometrically accurate bore, but they differ fundamentally in the way metal is removed, the surface texture they leave behind, and the type of application each serves best. Understanding these differences is not a matter of factory trivia — it directly determines seal life, cylinder cycle count, leakage rates, and total cost of ownership for any hydraulic system operating under real industrial conditions.
Require a hydraulic cylinder with precision bore finishing for your application? Our engineering team is ready.
The Core Mechanics: What Each Process Actually Does to the Metal
Honing uses a rotating tool fitted with abrasive sticks — typically made from aluminium oxide, silicon carbide, or CBN (cubic boron nitride) — that expands radially against the bore wall while the tool simultaneously reciprocates axially. The combined rotary and linear motion produces the characteristic cross-hatch pattern visible on a correctly honed bore surface. This cross-hatch geometry is not cosmetic; the angular grooves function as micro-reservoirs for lubricating oil film, which is exactly what a reciprocating hydraulic seal needs to survive millions of cycles without dry contact. Honing removes material in very small increments — typically in the region of 0.01 mm to 0.05 mm per pass — making it a precision finishing operation rather than a material removal process. It corrects minor geometric deviations such as out-of-roundness and taper left by previous operations like cold drawing or turning, and it achieves bore roughness values (Ra) between 0.2 µm and 0.8 µm depending on the abrasive grit and tool pressure selected.
Skiving — almost always used in combination with roller burnishing, hence the industry shorthand “skiving-burnishing” — is a two-stage single-pass operation performed on a specialised machine. In the skiving phase, indexable carbide inserts arranged in a cutting head remove material from the bore wall in a single axial pass, achieving dimensional accuracy and straightness at far higher rates than honing. In the immediately following burnishing phase, hardened steel rollers plastically deform the surface peaks left by the cutting inserts, cold-working the material to achieve a smooth, work-hardened surface with roughness values as low as Ra 0.05 µm to 0.2 µm. The plastically deformed surface layer has higher hardness and compressive residual stress than the base metal, which translates to better fatigue and wear resistance in service. The entire combined skiving and burnishing operation takes a fraction of the time required to hone a tube of equivalent length.
Surface Texture, Oil Film, and What Seals Actually Need
The connection between bore surface finish and seal performance is more nuanced than a single Ra number. Hydraulic seals — polyurethane U-cups, PTFE buffer seals, composite wiper rings — function by maintaining a coherent oil film between the seal lip and the bore wall. If the surface is too rough, the peaks abrade the seal material and the valleys trap contaminant particles that score the bore. If the surface is mirror-smooth, the oil film breaks down, the seal runs partially dry, and friction spikes cause stick-slip motion that degrades positional accuracy in servo-controlled circuits.
The 30° to 45° angle cross-hatch produced by honing is the gold standard for conventional hydraulic seals. The angled channels carry oil under the seal as the piston rod or piston advances and retracts, creating a stable elastohydrodynamic lubrication regime even at slow speeds and high clamping loads. This is why honing remains the preferred bore finishing process for cylinders that run slow-speed, high-load cycles — such as press cylinders, forging presses, and heavy earthmoving bucket circuits — where the oil replenishment function of the cross-hatch pattern makes the difference between a 20,000-hour seal life and a 3,000-hour one.
Roller burnishing produces what tribologists call a plateau surface — a flat, hard running surface interrupted by fine valleys. This geometry suits modern composite and PTFE-backed seals very well, since these materials generate less friction and tolerate a smoother counter-surface without risking dry running. The higher surface hardness from cold-working (typically an increase of HV 50 to HV 150 depending on base material) also slows the rate of bore wear under contaminated fluid conditions. For cylinders running higher-speed duty cycles in mobile hydraulic applications — like aerial work platforms and telehandlers common on UK construction sites — the burnished surface often produces lower running temperatures and quieter operation.
From a contamination control standpoint — a critical concern for any hydraulic system certified to NAS 1638 or ISO 4406 — skiving-burnished bores have an advantage in part because the process generates fewer loose abrasive particles. Honing produces fine aluminium oxide or silicon carbide swarf that must be thoroughly flushed before assembly. If residual abrasive remains in a honed bore and enters the hydraulic circuit, it acts as a lapping compound and accelerates wear across the entire system. Rigorous post-honing cleaning protocols are non-negotiable. Skiving produces metal chips that are easier to remove with a single air blast and wipe, though both processes require proper cleanliness validation before final assembly.
Bore Finishing Technical Performance Parameters Comparison
| Parameter | Honing | Skiving + Roller Burnishing |
|---|---|---|
| Surface Roughness Ra | 0.2 – 0.8 µm | 0.05 – 0.2 µm |
| Roundness Tolerance | IT7 – IT8 | IT6 – IT7 |
| Cylindricity | ±0.02 – ±0.05 mm | ±0.01 – ±0.03 mm |
| Surface Hardness Increase | Minimal (abrasive) | HV +50 to HV +150 (cold-work) |
| Processing Speed (per metre of bore) | 8 – 25 min | 1 – 4 min |
| Material Removal per Pass | 0.01 – 0.05 mm | 0.1 – 0.5 mm |
| Typical Tube Bore Diameter Range | 25 mm – 500 mm+ | 40 mm – 320 mm |
| Best Suited Cylinder Duty | Heavy-duty, slow-stroke, high-load | High-cycle, mobile hydraulics, OEM series |
| Tooling Cost | Low – Moderate | Moderate – High (machine investment) |
| Residual Stress in Surface | Neutral to tensile (grinding burn risk) | Compressive (fatigue-beneficial) |
| Minimum Wall Thickness Suitability | Flexible (low cutting force) | Requires wall sufficient to resist roller force |
Industrial Application Scenarios and Which Method to Specify
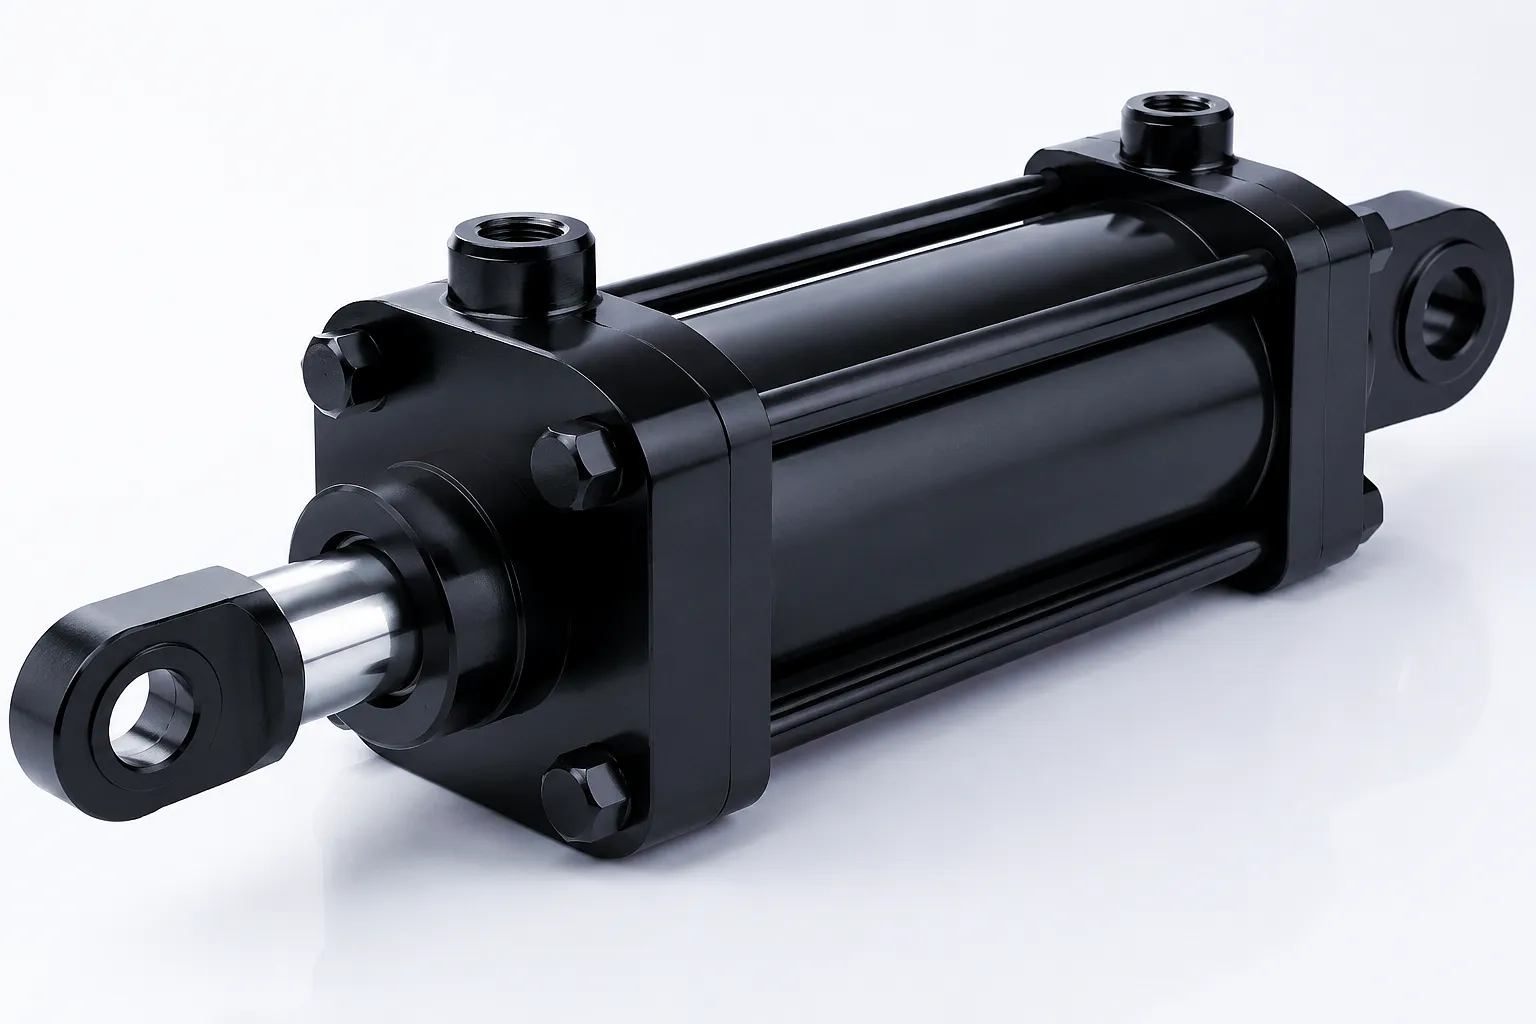
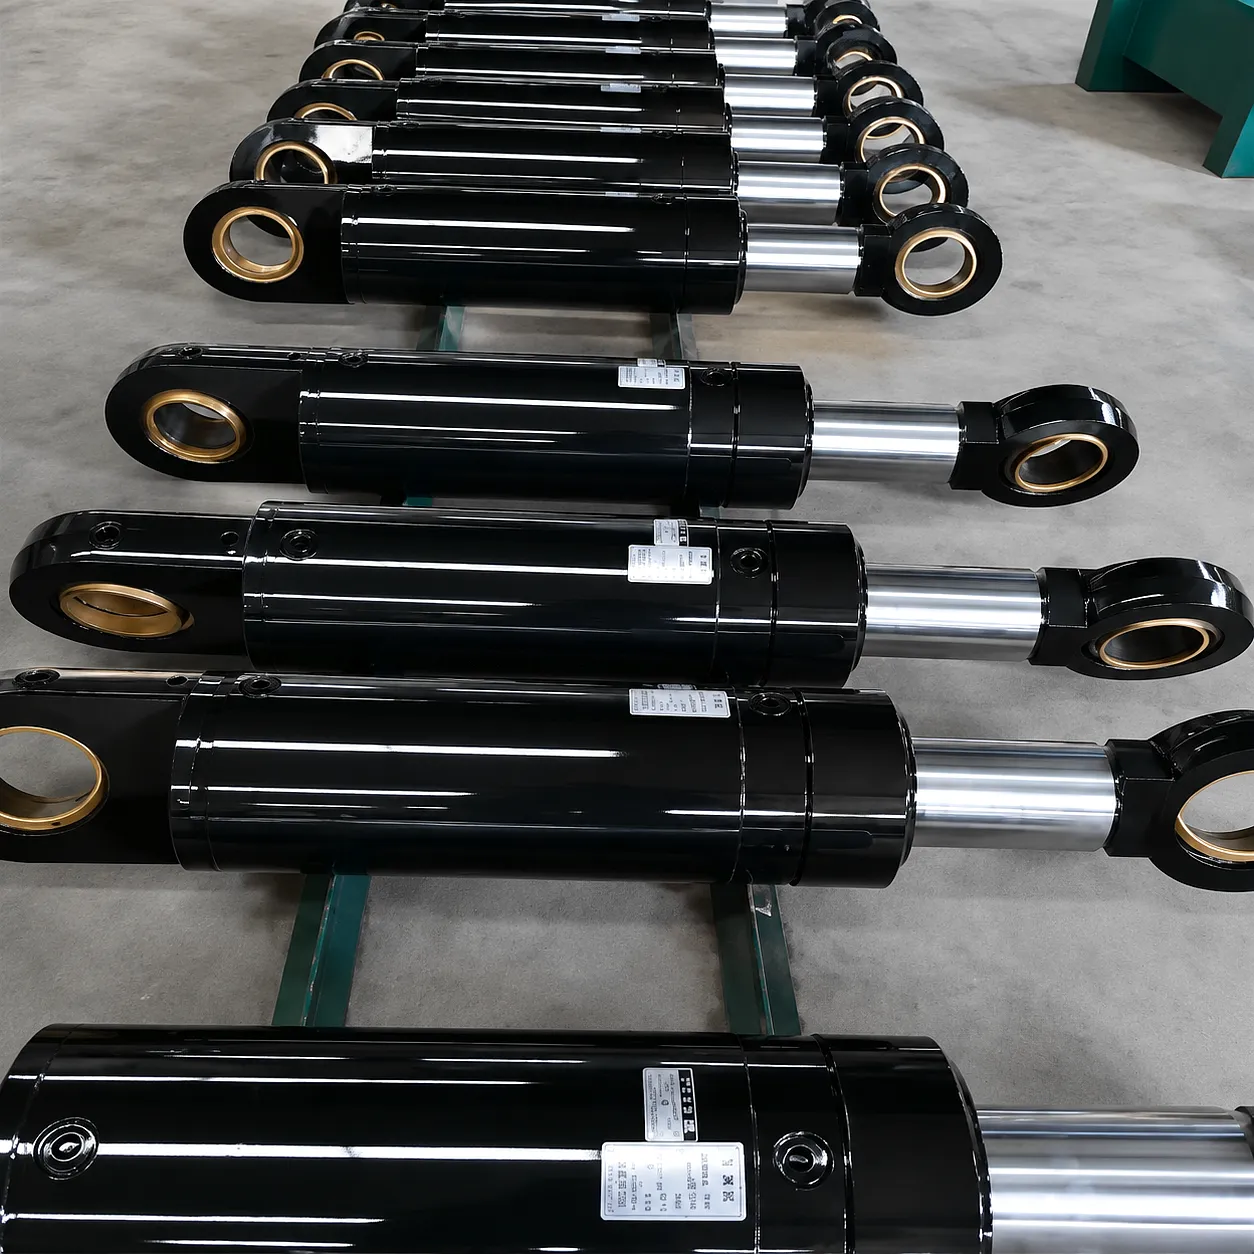 Aerial work platforms represent one of the most demanding environments for hydraulic cylinder bore quality. The cylinders extend and retract thousands of times per year, often in outdoor environments where temperature swings and contaminated air accelerate wear. The boom angle cylinders used on folding boom AWPs require dimensional accuracy over their full stroke to maintain the precise articulation angles needed for safe working at height. For this application, skiving-burnished bores offer production efficiency at scale and the surface hardness that resists abrasive wear from externally contaminated fluid. Our Klappbarer Auslegerwinkelzylinder (1458 mm Hub) is produced to this standard, with bore tolerances and surface specifications set to meet the duty cycle demands of OEM aerial platform manufacturers supplying the UK construction and utilities sectors.
Similarly, the main boom circuit in a telescopic aerial platform requires a cylinder that can maintain position precisely at full extension. Our Aerial Platform Main Boom Angle Cylinder (555mm Stroke) uses a bore finished and verified to tight surface roughness limits, ensuring the seal package performs reliably throughout its service life on both urban utility work and building maintenance applications common from London Docklands to the new developments in Leeds and Birmingham’s Digbeth quarter.
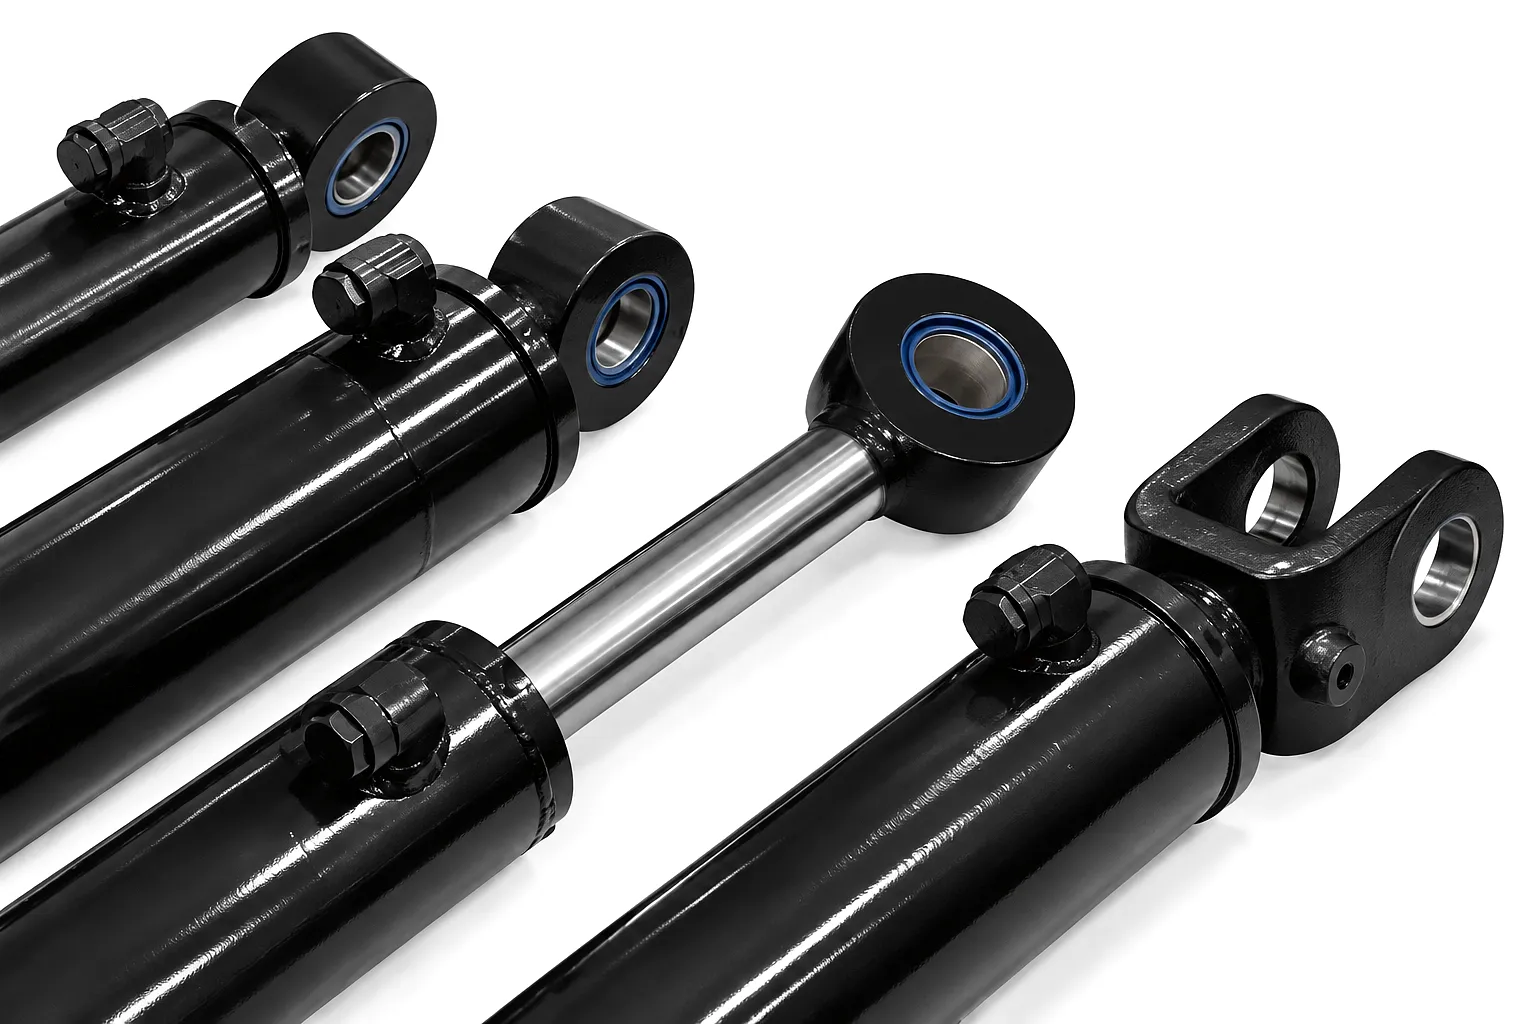
Materials and Their Influence on Finishing Method Selection
The base material of the hydraulic cylinder tube is not a secondary consideration — it is one of the primary factors that determines whether honing or skiving-burnishing will deliver the best result. The two processes interact with metal in fundamentally different ways, and some tube materials respond far better to one than the other. Understanding this relationship prevents costly process mismatches that degrade bore quality or shorten tube service life.
The workhorse tube material for hydraulic cylinders worldwide, E355 cold-drawn seamless steel has a consistent yield strength of 355 MPa minimum and a bore surface from the drawing process that already approaches the tolerances needed for skiving-burnishing entry. For standard mobile hydraulic applications, skiving-burnished E355 tube is the most economical and technically sound combination available. The material’s work-hardening rate is predictable, and the rolled burnishing operation consistently achieves surface hardness improvements of HV 60 to HV 100 above the base material specification. Honing is equally applicable where geometric correction after welding or heat treatment is required.
42CrMo4 is selected for high-pressure, thin-wall cylinders where yield strength and fatigue life take priority. Its higher hardness (typically HRC 28 to 36 after heat treatment) makes honing with CBN abrasive sticks the technically preferred finishing route because conventional aluminium oxide stones load rapidly with the harder material. Skiving carbide inserts handle 42CrMo4 well, but the burnishing force required to achieve a satisfactory surface must be carefully calibrated to avoid cracking in the heat-affected zone of welded components. Experienced hydraulic cylinder manufacturers routinely finish 42CrMo4 by both methods but apply tighter in-process monitoring when burnishing heat-treated material.
Stainless steel cylinder tubes, specified for food processing equipment, pharmaceutical plant, marine deck hardware, and chemical process applications, present the most challenging finishing scenario. Austenitic grades like 316L have a strong tendency to work-harden during machining, which can cause cutting tool loading during skiving and unpredictable surface quality during burnishing if cutting speeds and feeds are not precisely controlled. Honing with appropriate abrasive selection and lubricant — typically a high-pressure sulphurised grinding oil — provides more process control and more consistent surface finish on stainless bores. For stainless applications across UK food processing facilities in the Yorkshire and Lancashire valleys, honing remains the recommended and most widely specified process.
Ever Power: Precision Bore Finishing and Custom Hydraulic Cylinder Manufacturing
 Ever Power operates dedicated skiving-burnishing lines and precision honing capacity within the same manufacturing facility, giving our engineering team the flexibility to select the correct bore finishing process for each customer’s specific application — rather than defaulting to whichever single process the factory happens to run. This dual-process capability is a practical differentiator that matters to UK buyers specifying cylinders across multiple machine families with different duty cycle and bore quality requirements.
Our customisation service covers bore diameter from 25 mm to 400 mm, stroke lengths from 100 mm to 8,000 mm, operating pressures to 420 bar, and a full range of mounting configurations including clevis, flange, foot, and trunnion types. Tube materials are sourced from certified European and domestic mills with full material traceability documentation, and our quality system issues a bore measurement report for each cylinder with Ra verification and dimensional records. For UK export documentation requirements, we provide full CE marking support, material certificates to EN 10204 3.1B, and pressure test certificates to the specific working pressure of each order.
Our supply chain logistics are configured for efficient delivery into UK ports including Felixstowe, Southampton, and Liverpool, with standard lead times of 25 to 45 days for custom-designed cylinders and express production slots available for replacement-critical orders. Technical drawing review, custom seal specification, and application engineering support are included as standard services for B2B customers placing serial orders.
Customer Success Story: Leeds-Based Mobile Plant Manufacturer
A mid-sized OEM based in the Aire Valley industrial corridor near Leeds had been manufacturing articulated boom lifts for the UK construction rental market for over a decade. Their hydraulic cylinder supplier at the time used only a honing process for bore finishing, which delivered acceptable performance on the main boom cylinders but was creating a bottleneck in production scheduling — honing the cylinder bores across their seasonal peak production run of 60 machines per month was consuming significantly more machine time than their capacity allowed.
Their design team approached Ever Power after seeing our technical documentation on the skiving-burnishing process. Following a detailed application review — including load data, expected duty cycles, seal specification, and fluid cleanliness targets — our engineering team recommended transitioning the 80 mm and 100 mm boom angle cylinder tubes to a skiving-burnished finish while retaining honing for the two large-diameter levelling cylinders where slow-speed operation made the cross-hatch pattern more valuable.
The hybrid approach — using both bore finishing methods strategically within the same machine design — cut the customer’s cylinder lead time by 34% and reduced bore-related seal failures in the first 500 field hours by approximately 60% compared to their previous single-process supplier’s product. Seal break-out force consistency across production batches also improved markedly, allowing the customer to reduce their own factory acceptance test time per machine. The customer has since extended the partnership to cover their new 28-metre all-terrain boom platform product line, with cylinder specifications developed jointly with Ever Power’s application engineering team.
“We had a bore-related seal failure rate that was genuinely costing us money on warranty claims. Ever Power’s recommendation to switch to skiving-burnished tubes on our shorter-stroke boom cylinders halved our warranty call-outs in the first year. The bore measurement reports they send with each batch give us full confidence at assembly.”
“The customisation capability at Ever Power is genuinely impressive. We had a non-standard bore dimension and a specific surface roughness target from our seal supplier, and Ever Power hit both on the first sample batch. The lead time from drawing approval to delivery at our Leeds facility was better than what we had been getting from a European supplier.”
“What sets Ever Power apart technically is that they actually understand both honing and skiving — they don’t just default to one process and apply it everywhere. Our press-fit application needed honing for geometric correction after welded end cap assembly, and they got that right without us having to over-specify. EN 10204 3.1B material certs were provided without any additional pressure from our side.”
Making the Decision: A Practical Selection Framework
The question of honing versus skiving-burnishing rarely has a single correct answer at the application level — it has a context-dependent correct answer. The selection framework below captures the most important variables that experienced hydraulic engineers use when specifying bore finishing methods. Think of it as a set of questions to work through with your cylinder supplier’s application team rather than a prescriptive rulebook, because real applications almost always involve compound factors.
| Selection Factor | Favour Honing | Favour Skiving-Burnishing |
|---|---|---|
| Stroke speed | Below 50 mm/s (slow-cycle press) | Above 100 mm/s (mobile, fast-cycle) |
| Production volume | Low to medium (custom, bespoke) | High volume OEM series |
| Bore diameter | Very large (>320 mm) or very small | 40 – 320 mm standard range |
| Seal type | Conventional NBR / PUR U-cup | PTFE-backed composite, low-friction |
| Field repairability required | Yes (offshore, remote site) | Not required (workshop return) |
| Working fluid type | Fire-resistant, water-glycol | Standard mineral hydraulic oil |
| Geometry correction needed post-weld | Ja | Begrenzt (vor der Endbearbeitung muss die Rohre geradlinig sein) |
Häufig gestellte Fragen
Das Anwendungstechnik-Team von Ever Power arbeitet mit britischen Einkäufern, OEM-Entwicklungsteams und Beschaffungsmanagern zusammen, um die passende Bohrungsspezifikation für jede Anwendung auszuwählen und zu überprüfen. Teilen Sie uns Ihre Zeichnungen, Betriebszyklusdaten und Mengenanforderungen mit, und wir senden Ihnen eine technische Bewertung und ein wettbewerbsfähiges Angebot.
 German
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French
 Greek