
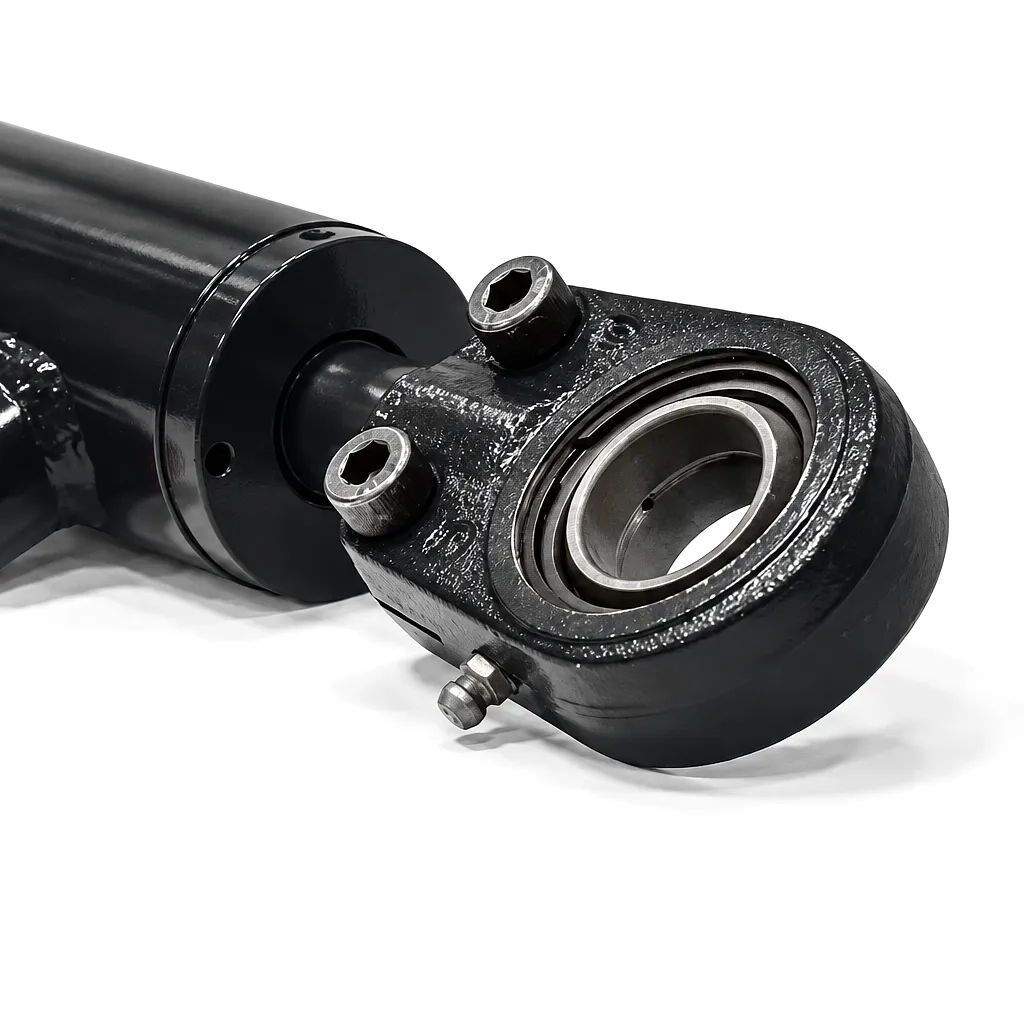
 When engineers in Birmingham machine shops or Sheffield steel processing plants spec a 12-inch stroke double-acting hydraulic cylinder, the first decision they face is rarely bore size or pressure rating — it is construction method. Tie-rod and welded cylinders share the same fundamental operating principle: pressurised hydraulic fluid alternates between cap-end and rod-end ports, producing controlled bidirectional linear force without the need for external springs or return mechanisms. But from that shared starting point, the two design philosophies diverge significantly in terms of load capacity, serviceability, installation envelope, and total cost of ownership over a working life measured in millions of cycles.
How the Double-Acting Operating Principle Works Across 12 Inches of Travel
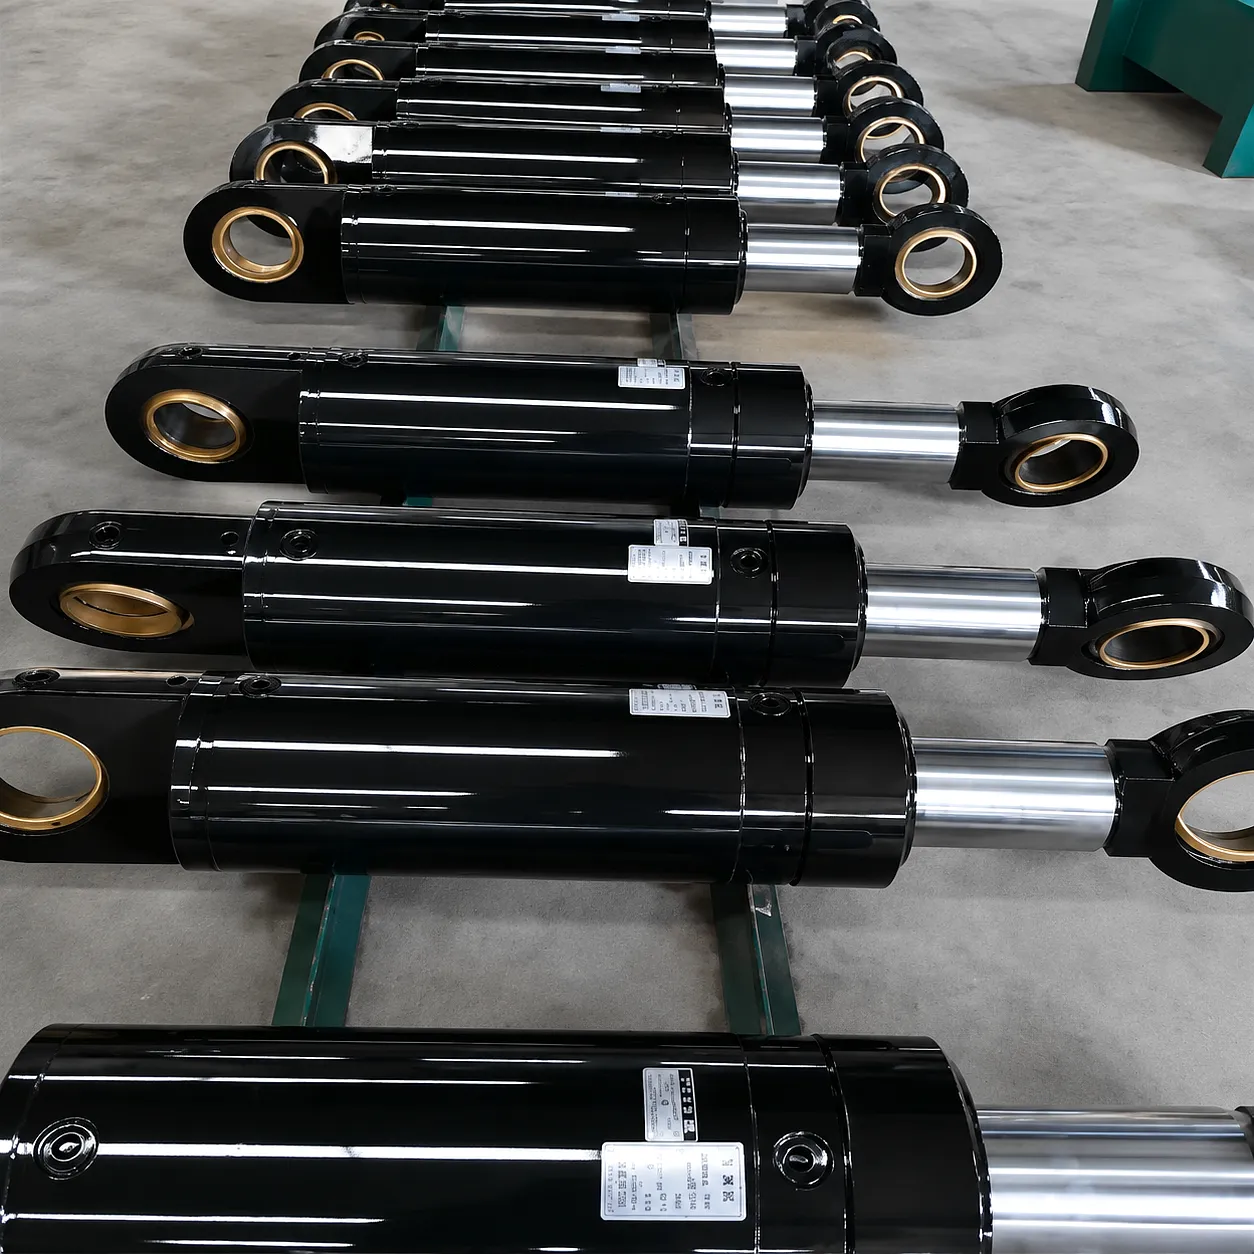
The double-acting cylinder generates force in both extension and retraction. Hydraulic fluid from the pump enters the cap-end port, building pressure against the full face of the piston. The resulting force — calculated as pressure multiplied by piston area — drives the rod forward through the full 12-inch stroke. Simultaneously, fluid displaced from the rod-end port returns to the reservoir through the control valve. When the valve shifts, flow is reversed: fluid enters the rod-end port and acts on the annular area of the piston (full bore area minus rod cross-section), retracting the cylinder with somewhat less force due to that reduced effective area. This differential area characteristic is particularly relevant in clamping, pressing and material-handling applications where extension force and retraction speed must be balanced against system flow rate and back-pressure.
Over a 12-inch stroke, dynamic sealing performance becomes critical. As the rod traverses the full travel length on every cycle, the wiper seal, rod seal and piston seal must collectively maintain a consistent fluid barrier against the rod surface and barrel bore. Any surface finish inconsistency — typically expressed as Ra (average roughness) in micrometres — accelerates seal wear and promotes bypass. The chrome-plated or induction-hardened rod surface must sustain a finish of Ra 0.4 µm or better across the entire stroke length, a specification that welded cylinder manufacturers who hard-turn and grind rods in-house can control with greater consistency than those relying on outsourced rod supply.
Key Principle Metrics for 12-Inch Stroke Design
Effective rod area ratio (single rod): typically 0.55–0.75 of cap-end area depending on rod diameter. End-of-stroke impact energy: kinetic energy = 0.5 × moving mass × velocity². Cushioning chambers sized to absorb this energy within the last 1.0–1.5 inches of travel are standard on quality double-acting cylinders used in repetitive cycle duty.
Tie-Rod Construction: Assembly, Strengths and Where It Belongs
Modular Steel Assembly
Tie-rod cylinders are assembled from discrete machined components — front and rear heads, barrel tube, piston rod, and piston — held together under pre-load by four or more threaded steel rods torqued to precise values. This modular architecture means any individual component can be replaced without scrapping the cylinder body. For plant engineering teams in Manchester or Coventry managing a large fleet of standard cylinders across multiple press lines, this repairability can substantially reduce mean cost-per-cycle over a five-year horizon.
Pressure Rating & NFPA Standardisation
NFPA-interchangeable tie-rod cylinders are rated to 2,000–3,000 PSI in most standard bore sizes. The standardised mounting dimensions mean a cylinder from one supplier can, in principle, be replaced with an equivalent unit from another without machine modifications — a significant benefit for UK procurement teams managing supply continuity risk. However, the tie-rod design does impose an outer envelope penalty: the rods themselves add width beyond the barrel diameter, which matters in confined installation spaces.
On-Site Seal Replacement
Tie-rod cylinders can typically be disassembled and resealed by a competent hydraulic technician using hand tools, without returning the unit to the manufacturer. This characteristic is particularly valued in continuous-process environments such as paper mills in Aberdeen or automotive stamping lines in the West Midlands, where unplanned downtime carries a cost measured in thousands of pounds per hour and rapid field repair is the priority over ultimate pressure performance.
Welded Construction: Compact Force Density and Heavy-Duty Reliability
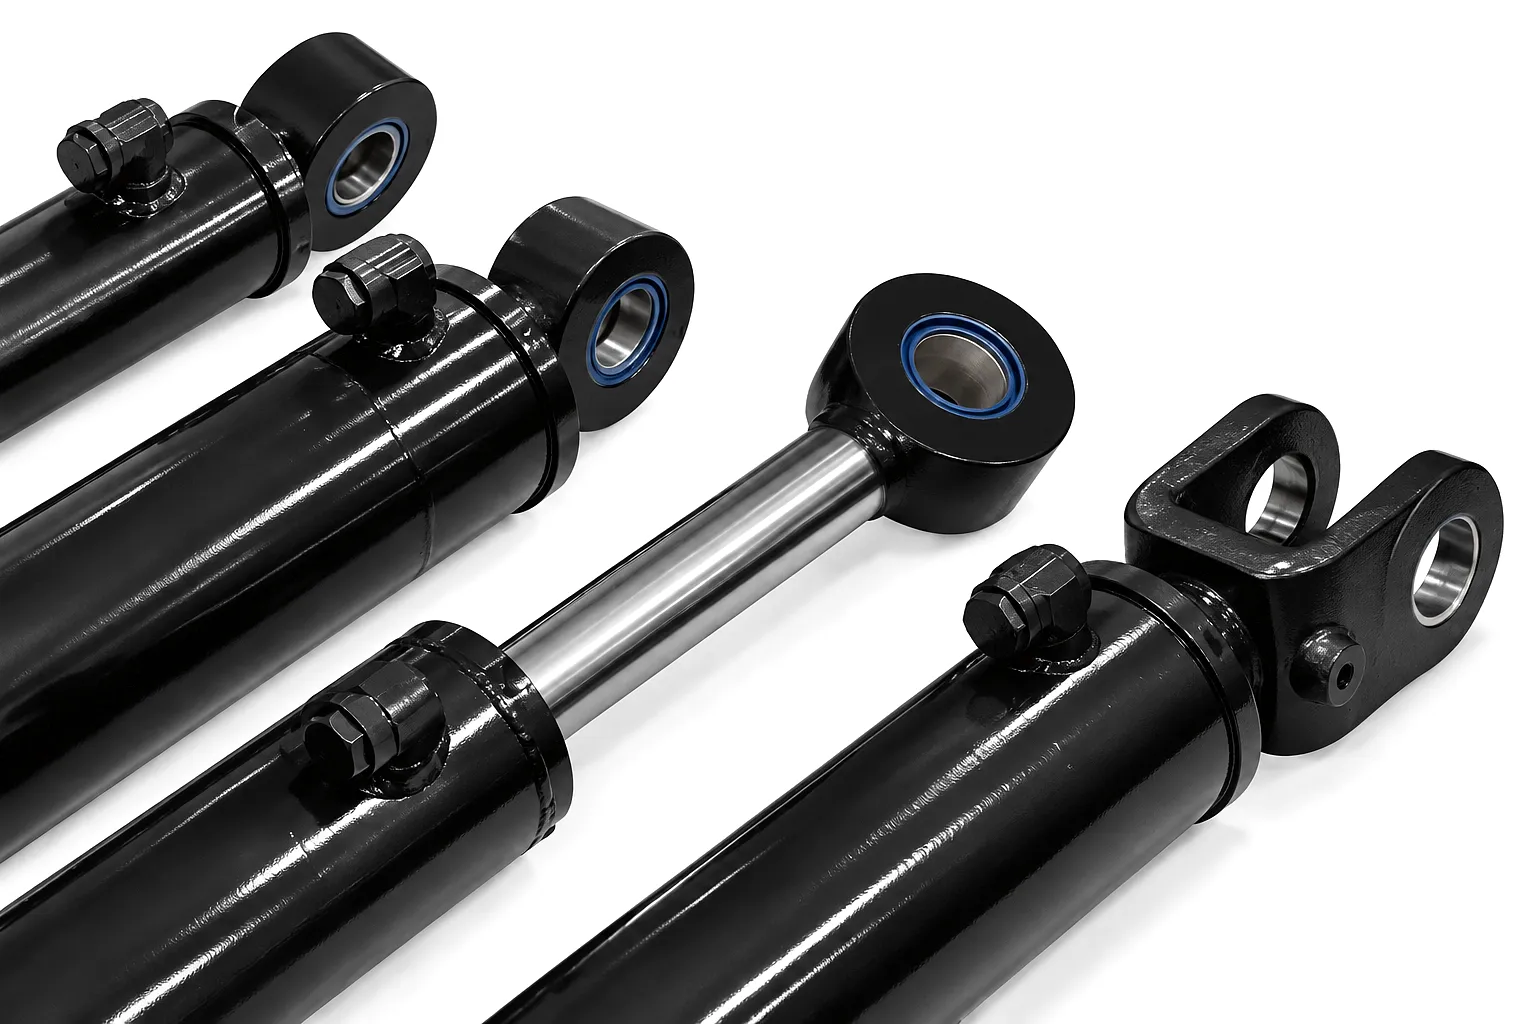
In a welded hydraulic cylinder, the end caps are directly welded to the barrel tube, eliminating the external tie-rod structure entirely. The result is a cylinder that is mechanically stiffer, dimensionally more compact for its bore size, and capable of handling considerably higher working pressures — typically 3,000–5,000 PSI and above in heavy industrial configurations. That pressure capability, combined with the absence of torque-sensitive assembly joints, makes welded cylinders the default choice for mobile plant, construction equipment, mining machinery and heavy press applications where physical envelope is limited and peak loads are extreme.
The structural continuity of a welded body also means the cylinder can absorb side loading and moment loading without the risk of the end-cap-to-barrel joint working loose under vibration — a failure mode that tie-rod cylinders are susceptible to if rod torque is not periodically maintained. In the demanding environments found on rail track maintenance machines operated around Leeds, or on aggregate processing equipment in Scottish quarrying operations, the welded cylinder’s resistance to vibration-induced loosening translates directly into longer mean time between failures.
Welded Cylinder: Key Structural Advantage
The absence of external assembly hardware reduces the overall outer diameter by 15–25% compared to an equivalent-bore tie-rod unit. For OEM integration in limited-clearance packaging — excavator booms, compact presses, agricultural linkages — this space reclaim frequently justifies the higher unit cost and reduced field repairability of welded construction.
Construction Trade-Offs at a Glance
Welded cylinders cannot be resealed without specialist workshop equipment — the end caps must be cut off, seals replaced, and new weld beads applied and radiographically inspected on critical applications
For most continuous-process plant, the design life of a properly specified welded cylinder comfortably exceeds the expected service interval before reseal would be needed
Welded construction handles lateral and torsional loads that would overstress tie-rod assembly joints in applications involving eccentric loading or guide-less stroke operation
Core Materials: What Goes Into a 12-Inch Stroke Double-Acting Cylinder That Lasts
Technical Performance & Specification Parameter Table
| Paramètre | Tie-Rod Construction | Welded Construction |
|---|---|---|
| Longueur de la course | 12 in / 305 mm (standard) | 12 in / 305 mm (standard) |
| Working Pressure (max) | 2,000–3,000 PSI (138–207 bar) | 3,000–5,000 PSI (207–345 bar) |
| Bore Size Range | 1.5 in – 8 in (NFPA standard) | 1.0 in – 24 in (custom bore) |
| Rod Diameter (12 in stroke) | 0.625 in – 3.5 in (standard) | 0.75 in – 5 in (custom) |
| Matériau du fût | ST52 seamless tube / 316L option | ST52 / S355J2 / 316L option |
| Rod Surface Finish | Chrome-plated, Ra ≤ 0.4 µm | Chrome / induction-hardened, Ra ≤ 0.3 µm |
| Température de fonctionnement | -25°C to +80°C (standard PU) | -40°C to +120°C (FKM option) |
| Amortissement | Adjustable both ends (optional) | Fixed or adjustable both ends |
| Options de montage | NFPA flange, side lug, foot, clevis | Clevis, flange, trunnion, custom |
| Side Load Resistance | Low–Moderate (guide recommended) | High (integral structural body) |
| Field Repairability | High (hand tools, standard seals) | Low (workshop weld re-work) |
| Typical Application | Industrial presses, automation, maintenance | Mobile plant, mining, heavy press, OEM |
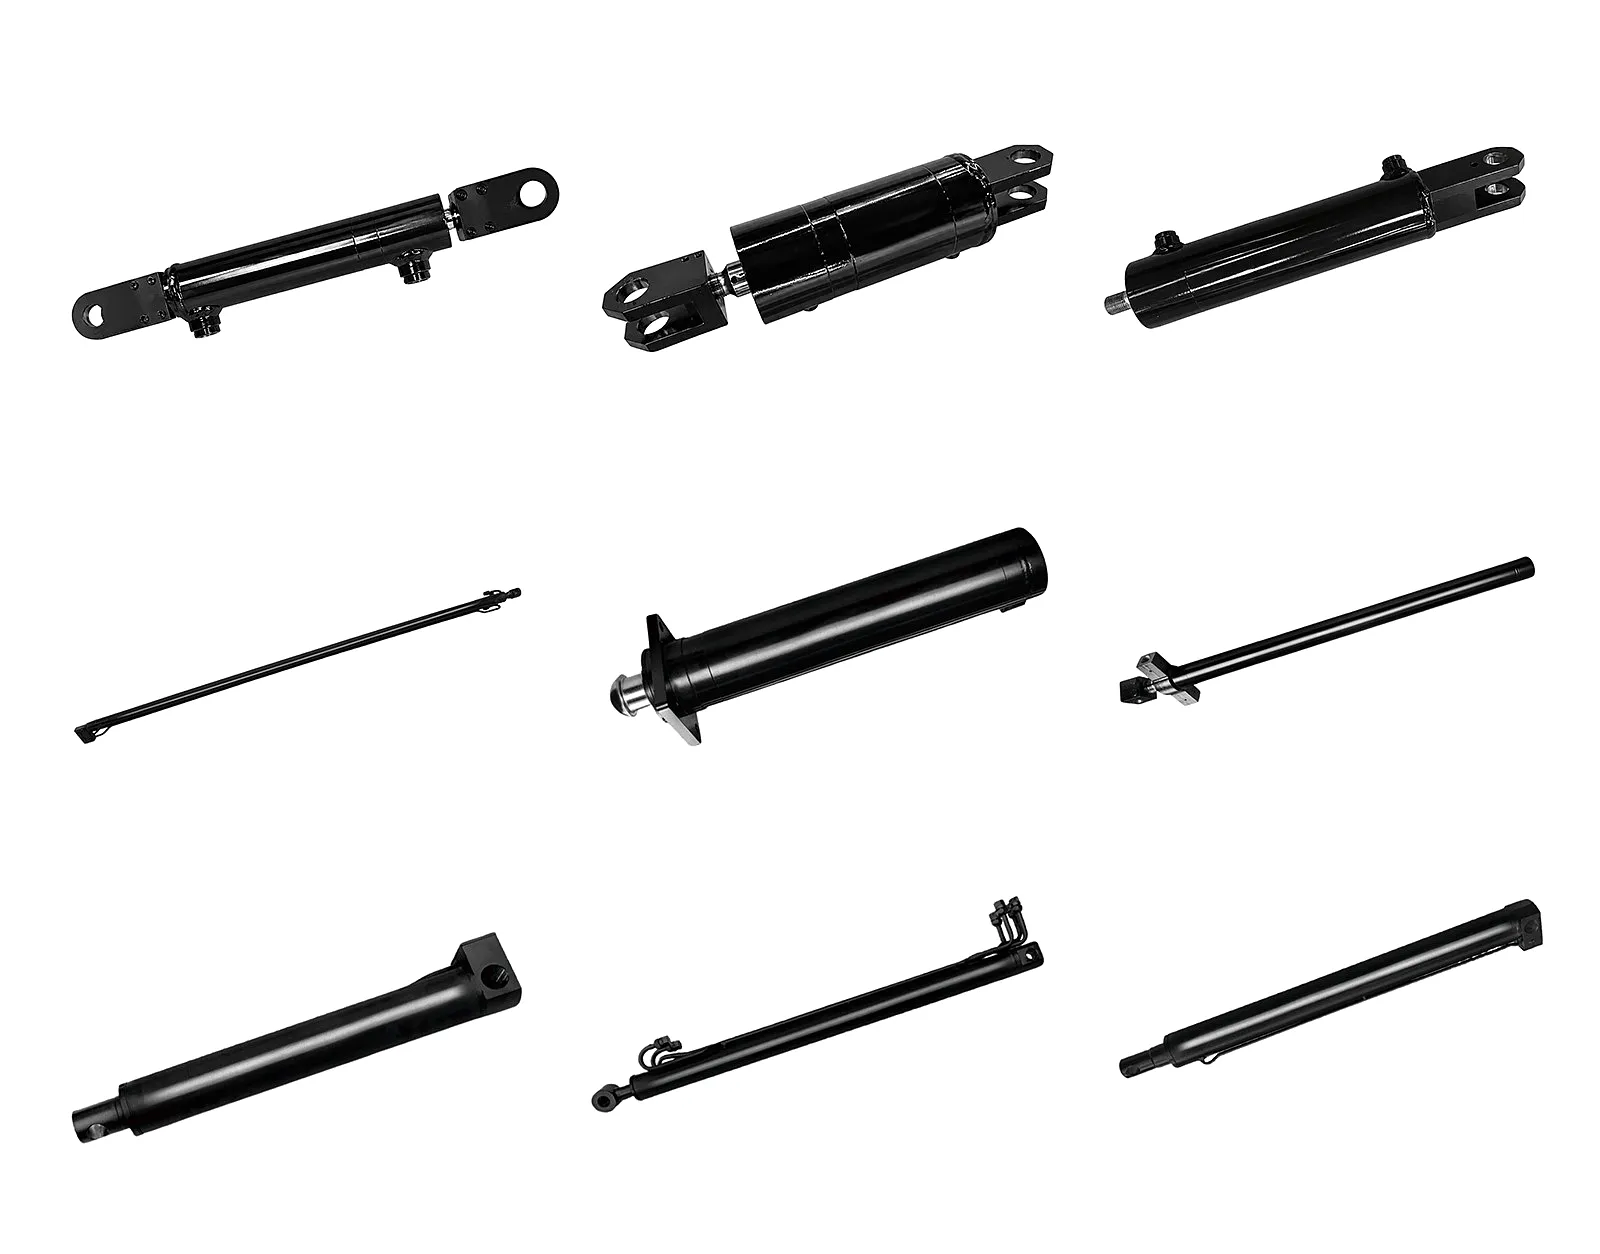
Industrial Application Scenarios: Where a 12-Inch Stroke Double-Acting Cylinder Works Hardest
Hydraulic Press & Forming Applications — Sheffield & Midlands Fabrication
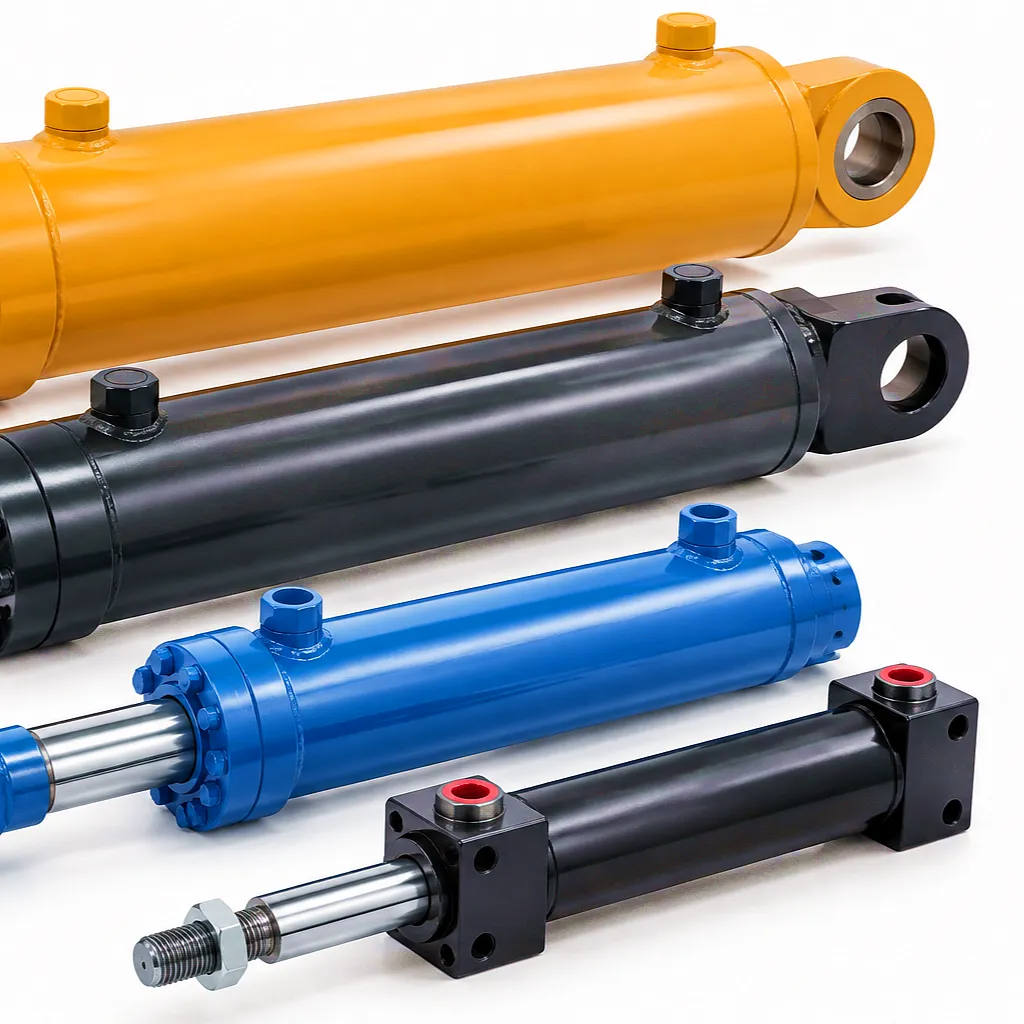 In metal pressing and forming operations — from structural steel fabrication yards in Sheffield to aluminium die-casting facilities across the West Midlands — a 12-inch stroke double-acting hydraulic cylinder provides the controlled, bidirectional force profile that mechanical eccentric presses cannot easily deliver. The full 305 mm of usable stroke accommodates die opening heights from deep-draw tooling, while the double-acting arrangement allows active extraction (stripping) force to be applied on the return stroke, removing formed parts from the die without mechanical strippers or springs that add cycle time and create alignment challenges. Tie-rod construction dominates this segment because seal replacement during scheduled maintenance shutdowns is a standard expectation. Ever Power supplies cylinders for this sector with optional magnetic position sensors integrated directly into the barrel for closed-loop press control.
Boom & Arm Actuation on Compact Excavators and Material Handlers
Compact excavators operating on infrastructure and utility projects across the UK — from urban drainage works in London to water main replacement in rural Northumberland — increasingly specify 12-inch stroke welded double-acting cylinders on boom and arm circuits. The welded design provides the structural stiffness to handle the combined bending and compressive loads generated when the bucket engages hard-packed ground, while the compact outer profile keeps within the tight envelope constraints of sub-5-tonne machines. Welded hydraulic cylinder construction also handles the shock-loading events from rock strikes and frozen ground penetration better than tie-rod alternatives, where repeated impact can work-loosen tie-rod pre-load over time. These cylinders are typically designed to operate at 3,200–4,200 PSI with cushioning at both ends to protect hydraulic pump components from pressure spikes at end of stroke.
Automated Assembly Line Clamping — Automotive Tier 1 Suppliers, Birmingham
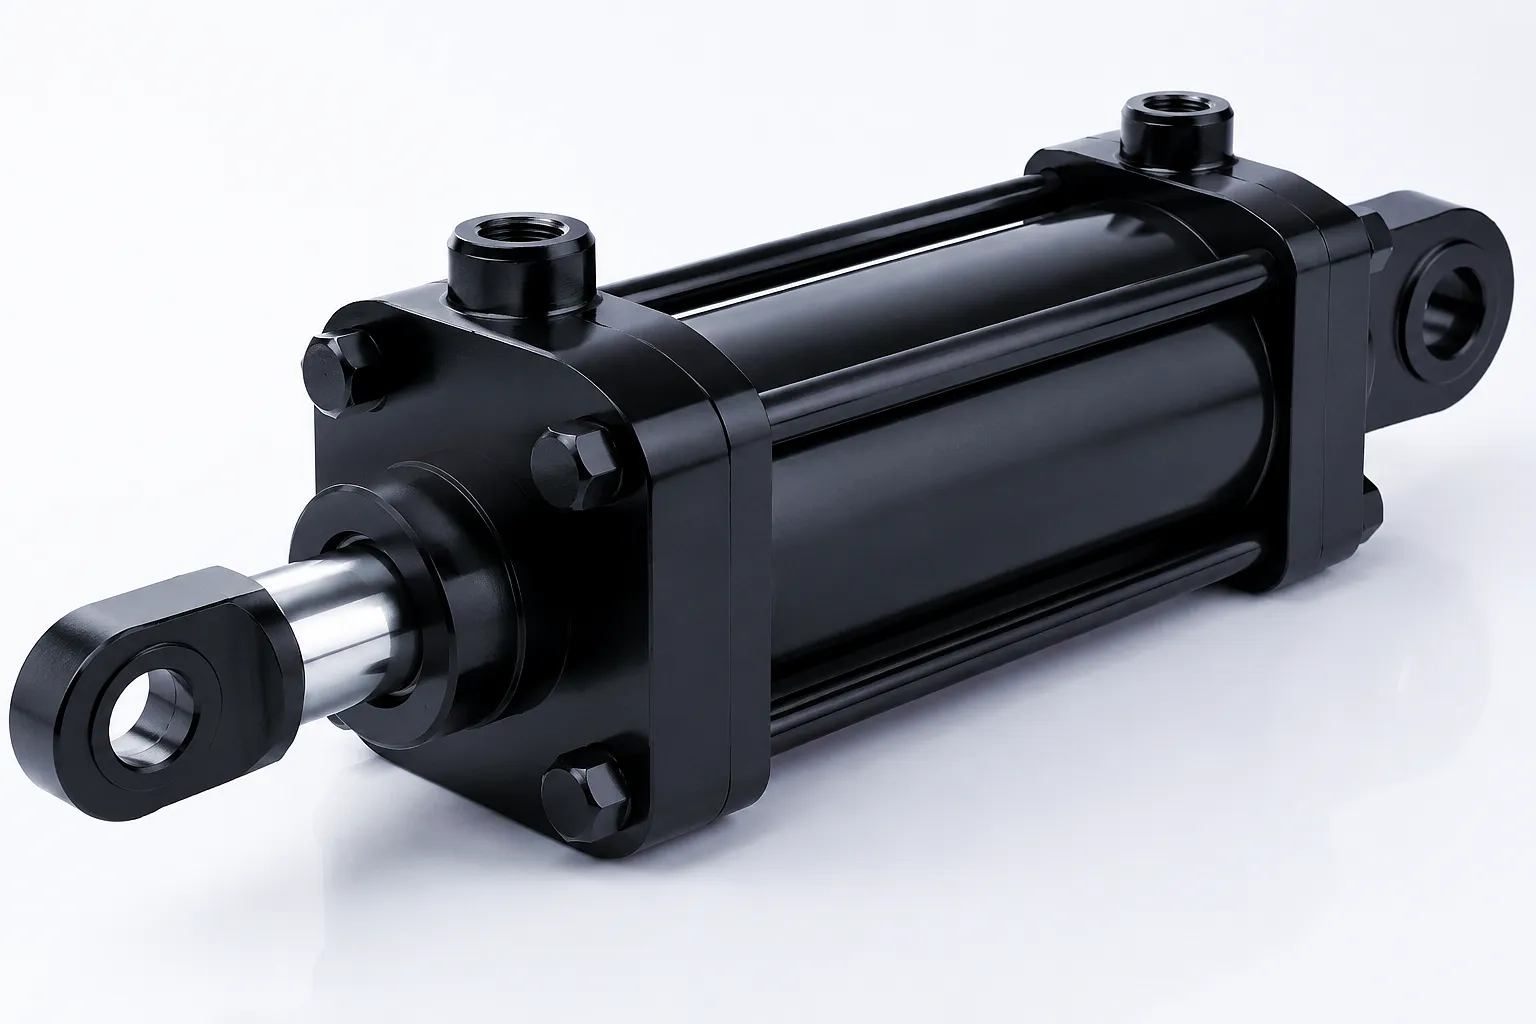 Automotive Tier 1 component manufacturers in Birmingham and Solihull operate high-cycle robotic welding and assembly lines where a 12-inch stroke double-acting cylinder may complete 5–12 million cycles per year in automated clamping stations. In this environment, cycle time consistency is as important as raw force output. The double-acting design delivers repeatable, fast retraction strokes without hydraulic intensification or spring delays, allowing part-to-part cycle times to be held within ±0.05 seconds. Tie-rod hydraulic cylinders dominate this segment because standard NFPA dimensions allow direct replacement during planned shutdown windows without machine re-engineering, and the seal kits are stocked by UK hydraulic service providers for next-day delivery. Position feedback via external LVDT or integrated magnetostrictive transducer is a standard specification requirement for modern closed-loop clamping applications.
Agricultural Implement Lifting & Folding — East Anglian Arable Farming
Modern wide-span agricultural implements — folding harrows, multi-section disc cultivators, seeder toolbar wings — used across the large arable fields of Lincolnshire, Norfolk and Cambridgeshire require cylinder folding circuits that can handle full implement weight on the retraction stroke, often against gravity and implement inertia simultaneously. A 12-inch stroke welded double-acting hydraulic cylinder handles this application well: the active return stroke provides controlled descent speed through a counterbalance valve arrangement, preventing implement drop if a hydraulic hose is damaged or a coupling is inadvertently disconnected. Agricultural operating environments demand specific seal compatibility with biodegradable hydraulic fluids increasingly mandated by UK environmental regulations for fieldwork near watercourses, and Ever Power supplies compatible seal formulations across its double-acting cylinder range on request.
Core Technical Advantages of the Double-Acting 12-Inch Stroke Design
Bidirectional Active Force
Unlike single-acting or spring-return designs, the double-acting configuration delivers controlled, measurable force in both extension and retraction. This means both work strokes are productive — critical in high-throughput pressing, clamping, and material handling where lost motion equals lost revenue.
Precision Velocity Control
Flow control valves on both port lines provide independent speed adjustment for extension and retraction strokes. The 12-inch stroke length gives a practical velocity range of 0.05 m/s to 0.6 m/s in typical industrial circuits — wide enough to serve both slow-speed precision positioning and fast-cycle automation without cylinder changes.
Load-Holding Without Energy Consumption
A double-acting cylinder stopped in mid-stroke with a closed-centre directional valve holds its position by trapping pressurised fluid in both chambers. No electrical power, no spring pre-load and no hydraulic pump flow is required to maintain position — particularly valuable in hold-down and clamping applications where parts must be secured during machining operations lasting several minutes.
Integrated Cushioning on 12-Inch Stroke
Adjustable hydraulic cushions at both end positions decelerate the piston and rod assembly in the final travel segment — typically the last 20–30 mm — preventing metal-to-metal impact. For high-cycle automated systems this is not optional: a 12-inch stroke cylinder without cushioning in a system cycling twice per minute will accumulate 1 million end-of-stroke impacts within 347 days of operation, generating impact forces that fatigue both the cylinder body and the machine structure.
Customer Success Story: Rotherham Steel Processing Facility
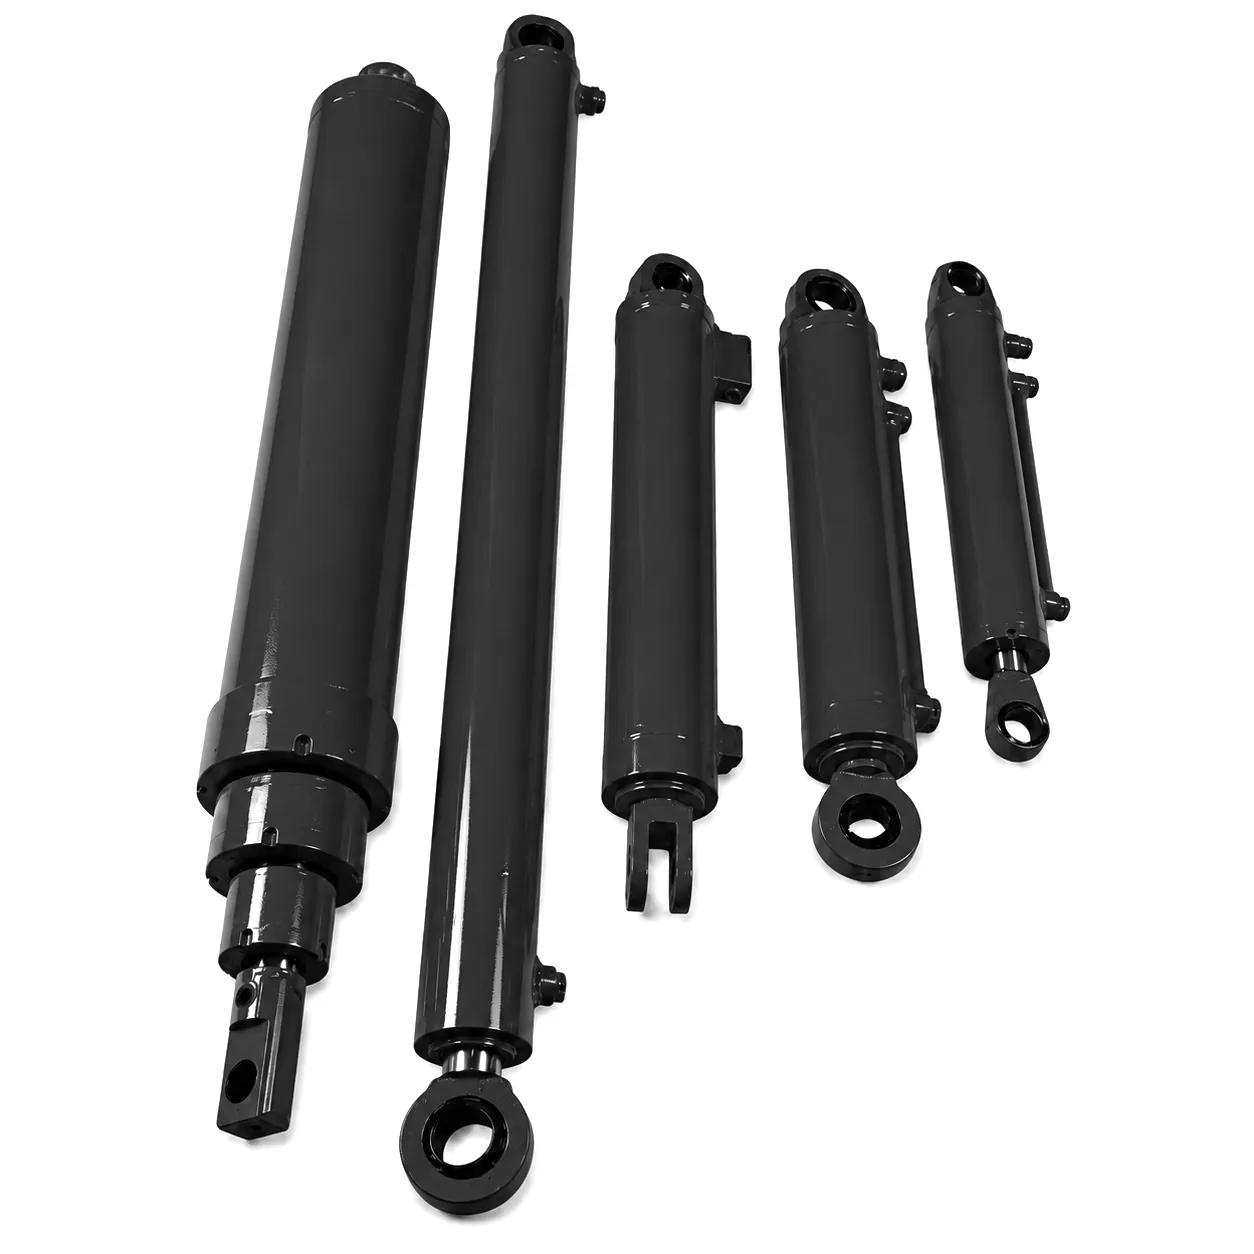 A hot-rolling mill in Rotherham operating a continuous strip processing line was experiencing chronic seal failures on the edge-guide hydraulic cylinders controlling coil width positioning. The existing tie-rod cylinders were rated to 2,500 PSI, but operating temperatures in the proximity of the rolling mill consistently reached 95–110°C during peak throughput — well beyond the rated service range of the standard polyurethane seals originally fitted. Seal failure intervals had dropped to 6–8 weeks, requiring mill stoppages that cost an estimated £18,000 per unplanned event in lost output, labour, and fluid cleanup.
Foire aux questions
What is the typical price or cost difference between a tie-rod and a welded double-acting hydraulic cylinder with a 12-inch stroke for UK industrial buyers?
For equivalent bore sizes, welded double-acting cylinders typically carry a unit price premium of 15–35% over NFPA-standard tie-rod equivalents, reflecting higher manufacturing complexity and the absence of interchangeable-component economies of scale. However, total cost of ownership calculations that include unplanned downtime costs, energy consumption from fluid leakage, and crane-time for cylinder change-outs often reverse this apparent differential — particularly in high-pressure or high-temperature environments where welded construction delivers meaningfully longer service intervals. For a UK site sourcing from Ever Power, indicative prices for a 3-inch bore, 12-inch stroke welded cylinder start from approximately £280–£420 ex-works depending on specification; tie-rod equivalents from £180–£260. Request a formal quote from [email protected] for your exact specification.
How do I find a reliable hydraulic cylinder supplier in the UK who can deliver a custom 12-inch stroke double-acting cylinder quickly for an urgent replacement?
For urgent cylinder replacements, the fastest route is typically to contact a UK hydraulic distributor who maintains stock of standard NFPA tie-rod units (1.5–4 inch bore, standard strokes) for same-day or next-day dispatch, while simultaneously requesting a custom-build quote from the original manufacturer for a permanent replacement if the failed cylinder was non-standard. Ever Power offers an expedited 10-day manufacturing track for welded double-acting cylinders for UK customers with urgent plant breakdown requirements. Email [email protected] with the failed cylinder’s nameplate data, bore, stroke, port sizes, and mounting configuration and the application team will respond with availability and lead time within one business day.
Which construction type — tie-rod or welded — should I choose for a Birmingham automotive press application running more than 5 million cycles per year at 2,500 PSI?
At 5 million cycles per year and 2,500 PSI, both construction types are technically viable, but the decisive factor is your maintenance model. If your Birmingham facility has scheduled downtime windows every 6–12 months where technicians can reseal cylinders in-situ, tie-rod construction provides lower unit cost and straightforward field repair using standard NFPA seal kits that UK hydraulic distributors stock locally. If your press runs continuous shifts with minimal planned downtime and cylinder failure has a high unplanned cost, welded construction — with FKM seal compounds and induction-hardened rod surfaces — typically delivers longer mean service intervals that justify the higher unit cost and workshop-repair requirement. Ever Power’s application team can assist with duty-cycle analysis and total-cost-of-ownership comparison if you provide cycle frequency, duty cycle percentage and fluid temperature data.
Where can I get a quote for a double-acting welded hydraulic cylinder that can handle high temperatures on a steel plant in Sheffield or Rotherham?
Contactez directement Ever Power au [email protected] en précisant l'alésage, la course (12 pouces ou autre), la pression de service, la température maximale du fluide hydraulique, la température ambiante au niveau du vérin, le type de montage et les spécifications des orifices (BSP ou SAE). Spécialisée dans les environnements sidérurgiques de Sheffield et Rotherham, Ever Power possède une expertise reconnue dans la spécification de composés d'étanchéité FKM, de revêtements de tiges par projection thermique céramique et de visserie externe en acier inoxydable. Ces solutions permettent de résister aux conditions extrêmes de température ambiante élevée, de chaleur rayonnée et de calamine, un environnement corrosif qui provoque la défaillance prématurée des vérins standard. Un devis standard inclut une proposition technique détaillée, accompagnée de plans cotés et d'un certificat de conformité.
Quelle est la durée de vie d'un vérin hydraulique à double effet de 12 pouces de course en utilisation industrielle intensive, et quand faut-il envisager son remplacement plutôt que son étanchéité ?
La durée de vie varie considérablement en fonction de la sévérité de l'utilisation, de la propreté du fluide et de la qualité des spécifications. Un vérin double effet correctement spécifié, utilisé dans un environnement industriel propre et à température contrôlée, avec 1 à 2 millions de cycles par an, peut avoir une durée de vie de 8 à 12 ans, voire plus, avant que l'usure du corps, la dégradation de la surface de la tige ou la fatigue structurelle ne nécessitent son remplacement. Dans des environnements agressifs (haute température, fluide contaminé ou applications soumises à des chocs), cette durée peut être réduite à 3 à 5 ans. Le choix entre une réparation et un remplacement dépend de l'usure de l'alésage du corps (généralement réparable de manière économique en dessous de 0,1% du diamètre nominal), de l'état du chromage de la tige (une piqûre de plus de 0,05 mm de profondeur justifie généralement son remplacement) et de l'état structurel du corps du vérin et des soudures du bouchon. Ever Power peut fournir un rapport d'inspection pour les vérins retournés si vous hésitez sur la solution la plus économique.
Quelles sont les dimensions d'alésage standard disponibles pour un vérin hydraulique double effet à course de 12 pouces, et Ever Power peut-il fournir des dimensions d'alésage non standard pour une application OEM britannique sur mesure ?
Pour les tirants, les alésages conformes à la norme NFPA (course de 12 pouces) sont disponibles dans des diamètres allant de 1,5 à 8 pouces par incréments standard (1,5, 2, 2,5, 3, 3,5, 4, 5, 6, 7, 7, 8 et 8 pouces). Pour les constructions soudées, Ever Power fabrique des alésages sur mesure de 25 mm à 600 mm, y compris les dimensions métriques privilégiées par les équipementiers européens. Pour les équipementiers britanniques développant de nouvelles gammes de produits avec des rapports alésage/course spécifiques, dictés par des contraintes d'espace ou des exigences de force se situant entre les dimensions standard, les ingénieurs d'application d'Ever Power analyseront le projet et fourniront, sur demande, un cahier des charges d'alésage personnalisé, incluant les frais d'outillage (le cas échéant) et le prix unitaire. La quantité minimale de commande pour les alésages sur mesure est généralement de 5 unités pour les premiers lots de prototypes.
Ever Power — Spécialistes des vérins hydrauliques
Spécifiez votre cylindre à course de 12 pouces dès aujourd'hui
À tirants ou soudé, standard ou entièrement personnalisé — notre équipe d'ingénierie d'application travaille avec vos exigences dimensionnelles et de service pour spécifier le vérin hydraulique à double effet adapté à votre application.
✉ Demandez un devis — [email protected]
édité par gzl
 French
 English
 Italian
 Portuguese
 Dutch
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 Greek