HYDRAULIC SYSTEMS · STORAGE ENGINEERING · CORROSION PROTECTION

How to Store Hydraulic Cylinders: Preventing Corrosion During Long-Term Storage

A practical engineering guide for UK manufacturing and heavy industry — covering proven storage methods, corrosion prevention protocols, and the standards that protect your hydraulic cylinder investment across months or years of inactivity.

Get a Free Quote →

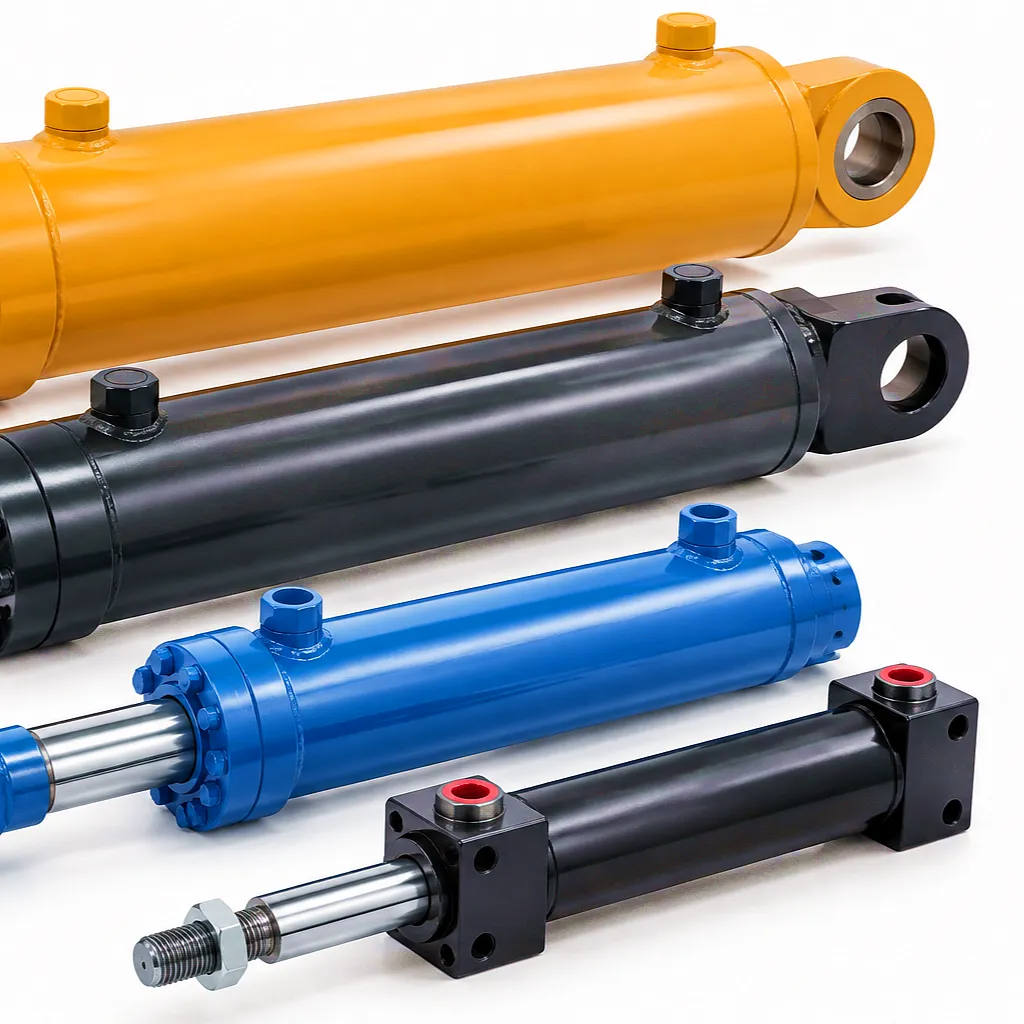
Przyczyny uszkodzenia tłoczyska siłownika hydraulicznegoWalk through any warehouse in Sheffield, Birmingham, or along the industrial corridors of the Midlands, and you will find hydraulic cylinders sitting in inventory for weeks, months, or sometimes years between project cycles. These components represent a significant capital commitment — precision-machined chrome rods, hardened steel barrels, and high-specification sealing systems that must perform flawlessly the moment they are called back into service. The challenge is straightforward but routinely underestimated: a hydraulic cylinder that looks intact on the outside can carry invisible corrosion damage that renders it unreliable or entirely inoperable once reinstalled.

Corrosion is not simply a surface problem. Pitting on a chrome-plated rod creates a scoring path that destroys rod seals within hours of pressurised operation. Rust inside the barrel increases particulate contamination in the hydraulic fluid, accelerating wear across the entire circuit. Degraded end-cap seals allow moisture ingress that promotes internal oxidation of the piston and cylinder walls. Understanding how corrosion initiates and progresses during storage is the starting point for any effective prevention strategy — and this guide gives you the full technical picture, from preparation and environmental controls through to reinspection protocols before return to service.

Need hydraulic cylinders with long-term corrosion protection built in from the factory?

Uzyskaj wycenę

Why Hydraulic Cylinders Corrode in Storage

🌡️
Temperature Cycling

UK warehouses and outdoor storage yards experience significant daily and seasonal temperature swings. When a hydraulic cylinder cools overnight, the air trapped inside the barrel contracts, drawing in ambient air through imperfect seals. As temperatures rise again, that moisture-laden air deposits condensation directly onto internal metal surfaces. This thermal pumping effect — cycling through hundreds of warm-cool-warm events over a single winter — generates far more internal moisture exposure than most engineers anticipate. Steel that would be stable for years in a controlled environment can show visible rust within a few months under these conditions.

💧
Residual Hydraulic Fluid

Hydraulic fluid left inside a cylinder during storage is a double-edged asset. Fresh, well-maintained mineral oil provides a protective film on internal surfaces — but degraded fluid, or fluid that has absorbed water during service, becomes actively corrosive. Water-contaminated hydraulic oil forms acidic compounds that attack both steel and aluminium alloy components. Cylinders removed from plant equipment should always be drained, flushed with clean preservative oil, and refilled before storage. Leaving service fluid in place without testing its condition is one of the most common and most damaging storage errors made across UK industrial workshops.

🌬️
Exposed Rod Surface

The chrome-plated piston rod is the most visible and most vulnerable component during storage. Chrome plating provides excellent corrosion resistance under dynamic operating conditions — the rod is continuously lubricated by the wiper seal — but in static storage, any area of exposed rod that protrudes beyond the rod seal is at the mercy of ambient humidity and airborne contaminants. Near coastal or industrial areas of the UK, such as those around Bristol, Teesside, or the Humber estuary, salt-laden or chemically active air can initiate corrosion on unprotected chrome within days. Even micro-pitting invisible to the naked eye compromises the sealing surface for the working life of the cylinder.

Pre-Storage Preparation: The Correct Procedure

No storage method is effective without proper preparation before the cylinder goes on the shelf. The preparation sequence is not a checklist of optional extras — it is a systematic engineering process that determines the condition of the cylinder when it returns to service. Hydraulic cylinders that have been correctly prepared before long-term storage can remain in fully serviceable condition for 18 to 36 months without any intermediate intervention. Cylinders that go into storage in service condition — ports open, rod exposed, fluid unchecked — can show significant corrosion damage within 90 days, particularly in UK storage environments where ambient humidity regularly exceeds 70% RH from autumn through spring.

1
External Cleaning

Remove all contamination from the external barrel, end caps, and rod using a non-corrosive degreasing agent. Pay particular attention to port threads and seal grooves. Any trapped mud, cutting fluid, or industrial residue left on the surface will hold moisture against the metal and accelerate localised corrosion during storage.

2
Fluid Drain and Flush

Drain all service hydraulic fluid and test it for water content before proceeding. If water content exceeds 500 ppm or the acid number is elevated, the fluid must be replaced. Flush the internal chamber with clean, fresh mineral oil (ISO VG 46 or 68 grade) until effluent runs clear. This removes acid degradation products and suspended particles that would otherwise remain in contact with internal surfaces throughout storage.

3
Preservative Oil Fill

After flushing, fill the cylinder completely with a storage-grade preservative oil. Specialist hydraulic preservation fluids contain vapour-phase corrosion inhibitors (VCI additives) that protect surfaces not directly wetted by the oil film. Fill to 100% of internal volume to eliminate the air gap that would otherwise allow condensation. Ensure the cylinder is positioned horizontally and rotated 90 degrees every 4 to 6 months to redistribute the preservative coating across all internal surfaces.

4
Rod Protection

Retract the piston rod to its fully retracted position before storage — this minimises the rod surface area exposed beyond the rod seal. Coat all exposed chrome rod surface with a thin layer of VCI-impregnated grease or a specialist wax-based rod preservation compound. Do not use petroleum jelly (Vaseline) as a long-term coating: it degrades, absorbs moisture, and can contaminate the hydraulic system when the cylinder returns to service.

5
Port Sealing

Install solid plastic or metal port plugs in every hydraulic port — both pressure and return side. Plastic dust caps are inadequate for long-term storage: they permit air movement. Solid plugs maintain the internal pressure of the preservative fill and prevent atmospheric moisture from bypassing the plugs through thread gaps. Label each plug with the port size and thread specification so they can be correctly replaced with matching hydraulic fittings when the cylinder is returned to service.

Storage Environment Requirements

The storage environment is as important as the preparation of the cylinder itself. Even a perfectly prepared hydraulic cylinder will suffer degradation if placed in an unsuitable environment. Across Birmingham’s manufacturing belt, Sheffield’s steel fabrication yards, and the logistics hubs around Leeds and Manchester, storage conditions vary enormously — from temperature-controlled warehouse bays to open outdoor storage compounds where cylinders are left stacked on pallets exposed to the elements. Understanding what each environment does to a stored cylinder is essential for making the right storage decisions.

🌡️ Temperature Range

Ideal storage temperature for hydraulic cylinders is between +5°C and +25°C. Below 0°C, trapped water in seals or residual fluid can expand on freezing, damaging seal lips and cracking polyurethane components. Above 35°C sustained, elastomeric seals begin to harden and lose recovery — a process that is not reversed when temperatures normalise. UK climate is generally within range, but outdoor or uninsulated storage in January in northern England regularly breaches the lower threshold.

💧 Relative Humidity

Relative humidity must be maintained below 60% RH for corrosion risk to remain low. Above 70% RH, condensation becomes active on metal surfaces whenever temperature fluctuates. Above 85% RH — a common condition in unventilated UK storage sheds during winter — even well-prepared cylinders with coated rod surfaces can develop surface corrosion within 60 days if any preparation step was incomplete. Installing dehumidifiers rated for the storage volume is strongly recommended for any facility storing more than 10 cylinders over a period exceeding 90 days.

📦 Physical Positioning

Hydraulic cylinders must be stored horizontally on padded racking — never vertically with the rod facing down, which causes preservative oil to drain away from the rod seal area, and never standing upright on their end caps, which concentrates load stress on gland threads. Horizontal storage keeps the preservative fluid evenly distributed across internal surfaces. Padding the contact points with rubber or HDPE blocks prevents the barrel from developing flat spots, particularly on thinner-wall cylinders used in mobile plant applications.

🔒 Wrapping and Covering

Wrap each cylinder individually in VCI (Vapour Corrosion Inhibitor) poly film before placing it in storage. VCI film emits a chemical vapour that forms a monomolecular protective layer on metal surfaces within the enclosed space, providing ongoing corrosion protection even against moisture that penetrates the external packaging. Do not use standard polythene sheeting as a substitute — it traps moisture rather than controlling it, creating a warm, humid microenvironment that accelerates corrosion instead of preventing it.
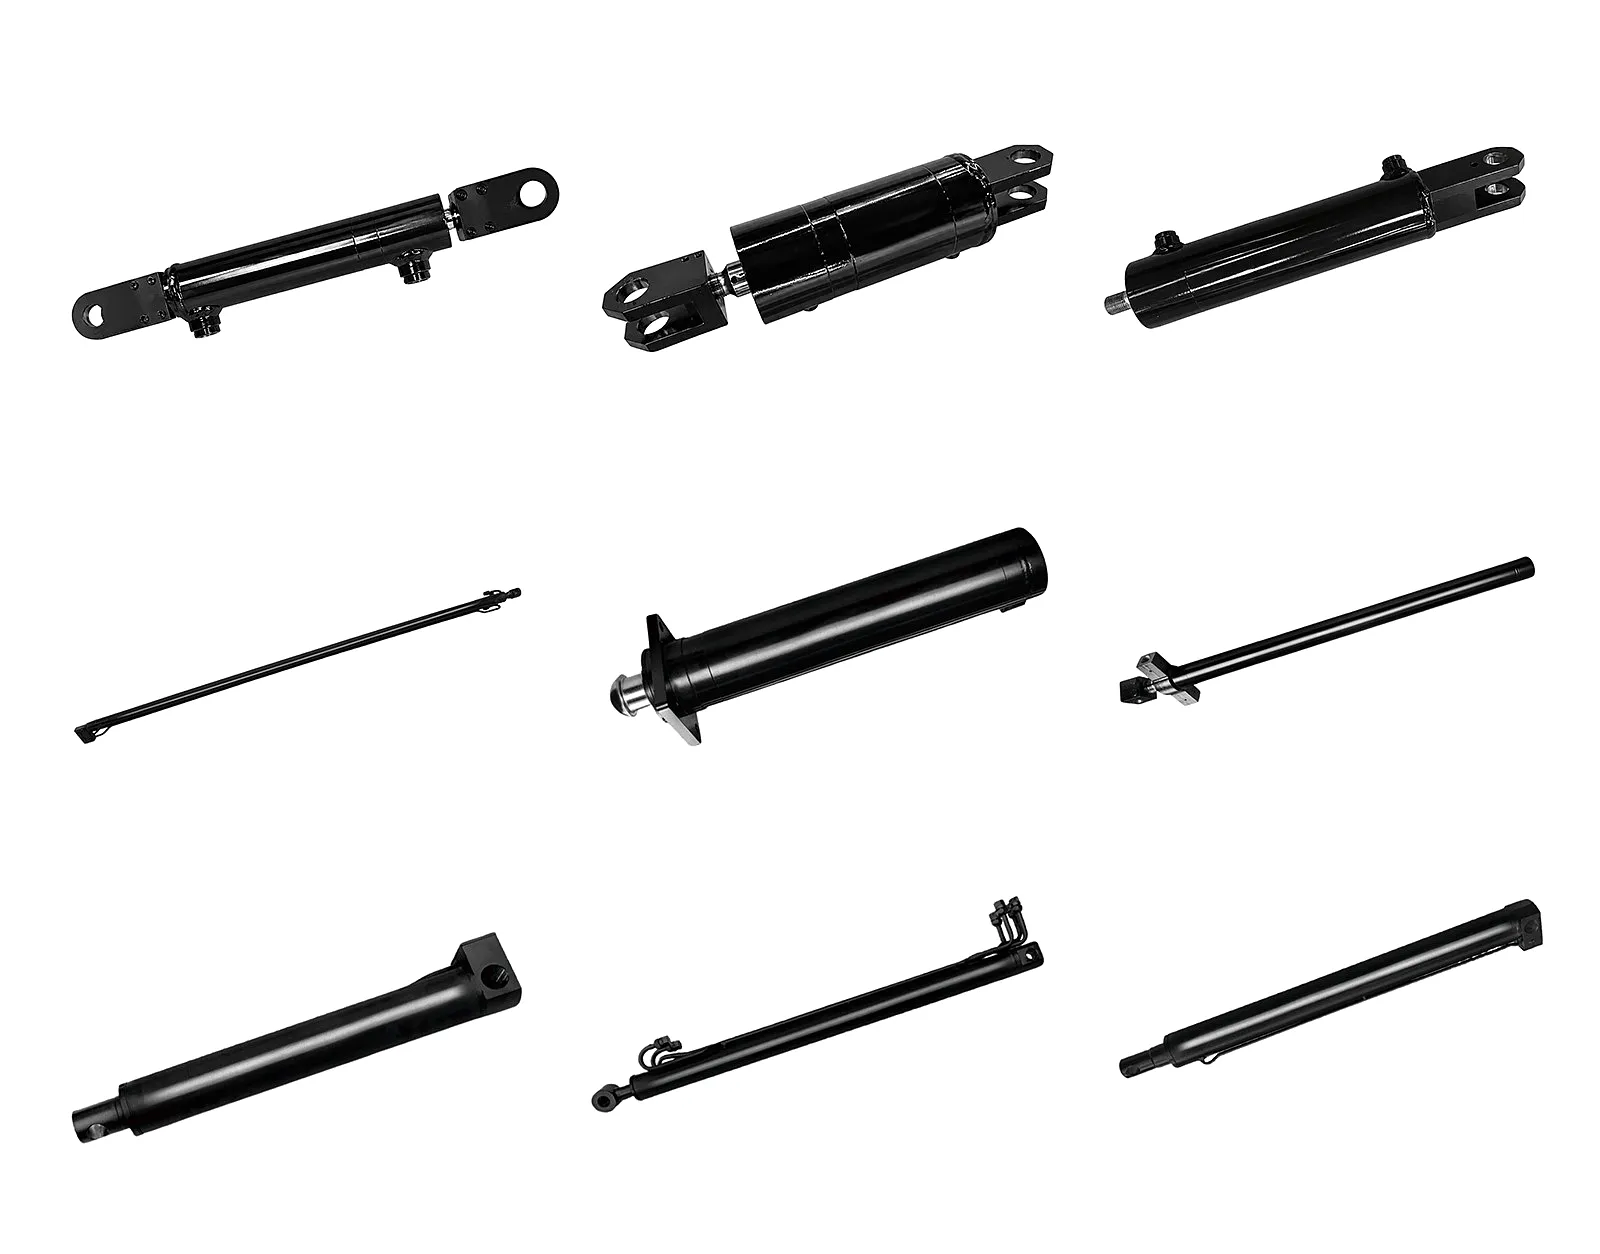
Asortyment produktów cylindrów hydraulicznych Ever Power

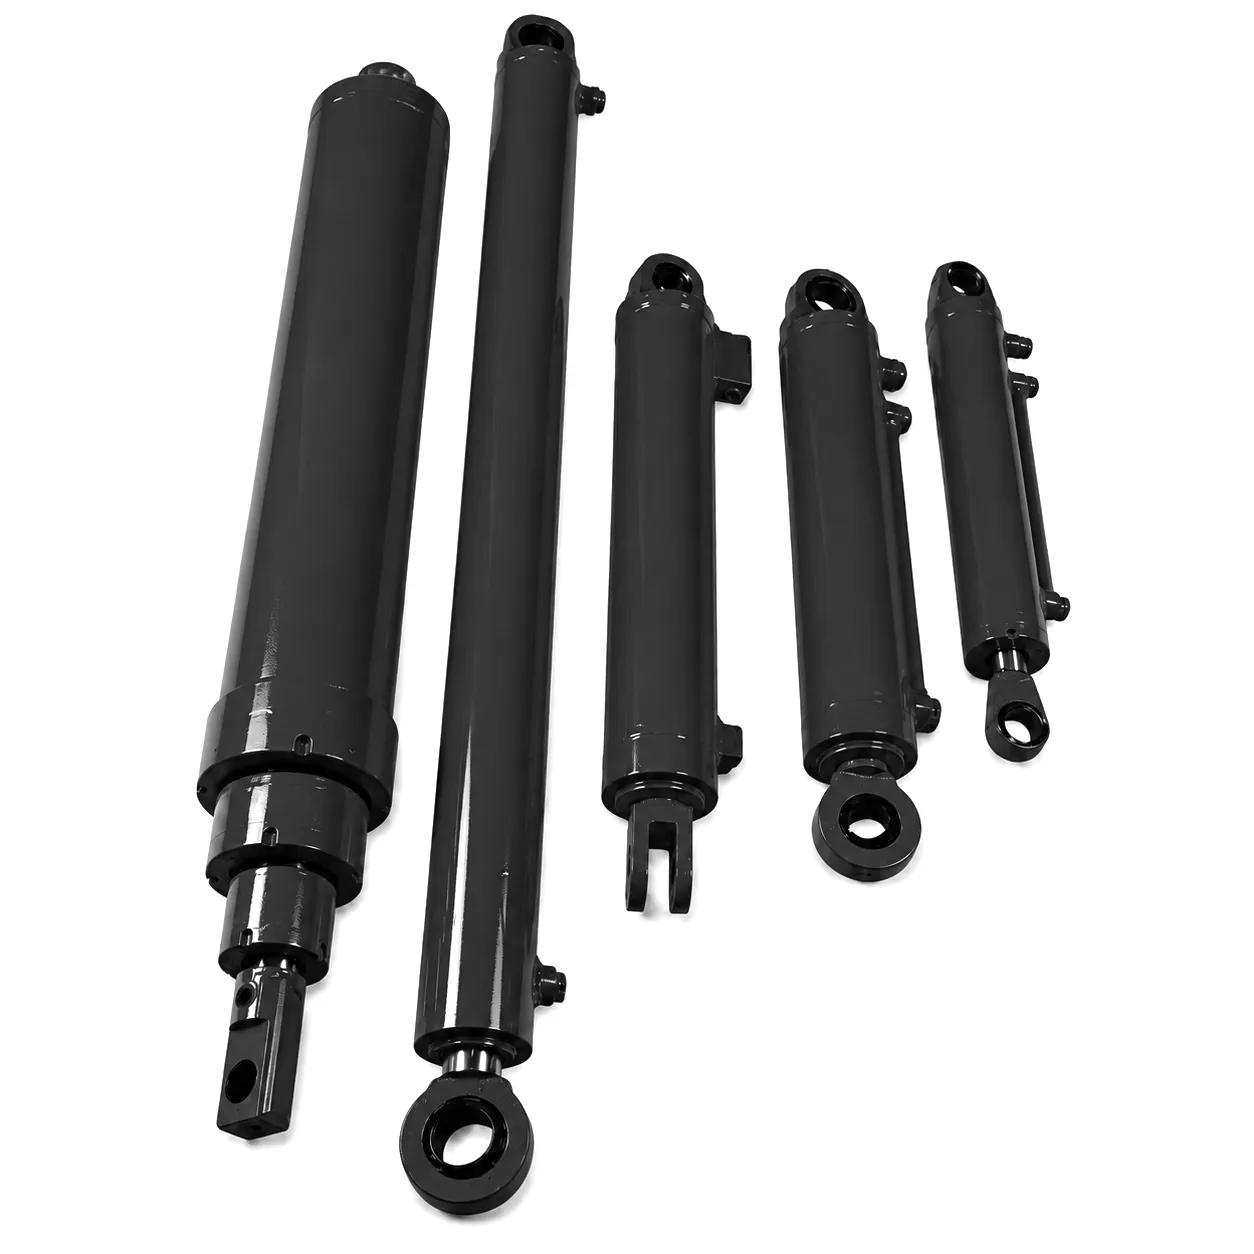
Ever Power hydraulic cylinder product range — engineered for demanding UK industrial applications

Hydraulic Cylinder Storage Parameters — Technical Reference Table

The table below consolidates the key storage parameters, material compatibility data, and performance thresholds for hydraulic cylinders in long-term UK storage conditions. These figures are based on engineering standards including BS EN ISO 4413 (Hydraulic Fluid Power — General Rules), internal testing from major cylinder manufacturers, and operational data from UK plant hire and heavy industry sectors. Use these values as minimum benchmarks for your own storage procedure documentation.

Parametr Short-Term (0–3 months) Medium-Term (3–12 months) Long-Term (12–36 months)
Storage Temperature 0°C to +35°C +5°C to +25°C +10°C to +20°C (controlled)
Max Relative Humidity ≤ 75% RH ≤ 60% RH ≤ 50% RH (dehumidified)
Internal Fluid Service oil if tested clean Preservation oil (VCI additive) Dedicated hydraulic preservation fluid, full fill
Rod Coating Light VCI grease layer VCI wax compound, 0.2–0.5 mm film Heavy wax preservation + VCI poly wrap
Port Plugs Plastic dust caps acceptable Solid steel or brass plugs Solid plugs + PTFE thread tape seal
Inspection Interval Visual check on receipt Every 90 days Every 60 days; fluid test every 6 months
Seal Material Limits PU: to -10°C; NBR: to -20°C PTFE/HNBR preferred HNBR or FKM for best shelf stability
Chrome Rod Hardness Maintained: 850–1000 HV Maintained if correctly coated Verify on recommission; min 800 HV
Cylinder Rotation Not required 90° rotation every 6 months 90° rotation every 4 months
Opakowanie Standard poly wrap VCI poly film VCI film + sealed VCI bag + moisture indicator

Industrial Storage Scenarios: Where These Guidelines Apply

These hydraulic cylinder storage protocols are not theoretical — they apply directly to real-world industrial operations across the UK where cylinders routinely spend extended periods in inventory. The specific challenges and risk factors differ between industry sectors, and understanding those differences allows procurement and maintenance teams to tailor their storage procedures accordingly.
🚜
Agricultural Machinery — East Anglia and the East Midlands

Combine harvesters, balers, and tractor-mounted implements use hydraulic cylinders that are entirely idle during the winter off-season — typically October through March in UK arable operations. These cylinders have been operating in some of the most contaminating conditions possible: crop debris, fertiliser dust, and rain exposure throughout the harvest season. Before winter storage, each cylinder should be removed from the machine, inspected for seal condition, rod scoring, and port thread damage, and then prepared for storage using the full preservative fill and rod coating procedure.

Agricultural machinery operators in Lincolnshire and Norfolk frequently discover that cylinders stored in unheated farm buildings without preparation require seal replacement every two seasons rather than every five — a direct consequence of inadequate storage practice and a significant maintenance cost that is entirely preventable. See our Hydraulic Cylinders for Combine Harvester Machines to understand the specification requirements for agricultural applications.

🏗️
Construction Plant Hire — Birmingham and the West Midlands

Plant hire companies hold hydraulic cylinder inventory — both as spare components and as part of machines awaiting deployment — across large depots serving construction projects in Birmingham, Coventry, and Wolverhampton. The unique challenge in plant hire is the uncertainty of deployment timing: a cylinder placed in store as a three-month contingency spare may remain unused for 18 months or more if the project for which it was ordered is delayed or cancelled. Storage procedures must therefore default to the most conservative long-term approach from day one, rather than being upgraded retrospectively when the storage period extends beyond initial expectations.

Boom cylinders — the primary hydraulic cylinders in excavator and telehandler boom arms — are the highest-value and most frequently stored cylinder type in the West Midlands plant hire sector. Their large bore diameters (often 80 mm to 160 mm) and long stroke lengths make preservative fill management particularly important.

🔼
Lifting Platform Manufacturing — Sheffield and South Yorkshire

Manufacturers of scissor lifts, vehicle hoists, and industrial lifting platforms in Sheffield and the surrounding South Yorkshire manufacturing corridor hold hydraulic cylinder inventory as production buffer stock. Lead times for custom-bore telescopic cylinders can extend to 12–16 weeks, making buffer stock a commercial necessity. These cylinders typically sit in a temperature-variable factory stores environment for 4 to 8 months before assembly, a period long enough to cause significant corrosion to unprotected internal surfaces or exposed rod sections.

Telescopic cylinder designs present additional challenges for long-term storage: the multiple inner stages must be fully retracted and individually coated before the assembly is sealed. Our range of Custom Double Acting Telescopic Hydraulic Cylinders for Lifting Platforms are supplied with factory storage treatment included as standard when ordered for buffer inventory.

⚓
Offshore and Port Equipment — Aberdeen, Liverpool and Humber

Port handling equipment in Liverpool and Immingham, and offshore support vessels operating out of Aberdeen, use large-format hydraulic cylinders in crane systems, hatch actuators, and stabiliser equipment. These cylinders face the most aggressive storage environment of any UK industrial sector: coastal salt air creates a chloride-rich atmosphere that strips unprotected chrome plating and initiates galvanic corrosion at every metal-to-metal contact point within weeks. Storage in portside sheds without humidity control is effectively equivalent to outdoor storage in terms of corrosion risk.

For offshore-specification cylinders — typically featuring stainless steel rod, hard anodised aluminium components, or nickel-chrome composite plating — the standard storage protocols in this guide apply with enhanced sealing and a shortened inspection interval of 45 days.

Ever Power: Factory Preparation and Storage Solutions

Zakład produkcyjny cylindrów hydraulicznych Ever Power

At Ever Power, every hydraulic cylinder supplied to UK customers is prepared to a factory storage standard that goes significantly beyond what is typically offered in the industry. Our preparation process begins on the production line: chrome rods are ground and polished to a surface finish of Ra 0.2 µm or better before plating, creating a dense, low-porosity chrome layer that provides inherently superior corrosion resistance compared to standard-finish rods. End caps are machined to tighter tolerances, and seal glands are dimensioned to eliminate the micro-gaps that allow atmospheric moisture ingress through port plug interfaces.

🔧 Custom Bore and Stroke

Ever Power manufactures cylinders to any bore diameter from 20 mm through 500 mm, and stroke lengths from 50 mm to over 6,000 mm for special applications. All custom specifications are documented for future batch matching when replacement or additional cylinders are required.

🧪 Material Options

Barrel materials range from ST52 carbon steel through S355 structural steel to 316L stainless steel for corrosive environments. Rod options include 42CrMo4 alloy steel (standard), stainless steel (AISI 304/316), and Inconel for extreme temperature applications. Seal kits are available in NBR, HNBR, PTFE, and FKM grades.

📋 Storage Certification

Each cylinder is shipped with a factory storage certificate documenting the preservative fluid specification, fill date, port plug sizes, and recommended inspection schedule. This certificate provides the receiving facility with a complete starting record for their own storage management procedure.

🚢 UK Logistics

Ever Power ships directly to UK mainland destinations via consolidated freight from our manufacturing facility, with transit packaging designed to maintain storage integrity throughout the logistics chain. Customs documentation and CE/UKCA compliance declarations are provided as standard for all exports to UK customers.

Request a Custom Storage-Ready Cylinder Specification

Tell us your bore, stroke, pressure rating, and storage duration — our engineering team will provide a full specification with factory storage treatment included and a competitive price for UK delivery.

Uzyskaj wycenę →

Recommissioning After Long-Term Storage
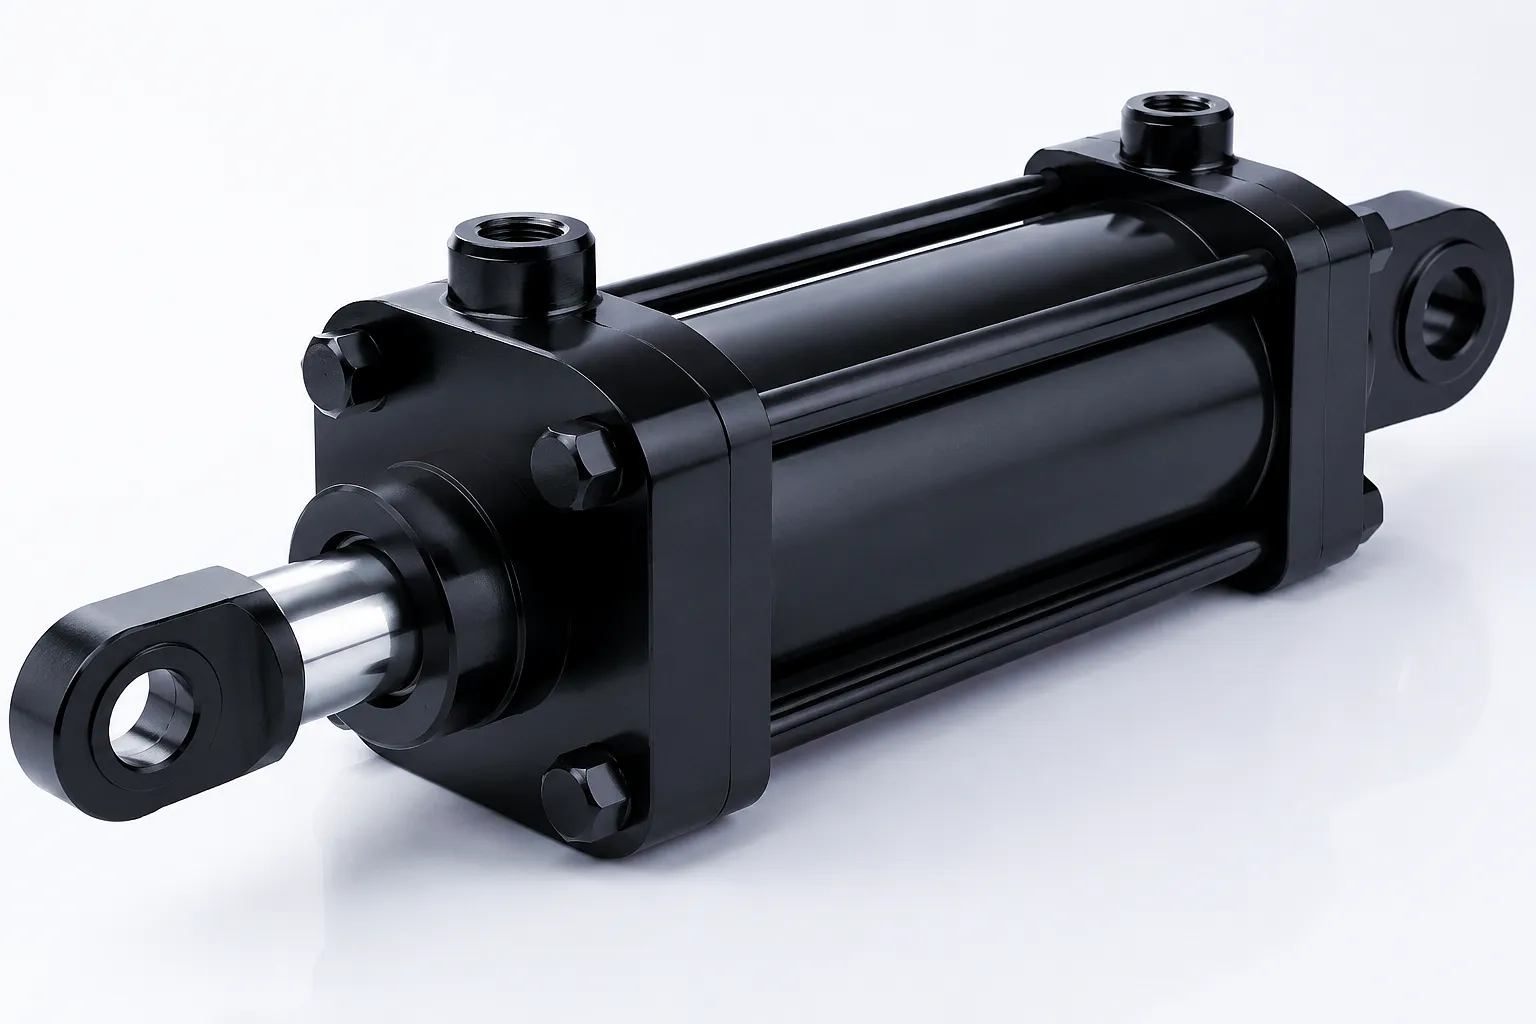
Proces kontroli i ponownego uruchomienia cylindra hydraulicznego

Recommissioning a hydraulic cylinder from long-term storage requires a structured inspection and preparation sequence before the cylinder is installed in the machine. The purpose of this sequence is to verify that the storage period has not compromised any component, and to prepare the cylinder for the transition from its preservation state to operational hydraulic service. Skipping this process and installing a stored cylinder directly is a false economy: an unverified cylinder that fails in service costs many times more in downtime and repair than the 30–60 minutes required for a thorough recommissioning inspection.

External Visual Inspection

Check the entire external surface for corrosion, impact damage, and seal condition. Inspect the chrome rod surface under direct light for pitting, scoring, or corrosion spots. Any visible pitting larger than 0.2 mm diameter or deeper than 0.1 mm on the sealing zone of the rod is cause for rejection — the rod must be re-plated or the cylinder returned for refurbishment before installation.

Preservative Fluid Removal

Drain and collect all preservative fluid for disposal or analysis. If the preservation fluid has emulsified, shows visible discolouration, or tests positive for elevated water content, the internal surfaces should be flushed with clean mineral oil before service fluid is added. Do not discharge preservative hydraulic fluid to drain — dispose of it in accordance with EA (Environment Agency) waste oil regulations applicable in England.

Seal Integrity Test

Before full installation, conduct a bench pressure test at 1.5 times the rated working pressure, held for 5 minutes with no visible external leakage or pressure drop exceeding 2%. This test verifies that the rod and port seals have retained their elasticity and dimensional integrity through the storage period. Cylinders that fail the pressure test should be fully stripped for seal inspection — the seals may require replacement even if the storage conditions appeared correct.

Początkowy cykl docierania

Po montażu należy wykonać 10–15 cykli powolnego suwu przy maksymalnym ciśnieniu roboczym 30–40%, zanim cylinder osiągnie pełne obciążenie robocze. Ta procedura docierania redystrybuuje smarowanie uszczelnienia, usuwa resztki powietrza z układu i umożliwia ponowne dopasowanie się wargi uszczelnienia do powierzchni tłoczyska po zestaleniu statycznym, które nieuchronnie występuje podczas długotrwałego przechowywania. Monitorować pełzanie, dryft lub przecieki zewnętrzne przez pierwsze 4 godziny pracy pod obciążeniem.

Historia sukcesu klienta: Sheffield Steel Fabrication
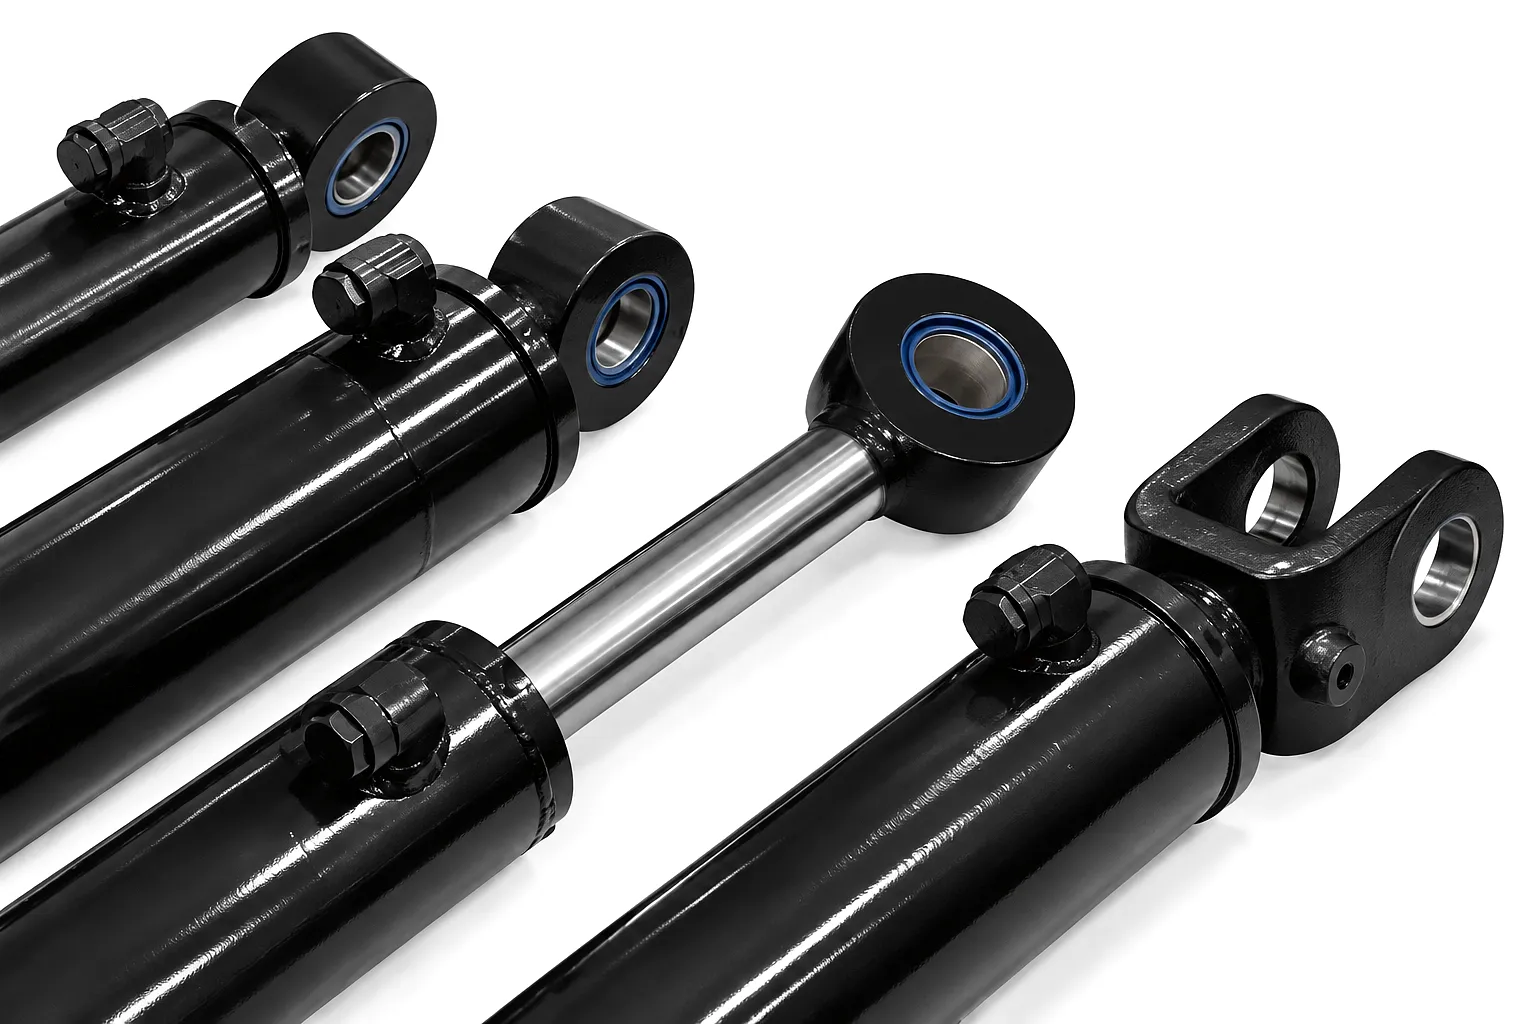
Meridian Steel Structures Ltd — Sheffield, South Yorkshire
Ciężki sprzęt do prasowania i formowania stali konstrukcyjnej

Siłowniki hydrauliczne w obiekcie do długotrwałego magazynowaniaMeridian Steel Structures, firma z siedzibą w Sheffield produkująca stalowe elementy konstrukcyjne do projektów mostowych i infrastrukturalnych, dysponuje serią wielkotonażowych pras hydraulicznych. Podczas 14-miesięcznej przerwy w realizacji dużego kontraktu na budowę mostu – spowodowanej opóźnieniami w zatwierdzeniu projektu nowego węzła autostradowego na północy – dwie z ich 250-tonowych pras zostały wyłączone z eksploatacji. Cylindry hydrauliczne w tych prasach, o średnicy cylindra 180 mm i 220 mm oraz ciśnieniu roboczym 350 barów, pozostały na miejscu bez żadnych formalnych procedur przygotowania do składowania.

Po ponownym uruchomieniu kontraktu, we wszystkich czterech cylindrach obu pras stwierdzono wewnętrzne zanieczyszczenie rdzą w obwodzie hydraulicznym, w dwóch tłoczyskach pojawiły się zadrapania w wyniku korozji wżerowej w pozycji wysuniętej, a w trzech konieczna była całkowita wymiana uszczelnień. Całkowity koszt renowacji przekroczył 22 000 funtów, w porównaniu z szacowanym kosztem zapobiegania poniżej 800 funtów, gdyby od początku przestrzegano formalnej procedury przechowywania.

Po tym doświadczeniu, dział inżynieryjny Meridian nawiązał współpracę z Ever Power w celu wymiany uszkodzonych cylindrów na nowe, wyprodukowane zgodnie z ulepszoną specyfikacją, a także opracowania pisemnej procedury magazynowania na wypadek wszystkich przyszłych przestojów. Ever Power dostarczył cztery zamienne cylindry prasy – dwa o średnicy 180 mm i dwa o średnicy 220 mm, każdy z tłoczyskiem ze stali nierdzewnej 316L, zestawami uszczelnień HNBR i fabrycznie nałożonym wypełnieniem konserwującym – dostarczone do Sheffield w ciągu 11 tygodni od potwierdzenia zamówienia. Zespół inżynierów Ever Power zapewnił również wsparcie na miejscu w zakresie opracowania wewnętrznego dokumentu procedury magazynowania Meridian, który jest obecnie zintegrowany z systemem zarządzania konserwacją ISO 9001.

Od tego czasu miały miejsce dwa kolejne planowane przestoje. W obu przypadkach przestrzegano procedury magazynowania, cylindry sprawdzono przy ponownym uruchomieniu, a wszystkie jednostki przeszły próbę ciśnieniową bez konieczności serwisowania – wynik, który kierownik ds. utrzymania ruchu w Meridian określił jako całkowitą transformację sposobu, w jaki firma zarządza konserwacją zasobów hydraulicznych podczas planowanych przerw w produkcji.

★★★★★

„Zamienne cylindry od Ever Power zostały dostarczone wstępnie napełnione olejem konserwującym i prawidłowo uszczelnione — były gotowe do przechowywania, czego nigdy wcześniej nie widzieliśmy u żadnego dostawcy. Kiedy ponownie je uruchomiliśmy osiem miesięcy później, każdy z nich przeszedł test ciśnieniowy za pierwszym razem”.

James Holroyd
Kierownik ds. konserwacji, Meridian Steel Structures Ltd, Sheffield
★★★★★

„Specyfikacja prętów ze stali nierdzewnej w tych cylindrach okazała się wyjątkowa w naszym środowisku. Przechowujemy sprzęt w pobliżu nadmorskiej stoczni w Immingham, a poprzednie cylindry od innych dostawców wykazywały wżery wżerowe w ciągu sześciu miesięcy. Jednostki Ever Power przeszły już dwa pełne cykle magazynowania bez ani jednego problemu z korozją”.

Rachel Forsythe
Kierownik ds. zaopatrzenia w sprzęt, Humber Bulk Terminals, Immingham
★★★★★

„Zamówiliśmy niestandardowe uszczelnienia HNBR i tłoczysko 316L dla partii cylindrów na zapas buforowy w naszym zakładzie w Birmingham. Zespół techniczny Ever Power pomógł nam w doborze klasy uszczelnień do naszego konkretnego zakresu cieczy i temperatur, a cylindry zostały dostarczone z pełnym certyfikatem magazynowania fabrycznego. Dokładnie to, co powinien zaoferować poważny dostawca przemysłowy”.

Dawid Chatterjee
Kierownik ds. zakupów technicznych, Midland Hydraulic Solutions, Birmingham


Poznaj naszą ofertę cylindrów gotowych do przechowywania
⚙️
Wytrzymałe cylindry jednostronnego działania
Zobacz produkt →


🔼
Niestandardowe teleskopowe cylindry podnoszące
Zobacz produkt →

Kontrola i testowanie jakości cylindrów hydraulicznych

Często zadawane pytania

Jak długo można bezpiecznie przechowywać siłownik hydrauliczny w brytyjskim magazynie przemysłowym, zanim zajdzie konieczność wymiany uszczelnień?+
Siłownik hydrauliczny, który został prawidłowo przygotowany przy użyciu oleju konserwującego, powłoki tłoczyska VCI, solidnych korków portów i folii polietylenowej VCI, może być zazwyczaj przechowywany przez 24 do 36 miesięcy bez wymiany uszczelnień, pod warunkiem, że wilgotność względna w środowisku magazynowym utrzymuje się poniżej 60%, a temperatura od +5°C do +25°C. Bez przygotowania uszczelnienia HNBR i poliuretanowe w typowych warunkach magazynowych w Wielkiej Brytanii zaczynają wykazywać mierzalne twardnienie i zmniejszony powrót do pierwotnego kształtu w ciągu 12 do 18 miesięcy, co przekłada się na ryzyko wycieku po ponownym uruchomieniu siłownika. Certyfikat przechowywania dostarczany przez Ever Power wraz z każdym fabrycznie przygotowanym siłownikiem określa przewidywany okres szczelności uszczelnienia dla konkretnego rodzaju uszczelnienia.
Jaki jest koszt przygotowania cylindra hydraulicznego do składowania i czy opłaca się to firmie produkcyjnej z Birmingham, która ma zapas buforowy?+
Koszt przygotowania typowego cylindra hydraulicznego do przechowywania — obejmujący płukanie i napełnianie olejem konserwującym, preparat VCI do tłoczysk, solidne korki portów i owijkę VCI — zazwyczaj mieści się w przedziale od 35 do 120 funtów za cylinder, w zależności od średnicy i skoku tłoka. Dla porównania, typowy koszt wymiany uszczelki wynosi od 180 do 600 funtów za cylinder, plus ryzyko uszkodzenia wewnętrznego układu hydraulicznego przez zanieczyszczenie, które może znacznie zwiększyć koszty płukania układu, wymiany filtrów i zużycia pompy. Dla każdego producenta z Birmingham lub Wielkiej Brytanii przechowującego zapasy buforowe przez ponad 90 dni, przygotowanie do przechowywania zapewnia zwrot z inwestycji znacznie przekraczający 10:1 w większości rzeczywistych scenariuszy. W przypadku zamówień składanych w Ever Power, fabryczne przygotowanie do przechowywania jest wliczone w cenę dostawy dla zamówień, w których klient określa zastosowanie zapasu buforowego.
Który rodzaj powłoki tłoczysk cylindrów hydraulicznych jest najlepszy pod kątem zapobiegania korozji podczas przechowywania na zewnątrz w Sheffield lub w pobliżu obszarów przybrzeżnych Wielkiej Brytanii?+
W przypadku przechowywania na zewnątrz lub w pobliżu wybrzeża w Wielkiej Brytanii zaleca się zastosowanie podejścia łączonego: mikrokrystaliczny wosk impregnowany VCI nakładany bezpośrednio na pręt chromowy, pokryty szczelną powłoką z folii polietylenowej VCI. Wosk zapewnia fizyczną barierę przed wilgocią, a chemia VCI stale paruje, chroniąc powierzchnię metalu, nawet tam, gdzie bezpośredni kontakt z woskiem jest niedoskonały. W szczególnie agresywnych środowiskach przybrzeżnych w pobliżu Liverpoolu, Teesside lub Aberdeen, pręt ze stali nierdzewnej całkowicie eliminuje podatność chromu na korozję. Skontaktuj się z Ever Power, aby omówić dostępne materiały na pręty, jeśli warunki przechowywania obejmują narażenie na działanie soli morskiej — różnica w cenie między standardowym prętem chromowym a prętem ze stali nierdzewnej jest często niewielka w porównaniu z kosztem renowacji pręta po uszkodzeniu korozyjnym.
Gdzie mogę znaleźć dostawcę cylindrów hydraulicznych w Wielkiej Brytanii, który może przedstawić wycenę cylindrów niestandardowych, już poddanych obróbce fabrycznej?+
Ever Power dostarcza cylindry hydrauliczne klientom w Wielkiej Brytanii — w tym firmom w Birmingham, Sheffield, Manchesterze, Leeds, Bristolu, Liverpoolu oraz w całej Anglii, Szkocji i Walii — z możliwością fabrycznego magazynowania jako określoną opcją dostawy. Aby otrzymać cenę cylindrów niestandardowych z wypełnieniem konserwującym, powłoką VCI tłoczyska i certyfikatem fabrycznego magazynowania, prosimy o kontakt mailowy z działem sprzedaży technicznej pod adresem [email protected], podając średnicę otworu, długość skoku, ciśnienie robocze, preferowany rodzaj uszczelnienia i wymaganą ilość. Oferty są zazwyczaj wysyłane w ciągu 24 godzin w przypadku standardowych specyfikacji i w ciągu 48–72 godzin w przypadku projektów niestandardowych lub projektowanych.
Jak należy umieścić siłownik hydrauliczny przechowywany poziomo na regałach, aby zapobiec jego uszkodzeniom wewnętrznym w okresie sześciu miesięcy lub dłuższym?+
Cylindry hydrauliczne muszą być przechowywane poziomo, z lufą spoczywającą na wyściełanych punktach podparcia — co najmniej gumowych lub blokach HDPE — umieszczonych w zewnętrznych trzecich częściach długości lufy, aby rozłożyć obciążenie z dala od zaślepek. Tłoczysko powinno być w pozycji całkowicie schowanej. Co cztery do sześciu miesięcy należy obrócić cylinder o 90 stopni wokół jego osi podłużnej, aby rozprowadzić warstwę oleju konserwującego na górne powierzchnie wewnętrzne, z którymi olej osiadający grawitacyjnie nie ma już kontaktu. Nigdy nie należy przechowywać cylindrów na gołych stalowych regałach bez podkładek izolacyjnych: kontakt metal-metal między lufą a regałem tworzy punkt styku galwanicznego, który sprzyja korozji i może powodować płaskie miejsca w cienkościennych konstrukcjach beczek. Punkty styku powinny być wyraźnie oznaczone pianką ochronną lub profilami gumowymi, aby wyeliminować przypadkowy kontakt gołego metalu podczas przenoszenia.
Kiedy należy wymienić uszczelki w siłowniku hydraulicznym, który był przechowywany przez ponad 18 miesięcy w brytyjskim magazynie sprzętu do wynajęcia?+
Wymiana uszczelnienia po okresie magazynowania jest konieczna, gdy podczas kontroli ponownego uruchomienia zostanie stwierdzony którykolwiek z poniższych warunków: widoczne pęknięcia lub stwardnienie powierzchni na odsłoniętych obszarach wargi uszczelniającej; niepowodzenie testu utrzymania ciśnienia 1,5x (spadek ciśnienia o ponad 21 TP4T w ciągu 5 minut); ślady wewnętrznego zanieczyszczenia wilgocią w konserwowanym płynie; wyciek z obejścia uszczelnienia tłoczyska podczas cyklu powolnego suwu; lub pomiary twardości Shore'a A na dostępnych elementach uszczelnienia wykazujące wartość o ponad 10 punktów wyższą od oryginalnej specyfikacji. W brytyjskich magazynach wynajmu, w których butle są przechowywane w warunkach mieszanej temperatury bez aktywnej kontroli wilgotności, powszechną praktyką jest wymiana uszczelnień w każdym butlu, który był przechowywany przez ponad 24 miesiące, niezależnie od stanu wizualnego — jako koszt planowej konserwacji, który jest bardziej przewidywalny niż ryzyko awarii w terenie. Ever Power może dostarczyć kompatybilne zestawy uszczelnień do każdego butla z naszej oferty, w tym do butli o konstrukcji niestandardowej, zazwyczaj w ciągu 5 do 10 dni roboczych z dostawą na terenie Wielkiej Brytanii.

Chcesz zaopatrzyć się w gotowe do magazynowania cylindry hydrauliczne z dostawą do Wielkiej Brytanii?

Skontaktuj się z działem sprzedaży technicznej Ever Power, aby otrzymać indywidualną wycenę — w każdej odpowiedzi na zapytanie uwzględniona jest średnica cylindra, skok tłoka, stopień uszczelnienia, specyfikacja konserwacji oraz wysyłka na terenie Wielkiej Brytanii.

Uzyskaj wycenę — [email protected]

edytuj przez gzl

pl_PLPolish