
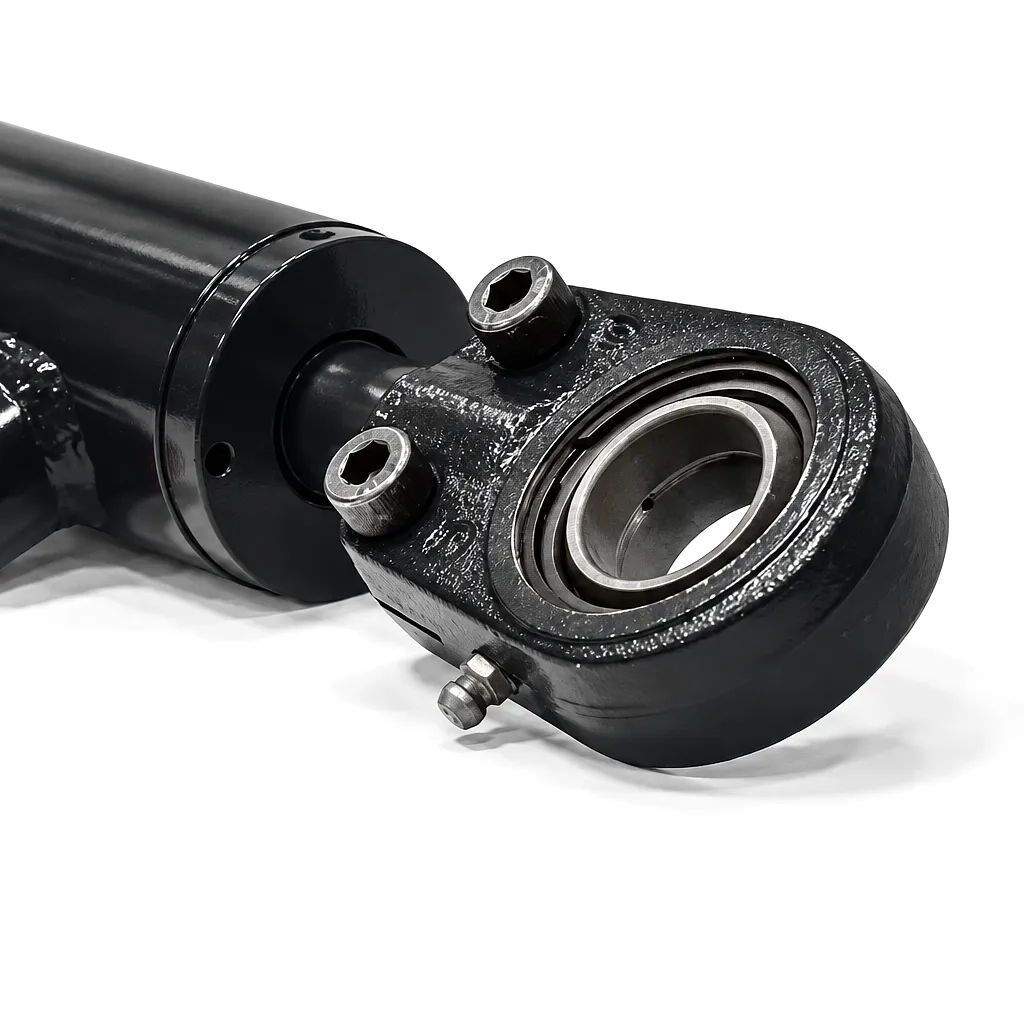
 When a crawler crane lifts hundreds of tonnes on a construction site in Manchester or positions structural steel across a Tyne bridge deck, the hydraulic boom cylinder is doing work that few components in engineering are asked to do. It must extend and retract under enormous axial loads, maintain precise stroke control over many hours of continuous operation, resist fatigue across thousands of cycles, and do all of this in British weather — rain, temperature swings, and the kind of ambient moisture that turns mild steel into a rust problem within months. Boom cylinders are not generic hydraulic actuators bolted into a crane afterthought. They are engineered to exact load ratings, stroke lengths, bore diameters, and mounting configurations that are unique to each crane model, and selecting the wrong specification is not merely a performance issue — it is a safety-critical failure waiting to happen. Understanding what boom cylinders actually do, how their load ratings are calculated, and what criteria matter most when choosing a replacement or upgrade cylinder is essential knowledge for plant engineers, procurement managers, and field service teams across the UK’s heavy lift and construction sectors.
How Boom Cylinders Generate and Manage Force on Crawler Cranes
Hydraulic Principle
A boom cylinder operates on Pascal’s Law: hydraulic fluid under pressure generates a force equal to the working pressure multiplied by the effective piston area. On a crawler crane, the hydraulic pump — typically a variable-displacement axial piston unit running at 350 to 420 bar — delivers pressurised fluid through hardened steel lines to the cylinder’s cap-end or rod-end port. When fluid enters the cap end, it acts on the full bore area of the piston, pushing the rod outward and raising or extending the boom. Retracting the boom routes fluid to the rod-end annular area, which is smaller because the rod itself occupies space, meaning the retract force is always lower than the extend force for the same pressure. This asymmetry is accounted for in every genuine load rating — a fact that is sometimes overlooked by less experienced procurement teams, leading to undersized cylinders that cavitate or blow seals under dynamic retract loads.
Load Rating Mechanics
A boom cylinder’s load rating is not a single number — it is a matrix that accounts for the static lifting force, the dynamic shock load during slewing and load swing, the column load (buckling risk on long-stroke cylinders when the rod is extended), and the thermal load caused by oil temperature rising under sustained high-pressure operation. For a typical 200-tonne crawler crane operating on a UK infrastructure site, the main boom cylinder may be rated at 3,500 kN extend force and 2,200 kN retract force at 400 bar working pressure, with a minimum safety factor of 4:1 on buckling per Euler’s column formula. Ignoring the column load calculation — which depends on stroke length, rod diameter, and end fixing type — is one of the most common causes of rod bending failure on aftermarket cylinders that were selected only by bore and stroke without engineering verification.
Stroke Control
Modern crawler crane boom cylinders incorporate cushioning at both ends of the stroke — a tapered hydraulic metering sleeve that progressively restricts flow as the piston approaches end-of-stroke, preventing the destructive metal-to-metal impact that would otherwise occur when tonnes of moving boom structure reach the mechanical limit. Cushioning geometry is not a commodity detail: the taper angle, sleeve length, and bypass orifice diameter must be matched to the cylinder’s maximum operating speed and the inertia of the boom section it is moving. Cylinders without correctly matched cushioning exhibit pressure spikes that can exceed 600 bar momentarily — enough to rupture seals, fatigue weld joints in the rod, or damage hydraulic fittings. For crawler cranes working on sensitive sites such as railway infrastructure near Birmingham New Street or in proximity to listed buildings, smooth deceleration at end of stroke is both a mechanical necessity and a site safety requirement.
Core Materials That Determine Boom Cylinder Durability
Cylinder Barrel
Cold-drawn seamless steel tube, typically ST52 or E355 (EN 10305-1), honed to Ra 0.4 µm internal finish. Wall thickness calculated to withstand 1.5x working pressure with deformation under 0.01mm. In UK marine or coastal applications, duplex stainless steel (1.4462) is specified to resist chloride-induced pitting.
Piston Rod
Case-hardened and ground 42CrMo4 alloy steel, chrome-plated to 25–35 µm hard chrome thickness then ground to Ra 0.1–0.2 µm. The chrome layer provides the hard, corrosion-resistant surface that seals ride on. For UK outdoor environments, nickel-chrome or ceramic-chrome alternatives with higher Vickers hardness (900–1100 HV) are increasingly specified to resist the salt-laden atmosphere in coastal regions like Plymouth or Aberdeen.
Sealing System
Polyurethane rod seals with PTFE-coated wiper lips resist the abrasion of fine particles common on demolition and construction sites. For high-temperature applications (ambient over 40°C or hydraulic oil above 80°C), Viton (FKM) seals replace standard NBR. Seal kits for boom cylinders on crawler cranes are never universal — bore diameter, pressure rating, and rod surface finish all influence which seal profile performs correctly.
End Caps & Flanges
Forged from S355J2 or 42CrMo4 steel, machined with O-ring face seal (ORFS) or BSP/NPT ports depending on customer system specification. Trunnion pins and clevis mounts are pin-bored to H7 tolerance and case-hardened for wear resistance through thousands of articulation cycles. For UK customers, SAE flange ports are common on newer crane builds but BSP remains prevalent on legacy fleet equipment.
Related Product: Hydraulic Rotary Actuator Steering Cylinder — engineered for precise angular positioning in crane slewing and steering systems, complementing boom cylinder assemblies in multi-axis crawler crane configurations.
Product Technical & Performance Parameter Table
The table below reflects standard performance envelopes for boom cylinders supplied by Ever Power for crawler crane applications in the 50 to 600 tonne lift-capacity range. Custom specifications beyond these ranges are available on request — stroke lengths up to 6,000 mm and bore diameters up to 450 mm have been manufactured for special-purpose crane applications in UK port and offshore sectors.
| Parameter | Small Crane (50–120 t) | Medium Crane (120–300 t) | Heavy Crane (300–600 t) |
|---|---|---|---|
| Bore Diameter (mm) | 80 – 140 | 140 – 220 | 220 – 380 |
| Rod Diameter (mm) | 56 – 100 | 100 – 160 | 160 – 280 |
| Stroke Length (mm) | 600 – 1,800 | 1,200 – 3,200 | 2,000 – 5,500 |
| Werkdruk (bar) | up to 350 | up to 400 | up to 420 |
| Test Pressure (bar) | 1.5x working | 1.5x working | 1.5x working |
| Extend Force Max (kN) | 175 – 540 | 540 – 1,520 | 1,520 – 4,760 |
| Retract Force Max (kN) | 120 – 400 | 400 – 1,050 | 1,050 – 3,200 |
| Operating Temperature (°C) | -25 to +80 | -25 to +80 | -30 to +90 (special) |
| Rod Material | 42CrMo4 + hard chrome | 42CrMo4 + hard chrome | 42CrMo4 / ceramic chrome |
| Barrel Material | ST52 seamless honed | E355 / ST52 | E355 / duplex SS option |
| Seal System | PU + NBR | PU + NBR / FKM option | PU + FKM / PTFE |
| Chrome Layer Thickness (µm) | 25 – 35 | 25 – 40 | 35 – 50 / ceramic |
| Port Standard | BSP / SAE / ORFS | BSP / SAE / ORFS | BSP / SAE / ORFS / NPT |
| Cushioning | Adjustable both ends | Adjustable both ends | Adjustable / fixed geometry |
| Mounting Options | Clevis, trunnion, flange | Clevis, trunnion, flange | Clevis, trunnion, spherical |
Core Technical Advantages of Ever Power Boom Cylinders
High-Precision Honing
Barrel bore honed to Ra 0.4 µm cylindricity, ensuring seal longevity exceeding 5,000 operating hours under rated load in field conditions. Tighter bore geometry means less seal deformation and lower internal leakage across the service life — a measurable energy efficiency gain on crane fleets working long shifts in Humberside port operations or North Sea support vessel handling.
Verified Buckling Resistance
Every long-stroke cylinder (stroke-to-rod-diameter ratio above 10:1) undergoes full Euler buckling verification with a 4:1 safety factor minimum before order release. Rod diameter selection is never left to approximation — FEA simulation is used on cylinders for crawler cranes above 250 tonnes where dynamic side loading from boom swing can add significant lateral force components to the axial rod load.
Corrosion-Grade Finishing
Chrome plating meets DIN EN ISO 1456 and DIN 50960 standards. For UK export-facing or marine-adjacent applications, nickel undercoat (20 µm Ni + 30 µm Cr) or ceramic-chrome composite coatings are offered. External surface painting uses two-pack epoxy primer followed by polyurethane topcoat, rated to 1,000-hour salt spray (ASTM B117) — essential for crawler cranes based on UK coastal sites or working in the Scottish Highlands where summer midge season and autumn rainfall create aggressive micro-corrosion environments.
Pressure-Tested at 1.5x Rating
Each cylinder undergoes hydraulic pressure testing at 1.5 times nominal working pressure before despatch, with no visible deformation, leakage, or seal extrusion permitted. Test certificates are issued as standard, providing the documentation UK plant engineers and site safety inspectors require under LOLER (Lifting Operations and Lifting Equipment Regulations 1998) when validating replacement cylinders for crane SWL certification.
OEM-Compatible Geometry
Ever Power maintains detailed dimensional records for boom cylinders across major crawler crane OEMs including Liebherr, Manitowoc, Kobelco, Tadano, Terex, and Sennebogen. Replacement cylinders are manufactured to match OEM envelope dimensions, port positions, trunnion pin diameters, and cushioning adjustment locations — so the crane returns to service without modification to hose routing or boom structure. This compatibility covers crane models dating back 25+ years, supporting the large fleet of legacy crawler cranes still operating across UK construction and infrastructure sectors.
LOLER-Compliant Documentation
Every Ever Power boom cylinder for UK customers ships with a full material traceability pack — mill certificates for barrel and rod steel, chrome plate inspection report, dimensional inspection report, pressure test certificate, and product drawing with revision history. This documentation package supports PSSR (Pressure Systems Safety Regulations 2000) compliance requirements and streamlines the insurance and site approval processes that UK crane operators must manage before any critical lift.
Boom Cylinder Selection Tips: What Matters and What Gets Missed
01 — Know Your Actual Working Pressure
Many fleet managers specify boom cylinders based on crane rated capacity without verifying the actual hydraulic system working pressure. A crane rated at 250 tonnes might run the main hoist circuit at 380 bar but supply the boom cylinder circuit at only 320 bar through a pressure-reducing valve. Specifying a cylinder for 380 bar on a 320-bar circuit wastes bore area and adds unnecessary weight. Conversely, if a crane system has been uprated by a previous owner without documentation — not uncommon in the UK secondhand crane market — a cylinder originally designed for 300 bar may be exposed to 370 bar, with predictable consequences for seal and port fitting integrity. Always confirm system pressure from the hydraulic schematic, not the crane capacity plate.
02 — Measure the Mounting Envelope Precisely
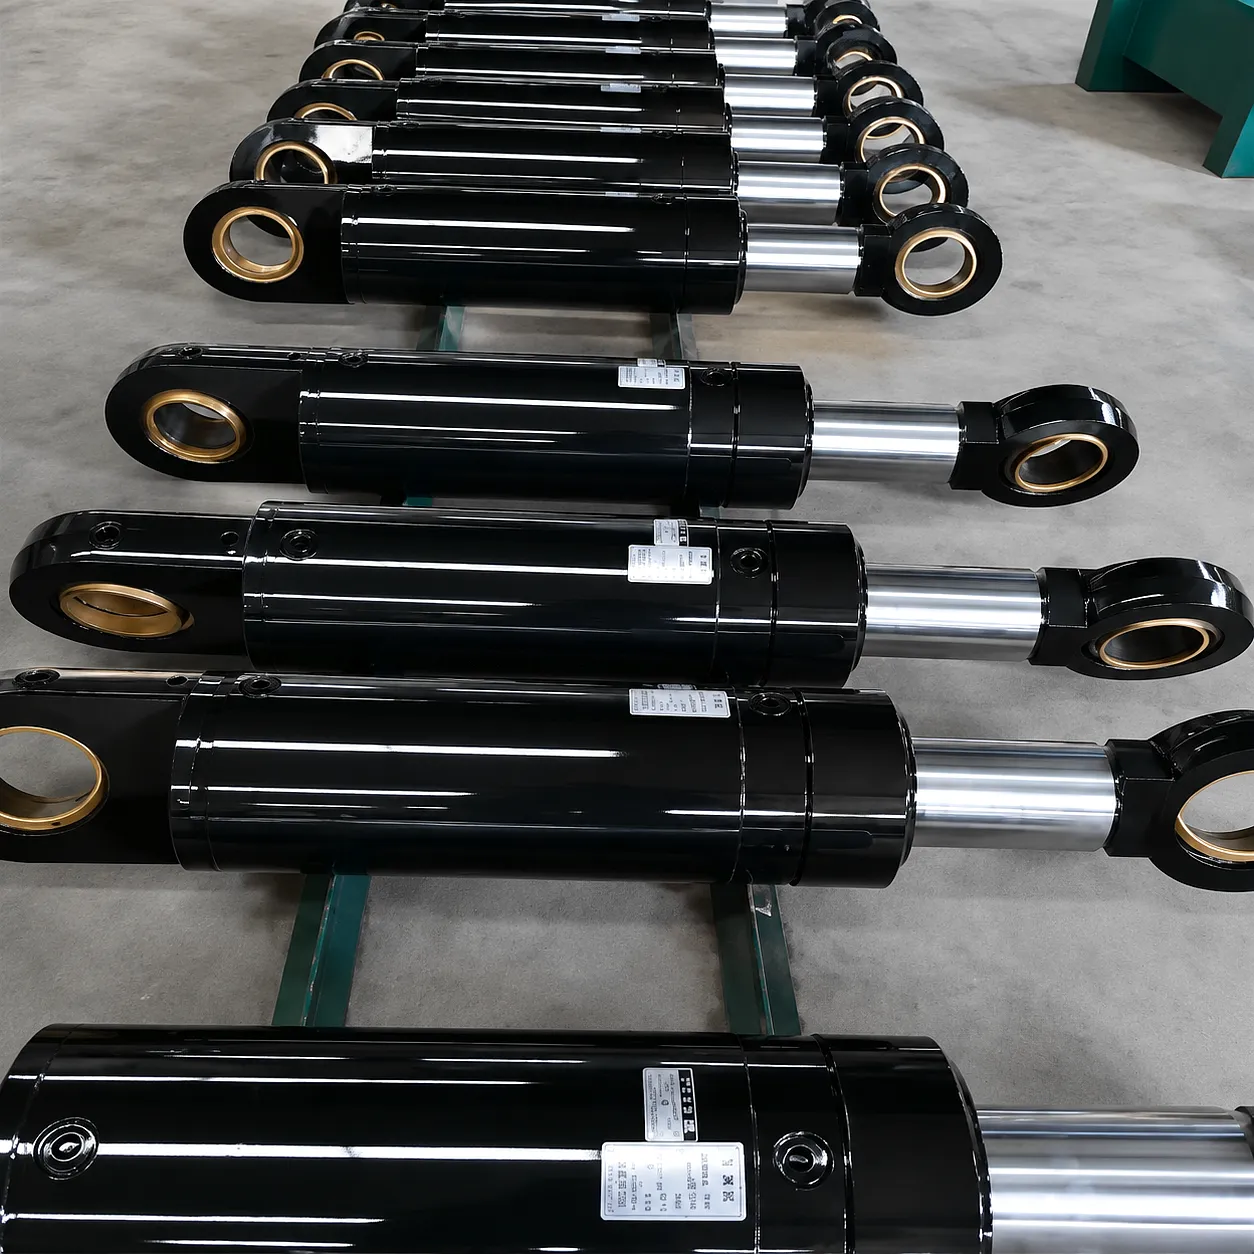
Boom cylinder mounts on crawler cranes are typically clevis-to-clevis or trunnion-to-clevis arrangements with specific centre-to-centre retracted and extended dimensions that are dictated by boom geometry. Even 5 mm of error in retracted length means the boom will not reach its designed minimum angle — a critical issue on cranes where maximum counterweight configuration is load-limited by boom angle. Pin diameter, bore tolerance, and lubricant groove specification in the clevis eye must also match the crane structure’s bronze or composite bush to avoid accelerated wear at the pin joint. Provide complete envelope drawings to Ever Power’s engineering team rather than just bore and stroke dimensions.
03 — Account for Dynamic Load Multipliers
Static load ratings tell only part of the story. A crawler crane slewing at 0.5 rpm with a 200-tonne suspended load introduces dynamic swing forces that the boom cylinder must resist through the hydraulic lock created by counterbalance valves. When those valves open and close, the pressure spike reaching the cylinder can be two to three times the static working pressure for milliseconds at a time. Cylinders must be designed with burst pressure margins — typically 4x working pressure — and port connections must use forged fittings, not cast or welded, to survive these repeated transient loads. On long-duration infrastructure projects like HS2 enabling works or Hinkley Point C construction support, where cranes may cycle continuously for 10-hour shifts, this dynamic fatigue loading is the dominant life-limiting factor for boom cylinders.
04 — Check Fluid Compatibility with Seal Grade
An increasing number of UK construction sites — particularly those operating within SSSI boundaries or near water courses — require fire-resistant or readily biodegradable hydraulic fluids (HEES or HFC types). Standard NBR seals are incompatible with many of these fluids and will swell or degrade within weeks. If you are procuring boom cylinders for a crane that will be operated under an Environmental Management Plan specifying alternative hydraulic fluid, this must be communicated to Ever Power at the enquiry stage so that FKM or EPDM seal kits are specified from the outset. Retrofitting the wrong seal grade after delivery is a preventable cost that the UK crane hire sector encounters regularly.
Industrial Application Scenarios for Boom Cylinders on Crawler Cranes
Nuclear New Build — Somerset & Suffolk
At Hinkley Point C and Sizewell C, crawler cranes in the 500 to 1,000 tonne range lift reactor building modules and containment dome sections. Boom cylinders in these environments must meet nuclear quality assurance requirements, including full traceability of all materials to mill heat numbers, and witnessed pressure testing witnessed by a third-party inspector. Replacement lead times are measured in weeks, making robust cylinders with 2x the standard service life interval critical to project schedule.
Offshore Wind Installation — East Anglia & Dogger Bank
Jack-up vessels and self-propelled heavy lift vessels deploying crawler cranes for offshore wind monopile installation expose boom cylinders to salt spray, high humidity, and temperature cycling that far exceeds typical land-based duty cycles. Boom cylinders used in this sector typically require ceramic-chrome rod coatings, stainless steel port plugs, and epoxy-primed exterior surfaces. The Wind Turbine Hydraulic Pitch Cylinder complements the boom system, controlling blade pitch during installation and commissioning phases where precise angular positioning at height is critical.
Bridge Deck Erection — Sheffield & Northern England
Rail and road bridge deck installation in constrained urban corridors — including viaduct work on the M62, A1 upgrades, and Network Rail projects around Sheffield and Leeds — demands crawler cranes with precise boom angle control to place steel sections within millimetres of target. The boom cylinder’s position directly determines the lift radius at any given counterweight setting, making cushioning quality and positional repeatability more critical than in general construction lift scenarios.
Steel Erection & Industrial Plant — Birmingham & Midlands
The West Midlands manufacturing belt — from Birmingham’s logistics parks to Coventry’s EV battery gigafactories and Staffordshire’s chemical processing plants — maintains a substantial population of crawler cranes for ongoing plant maintenance and capital project execution. These cranes often work with relatively short boom lengths at high loads (high-capacity, low-radius lifts), which places extreme compressive loads on boom cylinders at mid-stroke positions. Cylinder bore sizing must account for these specific loading geometries rather than defaulting to catalogue selections.
Port & Shipyard Heavy Lift — Liverpool & Glasgow
Liverpool’s Freeport and Clydebank’s shipyard redevelopments rely on crawler cranes to shift prefabricated ship sections, port infrastructure modules, and breakwater blocks up to 800 tonnes. In tidal zones and on quayside exposed locations, boom cylinders are subjected to salt-laden wind-driven rain throughout the working day. Epoxy-PVDF coating systems with stainless port plugs and sacrificial anode brackets are standard specification for these environments.
Demolition & Remediation — London & South East
Urban demolition in London — including regeneration schemes at Elephant & Castle, Nine Elms, and along the Thames estuary — uses crawler cranes fitted with demolition accessories including ball weights and hydraulic shears. These attachments create extreme shock loads transmitted back through the boom and into the boom cylinders. Cylinders for demolition-configured crawler cranes should be specified with thicker rod diameters (typically rod-to-bore ratio above 0.65), relief valve protection, and additional port reinforcement at the cylinder body to absorb repeated shock events.
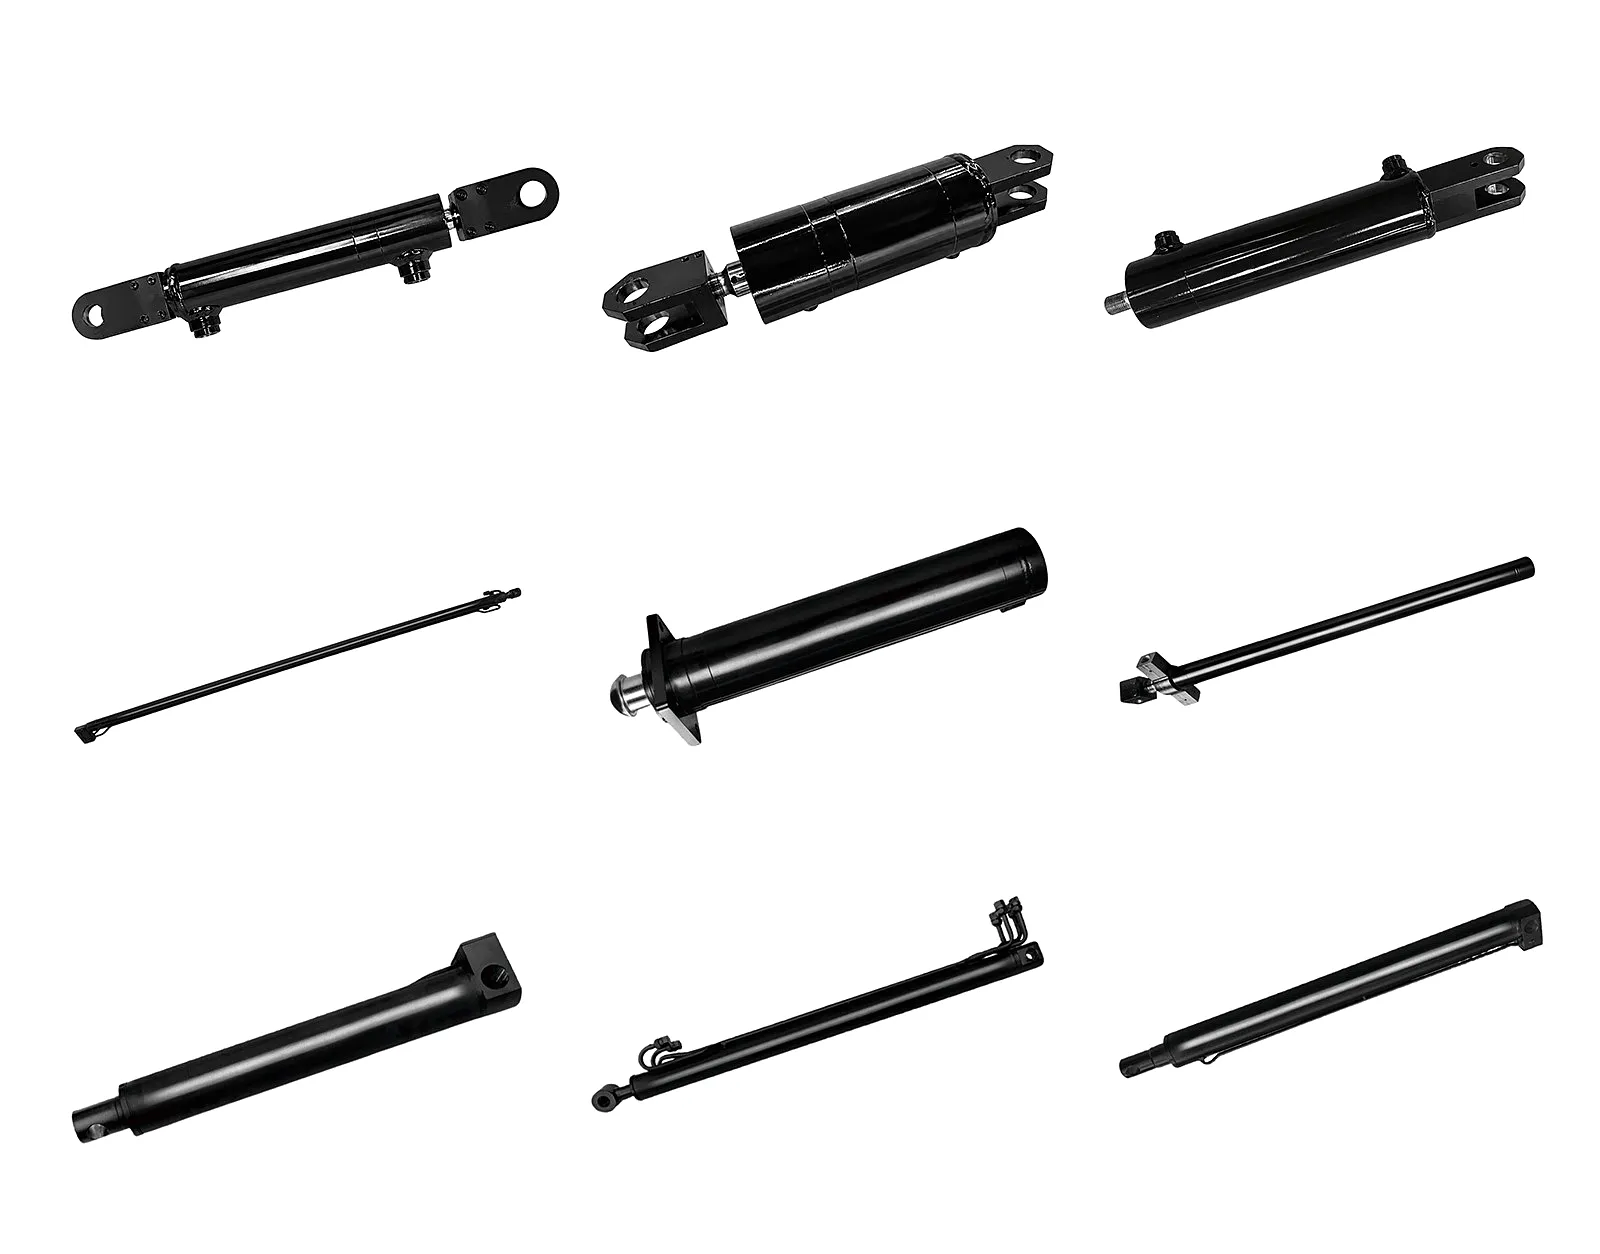
Ever Power Boom Cylinder Product Range — Custom Manufactured for Every Crawler Crane Configuration
Ever Power: Factory Capabilities and Customisation Services
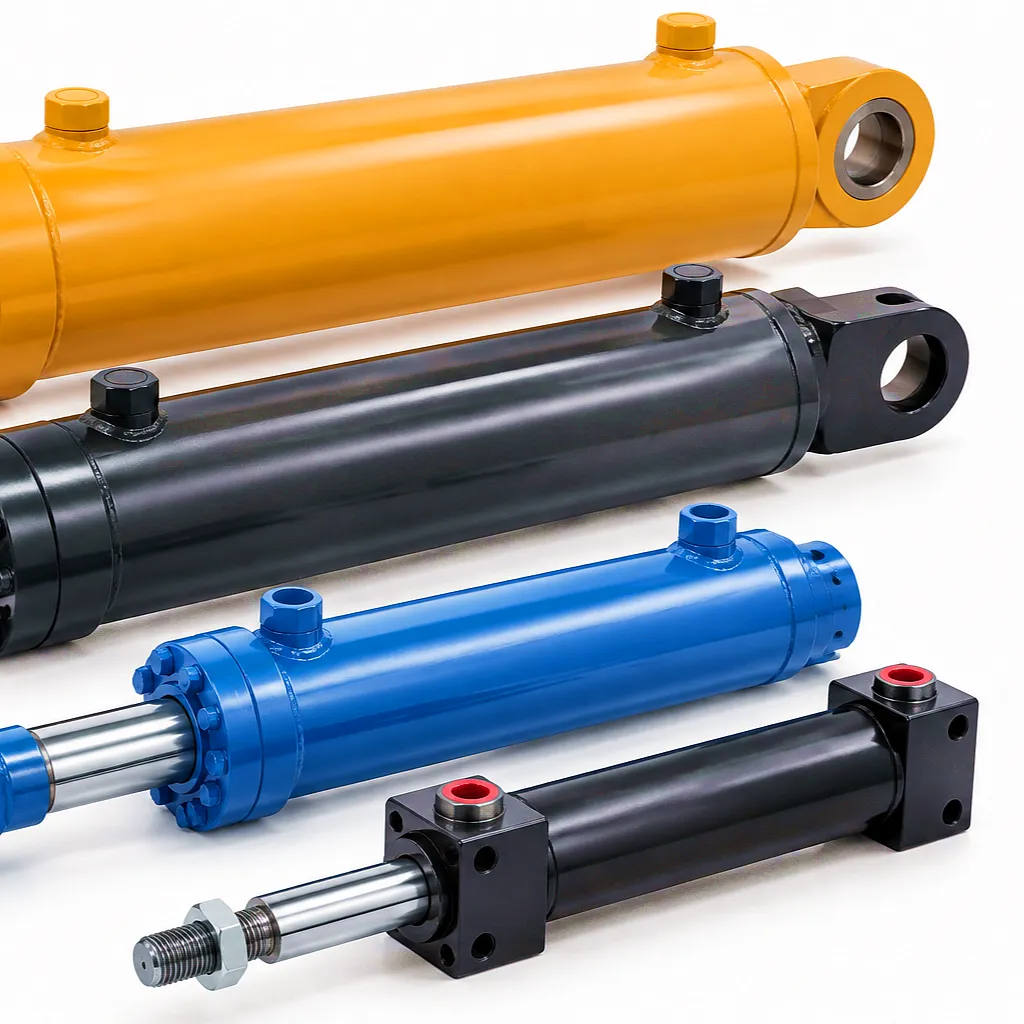
Ever Power operates purpose-built hydraulic cylinder manufacturing facilities with equipment scaled for the demands of heavy crane cylinder production. CNC deep-hole drilling and honing machines handle barrel lengths up to 8,000 mm. Chrome plating tanks accommodate rods up to 6,000 mm in a single uninterrupted plating run, eliminating the join marks and thickness variations that arise when shorter tanks require multiple dip cycles on long rods. Vertical assembly presses with guided alignment fixtures ensure consistent seal fitting across all bore sizes without distortion of the gland or barrel bore.
Full Custom Engineering
From customer-supplied drawings or OEM part numbers, Ever Power’s engineering team produces complete manufacturing drawings, material selection rationale, and FEA summary within 5 working days for most boom cylinder configurations. Non-standard port locations, angled ports, integrated manifold blocks, and position transducer provisions are all within standard customisation scope.
Supply Chain Certainty
Ever Power heeft een voorraad van gangbare cilinderdiameters, verchroomde stangblanks en afdichtingssets voor de meest gebruikte boringdiameters op Liebherr-, Manitowoc- en Kobelco-rupskranen. Deze voorraadstrategie verkort de levertijd voor herhaalbestellingen tot 3-6 weken, vergeleken met de gebruikelijke 16-20 weken bij OEM-inkoop via Europese distributeurs. Dit biedt een doorslaggevend voordeel wanneer een kraan in een Brits project onverwacht buiten gebruik raakt.
Inspectie en certificering
Een inspectie door een onafhankelijke derde partij, zoals SGS, Bureau Veritas of Lloyd's Register, is op aanvraag beschikbaar. Complete materiaaltraceerbaarheidsdocumenten, dimensionale inspectierapporten, druktestcertificaten en inspectierapporten van het verfsysteem worden standaard voor alle bestellingen van kraancilinders in het Verenigd Koninkrijk opgesteld, klaar voor indiening bij de veiligheids- en verzekeringsteams op de bouwplaats.
Vraag een offerte aan voor een giekcilinder op maat bij Ever Power.
Deel uw boring, slag, werkdruk, OEM-referentienummer of bestaande cilinderafmetingen — ons team reageert binnen 24 uur.
Klantsuccesverhaal: Snelle cilindervervanging tijdens een stilstand van een petrochemische fabriek in Teesside
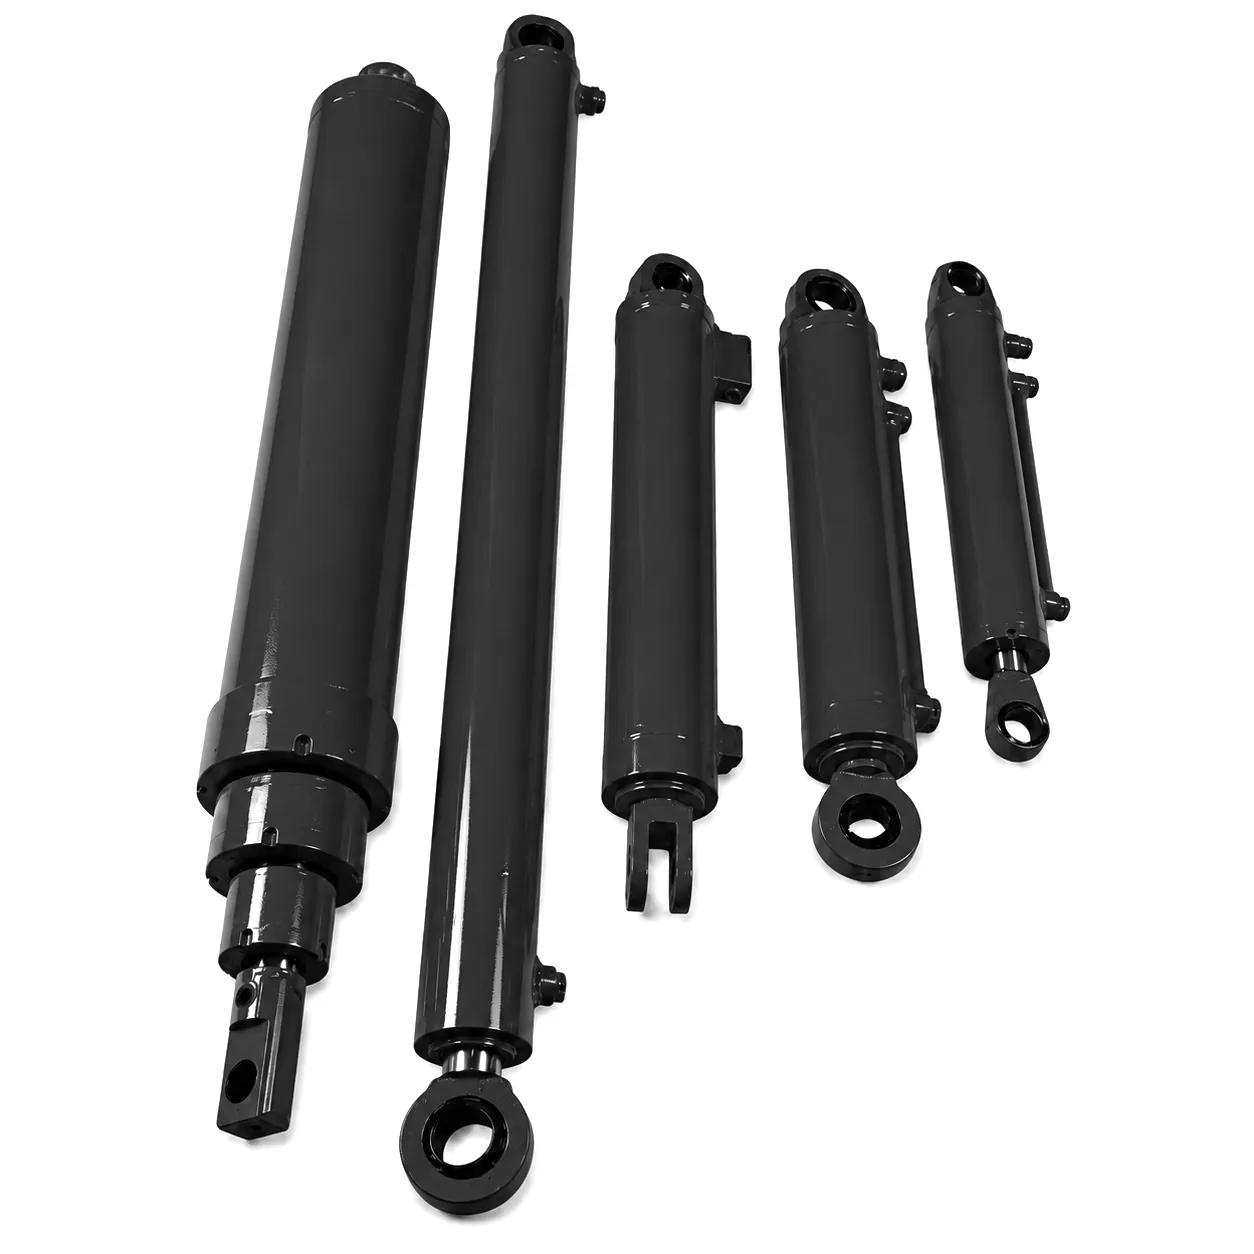
Een groot kraanverhuurbedrijf uit Middlesbrough had een Liebherr LR 1300 rupskraan ingezet voor een gepland onderhoudsprogramma bij een grote petrochemische fabriek in Teesside. De kraan was 17 dagen bezig met een programma van 26 dagen toen er aan het einde van een werkdag een interne lekkage ontstond in de primaire giekverstelcilinder, die de zuigerafdichtingen lekte. Dit bleek uit de overmatige drijfstangverplaatsing onder belasting en de stijgende olietemperatuur in het cilindercircuit. De werkzaamheden van de kraan maakten deel uit van een geplande onderhoudsstop die de klant meer dan £200.000 per dag aan productieverlies kostte. De levertijd voor een vervangende cilinder werd door de Duitse fabrikant geschat op 14 tot 16 weken.
Het kraanteam van Middlesbrough nam contact op met Ever Power nadat een voormalige collega hen had aangeraden een vervangende giekcilinder via het bedrijf te bestellen. Het engineeringteam van Ever Power bevestigde de boring (220 mm), stang (160 mm), slag (2640 mm) en de geometrie van de scharnierbevestiging aan de hand van foto's en dimensionale metingen die ter plaatse waren uitgevoerd, binnen 90 minuten na het eerste telefoongesprek. Een vervangende cilinder die aan alle OEM-afmetingen voldeed, bleek op voorraad te zijn als een onbewerkte assemblage – met geboorde cilinder, geslepen en verchroomde stang en gefreesde eindkappen – die alleen nog gemonteerd hoefde te worden, inclusief het plaatsen van de afdichting en een druktesten.
De complete, geteste en gecertificeerde vervangende giekcilinder werd binnen 4 dagen na de eerste aanvraag per luchtvracht vanuit de fabriek van Ever Power naar Teesside Airport verzonden. De kraan was op de zesde dag van de ongeplande stilstand weer in gebruik, waardoor de klant naar schatting £ 2,2 miljoen aan extra kosten voor de stilstand bespaarde in vergelijking met de levertijd van de OEM. De cilinder heeft sindsdien meer dan 3.000 bedrijfsuren zonder problemen gedraaid en is als standaardvervangingsonderdeel in gebruik genomen voor twee andere LR 1300-kranen in het Britse wagenpark van hetzelfde verhuurbedrijf.
Wat Britse klanten zeggen over Ever Power giekcilinders
★★★★★
“De vervangende giekcilinder die Ever Power voor onze LR 1300 leverde, functioneerde vanaf de eerste dag feilloos. De concentriciteit van de boring en de chroomafwerking waren visueel superieur aan het origineel, en het certificaat van de druktest werd meegeleverd – precies wat het veiligheidsteam van onze klant nodig had voor de LOLER-regelgeving. Op een petrochemische locatie waar lekkage van cilinders in de buurt van hete proceszones absoluut niet is toegestaan, gaf de kwaliteit van de afdichting ons volledig vertrouwen.”
— Fabrieksdirecteur, specialistisch kraanverhuurbedrijf, Middlesbrough
★★★★★
“We hebben Ever Power ingeschakeld voor de vervanging van drie giekcilinders van de Manitowoc 18000-kranen op onze vloot die werkzaam is bij de offshore windparkprojecten in de Humber-regio. De op maat gemaakte scharniergeometrie paste perfect op onze kraanconstructies – geen opvulstukken of aanpassingen aan de bussen nodig. Wat ons het meest imponeerde, was dat het team van Ever Power een afwijking in onze meting van de lengte van de transmissiestang opmerkte en ons hierop attent maakte vóór de productie. Die aandacht voor detail is precies wat je nodig hebt bij het bestellen van structurele kraanonderdelen met een lange levertijd.”
— Fleet Engineering Manager, Operator van zware hijskranen, Hull
★★★★★
“Onze Kobelco CKE2500G vertoonde na 12.000 uur een langzame lasbreuk in de originele cilinderbehuizing van de giek. We ontvingen maattekeningen van Ever Power, kwamen een volledige revisie overeen met een verbeterde wanddikte en kregen de nieuwe cilinder binnen 6 weken geleverd – een opmerkelijke doorlooptijd voor een cilinder met een boring van 250 mm en een slag van 3.800 mm. De cilinder heeft nu nog eens 4.500 uur gedraaid op onze kraan voor de voorbereidende werkzaamheden aan de HS2, zonder dat er ook maar één afdichting vervangen hoefde te worden. De keramisch-chroom coating van de stang was duidelijk de juiste keuze voor de stoffige en schurende omstandigheden op de aanlooproute naar de Chiltern Tunnel.”
— Senior hydraulisch ingenieur, aannemer civiele infrastructuur, Birmingham
Related Product: Hydraulic Rotary Actuator Steering Cylinder — gebruikt in kraanonderstellen en rijsystemen waar nauwkeurige hoekregeling van de rupsbanden vereist is op hellend of krap terrein.
Veelgestelde vragen
Hoe bereken ik de juiste belastingscapaciteit voor een giekcilinder op mijn rupskraan in het Verenigd Koninkrijk?
Voor de berekening van de maximale belasting zijn vier gegevens nodig: de maximale hydraulische systeemdruk die het cilindercircuit voedt (in bar), de boringdiameter voor de uitschuifkracht of het ringoppervlak voor de intrekkracht, de verwachte dynamische belastingsvermenigvuldiger op basis van de zwenksnelheid van de kraan en de traagheid van de hangende last, en de Euler-knikveiligheidsfactor voor de combinatie van slag en stangdiameter. Het engineeringteam van Ever Power voert deze berekening kosteloos uit voor elke aanvraag met volledige dimensionale gegevens en systeemdrukgegevens. Voor Britse klanten die onder LOLER werken, maakt het resulterende belastingcertificaat deel uit van de documentatie van het keuringsschema van de kraan.
Wat is de gebruikelijke prijs voor een vervangende giekcilinder voor een rupskraan van 300 ton in het Verenigd Koninkrijk, en waar kan ik een offerte aanvragen?
De prijs van giekcilinders voor rupskranen van 300 ton varieert aanzienlijk, afhankelijk van de boringdiameter (doorgaans 200-260 mm), de slag (meestal 2.500-4.000 mm), de specificaties van de stangcoating en de documentatievereisten. Over het algemeen beginnen budgetvriendelijke aftermarket-units zonder certificering door een derde partij onder de prijzen van premium OEM-onderdelen, terwijl een volledig gedocumenteerde, drukgeteste en gecertificeerde vervangingscilinder van Ever Power – inclusief verchroomde stang tot 35 µm, compleet afdichtingssysteem en traceerbaarheidspakket – concurrerend is ten opzichte van de prijzen van Europese OEM-onderdelen en aanzienlijk kortere levertijden biedt. Neem contact op met [email protected] met uw OEM-referentie of cilinderafmetingen voor een specifieke offerte binnen 24 uur.
Welke leverancier van giekcilinders in het Verenigd Koninkrijk kan binnen zes weken een gecertificeerde vervangingseenheid leveren voor een Liebherr LR 1600?
Ever Power heeft voorgefabriceerde cilinder- en stangblanks op voorraad in de gangbare boringmaten voor Liebherr LR-serie rupskranen. Voor de LR 1600 vallen de standaard boringmaten van de giekcilinder binnen het assortiment van Ever Power, waardoor de eindmontage, het afdichten, de druktesten en de documentatie binnen 3 tot 5 weken na orderbevestiging kunnen worden voltooid – ruim binnen de levertijd van zes weken. Levering naar elke locatie op het Britse vasteland wordt geregeld via temperatuurgecontroleerd transport, waarbij de cilinder wordt verzonden in een op maat gemaakte houten kist met beschermende eindkappen en een roestwerende olievulling.
Wanneer moet ik de afdichtingen van de giekcilinder van een rupskraan op een bouwplaats in Birmingham vervangen, en hoe kan ik vroegtijdig defecten aan de afdichtingen herkennen?
De vervangingsintervallen van afdichtingen op giekcilinders zijn afhankelijk van het aantal bedrijfsuren, de omgevingstemperatuur, de zuiverheid van de vloeistof en de conditie van het stangoppervlak. Bij rupskranen die continu in ploegendienst werken in stoffige stedelijke omgevingen zoals sloop- of herontwikkelingslocaties in Birmingham, is een levensduur van 2.000 tot 4.000 uur voor polyurethaan stangafdichtingen typisch. Vroege tekenen van slijtage van de afdichting zijn onder andere een oliefilm op het stangoppervlak die langer aanhoudt dan de normale werking van de wisserafdichtingen, stangafwijking onder belasting (de cilinder houdt zijn positie niet vast onder statische belasting zonder actieve druk), een stijgende circuittemperatuur als gevolg van interne bypass en zichtbare olieverontreiniging op de giekconstructie onder de cilinderafdichting. Door deze tekenen vroegtijdig te herkennen, wordt beschadiging van de stang voorkomen, wat de levensduur van de afdichting aanzienlijk verkort.
Wie zijn de meest betrouwbare leveranciers van hydraulische cilinders voor rupskranen die actief zijn in de Britse offshore wind- en petrochemische sector?
Voor offshore wind- en petrochemische toepassingen in het VK betekent een betrouwbare cilinderlevering gedocumenteerde kwaliteit – niet alleen een concurrerende prijs. De belangrijkste onderscheidende kenmerken zijn de beschikbaarheid van inspecties door derden (SGS, Bureau Veritas, Lloyd's), volledige traceerbaarheid van het materiaal tot op chargenummer, druktesten bij 1,5 keer de werkdruk als standaardonderdeel in plaats van een premium optie, en specifieke corrosiebeschermingspakketten die geschikt zijn voor maritieme en procesinstallatieomgevingen. Ever Power levert gecertificeerde giekcilinders aan kraanmachinisten in het VK in beide sectoren, waarbij inspecties door derden worden gecoördineerd via in het VK gevestigde instanties om de documentatieketen te waarborgen die vereist is voor de leveranciersgoedkeuringsprocessen van grote klanten in de Britse energiesector.
Welke documenten heb ik nodig van een leverancier van giekcilinders om in het Verenigd Koninkrijk een grondige LOLER-keuring te doorstaan na het monteren van een vervangende cilinder?
Voor een grondige LOLER-keuring na vervanging van een giekcilinder heeft de keurder doorgaans de volgende documenten nodig: een conformiteitsverklaring of conformiteitscertificaat voor de cilinder, het certificaat van de hydraulische druktest met vermelding van testdruk, duur en resultaat, een dimensionaal inspectierapport dat bevestigt dat de cilinder voldoet aan de gespecificeerde geometrie, materiaalcertificaten (EN 10204 3.1 of 3.2) voor het cilinderstaal en het stangstaal, en het specificatierapport van de afdichting. Ever Power levert dit complete documentatiepakket standaard bij elke cilinder die aan Britse klanten wordt geleverd. De documenten zijn zo opgemaakt dat ze direct bruikbaar zijn voor de door de verzekeraar erkende keurder, waardoor het heen en weer gecommuniceerd met buitenlandse leveranciers, dat vaak de LOLER-goedkeuring vertraagt en ervoor zorgt dat kranen langer dan nodig buiten gebruik blijven, wordt vermeden.
Ever Power — Precisie hydraulische cilinders voor zware lasten
Bent u klaar om uw volgende giekcilinder te specificeren?
Deel uw boring, slag, werkdruk en OEM-referentienummer. Ons engineeringteam reageert binnen 24 uur met een technische bevestiging en een concurrerende offerte.
✉ Vraag een offerte aan — [email protected]
bewerkt door gzl
 Dutch
 English
 Italian
 Portuguese
 Swedish
 Danish
 Finnish
 Polish
 Hindi
 Kazakh
 Turkish
 Ukrainian
 Romanian
 Spanish
 German
 Russian
 Korean
 Japanese
 Vietnamese
 Thai
 Indonesian
 Malay
 French
 Greek